china backpack manufacturer
Home

Blog

Blog

  • What Does PFAS-Free Mean?
    What Does PFAS-Free Mean? Nov 18, 2026
      PFAS-free (free of per- and polyfluoroalkyl substances) is a claim or certification mark meaning that no PFAS has been intentionally added to a product, and that testing confirms any residual content is below the limit of detection or below specific strict thresholds. PFAS are a class of man-made chemicals known as "forever chemicals." Widely used for their water-, oil-, and heat-resistant properties, they resist degradation in the environment and may pose risks to human health. What qualifies as "PFAS-free"? Currently, there is no unified, mandatory legal definition of "PFAS-free" worldwide. Mainstream third-party certification bodies generally evaluate products on two levels: •Supply-chain declaration — proving "no intentional use." The company must demonstrate that no PFAS was intentionally used in its production or sourcing processes. •Finished-product testing — below trace limits. SGS certification, for example, requires total fluorine (TF) below 20 ppm, or total targeted PFAS below 25 ppb (depending on the test method). NSF certification likewise requires total organic fluorine (TOF) to approach zero detection. Contents •What is PFAS, and why is it in the textile industry? •How do you achieve PFAS-free? •Does going fluorine-free compromise performance? •2026 global regulations explained •How we help bag brands achieve PFAS compliance •FAQ •Conclusion   1. What Is PFAS, and Why Is It in the Textile Industry?   1.1 Definition and characteristics PFAS stands for per- and polyfluoroalkyl substances — a large family of synthetic chemicals defined by at least one fully fluorinated carbon atom (—CF2— or —CF3) in the molecular structure, with more than 10,000 known variants. Familiar members of the family include PFOA (perfluorooctanoic acid), PFOS (perfluorooctane sulfonic acid), and PTFE (polytetrafluoroethylene). The defining feature of PFAS is the carbon–fluorine bond (C–F), one of the strongest bonds in organic chemistry. It gives PFAS two "superpowers": •Extreme stability: resistant to heat, acids, alkalis, and oxidation, with virtually no degradation in nature — hence the name "forever chemicals"; •Exceptional surface performance: simultaneously repelling water, oil, and stains, which makes PFAS the most effective raw material ever used in water-, oil-, and stain-repellent finishes. 1.2 Typical applications of PFAS in bag fabrics For the bag industry, PFAS are used widely. Common applications include: •DWR (durable water repellent) finishes: the "lotus-leaf effect" water repellency on backpacks and travel bags has traditionally relied on fluorinated (C8/C6) water repellents; •Triple-protection finishes: oil- and stain-resistant treatments, common on laptop bags, cosmetic bags, and diaper bags; •Coating and lamination: fluorinated auxiliaries used in certain PU/PVC coating processes; •Zippers, webbing, and sewing thread: these accessories may also carry fluorinated finishes; •Membranes: PTFE-based waterproof-breathable membranes (used in some premium outdoor fabrics). 1.3 Why restrict PFAS? The stability of the carbon–fluorine bond is a double-edged sword. Once released into the environment, PFAS barely break down and accumulate through water systems and the food chain. Certain PFAS (such as PFOA and PFOS) have been linked to immunotoxicity, endocrine disruption, and liver and kidney damage. Both PFOA and PFOS are listed under the Stockholm Convention on Persistent Organic Pollutants (POPs) and are banned or severely restricted worldwide. In addition, the production of fluorinated water-repellent finishes is itself a significant industrial source of PFAS emissions.   2. How Do You Achieve PFAS-Free?   2.1 Formulation: switch to "C0" water repellents In the bag industry, C8, C6, and C0 refer to the length of the fluorocarbon chain in a water repellent: C8 is the original long-chain chemistry (now largely phased out), C6 is the short-chain replacement (still a PFAS), and C0 is a fluorine-free water repellent. Switching to fluorine-free (C0) finishes is widely recognized in the Customized bag industry as the most direct technical route. In principle, fluorine-free repellents rely on long-chain alkyl, polyurethane, or polyacrylate structures to form a low-surface-tension layer on the fiber, creating the "lotus-leaf" water-repellent effect. Compared with fluorinated finishes, their water repellency can approach similar levels, but oil and stain resistance is inherently weaker — which is why fluorine-free adoption has been slower in categories with high stain-resistance requirements, such as laptop bags and cosmetic bags. Brands should first clarify the true functional priorities of the product: if water repellency is the core need, fluorine-free solutions are relatively mature; if oil and stain resistance is also essential, achieving it usually requires changes to fabric construction or additional functional finishes, rather than relying on a single water-repellent agent.   2.2 Process •Pre-treatment: Fluorine-free repellents are far more sensitive to pre-treatment cleanliness than fluorinated systems. Residual sizing, incompletely scoured oils, dye residues, and even calcium and magnesium ions in the water compete for adsorption with the active ingredients, preventing uniform film formation on the fiber surface. The visible results are low initial spray ratings, patchy "water marks," or uneven repellency. When switching to fluorine-free, the thoroughness of pre-treatment washing often matters more than repellent selection itself; an extra soaping step, or adjusted washing temperature and cycles, may be needed to ensure a clean, evenly hydrophilic fabric surface. •Curing: Curing parameters must be reset as well. Crosslinking and orientation of fluorine-free finishes on the fiber require sufficient, uniform heat input. Under-curing produces a weak film whose performance decays rapidly with washing; excessive or uneven heat can cause a harsh hand feel, shade change, or loss of strength. •Production-line changeover: Fluorine-free processing is extremely sensitive to cross-contamination. If a stenter or finishing bath previously handled fluorinated agents and was not thoroughly cleaned, residual fluorine alone can push total fluorine test results over the limit. Cleanliness management on the process side is, in effect, a precondition for passing compliance testing after a fluorine-free switch. 3. Does Going Fluorine-Free Compromise Performance? This is brands' most common concern. Objectively speaking: •Water repellency: modern fluorine-free DWRs (C0, silicone-, wax-, dendrimer-, and polyurethane-based) can achieve initial spray ratings comparable to fluorinated products (e.g., 90–100 in spray tests) — more than enough for everyday backpacks and commuter bags; •Wash durability: fluorine-free finishes decay slightly faster after washing; performance can be reactivated by tumble drying or low-temperature ironing, or improved by choosing durable formulations; •Oil and stain resistance: this is the genuine weakness of fluorine-free technology — no fully equivalent replacement for the oil repellency of carbon–fluorine bonds currently exists. For categories with demanding oil-resistance requirements (such as outdoor cookware storage or industrial protective bags), compensation comes through dense fabric constructions, soil-release finishes, or liner design. Category recommendations: Category Recommended approach City commuter bags, laptop bags C0 fluorine-free DWR is sufficient; no perceptible performance difference Outdoor backpacks, travel bags High-performance fluorine-free DWR + water-repellent zippers + structural waterproofing Diaper bags, cosmetic bags Fluorine-free triple-protection alternatives; prioritize stain-resistant, soil-release finishes Professional protective / industrial use Monitor "essential use" exemptions in national regulations, but assess long-term supply risks   4. 2026 Global Regulations Explained Below is a market-by-market summary of the regulatory requirements and timelines directly relevant to bag products.   4.1 European Union: a multi-layered regulatory web (1) POPs Regulation (in force): Regulation (EU) 2019/1021 has long prohibited the use of PFOS, PFOA, PFHxS, their salts, and precursor substances on the EU market (subject to specific exemptions). (2) REACH Annex XVII Entry 79 — PFHxA restriction: Commission Regulation (EU) 2024/2462 provides that, from 10 October 2026, textiles, leather, fur, and footwear placed on the market for the general public must not contain PFHxA and its salts above 25 ppb in total, or PFHxA-related substances above 1,000 ppb in sum. PFHxA is the typical degradation product of C6 repellents, so this rule effectively restricts the use of short-chain fluorinated finishes in EU consumer applications.   (3) Universal PFAS restriction proposal (in progress): submitted in 2023 by Denmark, Germany, the Netherlands, Norway, and Sweden, this REACH restriction proposal targets all roughly 10,000 PFAS. Latest progress: ECHA's Risk Assessment Committee (RAC) adopted its final opinion in March 2026, confirming that the risks are sufficient to support a strict restriction; the Committee for Socio-Economic Analysis (SEAC) is expected to deliver its final opinion by the end of 2026, after which the proposal enters the European Commission's legislative process. The industry generally expects adoption around 2028–2029 — the "final act" hanging over all fluorinated materials. (4) PPWR packaging regulation: from 12 August 2026, the EU Packaging and Packaging Waste Regulation (PPWR) imposes PFAS limits on food-contact packaging. The direct takeaway for bag brands: EU PFAS controls are spreading across all product categories.   4.2 France: the first national ban in force Law No. 2025-188 (adopted in February 2025) and its implementing Decree No. 2025-1376 are currently the world's most aggressive consumer-product PFAS legislation: Timeline Requirement 1 January 2026 Ban on manufacturing, importing, and selling cosmetics, clothing textiles, footwear, waterproofing products, and ski waxes above PFAS thresholds 31 December 2026 Sell-through deadline for stock produced before 2026 1 January 2030 Ban extends to all textiles (except industrial and defense protective uses)   Content thresholds (aligned with the EU PPWR): •Any single PFAS (excluding polymers): < 25 ppb •Sum of all PFAS (excluding polymers): < 250 ppb •Sum of all PFAS (including polymers): < 50 ppm, equivalent to 50 mg/kg total fluorine   4.3 Denmark: total fluorine as the benchmark From 1 July 2026, Denmark prohibits the import and sale of clothing, footwear, and waterproofing products with total fluorine content at or above 50 mg/kg. Using "total fluorine" as the criterion means fluorine from any source — including fluoropolymers — counts toward the limit.   4.4 United States: dense state-level legislation •California AB 1817: from 1 January 2025, intentionally added PFAS is banned in textiles (apparel, bedding, towels, etc.), and manufacturers must provide a certificate of compliance (CoC); outdoor apparel for severe wet conditions has a transition period through 1 January 2028. California's threshold is expressed as total organic fluorine (TOF) in ppm and tightens over time. •New York S5648: from 1 January 2025, the sale of apparel with intentionally added PFAS is banned; extreme-condition outdoor apparel follows in 2028. •Vermont Act 131: from 1 January 2026, intentionally added PFAS is banned across multiple product categories, including textiles, cosmetics, and juvenile products. •Other states: Washington, Colorado, Maine, and others have their own bans or reporting requirements (Maine requires reporting of intentionally added PFAS in products from 2026). The US market is characterized by parallel state rules with inconsistent definitions. Brands typically standardize their supply to the strictest standard (dual control of total fluorine and intentional use) to avoid the complexity of splitting inventory by state.   5. How We Help Bag Brands Achieve PFAS Compliance   5.1 Inquiry stage — declare the standard early We recommend that brands state their specific compliance requirements and target markets at the inquiry stage of a waterproof backpack OEM project. Fluorine-free water repellency usually requires custom development — off-the-shelf water-repellent fabrics rarely qualify — so the standard must be locked in at this stage.   5.2 Sampling stage — sample testing For larger backpack OEM/ODM projects, fluorine-free fabrics can be custom-developed against the target market's regulatory standards and submitted for targeted testing; costs are typically high, making this approach best suited to volume orders. Recommended test standards: total fluorine only tells you "is there fluorine," not "which PFAS." Choose the method by material: •Textiles: EN 17681-1:2025 (the current mainstream EU method), GB/T 31126.1-2025 (Chinese national standard); •Leather and coated leather: ISO 23702-1:2023. Test reports should come from an ISO/IEC 17025-accredited laboratory and correspond to specific production batches.   5.3 Pre-production stage — bulk sample testing Passing at the sampling stage only proves that the swatch or custom fabric meets the standard. For volume bag buyers, passing pre-production bulk-sample testing is the most critical step in locking compliant fabric into production. Bulk production often involves different fabric lots and dye lots, plus re-sourced accessories such as zippers, webbing, and sewing thread. Any process adjustment in any link can push total fluorine or targeted PFAS content back over the limit. The point of pre-production testing is therefore not to re-confirm the compliance of the material itself, but to verify that the actual combination of fabrics, accessories, and processes used in production remains consistent with the sampling stage.   5.4 Production stage — segregated incoming-material control Once bulk production begins, the focus of compliance management shifts from "verifying samples" to "holding the batches." Segregated incoming-material control physically isolates PFAS risk at both the warehouse and the production line: •Material segregation: store approved fluorine-free fabrics and accessories separately from materials awaiting testing, with dedicated labels and color coding to prevent mixing or misuse; •Line segregation: fluorine-free orders should, in principle, run on dedicated lines or in dedicated time slots; •Supplier segregation: fix the source and formulation of each material, avoiding untraceable differences in total fluorine between "same-named" fabrics from different suppliers. With these four stages under control, a brand can compress PFAS risk from the "uncontrollable raw-material end" down to a "traceable batch end" — achieving a closed loop of traceability from raw material to production. 6. FAQ   Q1. Is PFAS-free certification mandatory for the bag industry? Apart from a few markets such as France and Denmark, which set mandatory limits by law, there is no unified mandatory "PFAS-free" certification worldwide. Certifications from bodies such as SGS and NSF are voluntary; their value lies in providing verifiable, third-party evidence for both "no intentional use" and "below the limit."   Q2. Does C0 equal PFAS-free? C0 is a formulation-level attribute — a precondition for PFAS-free, but not a sufficient condition on its own. Only when formulation, process, and testing all close the loop can C0 be converted into a PFAS-free claim that can actually be delivered to customers and regulators.   Q3. Is total fluorine testing alone enough? Total fluorine testing answers "is there fluorine" but not "which PFAS." For rules targeting specific substances or "intentional use" — such as the EU PFHxA restriction or California AB 1817 — total fluorine results alone are usually insufficient to demonstrate compliance; targeted PFAS testing is needed. In practice, the common approach is to use total fluorine for batch screening and add targeted testing for high-risk batches, balancing cost against compliance certainty.   Q4. How much more do fluorine-free fabrics cost? The cost increase depends on fabric construction, performance requirements, and order volume — there is no single answer. Generally speaking, fluorine-free water repellency requires customization and is rarely available from stock, so the amortized cost for small orders is significantly higher. We recommend that brands state their compliance requirements and target markets clearly at the inquiry stage and have the supplier quote against the actual solution, avoiding rework caused by late changes to standards.   Q5. What should we do with existing fluorinated inventory? This must be judged market by market. France, for example, sets a sell-through deadline for stock produced before 2026, during which it may still be sold; some markets allow no transition for products placed on the market after the ban takes effect. Brands should promptly inventory the fluorine status and production dates of their stock, and build sell-through or diversion plans around each market's effective dates, so that inventory does not end up stranded.   Q6. Do accessories and packaging need to be controlled too? Yes. Zippers, webbing, sewing thread, labels, and packaging materials may carry fluorinated finishes or contain fluorine themselves, and they count toward total fluorine in finished-product testing. Controlling only the main fabric while ignoring accessories is one of the most common sources of total-fluorine failures. Incoming-material segregation should include accessories and packaging, with fixed sources and formulations, ensuring the compliance of the whole product rather than a single fabric.   7. Conclusion As the sections above show, PFAS regulation is not an isolated move by any single market but a dense network taking shape across the EU, France, Denmark, and multiple US states, with timelines highly concentrated around 2026. For bag brands, early action pays off on three levels: •Controllable compliance costs: selecting materials and locking in suppliers and standards early lets the cost increase of fluorine-free customization be amortized over a longer stocking cycle, rather than forcing the brand to accept rush-order premiums just before a ban takes effect. •Supply-chain leverage: a backpack factory that can stably supply compliant fluorine-free fabrics will inevitably prioritize long-term customers with clear standards when orders flood in; brands entering late will struggle to secure capacity. •Market trust: as end consumers and channel partners begin to care about PFAS, a brand that can produce batch-specific, lab-verifiable test reports and compliance declarations has built a competitive barrier in itself. As a professional bag manufacturer with over 30 years of production experience, SYNBERRY BAG keeps pace with evolving market compliance requirements in practice, building deployable experience in material selection, process validation, and batch control — and turning that experience into reusable compliance workflows that help brands convert regulatory requirements into stable, deliverable product capability.   Author        
  • What Is a Vacuum Compression Backpack?
    What Is a Vacuum Compression Backpack? Nov 13, 2026
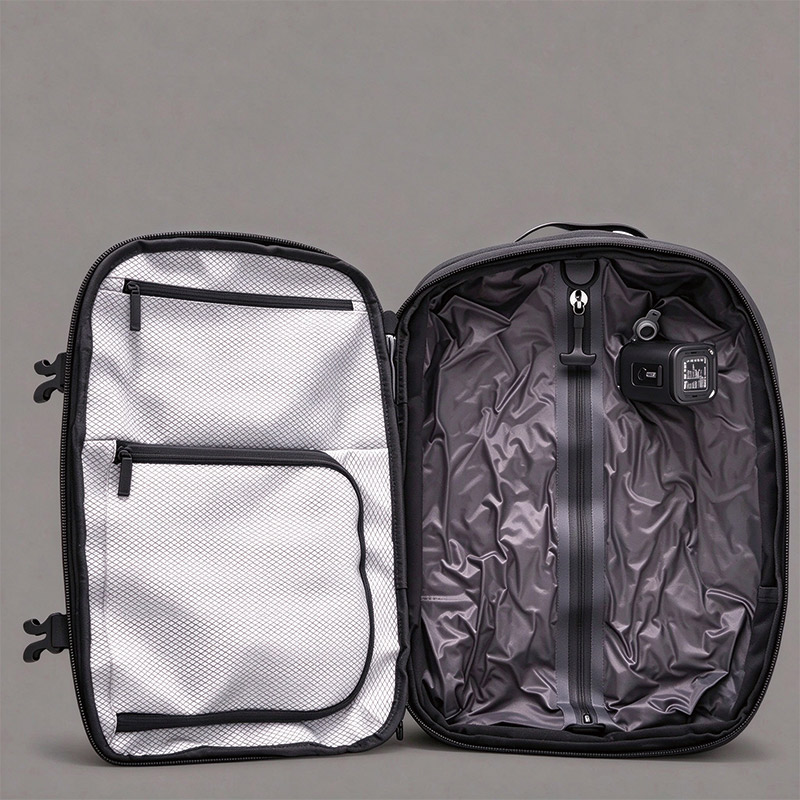
      A vacuum compression backpack is a functional backpack equipped with an airtight, compressible compartment and a one-way air-release valve system. Its core mechanism involves placing clothing or other soft items inside a sealed compartment, then removing the air with a manual pump, electric pump, or external vacuum device. This increases the effective packing capacity for soft items such as clothing without increasing the backpack’s external dimensions. In another word, its primary benefit is to pack more clothing and other soft belongings inside while maintaining the backpack’s overall size.  It is important to understand that vacuum compression reduces volume only, not weight. This article explores the construction and operating principles, compression performance, material selection and manufacturing processes, typical applications, and OEM/ODM customization options for vacuum compression backpacks. It also addresses sourcing considerations such as prototype development, material compliance, and customization coordination, helping brands and procurement teams assess project feasibility at the planning stage. Contents Ⅰ. Core Construction and Operating Principles Ⅱ. Material Selection and Manufacturing Processes Ⅲ. Typical Applications and OEM/ODM Customization Ⅳ. Frequently Asked Questions Ⅴ. Conclusion   Ⅰ. Core Construction and Operating Principles A vacuum compression backpack is more than a conventional backpack combined with a vacuum storage bag. It requires the integrated design of the pack body, airtight compartment, air-release valve, and carrying system. 1. Airtight Compartment The airtight compartment is the key component for creating and maintaining negative pressure. It is generally made from TPU-laminated film. TPU offers good flex-fatigue resistance and flexibility and can be heat-welded, making it suitable for repeated folding and sealing.   Key structural considerations:  •  The backpack’s outer fabric and airtight compartment are separate components. The outer layer provides carrying support, appearance, and abrasion protection, while the inner layer provides the airtight seal and compression function. •  The most common design permanently integrates the airtight compartment into the pack body. Alternatively, buckles, hook-and-loop fasteners, or similar components can be used to create a removable compartment as an optional customization feature. •  The compression area should be designated exclusively for soft clothing and kept separate from the laptop compartment, accessory pockets, and storage areas for rigid equipment. This prevents compression pressure from being transferred to electronic devices or hard items. 2. One-Way Air-Release Valve A one-way air-release valve consists of a valve base, an elastic sealing diaphragm, and a dust cap. During air extraction, the diaphragm opens to let air escape. Once pumping stops, the diaphragm closes to prevent air from flowing back into the compartment. The key performance criterion is the valve’s ability to maintain negative pressure after repeated air-extraction cycles and a period of rest—not simply how quickly it releases air in a single cycle. The valve should be positioned away from areas exposed to pressure from the wearer’s back and from areas where water may collect, while remaining easy to access during pumping. 3. Pump Types and Power Options Three pump configurations are commonly used in the market: a built-in pump integrated into the backpack, a separate detachable pump, and a manual pump. Each serves a different product positioning and should be evaluated together with the airtight compartment, valve, and carrying structure during the prototyping stage. Pump configuration comparison: Configuration Positioning Advantages Limitations Built-in integrated pump Mid- to high-end models Integrated into the backpack; no separate accessory to carry or lose; easy to operate Adds weight; battery performance may decline at low temperatures; complex integration and more difficult repairs Separate detachable pump A balance of speed and flexibility; a common market option Not constrained by the backpack’s internal space, allowing higher airflow options; carried only when needed, so it does not permanently add weight to the pack Requires storage for an extra accessory; fit between the valve port and pump head affects extraction efficiency Manual pump Low-cost, lightweight, and emergency option No electricity required; lightweight; low maintenance cost Longer operating time; more residual air; pumping effort may decrease during continuous use Important details: •  Built-in integrated pump: The pump is installed on the valve base within the backpack, so the complete pack has no detachable pump accessory. There are two power configurations: a built-in lithium-battery version, which charges via USB-C and can operate independently or while connected to an external power source; and a battery-free version, which must remain connected through USB-C to an external power source such as a power bank, charger, or computer. Manufacturers should consider overall weight, low-temperature battery performance, maximum operating time, and export shipping documentation for electronic components. •  Separate detachable pump: The pump is a removable accessory, while the backpack itself retains only the one-way valve. It is available in both built-in lithium-battery and battery-free USB-powered versions (requiring an external power source). Because it is not constrained by the backpack’s internal space, a separate pump generally offers higher airflow than an integrated miniature pump at a comparable cost. Users can also choose whether to carry it, so the backpack does not permanently bear the additional weight. However, the fit between the valve port and pump connector, as well as hose durability, directly affects air-extraction efficiency. •  Manual pump: Compressing a medium-sized vacuum bag takes approximately 90–150 seconds, with a residual air ratio of around 30%–35%. An electric pump can reduce the residual air ratio to approximately 12%–15% and shorten the process to 45–70 seconds. A manual pump is better suited as a low-cost included accessory or for lightweight, battery-free models; it is not recommended as the primary selling point of a mid- to high-end product. Pump selection recommendations: For convenient mid- to high-end models, prioritize evaluating a built-in integrated pump. For faster operation or to avoid permanently increasing the backpack’s weight, consider a separate detachable pump. For small initial orders, tight cost targets, complex structures, or lightweight models, a manual or detachable pump may be more appropriate; there is no need to force the integration of an electric pump. 4. Factors Affecting Compression Performance and Practical Limitations Compression performance depends on the fiber structure of the contents. Different items trap different amounts of air, so their compression ratios can vary significantly. The following figures are for reference: Contents Air Retention Reference Volume Reduction Down jackets and padded coats Very high Approx. 65%–80% Knitwear, sweatshirts, and fleece High Approx. 50%–60% Cotton T-shirts and underwear Medium Approx. 35%–45% Denim, khaki trousers, and canvas items Low Approx. 20%–30%   Ⅱ. Material Selection and Manufacturing Processes The most common quality issues with vacuum compression backpacks are air leakage, cracked weld seams, and declining valve sealing performance. Material selection and heat-sealing/welding processes are therefore critical areas of production control.   1. Materials for the Airtight Compartment The airtight compartment is typically made from a TPU film laminated to a fabric layer. Film thickness must balance airtightness, resistance to negative pressure, and flexibility: •  Film that is too thin: Airtightness becomes less stable after repeated folding. •  Film that is too thick: Flexibility decreases, making stress-related damage more likely at fold lines. The TPU-to-fabric lamination process directly affects long-term service life. Different constructions vary in peel strength, aging resistance, and flex resistance. During cutting, heat sealing, and folding, manufacturers must control surface cleanliness and material tension to prevent contamination, wrinkles, or localized stress concentrations from compromising the weld-seam seal.   2. Outer Shell and Structural Fabrics Common outer-shell materials include high-density nylon, Oxford fabric, and polyester, which can be treated with a water-repellent finish. Fabric weight, density, abrasion resistance, and tear strength should be selected according to the product’s positioning. For models requiring water resistance, the outer fabric and seam-treatment specifications should be determined based on the target market and intended use.   3. TPU Welding and Sealing Processes High-frequency welding and heat-press sealing are the most common methods for joining airtight compartments. Sealing performance is affected by fabric specifications, weld-seam condition, and cleanliness during sealing. Airtightness spot checks are typically conducted during mass production to ensure consistent finished-product quality. An airtight zipper opening offers greater convenience, but it costs more and may provide less stable sealing over repeated long-term opening and closing than a heat-sealed opening. The choice should balance ease of use with sealing reliability.   4. Valve and Pump Assembly Compatibility The main methods for joining the valve to the TPU compartment are thermal welding, flat-plate heat sealing, and compression fitting with a sealing gasket. Key assembly controls include ensuring that the joining surfaces are flat and that the sealing surfaces are free from damage. When an electric pump is selected, the design must also account for pump mounting, airflow-channel alignment, battery-compartment layout, and dust- and water-resistant construction. The integration of electronic components with the backpack structure should be repeatedly validated during prototyping. For backpack OEM/ODM projects, the factory selects the valve model, air-extraction configuration, and accessory suppliers according to the product positioning, then confirms the complete structure during the pre-production sample stage.   5. Carrying Structure and Load Stability Once compressed, clothing forms a compact mass inside the compartment. Positioning it close to the back panel can reduce movement while walking. This places corresponding requirements on the carrying system: the shoulder straps and back-panel support structure must accommodate the compressed load so that the center of gravity sits closer to the wearer’s body. During pattern development, the curvature of the back panel, shoulder-strap thickness, and sternum-strap position can be adjusted according to the target capacity and compartment layout. For models designed primarily for commuting and business travel, carrying stability is just as important as the compression function, and both should be evaluated when the pattern is finalized.   Ⅲ. Typical Applications and OEM/ODM Customization   1. Typical Applications •  Travel and air travel: Airlines in Europe and North America continue to enforce carry-on size limits, and bags that fail gate-size checks may incur additional charges. The key advantage of a vacuum compression backpack is that it can remain within the target airline’s carry-on size limits while increasing the amount of soft clothing it can hold without changing its external dimensions. •  Outdoor activities and short trips: Suitable for short camping trips and hikes, the backpack can compress bulky winter gear to free up main-compartment space. The compression structure can be integrated into outdoor backpacks and travel bags. •  Business travel and commuting: A business backpack can use a removable airtight compartment to support both everyday commuting and short business trips. The laptop compartment and compression compartment should be structurally separated to ensure that compression pressure is not transferred directly to the electronics compartment. •  Sports and fitness: The design can store soft items such as workout clothes and towels and can be incorporated into gym bags and sports backpacks. •  Emergency storage and organization: Suitable for storing seasonal clothing and backup soft gear, this concept can support product lines designed for both travel organization and home storage.   2. Differentiation from Conventional Storage Solutions Comparison Factor Vacuum Compression Backpack Compression Straps / External Cinching Conventional Storage Bag Operating principle A one-way valve removes air from the compartment to create and maintain negative pressure External force compresses the contents and pushes air out from between fibers, but cannot maintain negative pressure Separates and organizes items Volume reduction of soft clothing Relatively high; depends on the fabric and contents Usually only a few to just over ten percent; contents visibly rebound after resting Little to no volume reduction Pack shape More likely to retain a smooth, even profile Can develop localized bulges and become misshapen Does not change the pack’s external shape Protection of contents Airtight compartment helps block moisture and splashes Contents remain directly exposed to ambient moisture Contents remain directly exposed to ambient moisture Typical applications Travel involving a high proportion of soft clothing Heavy-load carrying and external compression/securement Item organization and everyday storage The key differentiator is the ability to maintain negative pressure. External straps rely on mechanical force to compress the contents and expel air trapped between fibers; once the force is released, the contents tend to rebound. By contrast, a vacuum valve can maintain negative pressure after air extraction, resulting in more consistent volume reduction.   3. OEM/ODM Customization Options •  OEM, based on customer-provided designs and samples: The brand supplies the Tech Pack, structural drawings, material specifications, and logo artwork. The backpack factory develops samples and proceeds to mass production according to the requirements. This approach is suitable for projects with an established structural design. •  ODM, using and modifying existing models: The customer selects an existing backpack pattern and airtight-compartment structure from the factory, then adjusts the fabric, color scheme, logo application, selected functions, and packaging. This option helps shorten development lead times and accelerate product launches. •  Light customization for market testing: Based on an existing structure, non-structural components such as the logo, colors, webbing, zipper pulls, and packaging can be changed. This is suitable for emerging brands and cross-border e-commerce sellers testing market demand.   Ⅳ. Frequently Asked Questions   Q1. How is the sealing performance of an airtight compartment evaluated after repeated use? A: Airtight reliability is determined jointly by the film substrate, weld-seam edges, and valve connections. Common validation methods include weld-sample inspection, negative-pressure retention tests on the compartment, and repeat airtightness tests after multiple air-extraction and release cycles followed by a resting period. Test frequency and acceptance criteria for different product grades can be agreed upon when the order is confirmed.   Q2. What material-compliance requirements commonly apply to vacuum compression backpacks exported to Europe and North America? A: European and North American markets have specific compliance requirements for bag fabrics, coatings, hardware, accessories, and chemicals. A vacuum compression backpack may contain TPU film, outer fabric, water-repellent treatments, webbing, sewing thread, and hardware. These materials should undergo the relevant testing and documentation procedures for the target market. Common compliance frameworks and programs include REACH, California Proposition 65 (CA Prop 65), and OEKO-TEX. The exact test list depends on the order requirements and applicable local regulations.   Q3. Can the compression compartment be designed to be removable? What are the structural and cost implications? A: Yes. A removable airtight compartment can be secured inside the backpack using zipper tracks, buckles, or hook-and-loop fasteners. This allows the user to switch between business commuting and short-trip configurations and makes it easier to replace the compartment if it is damaged. However, it adds the cost of zippers or buckles. The interfaces also require sealing and load-bearing validation, and the compression-compartment boundaries and backpack pattern must be adjusted accordingly.   Q4. What should manufacturers consider when integrating an electric pump? A: An integrated electric-pump system includes the pump, battery, wiring, and airflow-channel components. Key considerations include secure pump mounting, heat dissipation, dust and water resistance, and electronic-component reliability. The relevant lithium-battery shipping documentation must also be prepared for export. For smaller orders or complex structures, a manual pump or separate detachable pump may be recommended as an alternative.   Q5. Does the compression compartment affect the safety of laptops or other electronic devices? A: With an independent-compartment design, the airtight compression compartment is separated from the laptop compartment, so negative pressure is not transferred to the electronics compartment. By planning the compartment boundaries and lining structure during pattern development, manufacturers can achieve both compression storage and device protection.   Ⅴ. Conclusion A vacuum compression backpack is a functional bag that places high demands on airtight construction, material compatibility, and heat-sealing processes. Product consistency depends on the coordinated design of the TPU compartment, one-way valve, pump configuration, and backpack structure. As a bag OEM/ODM manufacturer, we can provide structural assessments, material selection, logo-application development, sample development, and mass-production services. If you are planning a vacuum compression backpack project, please share your target market, backpack capacity, compression-compartment ratio, preferred pump configuration, and estimated initial order quantity. We will provide professional recommendations to help you select the right solution.   Author        
  • How to Customize an AirTag Backpack for Your Brand?
    How to Customize an AirTag Backpack for Your Brand? Nov 12, 2026
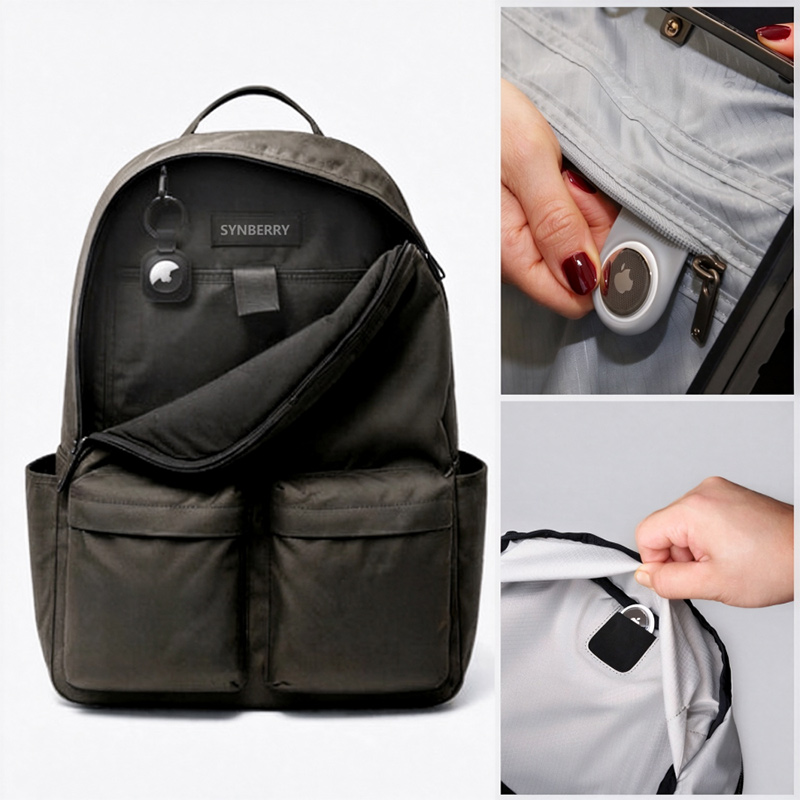
      Customizing an AirTag backpack usually follows one of two cooperation models — the "bare bag" model and the "bundle" model. Bare bag model: The factory is only responsible for the backpack itself and the built-in AirTag holder structure. Consumers purchase the AirTag separately, and the packaging is marked "AirTag not included." Bundle model: The brand either sources genuine Apple AirTags or third-party authorized AirTags on its own, or commissions the factory to procure them, and the AirTags are packed together with the backpacks before delivery.   Whichever model you choose, the core engineering work is the same: adding a purpose-designed AirTag holder structure to the standard backpack development process. First, define the product positioning and usage scenarios. Next, work with the backpack OEM/ODM factory to complete the holder's structural design, material selection, and prototype testing. Finally, layer in brand elements such as your logo, color schemes, and packaging, then move into mass production and delivery following the standard inspection process. The difference between the two models lies not in the product itself, but in the commercial arrangements: who procures the AirTags, who bears the shipping compliance responsibility for products containing lithium batteries, and who controls the regulatory certifications for the target markets. What looks like simply "adding a small pocket" is, in fact, systematic engineering that spans five dimensions: structural design, signal compatibility, anti-loss safety, supply chain quality control, and certification compliance. Table of Contents: I. What Is an AirTag Tracker? II. Product Positioning: Does Your Brand Need This Category?  III. Scenario Positioning: How Should It Be Done?  IV. Practical Solutions in the AirTag Backpack OEM Process V. How We Implement Quality Control in Specific Orders VI. Certifications and Compliance for AirTag Backpacks VII. Frequently Asked Questions (FAQ) VIII. Conclusion   I. What Is an AirTag Tracker? Before customizing, you first need to understand what an AirTag is and confirm whether this category makes sense for your brand — this determines the scale of every investment that follows. The AirTag is a Bluetooth tracking device launched by Apple. Shaped like a small round disc, the official model measures about 31.5 mm in diameter and about 8 mm thick, weighing only 11 grams. It contains a built-in speaker, an accelerometer, and a Bluetooth chip, and it locates items through Apple's "Find My" network. Users place an AirTag inside a backpack or suitcase, or attach it to their keys, and can then view the item's location on their phone. When an item is lost, they can enable Lost Mode, which lets nearby passing Apple devices help relay location information back to them. For backpack brands, the key to understanding how AirTag works lies in its relationship with the bag itself: the AirTag does not rely on GPS for positioning. Instead, it reports its location through Bluetooth interaction with surrounding Apple devices, which means its signal quality depends heavily on the materials and shielding conditions around its mounting position. In addition, the AirTag is powered by a coin cell battery with a battery life of about one year, and users need to replace the battery periodically. This means the holder must balance two requirements: "easy to insert and remove" and "not easy to fall out." Its diameter and thickness also define the basic dimensional constraints of the holder design — if the holder is too shallow, the AirTag can easily slip out; if it is too tight, users will struggle considerably when replacing the battery. II. Product Positioning: Does Your Brand Need This Category? AirTag backpacks solve a real and high-frequency pain point: bags getting lost, taken by mistake, or stolen. Apple's "Find My" network relies on hundreds of millions of Apple devices worldwide relaying location data, giving a tiny tracker near-global coverage for recovering lost items. For consumers, building an AirTag into a backpack or attaching one to it is like taking out a "recoverable" insurance policy on their belongings. For brands, it delivers fourfold value: Differentiated selling point: In a market where backpacks are heavily homogenized, "built-in anti-loss tracking" is a genuine functional selling point. Premium pricing potential: Backpacks with an integrated AirTag holder can typically command a noticeably higher retail price than a standard model with the same specifications. Scenario expansion: Business commuting, business travel, parent-and-baby, students, pet travel... almost every demographic segment has a "fear of losing things" pain point. Market demand: Judging by market signals, this category is still in a window of "high awareness, insufficient supply": cumulative AirTag sales have long reached the tens-of-millions scale, while search interest for keywords such as "AirTag backpack" and "AirTag luggage" on e-commerce platforms continues to climb. If your brand already has a mature commuter or travel bag line, you only need to add a holder to an existing pattern to enter this selling point at a relatively low development cost.   III. Scenario Positioning: How Should It Be Done? Once you have a reason to do it, the second step is to understand the usage requirements of each scenario, because scenario positioning directly determines where the holder should be placed and how it should be built. Different scenarios have entirely different requirements for the AirTag holder: Business commuter bags: Users care about concealment and a premium feel. The holder is best hidden in a lining compartment or behind the brand's woven label, leaving the exterior completely seamless. Travel backpacks / carry-on bags: Loss scenarios mostly occur at airports and train stations. Users need to quickly check the AirTag's battery level or replace the battery, so the holder must balance concealment with "easy for the owner to access, hard for others to access." Student bags / children's bags: Beyond anti-loss, you must also prevent children from accidentally swallowing the battery. The holder must have a safety locking structure (such as a screw-on clasp that requires a tool to open). Outdoor backpacks: Harsh environments demand a holder that is waterproof, shock-resistant, and able to withstand repeated friction.   IV. Practical Solutions in the AirTag Backpack OEM Process   4.1 Mainstream Holder Solutions: 4.1.1 Hidden Built-In Structure A hidden built-in structure tucks the AirTag holder entirely inside the backpack, with no visible opening or marking on the exterior. It suits commuting and business travel scenarios that pursue a clean appearance, where the anti-loss need is mainly "recovering your own item." Hidden inner pocket: A snug-fitting elastic slip pocket sewn onto the lining. The structure is the simplest and the cost is the lowest, making it suitable for commuter bags and business bags. Built-in dedicated holder tray: A custom-molded plastic tray that matches the AirTag's outer diameter, locking it in place with a press-fit. It is fixed inside a zippered pocket in the bag; when needed, the user opens the zipper to take it out, and when not needed, the zipper stays closed — offering excellent concealment.   Built-in clip-on structure: An independent hook or clip is installed inside the backpack. The AirTag, paired with a compatible silicone sleeve and keychain, hangs onto the holder. It can also be designed to sit inside a zippered pocket for added concealment.   4.1.2 Convenient External-Mount Structure Designed for quick personal item-finding, the core requirement of an external-mount structure is "always within reach" — users can see or feel where the AirTag is without opening the main compartment and digging around. It suits high-frequency outings such as daily commuting, walking the kids, or walking the dog. Common approaches include the following: External locking clip attachment point: A webbing attachment point with a metal buckle ring is added at the base of the shoulder strap or along the outer edge of a side pocket. The user secures the AirTag to the outside of the bag with a silicone sleeve and keychain. The signal is completely unobstructed and battery replacement is the most convenient, making it suitable for outdoor backpacks and lightweight commuter models.   Webbing/woven-label integrated position: The holder is woven directly into the backpack's webbing or side label.   Hidden zippered compartment: An independent zippered compartment set inside the trolley-sleeve strap, back panel, or side pocket. It offers the strongest versatility and convenient battery replacement, making it a common choice for travel bags. For premium business travel backpacks, we recommend prioritizing the hidden built-in solution: the hidden pocket is fixed to the inside of the back panel or within an internal zippered pocket, with no visible opening on the exterior. This balances concealment with a premium feel while retaining an open-and-close access channel, so users can replace the battery without rummaging through the main compartment. If your brand wants to emphasize the "quick confirmation" experience during travel, a woven-label marker can be added to the lining compartment, allowing users to identify the AirTag's location by touch without opening the bag. One point worth noting: once the holder solution is finalized, all subsequent structural prototyping, mold development, and production-line fixtures will be built around it. We therefore recommend confirming the backpack pattern, lining structure, and holder together at the solution review stage, to avoid rework later caused by changes in lining thickness or stitching direction. 4.2 Materials and Craftsmanship: Material selection must satisfy two goals at once: the functionality of the AirTag holder, and the quality consistency of the entire bag. Bag body fabric: Nylon (such as 1680D ballistic nylon), polyester, canvas, and recycled eco-friendly fabrics all work, and none of them affect the AirTag's signal. Holder materials: Silicone sleeves are recommended for holder trays — soft, highly resilient, and gentle on the AirTag's surface coating. For inner pockets, four-way stretch Lycra fabric or microfiber is recommended, as it grips the AirTag firmly while still allowing easy insertion and removal. Hardware and accessories: Zippers and buckles should be kept away from the area around the holder as much as possible, to reduce metal shielding. Craftsmanship essentials: The stitching at the holder is a high-frequency stress concentration point and must be reinforced with bar tacks.     4.3 Four Pitfall-Avoidance Tips: About the signal: The AirTag works via Bluetooth and UWB (ultra-wideband), so the holder must not be fully enclosed by metal materials (aluminum frames and metal linings will create shielding). PU, nylon, polyester, and genuine leather do not affect the signal, but if your design includes metal components, actual testing is a must. About removal and installation: Battery life is about one year, and users must be able to replace the battery themselves. The holder must be "openable by hand or with a tool, yet won't come loose under vigorous shaking." About anti-loss: Ironically, the anti-loss device itself can also get lost. The holder must not allow the AirTag to slip out easily during inversion, shaking, and compression tests. Privacy and safety: Children's products must account for the risk of accidental swallowing. You should also pay attention to Apple's design guidelines for AirTag accessories, avoiding structures that block the speaker and thereby weaken the "plays a sound when being located" function.   V. How We Implement Quality Control in Specific Orders The standard bag production process begins with confirming the design and craftsmanship, followed by prototype confirmation; mass production only begins after the sample is approved, and the goal at this stage is "consistency with the approved sample." As a professional backpack factory, our quality control process includes: Pre-production sample approval: A sealed sample is finalized before bulk cutting begins, and all details are based on the sealed sample. Incoming material inspection: Incoming material inspection is the first gate in the quality control chain. In-process patrol inspection: Every production node has a corresponding checklist; when a problem is found, the line is stopped and corrected on the spot, rather than waiting for finished products to come out and then repairing them. Pre-shipment inspection: Conducted according to the internationally accepted AQL sampling standard. SYNBERRY BAG typically performs sampling inspections at the high standard of AQL 4.0/1.5.     VI. Certifications and Compliance Quality control solves the consistency of the product itself; certifications and compliance solve the legality of the product entering the market. AirTag backpacks straddle two domains — "luggage + electronic accessory ecosystem" — which adds an extra layer of compliance considerations compared to ordinary backpacks. We break them down into four aspects:   6.1 Trademarks and Intellectual Property: Unbranded (no-logo) AirTags: "AirTag" is a registered trademark of Apple. Currently, most units on the domestic market are produced by third-party authorized companies, so the product itself must carry Apple's MFi certification to be sold legitimately. Customized brand logos: Unbranded products already carry MFi certification, but if you customize a brand logo on the product body, a new authorization certification is required. The certification fee is about USD 3,000, and the certification cycle takes 3–5 months. We therefore recommend that brands use neutral (unbranded) products when developing a new product line, to reduce initial development costs.   6.2 Product Safety and Chemical Compliance 6.2.1 On the Backpack Side: European Union: Fabrics and accessories must comply with the REACH regulation (SVHC candidate list of substances of very high concern, azo dyes, nickel release, etc.), including the latest PFAS control requirements — this is also why more and more European and American orders require PFAS-free fabrics. United States: Pay attention to the warning requirements of California's Proposition 65. Children's backpacks are classified as children's products and must comply with CPSIA, with a CPC (Children's Product Certificate) provided. Holder trays must pass small-parts testing to prevent accidental swallowing. Environmental claims: When your product page carries claims such as "eco-friendly" or "PFAS-free," they must be backed by test reports. Regulators in Europe and the U.S. are tightening oversight of greenwashing (the U.S. FTC Green Guides and the EU Green Claims Directive).   6.2.2 On the AirTag Side: European Union: When entering the EU market, the compliance pressure for AirTags comes mainly from the general requirements for electronic products, rather than from the luggage category itself. AirTag holder kits sold in member states must meet the relevant directives under the CE marking framework, among which RoHS is a foundational requirement. United States: In the U.S., the AirTag itself, as an electronic device with wireless transmission capability, is regulated by the FCC. If it is sold as a complete bundle with the bag, you need to confirm that the bundled accessories meet the FCC's relevant requirements for unintentional radiators, and retain compliance markings on the label and in the instruction manual. If the backpack only provides the holder structure without the AirTag itself, the product remains an ordinary piece of luggage, and responsibility for electronics regulations falls on the AirTag supplier's side. Brands need to clearly allocate this portion of responsibility in their supply chain contracts, to avoid unclear accountability when problems arise.   VII. Frequently Asked Questions (FAQ)   Q1: What is the typical minimum order quantity (MOQ) for custom AirTag backpacks? The hidden inner pocket solution involves no mold-making, so its MOQ is usually the same as that of an ordinary custom backpack (commonly starting from 500 units). The holder tray solution requires an injection mold, so factories generally demand a higher MOQ (1,000 units or more) to spread out the mold cost. The specifics depend on the factory and the complexity of the craftsmanship. When requesting quotes, we recommend writing the holder solution into the specification sheet before comparing prices.   Q2: Should the AirTag be included with the bag? Who procures it? Both models are viable. Most brands choose "no AirTag included," noting on the packaging and product page that "AirTag sold separately" — this keeps both costs and legal risks at their lowest. The bundle model brings a higher average order value, but you must solve the legitimate AirTag procurement channel and the shipping compliance issues for products containing lithium batteries on your own.   Q3: Does making an AirTag backpack require Apple's MFi certification or licensing? It depends on the cooperation model. MFi certification targets electronic accessories that use Apple's connectors and protocols (such as Lightning cables); a purely structural storage holder does not fall within its scope. However, if the AirTag is sold together with the bag, MFi certification is required.   Q4: Will the holder block the AirTag's signal? Not as long as it is properly designed. The AirTag works via Bluetooth and UWB, and nylon, polyester, genuine leather, silicone, and PC/ABS plastics cause no shielding. What you truly need to avoid is fully enclosing the AirTag in metal materials.   Q5: Can one holder be compatible with trackers from other brands at the same time? Yes, but the dimensions must be re-verified. The official Apple AirTag (31.9 mm in diameter), Samsung Galaxy SmartTag (about 39 mm square), and Tile Mate differ considerably in size, so a single holder can hardly fit them all. If Android users make up a high share of your target market, you can develop a dual solution of "AirTag holder + universal attachment point," or supply different versions for different markets.   Q6: Are there any special requirements for adding an AirTag holder to children's backpacks? There are two: the holder must have a protective cover or locking structure that prevents accidental swallowing (one that children cannot open with their bare hands); and exports to the U.S. must comply with CPSIA and be accompanied by a CPC certificate. VIII. Conclusion   For a brand looking to enter the smart backpack category, turning an idea into a product line that can be delivered stably is, at its core, a test of supply chain capability. What it tests is not just whether a bag manufacturer is willing to add one more holder, but whether someone can walk the brand through every step — from structural design, material selection, and signal validation to certification and compliance. What SYNBERRY BAG has accumulated across these steps is precisely this kind of hands-on experience that puts details into practice: every design is backed by test evidence, every inspection has traceable records, and every certification document can be delivered along with the order.   If you are evaluating the feasibility of an AirTag backpack product line, feel free to share with us the certification requirements of your target market, your intended bag patterns, and your approximate order volume. We can first provide recommendations on the holder solution, and then quote a practical, deliverable development and production plan based on it.   Author        
  • What Causes the Coating on PU Leather Bags to Peel Off? The Truth About PU Hydrolysis
    What Causes the Coating on PU Leather Bags to Peel Off? The Truth About PU Hydrolysis Nov 07, 2026
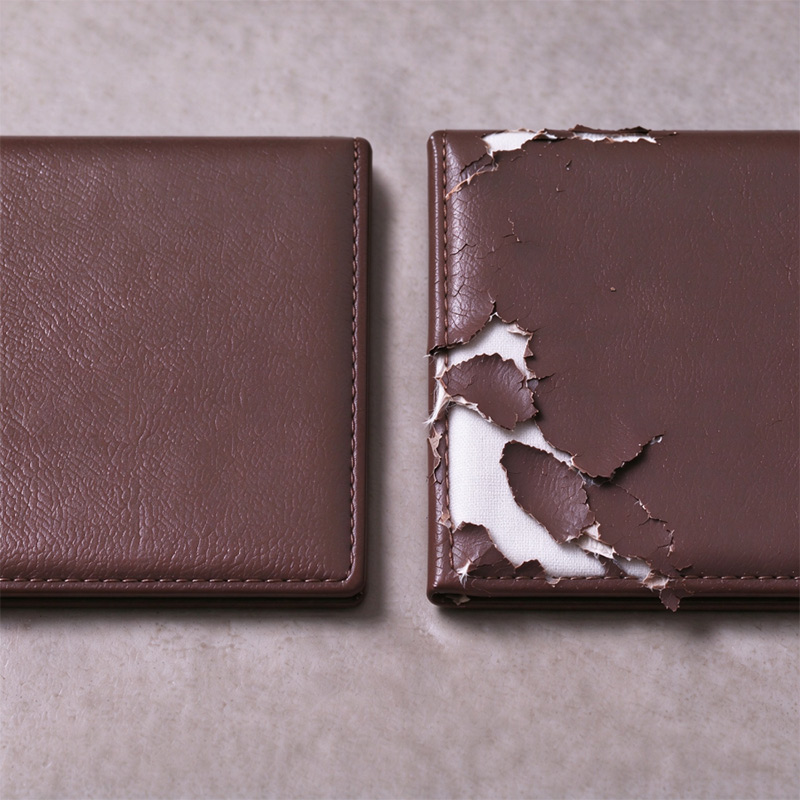
      The coating on PU leather bags can peel off for several reasons. Common causes include physical abrasion and scratching during everyday use, oxidation resulting from prolonged UV exposure, and chemical damage caused by frequent contact with alcohol or aggressive cleaning agents. However, in most after-sales complaints where there is no obvious external damage, the underlying cause is PU hydrolysis. Hydrolysis is an irreversible chemical degradation process. Moisture, including humidity in the air, reacts with the ester bonds in polyester-based polyurethane, causing the polymer chains to break. In simple terms, moisture gradually undermines the coating from within, causing it to lose elasticity and become brittle. Under normal flexing, the weakened coating eventually separates from the backing fabric and flakes off in sheets or fragments. This article examines the chemistry behind PU hydrolysis and explains how selecting the right material system and implementing proper warehousing and logistics practices can help reduce the risk at its source. Contents Ⅰ. Four Major Causes of Coating Peeling on PU Leather Bags Ⅱ. Understanding PU Hydrolysis: Why Does the Coating Deteriorate? Ⅲ. What Factors Accelerate PU Hydrolysis? Ⅳ. How Can B2B Buyers Manage the Risk of Hydrolysis? Ⅴ. Frequently Asked Questions (FAQ) Ⅵ. Conclusion   Ⅰ. Four Major Causes of Coating Peeling on PU Leather Bags Before taking a closer look at hydrolysis, it is important to distinguish among the different causes of coating delamination. Not every case of peeling is caused by hydrolysis. https://www.synberry.com/why-are-brands-choosing-pu-leather-for-cosmetic-bags • Physical Wear and Tear: Prolonged, intensive rubbing and scratching—such as abrasion on the bottom of a backpack or around frequently rubbed corners—gradually wear down the coating until the backing fabric is exposed. Typical signs: damage is concentrated on high-contact corners or edges and is accompanied by visible scuff marks. • UV Oxidation: Long-term exposure to direct sunlight can make the coating surface brittle and cause it to crack. These cracks allow moisture to penetrate, accelerating subsequent aging and peeling. Typical signs: cracking first appears on sun-exposed areas and is often accompanied by fading. • Chemical Attack: Repeated wiping with high-alcohol-content wipes or powerful cleaning agents can dissolve or damage the surface structure of the PU coating. Typical signs: the damaged area closely matches the area exposed to the chemical, with clearly defined edges. • PU Hydrolysis: This is a chemical degradation process that progresses from the inside out. It may cause the coating to become sticky, blister, crack, and eventually detach in large pieces. It is a form of deep-seated aging associated with the chemical characteristics of polyester-based PU synthetic leather. Typical signs: there are no obvious scratches caused by external force; the damage spreads gradually and is often accompanied by a powdery or sticky coating. Ⅱ. Understanding PU Hydrolysis: Why Does the Coating Deteriorate? When consumers or buyers find extensive peeling or a sticky surface on a bag with no obvious scratches, hydrolysis is often the underlying cause.   1. Polymer Chain Scission at the Molecular Level The polymer structure of a PU coating can be thought of as a network of tightly interwoven chains. Conventional polyester-based PU contains numerous ester bonds along these chains. When moisture in the environment, perspiration, or residual water from cleaning penetrates the coating, it can react with these ester bonds. Organic acids and salts in perspiration may act as catalysts, accelerating the reaction and breaking long polymer chains into shorter, weaker fragments. By contrast, the main chains of polyether-based PU contain ether linkages, which are more chemically stable and less susceptible to the same type of hydrolysis. 2. From Microscopic Chain Scission to Macroscopic Delamination Hydrolysis does not occur instantaneously. It typically develops through three stages: • Tackiness or Brittleness: As polymer chains break, the coating loses its original elasticity and flexibility, and subtle changes begin to appear on the surface. • Blistering and Cracking: As the topcoat resin degrades, its cohesive strength decreases. Two types of blistering should be distinguished: internal bubbles caused by degradation of the PU topcoat itself, and bubbles at the interface between the topcoat and backing fabric caused by moisture-induced failure of the laminating adhesive. The latter is not hydrolysis of the PU resin. • Final Delamination: The weakened coating can no longer withstand routine bending and handling. It eventually separates completely from the backing fabric, which may be cotton or polyester, resulting in the peeling commonly seen on PU leather products. 3. An Irreversible Chemical Change Hydrolysis changes the chemical structure of the material and is therefore irreversible. Once the coating becomes visibly sticky or begins to delaminate, surface cleaning, conditioning, or recoating cannot reconnect the polymer chains that have already been broken.   Ⅲ. What Factors Accelerate PU Hydrolysis? The rate of hydrolysis is closely related to the external environment in which the material is stored or used. Understanding these accelerating factors helps brands and cross-border e-commerce sellers prepare for risks throughout the supply chain.   1. The Combined Effects of High Temperature and High Humidity Temperature and humidity are key variables affecting the rate of hydrolysis. In tropical and subtropical monsoon regions, or inside shipping containers during long-distance ocean freight, high temperatures combined with localized condensation can significantly accelerate hydrolysis. Similarly, moisture can gradually penetrate bags stored for extended periods in poorly ventilated, high-humidity warehouses.   2. Non-Breathable Packaging and Storage If finished bags are not thoroughly dried before packing, or are sealed in plastic bags for extended periods, residual moisture may become trapped inside. This can create a localized high-humidity, greenhouse-like environment that accelerates coating deterioration.   3. Chemical Exposure During Everyday Use Human perspiration contains organic acids and salts that can catalyze ester-bond hydrolysis. In addition, everyday products such as sunscreen, insect repellent, and alcohol-based hand sanitizer may reduce the coating's hydrolysis resistance. Ⅳ. How Can B2B Buyers Manage the Risk of Hydrolysis? As an OEM/ODM supplier of bags and leather goods, we recommend that B2B customers select a PU material system based on the climate of the target market and the expected product service life during the sourcing and order-placement stages, rather than focusing narrowly on the label “hydrolysis-resistant.” Important note: Hydrolysis resistance of the topcoat does not guarantee hydrolysis resistance of the entire bag. Even if the top layer is made from polyether-based material, a conventional polyester-based laminating adhesive may still hydrolyze and cause delamination under prolonged hot and humid conditions. The resulting appearance can closely resemble hydrolysis of the topcoat. For orders involving long ocean-transit times or high-humidity markets, the hydrolysis-resistant adhesive system must also be verified.   1. Performance Comparison of Different PU Material Systems Material System Hydrolysis Resistance Suitable Markets and Applications Cost and Processing Considerations Performance Trade-Offs Conventional polyester-based PU Relatively low; prone to hydrolysis-related delamination in hot and humid environments. Fast-moving consumer goods markets with dry climates, moderate temperatures, and relatively short product replacement cycles. Significant cost advantage; established, conventional processing methods. Good abrasion resistance and UV resistance; no hydrolysis stabilizer is included. Modified polyester PU (with hydrolysis stabilizer) Moderate; better than conventional polyester PU but less resistant than polyether PU. Moderate-humidity environments and budget-conscious projects; not suitable for extremely humid, hot, long-ocean-transit conditions. Moderately low cost and good process compatibility. Service-life improvement has limitations. The regulatory compliance of carbodiimide-based stabilizers should be checked in advance. Polyether-based TPU Excellent hydrolysis resistance; dense structure with strong aging resistance and washability. High-humidity climates, frequent washing, and outdoor or professional equipment requiring a very long service life. Higher cost and a relatively narrow processing window; production capacity should be confirmed in advance. Can feel relatively stiff, limiting the hand-feel options for some designs. Note: Polyester-based TPU has hydrolysis resistance close to conventional polyester PU and must not be treated as equivalent to polyether-based TPU.   2. Material Approval and Aging Validation During Sampling To avoid performance differences between the approved sample and the bulk production run, the supplier and customer should confirm and lock in the exact material specifications during the sampling stage. For orders destined for hot and humid regions or involving long ocean-transit times, both parties can assess whether third-party accelerated aging tests are necessary based on the actual requirements. The specific test standards and acceptance criteria should be agreed upon by both parties during order negotiations. 3. Packaging Protection and Warehousing Recommendations • Use of Desiccants: For long-distance ocean shipments or destinations with high humidity, we recommend placing an appropriate amount of desiccant inside the packaging to absorb moisture and potential condensation inside the shipping container. • Breathable Packaging: Avoid heat-sealing finished products in plastic bags before they are completely dry. Use packaging materials with suitable air permeability. • Warehousing: Brands should pay attention to warehouse ventilation and temperature and humidity control when products are received into storage. Avoid keeping products in extremely humid environments for extended periods.   4. Parallel Considerations for Chemical Compliance Improving a material's hydrolysis resistance does not replace chemical compliance requirements. PU bags exported to the EU must comply with REACH requirements, including restrictions on certain azo dyes and phthalates. For exports to the United States, documents and requirements such as CPSIA should be confirmed according to the customer's requirements. During sampling and quotation, we work with customers to confirm the required tests and lead times, helping ensure that products meet both physical durability expectations and the chemical safety standards of the destination market.     Ⅴ. Frequently Asked Questions (FAQ)   Q1. If the topcoat is made from hydrolysis-resistant PU, does that mean we no longer need to worry about peeling? A: No. A hydrolysis-resistant topcoat does not guarantee that the entire bag will be free from coating delamination. PU leather is a multilayer composite structure, and the laminating adhesive and backing fabric are also critical components. Even when the topcoat uses a hydrolysis-resistant resin such as polyether PU, a conventional polyester-based laminating adhesive may hydrolyze first under prolonged hot and humid conditions or during humid ocean transit, resulting in delamination that looks very similar to topcoat hydrolysis.  When evaluating an order, both the topcoat resin and the laminating adhesive system should be included in the hydrolysis-resistance assessment. The topcoat material should never be evaluated in isolation.   Q2. How can we distinguish hydrolysis from a manufacturing or bonding defect? A: The two issues may look similar, but they have different causes. Poor lamination or bonding workmanship usually becomes apparent early in the product's use, and the interface tends to separate cleanly and uniformly. Delamination caused by hydrolysis is often accompanied by tackiness or powdering of the coating itself and generally develops gradually.   Q3. If the coating has started to feel slightly sticky, can it be repaired by applying a spray-on conditioner? A: No. Stickiness indicates that hydrolytic chain scission has already occurred in the PU polymer. This is a chemical change in the material itself. A surface-care product may provide temporary coverage or lubrication, but it cannot reverse the chemical degradation or restore the bond between the coating and the backing fabric.   Q4. If ocean transit takes a long time, what protective measures can we take before shipment? A: In addition to placing desiccants inside the packaging, we recommend thoroughly drying the bags before shipment to prevent residual moisture from being sealed inside. If conditions allow, conduct random inspections of the shipment batch to check the surface hand feel and bonding condition of the coating. Customers at the destination should also be reminded to store the products in well-ventilated conditions after receipt and avoid prolonged stacking in non-breathable environments.   Ⅵ. Conclusion Coating peeling on PU leather bags can be caused by multiple factors. In hot and humid environments, PU hydrolysis is a particularly important chemical aging mechanism to consider. As a manufacturer of leather products, we can recommend suitable PU materials based on the climate of your target market and assess the laminating adhesive system at the same time. We help lock in material specifications during sampling and provide integrated technical support for moisture protection throughout packaging, warehousing, and ocean freight for OEM bag orders. Whether you are launching a new product or reviewing the durability of an existing material specification, share your product application, target market, and order expectations with us. We can help you develop a material selection plan that meets your needs.   Author        
  • What Certifications Are Required to Sell Customized Backpacks on Amazon US? (2026 Latest Compliance Checklist)
    What Certifications Are Required to Sell Customized Backpacks on Amazon US? (2026 Latest Compliance Checklist) Nov 03, 2026
      There is no single, unified Amazon US certification standard for ordinary adult backpacks. Compliance requirements generally need to be assessed across multiple dimensions, including the product's intended age group, raw material composition, additional features, compliance regulations applicable in the primary US states where the product will be sold, and Amazon's individualized review requirements for specific ASINs. The corresponding compliance documents and testing obligations should then be determined accordingly. For ordinary customized adult backpacks without electronic functions or special safety features, there is generally no specific mandatory "backpack certification." These basic products are typically subject to standard consumer product safety compliance requirements. If a product is primarily designed or marketed for children aged 12 or younger, it will generally need to comply with applicable children's product-specific regulatory requirements, including completing the required testing, issuing a Children's Product Certificate (CPC), and placing compliant permanent tracking labels on both the product and its packaging. Table of Contents First, Determine the Product Classification: Is Your Backpack a "Children's Product"? What Standards Must Children's Backpacks Meet? What Standards Must Ordinary Adult Backpacks Meet? New Requirements After July 2026: CPSC eFiling Electronic Filing Compliance Pathways by Product Type How We Help Brands Manage Compliance Risks FAQ Conclusion   1. First, Determine the Product Classification: Is Your Backpack a "Children's Product"? The US Consumer Product Safety Commission (CPSC) has a clear, legally binding definition of a "children's product": a consumer product specifically designed for children aged 12 or younger, or primarily intended for use by children aged 12 or younger. This classification is not determined by the seller's subjective marketing claims. Children's backpacks and school backpacks unquestionably fall within this regulatory scope. Amazon's review requirements for children's backpacks are very specific. Products must comply with CPSIA Section 101 (lead content), Washington State Children's Safe Products Act (CSPA), RCW 70.240.020 (phthalates and cadmium), 16 CFR 1500.50, and applicable small parts warning requirements.   In practice, many brands specializing in customized backpacks actually launch adult-oriented or general-purpose products. However, due to the use of imprecise keywords in their Amazon listings, product photography with a childlike aesthetic, or even misclassification by Amazon's automated categorization algorithms, their products may be classified by the system as "children's backpacks" or "children's school supplies." This can subsequently trigger compliance corrective action notices from Amazon. When appealing such decisions, sellers need to provide sufficient evidence demonstrating that their products are not designed or intended for use by children. Therefore, the first practical recommendation is as follows: If your branded backpacks are genuinely not designed for children, ensure that the listing copy, main and secondary product images, and lifestyle scenarios displayed on the A+ Content page clearly communicate the product's adult-oriented positioning. Explicitly showcase adult use cases such as commuting, travel, and outdoor activities. Even so, Amazon may still request compliance documentation, particularly when the product features cartoon patterns, highly saturated and bright colors, or appears in search results associated with terms related to "school supplies."   2. What Standards Must Children's Backpacks Meet? Once a product is classified as a children's product, a CPC (Children's Product Certificate) becomes an unavoidable mandatory compliance requirement. It is important to clarify that a CPC is not a "qualification certificate" issued by a government agency. Rather, it is a compliance declaration independently prepared by the manufacturer or importer, who assumes full legal responsibility for its accuracy and validity. However, the issuance of a CPC must be supported by a passing test report issued by a third-party laboratory recognized by the CPSC. A CPC without a valid supporting test report does not have legal compliance validity. 2.1 Standard Testing for Children's Backpacks Typically Covers the Following Key Items:  SIA Total Lead and Phthalates: The total lead content in all accessible components must not exceed 100 ppm, while lead content in paint and similar surface coatings must not exceed 90 ppm. Phthalate testing primarily covers the eight restricted phthalates, each subject to a limit of 0.1% (1,000 ppm). However, there is one important point that needs to be clarified first: The original regulatory language specifically applies to "children's toys" and "child care articles." In Amazon's CPC review practices, children's backpacks are generally assessed within this regulatory framework. Therefore, preparing for testing against all eight restricted phthalates is a relatively prudent approach when submitting products for testing, as it can help reduce the cost of repeated supplementary testing. Small Parts Warnings: If a backpack contains small detachable components, such as movable decorative charms, detachable shoulder strap buckles, or decorative rivets, it must comply with the relevant requirements of 16 CFR 1500.50. Clear small parts warning statements may also need to be displayed on the packaging or directly on the product. Flammability Performance: Textile materials used in backpacks, including outer fabrics and linings, generally need to comply with the flammability performance requirements under 16 CFR Part 1610 to avoid safety risks associated with easily ignitable fabrics.   2.2 The CPC Certificate Itself Must Include Seven Categories of Legally Required Information: Clear and traceable product identification; A complete list of the applicable regulations and standards; Information identifying the US-based importer or domestic manufacturer; The specific production date and manufacturing location of the product; The date and location where third-party testing was completed; Complete information about the CPSC-accepted third-party testing laboratory; Clear signature and certification details identifying the party responsible for issuing the certificate.   3. What Standards Must Ordinary Adult Backpacks Meet? A GCC (General Certificate of Conformity) is a written declaration of compliance required under the US Consumer Product Safety Act (CPSA). It primarily applies to non-children's products (i.e., "general use products") that are subject to specific CPSC safety rules, standards, or bans. For ordinary adult backpacks that do not fall under any applicable mandatory regulations, a GCC is generally not automatically required. The issuance process for a GCC is similar to that of a CPC. It is also a compliance declaration independently issued by the US importer or manufacturer based on a reasonable testing program. The difference is that a CPC specifically requires supporting test reports issued by a CPSC-accepted third-party laboratory, whereas a GCC only needs to be based on a "reasonable testing program." For customized backpack brands, testing can be conducted either by the company's internal laboratory or through an outsourced third-party laboratory. In actual Amazon compliance practices, requests for GCC documentation for adult backpacks are far less common and stringent than requests for CPC documentation for children's backpacks. The more common risk remains the misclassification of a product as a children's product, which subsequently triggers CPC requirements. Therefore, clearly communicating the product's positioning in the Amazon listing and avoiding factors that could trigger children's product classification should remain a higher priority than proactively obtaining a GCC.   3.1 Taking Ordinary Adult Textile Backpacks as an Example, the GCC Testing Items Include: The most commonly referenced requirement is the flammability standard for clothing textiles under 16 CFR Part 1610. Although the name of this standard specifically refers to clothing, the CPSC's practical compliance guidance also extends its scope to certain textile products intended to be worn. If the textile materials used in a backpack are included in the assessment, flammability testing is generally conducted in accordance with this standard.   3.2 The GCC Must Also Include Seven Required Items: Clear and traceable product identification; The applicable CPSC safety rules cited, such as the textile flammability requirements under 16 CFR Part 1610; Information identifying the US-based importer or domestic manufacturer; Information about the person responsible for maintaining testing records, including name, address, email address, and telephone number; The specific production date and manufacturing location of the product; The testing date and testing location; Third-party laboratory information: For a GCC, this field is generally completed as "N/A" because third-party testing is not mandatory. However, if third-party testing data are voluntarily used, the relevant laboratory information must be provided.   4. New Requirements After July 2026: CPSC eFiling Electronic Filing   Starting July 8, 2026, consumer products regulated by the CPSC must have their compliance certificate information electronically filed with US Customs when imported into the United States through the eFiling system. In simple terms, previously, once a CPC or GCC certificate had been issued, the seller could retain it and present it if requested during a customs inspection. Under the new system, however, certificate information must be proactively submitted electronically through the US Customs and Border Protection's Automated Commercial Environment (ACE) system at the time of importation. The key point is that eFiling does not change testing requirements and does not require products to undergo retesting. Existing valid test reports remain valid; only the method of submission has changed. However, if you have not coordinated the electronic filing process with your customs broker in advance, your shipment may face inspection delays or even detention when it arrives at the port. The information required for filing includes seven data elements, such as the product ID, applicable regulatory codes, manufacturing date and location, testing date, and laboratory information. For customized backpack brands, this means that an additional coordination step is required within the supply chain and logistics process: Confirm that your US Importer of Record (IOR) or customs broker has the capability to submit declarations through the ACE system, and organize the data from the CPC certificate into the required filing format before shipment. Picture display of the entire process of CPSC eFiling declaration in the United States   5. Compliance Pathways by Product Type Product Classification Key Certifications / Documents Mandatory? Children's backpacks (made entirely of textiles / standard accessories, intended for children aged 12 or younger) CPC certificate and import eFiling Yes Children's backpacks with toy-like features Children's product requirements + ASTM F963 toy safety testing Yes Adult / general-purpose backpacks GCC (if applicable) or compliance documents required by the platform No Backpacks with Bluetooth functionality (e.g., built-in Bluetooth speakers / anti-loss tracking modules) CPC/GCC (depending on product positioning) + FCC ID certification FCC ID is mandatory Backpacks with batteries / charging functionality (e.g., built-in lithium batteries, USB charging ports) Platform compliance documents + UN38.3 transportation test report + MSDS Yes (mandatory for transportation)   6. How We Help Brands Manage Compliance Risks In our cross-border compliance consulting work for customized backpacks, one of the most common situations we encounter is that brands only come to us for urgent confirmation of which compliance documents they need after receiving an Amazon Account Health or performance notification. These notifications typically contain only general requests, such as "Please provide a CPC" or "Please provide a test report." However, they do not specify exactly which testing items are required, who should issue the documents, or how the reports should correspond to specific ASINs to pass Amazon's review. The time and cost involved in making these compliance decisions and repeatedly going through trial and error are often more significant than the testing fees themselves. As a professional backpack factory, I generally put the classification logic outlined above into practice before an order officially enters mass production. Therefore, we recommend that brands provide their target user demographics and a complete list of material compositions before entering the OEM backpack sampling and customization stage. Based on the product positioning, we can help brands identify the specific testing points and applicable standards that need to be communicated to the relevant laboratory. This helps avoid unnecessary costs caused by excessive testing while also preventing subsequent corrective actions resulting from overlooked mandatory testing items. In addition, many custom backpacks are not made from a single material. Instead, they consist of multiple components, including outer fabrics, linings, webbing, zippers, plastic buckles, printed coatings, and special decorative components. During the testing process, several details need to be confirmed with the laboratory in advance: Which components are classified as "accessible components"? Will printed coatings be treated as separate surface coatings requiring independent testing? Do metal buckles need to be evaluated separately for lead content? These are all important details that require advance confirmation. We help brands break down their product structures and identify all material components that need to be tested, avoiding compliance risks caused by testing only the main fabric while overlooking the lining, webbing, or other components. 7. FAQ   Q1: Do ordinary adult backpacks require mandatory certification to be sold on Amazon US? Ordinary adult backpacks without electronic functions generally do not require any unified, mandatory "backpack certification." Sellers must still comply with country-of-origin labeling requirements, truthful advertising regulations, applicable state laws, and Amazon's platform review requirements. However, this does not mean that sellers must obtain CPC, CE, or so-called "FDA certification."   Q2: Do ordinary backpacks require a GCC? Not necessarily. GCC stands for General Certificate of Conformity. It is a written declaration generally translated into Chinese as "General Certificate of Conformity." It applies to general-use products subject to relevant CPSC safety rules, bans, or standards, rather than being a mandatory document required for all consumer products. For ordinary backpacks without electronic functions or special protective purposes, primarily intended for everyday adult use, a separate GCC certificate is generally not required if the product does not trigger any mandatory CPSC standards applicable to specific products or risks.   Q3: Do all children's backpacks need to undergo ASTM F963 and phthalate testing? No. ASTM F963 is a dedicated toy safety standard. A product should not automatically be classified as a toy simply because it is intended for use by children. Only when the backpack itself, its accompanying accessories, or the way the product is marketed and sold gives it clear toy-like characteristics is it necessary to further assess whether toy-related regulations apply.   Q4: Do all children's backpacks need lead content testing? Generally, yes. Lead limits are a fundamental compliance requirement for children's products. For backpacks primarily intended for children aged 12 or younger, the total lead content of components accessible to children must be evaluated to determine whether it complies with the limits established under the CPSIA. It is important to distinguish between lead content testing and phthalate testing, as they are two separate requirements. Lead content testing focuses on lead as a specific heavy metal and has a broader scope of application. Phthalate testing, on the other hand, applies only to specific plasticized materials in children's toys and child care articles. Even if a children's backpack does not require phthalate testing, it will generally still need to undergo lead content evaluation.   Q5: Do products sold on Amazon US need to be differentiated between California and other states? Amazon.com is a unified US marketplace. Ordinary products generally use the same listing and are sold to consumers throughout the United States. Sellers do not need to create separate "California versions" and "other states versions" of their listings. We recommend that brands evaluate their products based on nationwide US sales requirements before listing them on Amazon.   Q6: Must backpacks sold on Amazon have sewn-in fiber content and care labels? When selling backpacks on Amazon US, fiber content labeling is a legal requirement. However, whether a separate care or washing label is mandatory depends on the backpack's material composition and whether it can be washed. Simply put, as long as a backpack contains textile fibers, such as canvas, nylon, or polyester fabrics, it must have a permanently attached fiber content label sewn into the product. Care instructions, including washing or cleaning methods, must also be provided. However, for backpacks that cannot be washed, such as leather or PU products, indicating "Wipe Clean" is generally sufficient. It is not necessary to specify washing instructions in every case.     8. Conclusion For customized backpacks entering the Amazon US marketplace, the key takeaway is that ordinary adult backpacks do not have a unified certification requirement, while children's backpacks generally require a CPC. The key to compliance is to clearly establish the product's positioning before listing it on Amazon and use that classification as the starting point for determining the appropriate certification pathway. Therefore, for customized backpack brands, following the full implementation of CPSC eFiling in 2026, the real task is not simply to obtain the required certificates. Instead, brands should work with a professional bag manufacturer and move compliance assessments forward to the product selection and Amazon listing development stages. First, confirm the intended target users and actual usage scenarios. Then, determine the applicable standards based on the product's material composition, additional features, and target sales regions. Only after these steps should brands prepare the corresponding test reports and compliance documentation.     Author        
  • Why Are Brands Choosing PU Leather for Cosmetic Bags?
    Why Are Brands Choosing PU Leather for Cosmetic Bags? Oct 30, 2026
    Why are more and more brands choosing PU leather for cosmetic bags? The answer is simple — PU leather offers a good balance of practicality, appearance, and cost: Water-Repellent and Easy to Clean: Its surface does not easily absorb water. When exposed to small amounts of toner, lotion, or foundation, stains can usually be wiped away with a damp cloth, reducing the risk of liquids penetrating the material. Good Abrasion Resistance: When placed in a handbag or suitcase for everyday use, PU leather can withstand a certain degree of friction and compression. It is less likely to develop pilling as quickly as ordinary fabric. Rich Textures and Colors: PU leather can be made in various finishes, including glossy, matte, and pebbled textures. It is also available in a wide range of colors, combining the look of leather with fashionable design possibilities. Soft and Easy to Process: It is convenient for sewing, embossing, hot stamping, and creating different bag shapes. It is also suitable for designs featuring zippers, compartments, and linings. Lightweight and Cost-Effective: Compared with genuine leather, PU leather is generally lighter and more cost-effective. It also does not require complicated leather care and maintenance. Higher Material Utilization: Its relatively consistent width and performance help reduce cutting waste, making it suitable for mass production.     Table of Contents • What Is PU Leather? • What Are the Different Surface Finishes of PU Leather? • What Factors Affect the Quality of PU Leather? • How Do We Help Beauty Brands Find the Right PU Leather? • Frequently Asked Questions About Custom Leather Bags / PU Cosmetic Bags • Conclusion   1. What Is PU Leather? PU leather generally refers to artificial leather or synthetic leather products that use polyurethane (commonly abbreviated as PU) as the primary coating or film-forming material. It typically uses woven fabric, knitted fabric, non-woven fabric, or microfiber fabric as its base material. Through processes such as coating, impregnation, lamination, embossing, and surface finishing, it is transformed into a sheet material with the appearance and feel of genuine leather. By applying embossed patterns such as pebbled grain, crosshatch grain, or Nappa grain, PU leather can achieve different leather styles and appearances.   Therefore, PU leather is not natural leather processed from animal hides, nor should it simply be regarded as equivalent to all types of "faux leather." For example, PVC artificial leather also has a leather-like appearance, but its primary coating material, hand feel, flexibility at low temperatures, and processing methods differ from those of PU leather.   Key Advantages: For OEM cosmetic bag manufacturing, the value of PU leather lies in its material structure: the base fabric provides basic dimensional stability and tensile strength, while the polyurethane surface layer is responsible for the hand feel, abrasion resistance, water repellency, and overall appearance. This material structure is highly compatible with the usage environment of cosmetic pouches.   Cosmetic pouches frequently come into contact with foundation, lipstick, toner, and other skincare products. In addition, they must withstand frequent opening and closing, everyday carrying, and compression inside luggage. Therefore, they need to be easy to clean while maintaining a certain degree of flexibility and abrasion resistance.   Compared with ordinary uncoated fabrics, PU leather surfaces are generally less likely to absorb moisture and stains. Minor water stains or cosmetic residue can usually be wiped away with a slightly damp, soft cloth. Compared with genuine leather, PU leather is generally lighter, and its colors, textures, and batch-to-batch consistency are easier to control. It also does not require complicated leather care and maintenance.   2. What Are the Different Surface Finishes of PU Leather? Surface finishing of PU leather can be understood as a series of processes applied after the polyurethane coating has been formed. Through techniques such as embossing, printing, coating, film lamination, and functional finishing, these processes modify the texture, color, gloss, hand feel, and durability of the material. In actual production, multiple finishing techniques are often combined.   2.1 Texture Finishes 2.1.1 Embossing Embossing creates surface textures using embossing rollers or release paper. It is one of the most common surface treatment methods. This process enhances the leather-like appearance and can, to some extent, minimize the visual impact of minor scratches and creases. Common textures: Pebbled grain, crosshatch grain, and crocodile grain.     Special Embossed Patterns: Such as woven patterns, fabric-like textures, wheat-ear patterns, V-shaped patterns, geometric patterns, and wave patterns.   2.1.2 Plain Grain Finish This finish retains a delicate, smooth, and even surface, although it may also feature very subtle natural textures (such as Nappa grain). It is suitable for minimalist cosmetic bags and provides an ideal surface for screen printing, hot stamping, and logo embossing. However, scratches may be more noticeable on this type of surface.   2.1.3 Suede and Matte Velvet Finish This finish creates a soft, matte appearance with a delicate hand feel, producing an effect similar to suede leather. It is suitable for products with a natural, understated style.   2.2 Coating and Surface Finishes 2.2.1 High-Gloss and Mirror Finishes Through surface coating or film lamination, this treatment creates a high-gloss, patent-leather-like appearance. It delivers a strong visual impact and is suitable for gift cosmetic bags, limited-edition fashion collections, and small beauty pouches.   2.2.2 Matte Finish This finish reduces surface reflection, giving the leather a softer and more understated appearance. It is suitable for products positioned around minimalist, natural, or understated luxury styles.   2.2.3 Skin-Like and Soft-Touch Finish By adjusting the surface-layer formulation and coating process, this treatment gives the material a finer, smoother, and more pleasant hand feel. It is suitable for small makeup pouches that emphasize tactile quality.   2.2.4 Oil-Waxed and Vintage Finish This treatment gives the leather a natural sheen, variations in color depth, or a vintage leather appearance. It is suitable for travel toiletry bags and vintage-inspired collections.     2.3 Color and Decorative Finishes 2.3.1 Pearl and Metallic Finishes Pearlescent or metallic effects are incorporated into the surface finish to create appearances such as pearl white, champagne gold, and rose gold. These finishes are commonly used for makeup gift cosmetic bags, holiday gift sets, and loyalty program gift products.   2.3.2 Two-Tone and Multi-Tone Finishes By using differences between the base color and surface color, this treatment creates varying shades in the recessed and raised areas of the texture, enhancing the three-dimensional and vintage effects. The resulting color layers are richer and more dimensional, making this finish suitable for highlighting brand color schemes or coordinating with seasonal theme colors.     2.3.3 Printed Finishes Through screen printing, roller printing, or other suitable printing techniques, brand graphics, animal patterns, or geometric designs can be applied to the surface. This finish is suitable for themed collections and collaboration products.     2.3.4 Laser and Iridescent Finishes Special coatings or films are used to create reflective effects that change depending on the viewing angle. These finishes are suitable for products targeting younger consumers and trend-conscious markets.     2.4 Film Lamination Finishes Transparent, colored, or specially designed optical films are laminated onto the surface of PU leather. This process can create mirror, laser, and iridescent effects while also providing additional protection for printed designs or the leather surface     2.5 Functional Finishes In addition to decorative effects, the following post-processing treatments can also be applied according to the product positioning:  Stain-Resistant and Easy-to-Clean Treatment: Reduces the adhesion of water stains and certain types of dirt to the surface, making everyday cleaning easier.  Scratch-Resistant and Abrasion-Resistant Treatment: Improves the surface's resistance to minor friction and scratches. However, this does not mean the material is completely immune to scratches from sharp objects.  Anti-Yellowing and UV-Resistant Treatment: Slows down color changes caused by light exposure. This is particularly important for light-colored, white, and transparent-looking materials.  Hydrolysis-Resistant and Anti-Aging Treatment: Improves the material's stability in hot and humid environments, reducing the risk of coating powdering, cracking, or becoming sticky after long-term use.  Low-Temperature Flexibility Treatment: Reduces the possibility of the leather surface becoming stiff or cracking when bent in low-temperature environments. It is suitable for products intended for sale or transportation in cold regions.   Some of these performance characteristics come from surface finishing, while others are jointly determined by the base fabric, polyurethane formulation, and overall manufacturing process.   Before customizing a PU leather cosmetic bag, beauty brands can communicate their product usage scenarios and specific requirements to the factory in advance to determine which additional post-processing treatments are necessary.   However, it is important to note that additional post-processing treatments generally require a relatively high minimum order quantity (MOQ). Standard in-stock materials already provide basic stain resistance, water resistance, and abrasion resistance.   3. What Factors Affect the Quality of PU Leather? The quality of PU leather is not determined simply by whether it is "thick enough" or "soft to the touch." The durability of a PU leather material depends on the combined effects of its polyurethane formulation, base fabric, coating structure, and manufacturing processes.   3.1 Polyurethane Resin Formulation Polyurethane resin is the core raw material used to form the PU leather film. Its type, molecular structure, and formulation directly affect the material's softness, resilience, abrasion resistance, hydrolysis resistance, and aging resistance. Polyurethane can be divided into two main systems. Different types of polyurethane have different levels of stability in hot and humid environments: Polyester-Based Polyurethane: This is one of the more commonly used types in the market. It generally offers good abrasion resistance, mechanical strength, and a substantial, full hand feel. However, the ester bonds in its molecular structure are relatively sensitive to hot and humid environments. Prolonged exposure to high temperatures and humidity, or repeated contact with water-based skincare products, may cause hydrolysis. This can lead to a sticky surface, coating powdering, or peeling. Polyether-Based Polyurethane: Due to the relatively greater stability of the ether bonds in its molecular structure under hot and humid conditions, this type generally offers better hydrolysis resistance and low-temperature flexibility. Under the same usage conditions, polyether-based PU leather is less likely to experience coating powdering, stickiness, or significant reductions in strength caused by prolonged moisture exposure. Therefore, for toiletry bags that frequently come into contact with water-based skincare products such as toners and lotions, or are used in high-humidity regions or near bathrooms for extended periods, polyether-based polyurethane is a more reliable resin choice.   3.2 Base Fabric Quality The base fabric serves as the "skeleton" of PU leather. Common types include woven fabric, knitted fabric, non-woven fabric, and microfiber fabric. The main effects of base fabric quality on PU leather can be seen in the following aspects: Influencing Factor Impact on PU Leather Quality Potential Problems if Not Properly Controlled Fiber and Weaving Structure Affects the material's tensile strength, tear strength, and bursting strength, as well as its softness, flexibility, and resistance to deformation. The material may easily deform or tear under stress, or become damaged prematurely in high-stress areas such as handles and bag corners. Weight and Density Affect the material's thickness and fullness, resilience, structural support, and dimensional stability. The material may be too soft or thin, causing the bag to lose its shape or collapse. Uneven density may also result in inconsistent performance across different areas. Base Fabric Uniformity Affects coating distribution, finished material thickness, and hand-feel consistency throughout the entire roll. Uneven surface thickness, horizontal lines or streaks, and inconsistent softness or stiffness may occur, affecting cutting and sewing stability. Bonding with the Coating Determines the adhesion strength between the base fabric and polyurethane coating, affecting folding resistance and peel resistance. Blistering, delamination, peeling, or coating detachment in folded areas may occur during use.     Therefore, even if two types of PU leather use similar surface coatings, differences in their base fabrics can result in significantly different softness, deformation resistance, and durability in the finished materials.   3.3 Coating Structure and Uniformity PU leather is generally not made of just a single layer of coating. Instead, it typically consists of multiple layers, including the base fabric, impregnation layer, foam layer, surface layer, and decorative finish layer. The specific structure varies depending on the manufacturing process and product type.   The following aspects require particular attention:  Is the coating thickness uniform? Areas with coatings that are too thin are more susceptible to wear, while coatings that are too thick may negatively affect flexibility and hand feel.  Are the different layers firmly bonded? Insufficient adhesion can easily lead to peeling, blistering, and delamination.  Is the foaming process uniform? The foam cell structure affects softness, resilience, and folding performance.  Are there any pinholes, bubbles, or impurities? These defects not only affect the appearance but may also become starting points for subsequent cracking or wear.   3.4 Manufacturing Processes Even when using the same raw materials, different manufacturing conditions can result in different product quality. Key parameters include coating application weight, oven temperature, drying time, production speed, tension control, impregnation level, and curing conditions.  Insufficient drying or curing may result in residual odors, a sticky surface, or unstable coating performance.  Improper temperature or production speed control may cause abnormal foam cell structures, surface defects, shrinkage, or color differences.  Excessive production tension may also lead to inconsistencies in material width, thickness, and texture.   Therefore, PU leather quality cannot be evaluated based on hand feel and thickness alone. It is also closely related to polyurethane composition, coating structure, and post-processing techniques.   For a wash bag, what truly affects the user experience is whether the material can maintain its appearance and structural stability after repeated opening and closing, contact with cosmetics, and everyday carrying.   5. How Do We Help Beauty Brands Find the Right PU Leather? 5.1 Thickness Recommendations The common thickness range of PU leather used for bags is approximately 0.6–1.2 mm. Some travel bags and backpacks that require greater structural support use thicker specifications. For makeup bags, the following thickness ranges can serve as a reference:   Finished PU Leather Thickness Material Characteristics Typical Applications Approx. 0.5–0.7 mm Lightweight and soft, easy to fold and sew. Lipstick pouches, flat zipper bags, lightweight promotional gift bags. Approx. 0.6–0.8 mm Offers a relatively balanced combination of softness and durability. Everyday handheld cosmetic bags, small Boston-style bags, standard travel storage bags. Approx. 0.8–1.0 mm Provides enhanced structural support and a fuller bag shape. Semi-structured box bags, wide-opening toiletry pouches, cosmetic bags with compartments. Approx. 1.0–1.2 mm and above Provides stronger structural support and a more rigid, structured appearance. Box-shaped cosmetic bags, cosmetic cases, display-oriented products, and premium gift collections.   The thickness mentioned here generally refers to the finished material thickness, including both the base fabric and the coating. Even two materials with the same thickness may have completely different hand feels due to differences in base fabric density and coating softness or stiffness.   When customizing leather cosmetic bags, thicker material is not necessarily better. The appropriate specifications should be selected according to the product positioning.   For example, soft, small-sized pouches can prioritize lightweight materials and good folding performance. Larger, three-dimensional bags, on the other hand, may require a combination of thicker outer materials, padding, reinforcement materials, or internal support boards to achieve the desired shape.   Using excessively thick materials for small bags may actually result in bulky corners, difficult zipper operation, and challenges when turning the bag inside out during manufacturing.       5.2 Appearance and Texture Recommendations After confirming the bag structure, we can further match the appropriate leather surface finish:  Plain Grain and Fine Nappa Grain: Suitable for minimalist designs and ideal for screen printing, hot stamping, and logo embossing.  Pebbled Grain and Fine-Grain Textures: Offer a stronger leather-like appearance and are suitable for everyday retail products and travel storage bags.  Crosshatch Grain: Creates a clean and refined visual effect, making it suitable for structured and sophisticated cosmetic bags.  Pearlescent, Metallic, Mirror, and Iridescent Finishes: Suitable for holiday limited editions, collaborative collections, and themed gift boxes.  Decorative Textures Such as Crocodile Grain and Woven Patterns: Help strengthen collection recognition and visual identity. However, the proportion and scale of the texture on small cut panels should be carefully evaluated.   Colors can be developed based on brand color cards, Pantone color codes, or physical samples. At the same time, gloss level, embossing depth, and logo application techniques should also be confirmed.   For dark-colored embossed materials, mirror-finish materials, or specially laminated materials, the adhesion performance of hot stamping and printing should be evaluated in advance. This helps avoid situations where the material looks attractive but cannot consistently reproduce the brand logo.   5.3 Verifying Actual Performance Through Sample Testing Material swatches can only be used for preliminary selection. Actual product sampling is necessary to identify potential problems during manufacturing and use.   We pay particular attention to the forming results around sewing lines, edge binding, bag turning, corners, and zipper areas, checking for wrinkles, whitening, corner bursting, or coating cracks.   Considering the actual usage environment of leather cosmetic bags, we can also evaluate the following aspects according to the product positioning:  Color transfer after dry and wet rubbing tests.  Surface and printed-layer conditions after repeated folding and bending.  Surface abrasion resistance, scratch resistance, and coating adhesion performance.  Anti-yellowing and stain-resistance performance of light-colored materials.  Risks of stickiness, powdering, or delamination after exposure to hot and humid aging conditions.  Whether water stains and common cosmetic residues can be easily cleaned.   5.4 Supporting Compliance Testing Based on the Target Market We assist brands in identifying the testing items required according to their target markets and intended consumer groups. Compliance requirements for cosmetic bags and their materials are not entirely the same across different markets.  For products entering the European Union market: Attention should generally be paid to the restricted substance requirements under the REACH Regulation, including restrictions on certain phthalates, heavy metals, and specific azo dyes.  For products entering the United States market: Attention should generally be paid to the chemical substances listed under California Proposition 65, particularly phthalates and lead content. Although Proposition 65 does not directly prohibit the sale of products, it requires warning labels when exposure to listed chemicals exceeds applicable safe-harbor levels. Brands should therefore reserve sufficient space for relevant warnings on product packaging and product pages in advance.  For Asia-Pacific and Southeast Asian markets: Compliance requirements are relatively diverse and vary by country. Some countries refer to the EU REACH Regulation or International Organization for Standardization (ISO) testing methods, but enforcement levels and the scope of random inspections may differ.   For brands exporting products to multiple regions, we recommend prioritizing a relatively comprehensive testing plan, using EU standards as the foundation and supplementing them with specific testing items required by individual destination markets.   This approach can help reduce duplicated testing costs while lowering the risk of products failing random inspections in specific markets.   5.5 Maintaining Consistent Mass Production Quality Through a Standardized Quality Control System SYNBERRY BAG has established in-depth partnerships with dozens of beauty brands worldwide and has consistently followed a strict quality control system, which includes the following procedures:  Incoming Material Inspection: All PU leather raw materials entering our factory are inspected by batch before being stored in the warehouse. We check color, thickness, texture, and hand feel, and compare them with customer-approved samples and standard reference samples. Only after confirming that the materials meet the approved sample specifications can they proceed to the cutting stage.  Cutting and Sewing In-Process Inspection: During the cutting stage, we inspect cut panels for color differences, texture misalignment, surface scratches, and coating peeling. We also verify the cutting layout and material orientation to avoid mixing cut panels from different batches within the same bag.   During the sewing stage, we follow a three-step inspection process: First Article Approval – In-Process Inspection – Finished Product Sampling Inspection.   The first article must be checked to ensure that the bag shape, stitching, zipper position, edge binding, and logo application meet the required specifications. During  in-process inspections, we pay particular attention to sewing tension consistency and whether any stress-bearing areas show signs of pulling or deformation.    Pre-Packaging Inspection: Before packaging, each cosmetic bag is inspected for surface defects, loose threads, dirt, glue overflow, zipper smoothness, lining condition, and hardware durability. We also verify product quantities and label information to prevent mixed colors, incorrect styles, or discrepancies between labels and actual products.  Pre-Shipment Sampling Inspection: Before shipment, a final random inspection is conducted according to AQL standards or an inspection plan mutually agreed upon by both parties to ensure that the appearance and functionality of the entire batch meet the required specifications.   Relevant inspection records, retained samples, and test reports are archived according to each order, making it easier to manage repeat orders, trace customer complaints, and compare different production batches in the future.   Through this closed-loop management system, covering everything from raw materials to finished products, we can minimize the impact of batch variations on material performance to the greatest extent possible.   For beauty brands, choosing a professional cosmetic pouch factory like this not only helps reduce the risk of rework and quality issues at later stages but also contributes to maintaining consistent brand presentation and delivering a stable consumer experience in the market.     6. Frequently Asked Questions About Custom Leather Bags / PU Cosmetic Bags Q1: Is PU leather genuine leather? No. PU leather is generally made using woven fabric, knitted fabric, non-woven fabric, or microfiber fabric as its base material, combined with polyurethane coating, impregnation, and surface finishing processes. It can replicate the textures and hand feel of natural leather, but it is not genuine leather made from processed animal hides.   Q2: Are PU leather and microfiber leather the same material? No. Microfiber leather, also known as microfiber synthetic leather, uses ultra-fine fibers woven through specialized textile processes as its base material. It is then combined with polyurethane resin impregnation and surface coating treatments. Its overall structure and performance are closer to those of natural leather.   PU leather, on the other hand, can use a much wider range of base fabrics, including not only microfiber fabrics but also ordinary woven fabrics, knitted fabrics, and non-woven fabrics. The most noticeable differences between the two are their prices and performance:  Microfiber Leather: Its tear strength, abrasion resistance, folding resistance, and dimensional stability are generally better than those of ordinary PU leather. Its hand feel is also closer to genuine leather, but its cost is correspondingly higher.  PU Leather: Its advantages lie in the wide variety of available textures, colors, and surface finishes, as well as a broader price range. It can accommodate various product positioning requirements, from lightweight promotional items to mid-to-high-end everyday products.  Appearance and Hand Feel: It can be difficult for ordinary consumers to distinguish PU leather from microfiber leather just by looking at or touching them, because both materials can achieve similar surface finishes, such as pebbled grain, plain grain, and Nappa grain. Microfiber leather is also frequently used to develop highly realistic synthetic leather products.   However, differences gradually become apparent after a period of actual use. Microfiber leather generally demonstrates better stability under repeated bending, long-term friction, and humid conditions, with a lower likelihood of delamination, peeling, or coating powdering.   Q3: What Is the Difference Between PU Leather and PVC Artificial Leather? One of the main differences between the two materials lies in their surface composition. PU leather uses polyurethane as its primary film-forming material, while PVC artificial leather is primarily based on a polyvinyl chloride system.   They have different characteristics in terms of hand feel, weight, low-temperature flexibility, processing methods, and application scenarios. Their actual performance still depends on the specific formulation and manufacturing processes, so it is not accurate to simply assume that one material is superior to the other in every aspect.   Q4: What Are Water-Based PU and Solvent-Based PU? The key difference between water-based PU and solvent-based PU lies primarily in the medium used to disperse or dissolve polyurethane during production and processing. Water-based PU uses water as its dispersion medium, while solvent-based PU uses organic solvents as its medium. Both can be used to manufacture PU leather.   However, being "water-based" or "solvent-based" does not directly determine whether the final product is of better or inferior quality. Their main characteristics are as follows: Main Characteristics of Water-Based PU:  Uses water as its dispersion medium, which generally helps reduce the use of organic solvents and related odors.  With an appropriate formulation and manufacturing process, it can achieve a soft and delicate hand feel.  Has relatively high requirements for temperature and humidity conditions in the production environment, drying conditions, and equipment stability.  Water evaporation generally requires a sufficiently thorough drying process, which may increase drying time and energy consumption.   Main Characteristics of Solvent-Based PU:  Has relatively mature film-forming and processing adaptability, making it suitable for a wide variety of textures and surface finishes.  Requires strict control over coating, drying, solvent recovery, and production safety management.  If production control or post-processing is insufficient, it may result in odors, volatile substances, or specific residual solvents. • Its compliance and environmental performance depend on the specific formulation, residual solvent control, exhaust gas treatment, and testing results. It cannot be judged solely by whether it is solvent-based.   Q5: Are PU Leather Makeup Bags Waterproof? PU leather surfaces generally offer a certain degree of water repellency and resistance to liquid penetration. Small amounts of water can usually be wiped away promptly.   However, this does not mean that PU leather is completely waterproof. Moisture may still enter the inside of the cosmetic bag through needle holes, edge binding, seams, or zippers. Therefore, prolonged immersion in water is not recommended.   Q6: Why Does a PU Leather Bag Peel or Crack? Common causes include insufficient adhesion between the coating and base fabric, long-term wear, repeated bending, hydrolysis and aging caused by hot and humid environments, as well as high temperatures, light exposure, or improper storage.   Surface wear does not necessarily mean that the base fabric has already been damaged. However, once the coating begins to powder or peel over a large area, it is generally difficult to restore through simple cleaning.   Q7: How Long Does a PU Leather Makeup Bag Generally Last? There is no fixed lifespan that applies to all types of PU leather.   The service life is affected by factors such as resin formulation, base fabric, coating structure, surface finishing, frequency of use, and storage conditions.   Standard PU leather products on the market generally last around 2–3 years under normal use, while hydrolysis-resistant PU leather can extend this period to approximately 3–5 years without deterioration or peeling.   Q8: What Is the Typical MOQ for Custom PU Cosmetic Bags? The minimum order quantity (MOQ) is generally affected by whether the material is available in stock, whether custom colors or additional surface treatments are required, as well as the bag structure and manufacturing complexity.  Using In-Stock PU Leather and Standard Bag Designs: The MOQ is relatively low, generally starting at around 500 pieces.  Custom Development Requirements: If the order involves new embossing plates, custom embossing patterns, special color dyeing, or specialized finishing treatments, the production line usually needs to be arranged separately. In such cases, the MOQ often increases to more than 1,000 pieces.   Q9: How Long Does Sampling and Mass Production Usually Take for PU Leather Cosmetic Pouches? The sampling lead time for standard designs is generally around 7–15 working days. The exact timeframe depends on the complexity of the bag design, material availability, and logo application requirements.   If new cutting dies, customized hardware, or multiple pattern adjustments are required, the lead time will increase accordingly.   The mass production lead time is generally around 30–40 days. However, production schedules may be further extended during public holidays, peak seasons, or when special post-processing treatments are required.   When planning a product launch, we recommend that brands reserve at least 4–6 weeks of additional buffer time for sample approval and potential revisions. This helps prevent minor design adjustments from affecting the overall product launch schedule.   7. Conclusion For beauty brands, customizing a PU leather cosmetic bag is not simply about choosing a reliable cosmetic bag supplier. It is also a form of proactive management of the overall brand experience.   Every detail of a cosmetic bag, from its appearance and hand feel to zipper smoothness and lining neatness, contributes to the consumer's overall impression of the brand.   Only when the right materials are selected and manufacturing processes are consistently controlled can a product deliver a consistent appearance on retail shelves and a consistent user experience in consumers' hands.   This is also an important foundation for improving repeat purchases and strengthening consumer trust in the brand.       Author        
  • PVC vs. EVA vs. TPU: Which Material Is More Suitable for Transparent Bags?
    PVC vs. EVA vs. TPU: Which Material Is More Suitable for Transparent Bags? Oct 28, 2026
    During the OEM production of transparent bags, PVC, EVA, and TPU are the three most frequently mentioned materials. Among them, PVC has the widest range of applications, TPU offers the most balanced overall performance, while EVA is irreplaceable in specific applications due to its soft feel. Taking common transparent bag applications as examples: PVC, with its highest transparency and lower raw material cost, has long dominated the markets for fast-fashion packaging, promotional gift bags, and mass-produced transparent handbags; TPU, thanks to its excellent elasticity and recovery, low-temperature resistance, and abrasion resistance, has become the preferred choice for high-end cosmetic bags, outdoor waterproof bags, medical device packaging, and transparent storage products that require repeated use; EVA is more commonly used in baby products, stationery pencil cases, and as a lining material in multilayer composite structures where softness and cushioning are important requirements. Table of Contents Differences in Composition Differences in Performance Environmental Friendliness, Compliance, and Safety How Should Brands Make Their Choice? Frequently Asked Questions (FAQs)   I.  Differences in Composition PVC (Polyvinyl Chloride): PVC is a chlorine-containing vinyl polymer that is inherently rigid. Plasticizers (most commonly phthalates such as DOP/DEHP) must be added to make it into a soft, transparent film. Among the three materials, PVC offers the highest transparency and the strongest “crystal-clear” appearance. It also has the lowest raw material cost, which is why PVC has long dominated the low-end transparent bag market. EVA (Ethylene-Vinyl Acetate Copolymer): EVA is a copolymer of ethylene and vinyl acetate. Its softness is determined by the vinyl acetate (VA) content in the molecule: the higher the VA content, the softer and more transparent the material. EVA has natural flexibility without the need for plasticizers, which is the most fundamental difference between EVA and PVC. TPU (Thermoplastic Polyurethane): TPU is a block copolymer whose molecular chains contain both hard segments (which provide strength) and soft segments (which provide elasticity). As a result, it combines the elasticity of rubber with the processability of plastic, making it the only “elastomer” among the three materials.   II.  Differences in Performance 2.1 Transparency and Appearance: PVC > TPU > EVA PVC: Offers the highest light transmittance and the lowest haze, creating a visual appearance closest to “glass.” TPU: Ranks second in transparency. High-transparency TPU films can achieve light transmittance of over 90%. EVA: Typically has a light transmittance of around 85% and may appear slightly translucent, especially when the VA content is high. It offers the soft texture of “frosted crystal” rather than the sharp, crystal-clear transparency of PVC. 2.2 Softness and Hand Feel: EVA > TPU > PVC EVA: The softest of the three materials. With a Shore hardness of 60–70, it feels almost structureless when held in the hand. However, EVA's softness is associated with permanent deformation, meaning that creases tend to remain after folding. TPU: TPU offers a completely different type of softness—it is characterized by elastic recovery. When pressed or squeezed, it quickly returns to its original shape. PVC: The softness of PVC depends on the addition of plasticizers. Its hand feel often has a distinct “slippery” or “rubbery” texture, lacking the warm, smooth tactile quality of premium fabrics. It also tends to harden at low temperatures. 2.3 Temperature Resistance: TPU > EVA > PVC TPU: The best performer, typically with a temperature resistance range of -30°C to +80°C. It does not become brittle at low temperatures or soften and deform at high temperatures. EVA: Ranks second, with a temperature resistance range of approximately -20°C to +60°C. It tends to soften and stick together at high temperatures. PVC: The weakest performer. It becomes hard and brittle at low temperatures, making the corners prone to cracking in winter. At high temperatures, plasticizers may migrate out of the material, causing the film surface to become sticky.   2.4 Abrasion Resistance / Surface Scratch Resistance: TPU > PVC > EVA TPU: Has an absolute advantage in abrasion resistance among the three materials. This makes it almost irreplaceable in applications involving repeated friction, frequent contact with the contents, or long-term carrying and use. PVC: Ranks second. Its surface is initially glossy, but its overall abrasion resistance is weaker than that of TPU after repeated friction. However, the scratch resistance of high-quality PVC films has improved significantly through adjustments to their formulations, including surface hardness. EVA: Although the material is relatively soft, its surface strength is limited. It is more prone to scratches and abrasion marks during use, especially at the corners of the bag and in areas subjected to stress and repeated folding. After long-term use, its transparency and overall appearance deteriorate noticeably.   2.5 Visual Lifespan: Resistance to Yellowing and Whitening During the long-term use of transparent bags, resistance to yellowing and haze formation directly determines the product's visual lifespan. The differences among the three materials in this dimension reflect real-world user experience more accurately than short-term performance data.   Yellowing and whitening have different causes. Yellowing mainly occurs when the molecular structure of a material undergoes oxidative degradation after exposure to ultraviolet light, thermal oxidation, or contact with certain substances, resulting in the formation of chromophoric groups. Whitening, on the other hand, is often caused by additives or oligomers migrating to the surface and accumulating there to form fine precipitates, causing the film surface to lose its transparency. These two phenomena are often confused, but their mechanisms of damage to the appearance of transparent bags are completely different.   PVC: The root cause of yellowing in PVC still lies in its plasticizers. Phthalate-based plasticizers gradually oxidize under the influence of light and heat, producing colored substances such as quinones that cause the originally clear film surface to turn yellow. At the same time, the continuous migration of plasticizers to the surface can form an oily film that attracts dust, making the surface appear hazy. Both of these changes are irreversible.   However, selecting high-quality PVC made with environmentally friendly plasticizers can delay the onset of yellowing. For short-term applications such as fast-fashion packaging, this drawback may be acceptable. For mid-to-high-end products that require long-term display or repeated use, however, PVC's performance still needs to be evaluated carefully. EVA: EVA generally offers better resistance to yellowing than PVC. Its molecular chains do not contain easily decomposable chlorine atoms, so the initial rate of yellowing is slower. Under normal indoor lighting conditions, it can maintain its transparency for a relatively long period. However, the VA segments in EVA are relatively sensitive to thermal oxidation. Under continuous heat exposure or ultraviolet radiation, they can still undergo gradual oxidation, causing the surface to become increasingly sticky and develop slight yellowing over time. TPU needs to be discussed in two categories. The first category is standard, general-purpose TPU film: This typically refers to aromatic polyester-based TPU. This type of TPU has the weakest resistance to yellowing and whitening among the three materials. Over time and as usage conditions change, surface deposits may migrate to the surface, causing bloom-like deposits and a whitish appearance. This irreversible whitening is caused by the migration of additives and oligomers. It is particularly likely to become noticeable under conditions of high temperature, high humidity, or prolonged compression. This is a characteristic of conventional TPU rather than a quality defect. Therefore, transparent bags made from aromatic TPU are more suitable for indoor use or applications where color changes are not a major concern. The second category is high-quality modified TPU: This refers to aliphatic polyether-based TPU, which offers greater stability in terms of transparency and resistance to surface blooming, effectively delaying the onset of surface deposits. It can maintain a high level of light transmittance even after long-term outdoor use, making it a key material choice for high-end transparent bag products. In terms of ranking, resistance to yellowing is as follows: Aliphatic TPU > Aromatic TPU > EVA > PVC. Resistance to whitening is approximately: Aliphatic TPU ≥ EVA > PVC > Aromatic TPU. When selecting materials, if a brand has specific requirements for the long-term transparency of its transparent bags, aliphatic TPU should be the first choice. If overall performance is the main consideration and appearance lifespan is not a major concern, aromatic TPU can be selected.   2.6 Welding and Processability: PVC > TPU > EVA All three materials can be joined using high-frequency heat sealing or ultrasonic welding, but their performance differs significantly. PVC: Offers the best high-frequency welding performance because its molecules contain highly polar chlorine atoms. Under a high-frequency electric field, PVC exhibits high dielectric loss and high heating efficiency, resulting in fast heat-sealing speeds and stable seam strength. This makes it suitable for rapid, large-scale production. However, PVC releases chlorine-containing gases during welding, so adequate ventilation equipment is required; otherwise, it can adversely affect the working environment. TPU: Its high-frequency welding performance falls between PVC and EVA. TPU is a thermoplastic elastomer with a relatively broad melting temperature range, making it highly adaptable to ultrasonic welding. Its weld seams are flexible and resistant to cracking, which is particularly important for the corners of transparent bags that need to withstand repeated bending. However, high-frequency heat sealing of TPU requires higher frequencies and longer welding times, resulting in lower production efficiency than PVC. In addition, TPU film tends to stick to the mold surface during processing, so release treatment is required. EVA: Has the weakest high-frequency welding performance. EVA molecules are relatively less polar, so its heating efficiency during high-frequency heat sealing is lower than that of PVC and TPU. However, acceptable weld seams can still be achieved by appropriately adjusting welding parameters and mold pressure. Nevertheless, EVA has a relatively low melting point and a low heat distortion temperature, requiring more precise control of temperature and welding time. Even a slight error can easily result in burn-through or whitening of the weld seams. III.  Environmental Friendliness, Compliance, and Safety From the perspective of environmental friendliness, regulatory compliance, and safety, the differences among the three materials deserve even greater attention than their performance differences. These factors directly determine whether a product can enter its target market and whether it can be used for specific groups of people and in specific applications. They are also the key factors that truly distinguish the three materials.   3.1 PVC: The Biggest Concern Is Plasticizers The main concern with PVC lies in its plasticizers. Commonly used phthalate-based plasticizers in PVC, such as DEHP and DOP, may gradually migrate out of the material during prolonged contact with skin or oils, or when exposed to high-temperature environments.   European Union Market: The EU REACH Regulation has included certain phthalate-based plasticizers on the Candidate List of Substances of Very High Concern (SVHC) and restricts their use in children's products, food-contact materials, and medical devices. If the target market is the EU, it is recommended that the materials comply with EU REACH requirements. U.S. Market: If products are sold in California, the exposure warning requirements under California Proposition 65 for phthalate plasticizers such as DEHP must also be considered. Typically, an 8P phthalate test is required.   As a professional bag manufacturer, SYNBERRY selects materials that meet the environmental requirements of the target market based on the customer's market region and product application, ensuring that products meet the applicable regulatory requirements before export.   3.2 EVA: Plasticizer-Free and Chlorine-Free EVA does not contain plasticizers and has no chlorine in its composition, making it significantly better than PVC in terms of environmental friendliness and safety assessments. EVA has a long history of use in food-contact materials and children's toys. For general-purpose transparent bags, using EVA can substantially reduce regulatory compliance burdens. However, when in contact with oily contents, EVA offers lower resistance to oil and grease migration and lower long-term stability than TPU. Therefore, careful evaluation is still necessary for applications involving high-oil-content cosmetics or products that require repeated cleaning and disinfection.   3.3 TPU: The Most Advantageous in Terms of Regulatory Compliance TPU offers the greatest advantages in terms of regulatory compliance. It has good biocompatibility, can achieve softness and elasticity without the need for plasticizers, and certain types of TPU can be recycled. For high-end cosmetic bags, medical device packaging, and transparent bags exported to regions with strict environmental standards, TPU is a reliable choice for applications with the highest safety requirements. IV.  How Should Brands Choose? Start with the Application Scenario, Then Determine the Material Solution When translating the differences in composition, performance, and regulatory compliance discussed above into practical material selection, the choice of material for transparent bags should satisfy three key dimensions: whether safety and regulatory requirements are met in the target market, whether performance can withstand the actual intensity of use, and whether the cost matches the product positioning.   4.1 Compliance Considerations in the OEM Process for Cosmetic Bags From a safety and regulatory compliance perspective, whenever the target market is a region such as the European Union or California in the United States, where there are explicit restrictions on phthalate plasticizers, PVC should be carefully evaluated as a material or downgraded to an alternative option. This is because the risk of plasticizer migration is the most prominent among the three materials. Both EVA and TPU can meet requirements in this regard. However, if the contents have a high oil content or the product requires repeated cleaning and disinfection, EVA has relatively weak resistance to oil and grease migration, making TPU the more reliable choice.   4.2 Performance Requirements Based on Application Scenarios From the perspective of usage intensity, transparent bags intended for fast fashion or short-term use do not have high requirements for elastic recovery, abrasion resistance, or temperature resistance. PVC can meet these needs at a relatively low cost. However, for products that need to be opened and closed repeatedly, bent frequently, carried over long periods, or potentially used in low-temperature environments, PVC's weaknesses in brittleness and abrasion resistance will quickly become apparent. TPU's advantages in elastic recovery and flex-fatigue resistance translate directly into a noticeable difference in user experience.   The following table compares the suitable applications of the three materials based on actual transparent bag applications:   Bag Type or Requirement Preferred Material Reason for Selection Promotional giveaway cosmetic bags PVC Low cost, high transparency, and mature printing processes Mass-market retail transparent cosmetic bags PVC or EVA PVC is more cost-effective and offers greater stiffness, while EVA is lighter and has a softer hand feel Mid-to-high-end branded cosmetic bags TPU TPU is more durable, and its perceived quality can be enhanced through thickness selection, hardware, and printing Travel toiletry and storage bags All three materials are suitable Lightweight and easy to clean, making them suitable for general travel storage Storage bags for frequent business travel and long-term use TPU Abrasion-resistant and fold-resistant, suitable for frequent use Beach bags and transparent shopping bags PVC Easy to manufacture in large sizes, maintains a structured shape, and allows costs to be controlled Outdoor waterproof bags and stream-crossing bags TPU Good toughness and abrasion resistance, suitable for more demanding environments Protective bags for electronic products such as mobile phones and cameras TPU Offers better advantages in scratch resistance, fold resistance, and protective performance Children's stationery bags and lightweight, soft storage bags EVA Lightweight and soft, with a gentle hand feel, but chemical safety must still be verified according to children's product requirements Bags used in low-temperature environments TPU Generally more suitable than standard PVC and EVA for low-temperature conditions and repeated bending Bags emphasizing high transparency and a “glass-like” appearance PVC or high-transparency TPU Better suited to achieving a highly transparent appearance, depending on the film grade and thickness     4.3 Cost Considerations From a cost perspective, in terms of raw material unit prices, PVC is the least expensive, EVA comes next, and TPU is the most expensive. This is the most immediately noticeable difference among the three materials at the quotation stage. PVC: PVC has the most significant raw material price advantage and the highest efficiency in high-frequency welding, making it suitable for rapid, large-scale production. Therefore, when production capacity is sufficient and order volumes are large, PVC can achieve the lowest unit cost among the three materials. However, this conclusion applies only to markets with relatively lenient compliance requirements, short product usage cycles, and no contact with sensitive contents. Once exports to the EU or California in the United States are involved, the additional costs of environmentally friendly plasticizers required to meet REACH and Proposition 65 requirements, third-party testing fees, and supply chain traceability management can significantly increase PVC's overall cost. EVA: EVA has a relatively transparent cost structure. Its raw material price is higher than PVC but significantly lower than TPU. Its processing requirements are not particularly demanding. Although high-frequency heat sealing is slightly less efficient, finished-product waste rates and quality fluctuations can be kept within reasonable limits under experienced production conditions. Its greater cost advantage comes from the stability of its compliance profile: EVA requires no additional plasticizers and contains no chlorine, so most basic compliance tests do not need to be repeatedly commissioned.   The overall cost ranking of TPU also needs to be discussed in two categories: Aromatic TPU: Its price is at the lower end of the TPU range. Although its overall cost remains higher than that of EVA and PVC, it is relatively more economical than aliphatic TPU. Aliphatic TPU: Compared with aromatic TPU, its procurement price is even higher, and spot-market inventory is less stable.   The following table compares the costs of these three materials across multiple dimensions, assuming the same dimensions and thickness.   Comparison Item PVC Transparent Film EVA Transparent Film TPU Transparent Film Procurement Cost Lowest; mature supply chain and relatively stable prices Medium; generally more expensive than PVC Highest; significantly more expensive than PVC and EVA Material Density Relatively high; greater material weight for the same area and thickness Relatively low; lighter weight per unit area Generally between EVA and PVC Cost of Achieving the Same Softness Low; softness can be adjusted relatively easily through the plasticizer system Medium; softness depends on VA content High; significant price differences exist between hardness levels and grades Cost of Achieving Transparency Standard high transparency is easy to achieve at low cost Costs increase when high transparency is required Higher costs for high transparency and low haze Printing and Lamination Costs Mature processes, with a wide range of options such as screen printing and UV printing Surface adhesion and ink compatibility are inferior to PVC Printing, lamination, and surface treatment generally require higher standards Production Waste Low; factories have extensive processing experience Medium; wrinkles caused by heat, sticking, and dimensional stability need to be controlled Medium to high; stricter requirements for temperature, tension, and surface protection Overall Finished-Product Cost Low Medium High Suitable Cost Positioning Mass-market promotional products and price-sensitive orders Mid-range products emphasizing lightweight construction, softness, and environmental friendliness Mid-to-high-end products emphasizing durability, low-temperature resistance, and high quality   V.  Frequently Asked Questions About Transparent Cosmetic Bag OEM Q1: What Should You Do When a Transparent Cosmetic Bag Turns Yellow? Can It Be Restored? This is one of the most frequently asked questions in transparent bag OEM consultations. The conclusion is straightforward: once yellowing or haze develops, there is generally no way to restore the original appearance through washing, wiping, or simple treatments.   As discussed earlier, yellowing essentially results from oxidative degradation of the material's molecular structure, which produces new chromophoric groups. Haze, on the other hand, occurs when plasticizers or oligomers migrate to the surface and form a layer of deposits. These are not surface contaminants; they are changes within the material itself. Wiping with alcohol may temporarily remove the surface oil film, but the deposits will accumulate again after a few days. Applying hot air or ironing the material will not restore its transparency and may instead accelerate plasticizer migration and material aging.   Q2: Can PVC Transparent Bags Be Exported to the EU? Yes, but there are specific conditions. PVC itself is not completely banned in the EU. The main concerns involve plasticizers and heavy-metal stabilizers. As long as the selected PVC film passes REACH testing and any additional tests specified by the customer, PVC transparent bags can still enter the EU market.   Q3: Why Do Different Factories Quote Such Different Prices for the Same TPU Transparent Bag? The differences mainly come from four areas. First, material grade. Although all these materials are called TPU, prices can vary by more than twofold between aromatic polyester-based TPU, aliphatic polyether-based TPU, and films with different hardness levels and extrusion processes. Some quotations use recycled or blended materials. Their transparency may be acceptable, but their resistance to yellowing and surface blooming can be significantly worse.  Second, film thickness. Common thicknesses for transparent cosmetic bags range from 0.2 mm to 0.5 mm. A quotation may specify a thickness of 0.3 mm, while the actual finished product may be only 0.25 mm or even thinner. Thickness differences directly affect material costs and also influence the bag's stiffness and durability. Third, processing details. Transparent films are easily contaminated or scratched during sewing operations. This requires sufficient attention to the production environment, operating techniques, and quality control standards. Fourth, packaging details. TPU film tends to stick to itself. Whether interleaving tissue paper is required, whether moisture-proof bags or standard PE bags are used, and whether desiccants are included will all affect the unit cost.   Q4: If a Transparent Bag Has an Unpleasant Odor, Does That Mean There Is a Problem with the Material? Unpleasant odors from transparent bags generally come from two sources. First, plasticizer volatilization in PVC. The odor is particularly noticeable immediately after opening the package. It may weaken over time but cannot be eliminated completely, and it becomes more pronounced in sealed packaging or high-temperature environments. Second, residual solvents and low-molecular-weight decomposition products from the manufacturing process. These odors generally diminish significantly after the product has been left in a well-ventilated area for several days.   If a customer reports an odor problem after receiving a bulk order, the first step is to confirm the material type. EVA and aliphatic TPU generally have much lower inherent odors than PVC, making them more suitable for odor-sensitive applications, such as maternal and infant products or cosmetic products that remain close to the face for extended periods.   The second step is to inspect the packaging method. Sealed plastic bags trap odors inside. It is advisable to add a ventilation step before shipment or switch to more breathable packaging materials.   Q5: Can Transparent Bags Be Printed? Will the Printing Fade or Peel Off? Yes, transparent bags can be printed, but different materials have significantly different processing requirements. PVC: Generally the easiest to print, with mature processes that make it suitable for products requiring consistent mass production and vibrant colors. TPU: Can also deliver excellent printing results, but the ink and surface treatment must be properly matched. Adhesion must be carefully evaluated, especially when the material is repeatedly bent or stretched. EVA: Can be printed, but ink adhesion is affected by the formulation, surface condition, and hardness of the material. Actual sample testing is generally required beforehand.   Therefore, if a product has high requirements for print color and pattern complexity, PVC or surface-treated EVA is generally a more reliable choice. For TPU transparent bags, it is advisable to confirm the printing solution with the factory during the design stage rather than discovering inadequate adhesion during sampling.   Q6: Do Transparent Bags Become Hard in Winter? This depends on the material. PVC becomes noticeably harder at low temperatures, especially in thin sections and at the corners. Changes in hand feel become obvious below 10°C, and cracking during bending may even occur below 0°C.   EVA performs somewhat better than PVC at low temperatures, but it can still become harder below -10°C.   For outdoor use in winter or cold-chain transportation, TPU is a more reliable choice. Standard TPU can generally maintain its flexibility at temperatures around -30°C.   Q7: TPU Cosmetic Bags Develop Blooming or Whitening After a Period of Use. Can This Be Prevented? The onset of whitening can be delayed, but it is difficult to prevent it completely. The key factors are the TPU grade and formulation system.   Blooming and whitening essentially occur when low-molecular-weight substances, such as components of the TPU soft segments and additives, migrate to the surface and gradually precipitate after temperature changes, repeated bending, or prolonged storage. Unlike plasticizer migration in PVC, this phenomenon does not affect the material's chemical safety or mechanical strength. However, it creates a white, hazy, or powdery layer on the film surface, directly compromising the appearance of the transparent bag.   There are three main ways to reduce the likelihood of this problem. First, material selection. Different TPU grades vary significantly in their tendency to form surface deposits. Aliphatic polyether-based TPU generally offers more stable resistance to blooming and hydrolysis than aromatic polyester-based TPU. Second, formulation control. During TPU film production, slip agents, antioxidants, and mold-release additives may be incorporated. The types and quantities of these additives directly determine the rate and extent of subsequent blooming. Reputable film manufacturers adjust their formulations according to the intended application to keep the risk of surface deposits low. Some low-cost films, however, use excessive amounts of low-molecular-weight additives to improve processability, which can significantly worsen whitening after a period of use. Third, usage and storage conditions. High temperatures, high humidity, and frequent temperature fluctuations accelerate the migration of low-molecular-weight substances. During long-term storage, TPU transparent bags should be kept away from enclosed, high-temperature environments and should not remain in prolonged, close contact with dark-colored fabrics or other materials.   Q8: How Can You Select a Suitable Cosmetic Bag Manufacturer? When selecting a factory for products such as transparent cosmetic bags, price alone should not be the deciding factor. Greater priority should be given to material expertise, sampling response speed, and consistency in quality control. Many problems with transparent materials are not determined by machine precision alone, but rather by experience and attention to detail. First, determine whether the factory genuinely understands material differences. Many factories work exclusively with PVC and lack experience in processing TPU and EVA. Once a brand switches from PVC to TPU, sewing tension and packaging methods may need to be readjusted. A genuinely experienced factory can explain the performance differences among materials for different applications during the sampling stage, rather than relying on repeated trial and error after samples have been produced. Second, evaluate the factory's attention to detail during sampling. The most visible problems with transparent bags often emerge during the prototype stage rather than mass production. For example, whether the film surface gets scratched during sewing, whether the stitching is even and free of seam blowouts, and whether corners develop wrinkles due to improper tension control all reflect the factory's on-site management and workers' skill levels. If basic cleanliness cannot be maintained during sampling, the likelihood of widespread scratches and contamination during mass production will increase significantly. Third, check whether quality control checkpoints are clearly defined. Transparent film materials require professional and systematic procedures for incoming material inspection, surface protection after cutting, cleanliness during sewing, and assessment of yellowing and blooming risks during finished-product sampling inspections. Fourth, evaluate the factory's export and compliance support. Transparent cosmetic bags often need to meet requirements such as EU REACH and California Proposition 65 in the United States. Whether the factory is willing to retain samples from different production batches and cooperate with third-party testing directly affects whether orders can be exported smoothly.   Overall, a transparent cosmetic bag manufacturer suitable for long-term cooperation should meet at least three conditions: Have practical mass-production experience with all three materials: PVC, EVA, and TPU. Be able to control film cleanliness, scratching, and sewing-related issues during sampling. Be willing to cooperate with testing requirements for export compliance.   Price is certainly important. However, for transparent bags, which are sensitive to both appearance and regulatory compliance, a “low price” is meaningful only when both product quality and documentation meet the required standards.   Author        
  • How to Measure Backpack Capacity in Liters?
    How to Measure Backpack Capacity in Liters? Oct 26, 2026
    There are two widely used methods for measuring backpack capacity: geometric volume estimation and the ASTM F2153 fill test. During the design stage, the geometric formula (internal length × width × depth ÷ 1,000, multiplied by a pattern correction factor when necessary) can be used to estimate the maximum capacity. For sample approval and production capacity labeling, the unexpanded capacity measured using the ASTM F2153 fill test is generally used as the baseline. Geometric estimation is best suited to structured bags with regular shapes for preliminary space planning. Applying this method directly to sewn backpacks usually overestimates capacity. The fill test uses rigid plastic spheres with a diameter of 20 mm to fill all enclosed compartments; the spheres are then transferred to a calibrated measuring container to determine volume. The result can be used in purchase contracts, technical packs, inspection criteria, and product capacity labeling. For custom bag manufacturing, specifying the measurement method, included compartments, and tolerance alongside the capacity value helps align acceptance criteria between buyers and suppliers. Table of Contents Ⅰ. Why Backpacks with the Same Labeled Capacity Can Have Different Actual Volumes Ⅱ. Geometric Formula Estimation Ⅲ. ASTM F2153 Fill Test Ⅳ. Practical Recommendations for Backpack OEM Projects Ⅴ. Frequently Asked Questions (FAQ) Ⅵ. Conclusion   Ⅰ. Why Backpacks with the Same Labeled Capacity Can Have Different Actual Volumes   1. Backpack Capacity Has No Globally Uniform Mandatory Labeling Standard Unlike shoe sizing or fabric weight, backpack capacity is not subject to a globally uniform mandatory labeling rule. Products labeled as 30 L may be measured using four common methods in the industry, producing different usable-volume results. Measurement method What is measured Typical result Notes Multiply external dimensions External length × width × height of the bag Likely to be overstated Counts fabric, foam, and back-panel structures as volume; unsuitable for labeled capacity. Main compartment only Largest enclosed main-compartment space Conservative Perceived usable space may exceed the labeled value, but the scope is limited and comparisons are less meaningful. Add all enclosed pockets Main compartment, zippered pockets, and covered enclosed pockets More comparable Closer to the logic of ASTM F2153; agree in advance whether open pockets are included. Promote expanded capacity Capacity with the roll-top or expansion zipper fully opened Represents maximum expanded state only Volume is lower in the normally closed state; some expanded bags may exceed airline carry-on limits.   2. Main Reasons for Differences in the Same Labeled Capacity For a daypack labeled 30 L, an external-dimension calculation includes space occupied by the back panel and shoulder-strap structure. Under the ASTM F2153 fill test, only enclosed compartments are counted; mesh water-bottle pockets and open front stash pockets are excluded. As a result, the unexpanded measured capacity may be only 24–25 L. Such differences are usually not manufacturing defects. They primarily result from different measurement methods and boundaries for what is included.   3. Capacity Must Be Matched to the Intended Use State Capacity can be reported as unexpanded capacity and expanded capacity. Unexpanded capacity refers to the bag in its normally closed, everyday-use configuration. Expanded capacity is the maximum volume available when a roll-top is fully opened or an expansion zipper is completely unzipped. A specification sheet that lists only one capacity value does not clearly identify the intended use state and makes inspection decisions more difficult. For roll-top bags and bags with expansion zippers, also verify the fully loaded external dimensions to determine whether the bag meets carry-on baggage size limits.   Ⅱ. Geometric Formula Estimation   1. Basic Formula and Units A general geometric formula used in backpack OEM development is: Capacity (L) = Internal Length (cm) × Internal Width (cm) × Internal Depth (cm) ÷ 1,000 Example: With internal dimensions of 50 × 30 × 20 cm, the theoretical capacity is 50 × 30 × 20 ÷ 1,000 = 30 L. The formula uses centimeters and returns liters, based on 1 L = 1,000 cm³. For the North American market, capacity may also be listed in cubic inches; 1 L ≈ 61.024 cu in.   2. Appropriate Uses of the Geometric Formula • Reverse-engineering target dimensions during concept design: allocate internal usable dimensions based on the target capacity to support pattern and construction development. • Quickly estimating a capacity range during initial inquiries: when no physical sample is available, use external dimensions to make a preliminary assessment of the product category and support quotation and process evaluation. • Planning internal space before sampling: allocate space among the main compartment, laptop compartment, and front pockets, using the result as a theoretical upper-limit reference.   3. Why the Geometric Formula Can Be Inaccurate for Sewn Backpacks • The bag is not a perfect rectangular prism: daypacks that taper toward the top, roll-top bags, flap-top bags, and packs with curved suspension profiles have irregular shapes that cannot be accurately represented by a rectangular prism. • Fabric, foam, and suspension components reduce usable volume: laptop sleeves, back panels, and shoulder-strap anchor structures occupy space within the bag’s external profile. • Pocket-counting rules vary: external-dimension calculations may include side and front pockets, whereas standard fill testing counts enclosed compartments only and excludes open mesh pockets. • Seam allowances and lining thickness reduce usable space: sewing allowances, lining, and reinforcement materials reduce the effective internal volume. Conclusion: The geometric formula is a design-screening tool for estimating theoretical maximum volume; it should not be used directly as the labeled capacity of a sewn backpack. Results are more accurate for rectangular tote bags and simple travel duffels. For backpacks, technical outdoor packs, and styles with multiple complex compartments, capacity acceptance should be based on a fill test.   4. Early-Stage Estimation Before Sampling: Pattern Correction Factors During early development, before a physical sample is available, a pattern correction factor can help narrow the gap between theoretical and measured capacity. The adjusted formula is: Estimated capacity (L) ≈ [Internal length × internal width × internal depth (cm) ÷ 1,000] × K Select K according to the regularity of the bag’s shape. The ranges below are based on pattern databases and industry experience and are for design estimates only—not for official capacity labeling. The estimate must ultimately be calibrated against an ASTM fill test. Bag construction Reference correction factor Notes Boxy business backpack 0.80–0.85 Regular shape with high space efficiency. Standard daypack 0.75–0.80 Slightly contoured shape and space occupied by compartments. Outdoor hiking pack (internal aluminum-frame back panel) 0.70–0.75 Suspension system takes up more internal volume. Cylindrical duffel 0.72–0.78 Curved side walls reduce usable volume. Roll-top backpack 0.65–0.75 The rolled closure section is excluded from effective capacity. Tapered daypack, narrower at the top 0.70–0.78 The tapered cross-section makes the upper space less efficient. Example: A standard daypack with internal dimensions of 45 × 30 × 18 cm has a theoretical volume of 24.3 L. Using a correction factor of 0.78 gives an estimated capacity of approximately 19 L; subsequent fill testing will generally yield around 18–20 L. Important limitation: Correction factors are not universally transferable across factories or patterns. If the fabric weight or lining construction changes, re-test the bag and recalibrate K. In external technical communications, label this figure as a “design estimate,” not the contractual labeled capacity.   Ⅲ. ASTM F2153 Fill Test   1. Standard Overview and Scope A commonly used industry standard for backpack capacity testing is ASTM F2153, “Standard Test Method for Measurement of Backpack Capacity.” It is a voluntary test method intended to establish consistent, comparable capacity-measurement rules among brands, factories, and inspection teams.  Key principles: report both unexpanded and expanded capacity; count enclosed compartments only; exclude open mesh water-bottle pockets, open front stash pockets, and open compression pockets. The standard generally does not apply to small bags under 4 L. Crossbody mini bags, waist packs, and small organizers do not need to be labeled in liters; if a capacity value is provided, identify the alternative simplified test method used.   2. Standard Filling and Volume-Reading Procedure Step Procedure Control point 1. Prepare the test media Use uniform rigid plastic spheres with a diameter of 20 mm, commonly PP or PS. Foam beads and beans are for rough internal checks only; they compress or settle and have poor repeatability. Do not use them for official capacity labeling. 2. Fill all enclosed compartments Fill the main compartment and every zippered pocket. For roll-top bags, fill to the agreed number of rolls while ensuring normal closure. Close zippers after filling without pulling them taut. Do not omit any enclosed compartment. Exclude all open pockets. 3. Use a consistent settling procedure Gently shake the bag so the spheres settle naturally. A common procedure is three gentle shakes, approximately 10 seconds each. Do not deliberately press or compress the bag to inflate the reading. 4. Transfer the spheres to a calibrated measuring container Transfer all spheres into a graduated container calibrated by water-volume measurement. Gently agitate until the spheres settle, then record the volume. Large backpacks may be measured in multiple batches and the readings added together. Calibrate measuring equipment with water periodically and retain calibration records. 5. Repeat the test and average the results Conduct at least two independent tests. If the results differ by more than 1–2 L, filling or settling procedures may not have been consistent; repeat the test. Use the same spheres and measuring equipment for first-piece, in-line, and final inspections.   3. Limitations of the Standard and Its Relationship to Specification Sheets ASTM F2153 is voluntary and is not legally mandatory. Many retail product listings also omit the test method. The value of the test is that it allows the fill media, measuring equipment, included compartments, and tolerances to be defined in the specification sheet. If only a capacity number is listed without test details, results from different stages cannot be reliably compared.   4. When Full Laboratory Equipment Is Unavailable: Simplified Measurement Methods Not every inspection site has enough standard plastic spheres and calibrated measuring containers. A simplified method may be used during sampling, but the specification sheet must state that it differs from ASTM F2153. Scenario Simplified method Notes Compartments of 4 L or more Fill with 20 mm plastic spheres or uniform dry beans, then measure using a 1 L measuring cup and add the readings. Beans are for internal reference only; rigid plastic spheres are preferred for official capacity labeling. Compartments under 4 L Because small spheres stack with greater error, weigh the filling material first and convert to volume using a defined ratio if necessary. State in the documentation: “Not the ASTM F2153 standard procedure.” Curved or tapered bags Fill in vertical sections and add the readings from each section. A single rectangular-prism calculation will overestimate the capacity of tapered bags. Backpacks with multiple compartments Fill and measure each enclosed compartment separately, then total the results; list open pockets separately as excluded. Keep separate records to avoid confusion over what is included. Important: Capacity values obtained using different measurement methods should not be compared directly.   Ⅳ. Practical Recommendations for Backpack OEM Projects   1. Recommended Capacity Fields for Specification Sheets To reduce the risk of a finished product’s capacity differing from expectations, include the following six items in the capacity section of the specification sheet: Field Recommended wording Purpose Measurement method “ASTM F2153 fill test using 20 mm PP spheres” / “Calculated from external dimensions; design reference only.” Identifies the method used to determine capacity. Unexpanded capacity Capacity in liters in the normally closed state. Matches typical use and product labeling. Expanded capacity Capacity in liters with the expansion zipper fully open or the roll-top fully unrolled. Distinguishes maximum expanded volume. Compartments included “Includes the main compartment and all zippered pockets; excludes mesh water-bottle pockets and open front stash pockets.” Removes ambiguity about which pockets count. Units List L and cu in together and specify the conversion. Supports reading preferences in different Western markets. Tolerance Agree on a tolerance by capacity range; use the same test method when judging compliance. Sets a reasonable acceptance range for inspection.   2. Example Wording for a Specification Sheet Capacity: 28 L unexpanded (approx. 1,709 cu in) / 34 L expanded (approx. 2,075 cu in), measured using the ASTM F2153 fill test with 20 mm PP plastic spheres. Includes the main compartment and all zippered pockets; excludes mesh water-bottle pockets and open front stash pockets. Tolerance: ±1.5 L. File the test record with the initial sample approval documents.   3. Suggested Tolerances and Contract Language Capacity range Suggested tolerance Application notes Under 20 L ±1 L Small bags are sensitive to compartment and opening design; test conditions must be controlled. 20–40 L ±1.5–2 L Common range for daypacks and commuter laptop backpacks. Over 40 L / large travel bags ±2–3 L Fill-test variation may be greater for large bags; additional repeats are recommended. Retail products with strict controls ±3%, or agree that “labeled capacity must not exceed measured unexpanded capacity.” Suitable for tightly controlled cross-border retail programs. Note: Tolerance criteria must correspond to the capacity test method. A tolerance established using external dimensions cannot be used to judge results from a fill test.   4. Common Capacity-Related Discrepancies in Custom Backpack Development Type of discrepancy Explanation Control measure Including open pockets in labeled capacity The counting method differs from ASTM and can produce inconsistent figures. Clearly list included and excluded pockets in the specification sheet. Advertising only expanded capacity Does not reflect volume in the product’s normally closed state. Provide both unexpanded and expanded capacity. Using external dimensions directly for sewn backpacks Foam, back panels, and lining take up space, so the calculated value is high. Use fill testing as the basis for labeled capacity; use external dimensions only as a supplementary reference. Using one capacity value for all sizes of a style Pattern and suspension structures change by size, affecting volume. Test each size independently. Testing only the first sample, with no production recheck Pattern adjustments, lining changes, and pocket revisions can change capacity. Test the approved reference sample and production trial units. Mixing metric and imperial units without labels Can lead to misinterpretation of readings. List both L and cu in in technical documents, with the primary unit suited to the target market.   5. Key Points When Comparing Multiple Samples Two products labeled with the same capacity may not perform equally in actual loading. Compare external dimensions, the main compartment’s internal usable dimensions, opening design, and photos of the bag when loaded. Even when both are labeled 30 L, a boxy pack and a tapered pack may accommodate different shapes of items. For travel backpacks and school backpacks, capacity is only one consideration. Flap-top designs are better suited to flat items, while top-loading roll-top bags offer good compression but can make items deep inside the bag harder to access. For a more complete assessment, include capacity, main-compartment internal dimensions, opening type, and fully loaded external dimensions in the specification sheet.   6. When to Conduct Capacity Tests Lock in the capacity baseline during initial sample approval. Once the first sample is complete, test capacity using the agreed method. After the parameters are approved, record them in the technical pack and purchasing documents before starting mass production. During inspection, use the same sphere specifications, measuring equipment, and settling procedure as for the approved sample, and assess the results against the agreed tolerance.   7. Capacity Records and Compliance Documentation Capacity testing is a technical specification activity and is separate from chemical testing of materials. Nevertheless, related records should be archived together for easy reference. If a product is labeled as using recycled fabric, the material claims should align with applicable GRS, GOTS, or OEKO-TEX documentation. Children’s backpacks sold in the United States must also meet applicable CPSIA requirements. A substantial discrepancy between labeled and measured capacity may create a risk of misleading advertising in the US and European markets. Store capacity test records and compliance certificates in the technical pack so they can be retrieved for customer factory audits and marketplace reviews.   Ⅴ. Frequently Asked Questions (FAQ)   Q1: Is backpack capacity accurately measured by multiplying length × width × height and dividing by 1,000? This formula estimates only the theoretical upper limit. It counts fabric, foam, and back-panel structures as volume and therefore generally overestimates usable space in sewn backpacks. The discrepancy is smaller for rectangular tote bags and simple travel duffels. For backpacks, outdoor packs, and styles with multiple compartments, capacity acceptance should be based on the ASTM F2153 fill test. A pattern correction factor can support early sampling estimates, but the result is for internal reference only and must not be used as the official labeled capacity.   Q2: What is ASTM F2153? Are factories required to use it? ASTM F2153 is a voluntary test method for measuring backpack capacity; it is not legally mandatory. The core procedure is to fill all enclosed compartments with 20 mm rigid plastic spheres, transfer the spheres to a calibrated measuring container, and record both unexpanded and expanded capacity. Open water-bottle pockets and open stash pockets are excluded. The buyer and supplier should agree on whether to use the method in the technical documentation; once agreed, it becomes the basis for acceptance.   Q3: Why does a factory label a backpack as 30 L when the fill-test result is only 25 L? This is usually due to differences in measurement methods—for example, using external dimensions or including open pockets in the calculation. A difference of around 20% between a daypack’s labeled capacity and its ASTM fill-test result is not unusual in the industry. Buyers and suppliers can establish a consistent basis for acceptance by agreeing in advance on the test method, pocket-inclusion rules, and tolerance range in the specification sheet.   Q4: How should tolerances be set in a specification sheet, and which units should be used? For bags under 20 L, a tolerance of ±1 L is suggested; for 20–40 L, ±1.5–2 L; and for large bags over 40 L, ±2–3 L. For tightly controlled retail programs, the tolerance can be narrowed to ±3%, or the parties can agree that “the labeled capacity must not exceed the measured unexpanded capacity.” Use cubic inches (cu in) alongside liters for North America, while liters are generally preferred in Europe. Conversion: 1 L ≈ 61.024 cu in.   Q5: How should capacity be tested for small bags under 4 L, waist packs, and organizers? ASTM F2153 generally does not apply to bags under 4 L. A simplified method can use a calibrated measuring cup, uniform dry beans, or a weight-to-volume conversion. The specification sheet must state that the method is “not the ASTM F2153 standard procedure.” Small spheres can stack inconsistently in small compartments, so external capacity claims for small bags should be made cautiously.   Q6: Can rice or beans replace standard plastic spheres? They may be used for rough internal checks, but capacity figures used in contracts, specification sheets, or product labeling should not be based on rice or beans. Grains settle under pressure, and results vary between operators and batches, making repeatability poor. For formal testing, use 20 mm rigid PP/PS spheres and calibrated measuring equipment.   Q7: For a roll-top backpack, how many rolls count as the unexpanded state under ASTM F2153? ASTM F2153 does not mandate a specific number of roll-top folds, which can lead to disagreement for this style. The buyer and supplier should agree in writing in the technical pack on the number of folds used for normal closure (commonly 2–3 rolls in the industry). Fill the bag to the agreed number of rolls and confirm that it closes normally without fabric tension; record this as the unexpanded capacity. The reading with the roll-top fully unrolled is the expanded capacity.   Ⅵ. Conclusion From using geometric estimates to support early pattern planning, to determining labeled capacity through ASTM F2153 fill testing, and then specifying the test method, included compartments, and tolerances in clear technical terms, a verifiable capacity-assessment system is central to bag capacity management. Consistent criteria help project stakeholders avoid misunderstandings about specifications. As a professional bag manufacturer, we can support capacity-related technical requirements and help align project specifications with the agreed standards. Please contact us if you need assistance.   Author        
  • What Features Should a Good Pickleball Bag Have?
    What Features Should a Good Pickleball Bag Have? Oct 20, 2026
    A quality pickleball bag should meet four core standards: a scientifically designed compartment layout, a comfortable carrying system, high-quality craftsmanship, and durable, water-resistant materials. Only when all four elements are combined can a pickleball bag truly be considered a good one. Table of Contents: Scientific Compartment Design Comfortable Carrying System High-Quality Craftsmanship Durable, Water-Resistant Materials Customization Recommendations for Brands Frequently Asked Questions About Pickleball Bag Customization Conclusion   1. Scientific Compartment Design Pickleball paddle faces are primarily made of carbon fiber or fiberglass composite materials, which are susceptible to pressure, scratches, and prolonged exposure to high temperatures and direct sunlight. Therefore, a dedicated paddle compartment is an essential feature of a good pickleball bag. Specifically, an excellent paddle compartment should have the following features: Thickened, Insulated Paddle Compartment: The dedicated paddle compartment should feature a thickened EVA or pearl cotton cushioning layer to absorb impacts when the bag is dropped or squeezed. In addition, an aluminum foil thermal insulation lining can effectively resist high outdoor temperatures and help prevent paddle face deformation caused by prolonged exposure to direct sunlight. Large-Capacity Main Compartment: The main compartment should provide sufficient space to accommodate all the essential gear needed for daily training or competitions, such as clothing, towels, water bottles, and other items. Quick-Access Ball Pocket: Add a dedicated mesh or elastic compartment inside the main compartment for storing pickleballs. The separate, quick-access ball pocket keeps balls physically separated from clothing, helping maintain the cleanliness and organization of the gear. It also allows players to quickly access spare balls during warm-ups or between matches without having to search through the entire main compartment, improving overall efficiency and user experience. Separate, Ventilated Shoe Compartment: Isolated from the main compartment, it prevents wet or dirty shoes from soiling paddles and clothing while helping reduce unpleasant odors. This is a key feature that distinguishes a professional pickleball bag from an ordinary gym bag. Multiple Small Pockets: Designed to store personal items and accessories such as mobile phones, keys, overgrips, protective gear, and towels. Hidden Valuables Pocket: Features a soft, suede-lined interior to safely store valuables that are susceptible to scratches.   2. Comfortable Carrying System Pickleball bags commonly come in three carrying styles: backpacks, shoulder/crossbody bags, and convertible bags that can be carried by hand or worn as backpacks.   Backpack: Ideal for carrying multiple paddles and a full set of gear, its key features lie in the design of the shoulder straps and back panel. The shoulder straps of a high-quality backpack should be wide and thick, filled with high-density foam, and covered with breathable mesh fabric to distribute pressure across the shoulders and promote airflow, preventing excessive heat buildup and pressure marks during extended wear. The back panel should incorporate an EVA or PE pearl cotton support layer to prevent it from deforming or collapsing under heavy loads. It should also conform to the natural curvature of the spine, providing stable and reliable support. Shoulder Bags or Crossbody Bags: These bags prioritize lightweight convenience and flexibility, making them ideal for short training sessions or situations where only a small amount of gear is needed. The shoulder strap should be sufficiently wide to prevent slipping, while the shoulder pad should incorporate a cushioning layer to reduce the strain of carrying weight on one shoulder. An adjustable shoulder strap allows users of different heights to find a comfortable fit. Convertible Tote and Backpack: For users who value versatility, a convertible tote and backpack offers greater flexibility. This type of bag typically features a reinforced top handle for convenient carrying over short distances or placing the bag in a vehicle, as well as a padded side handle designed to reduce pressure on the hand and prevent discomfort when carrying the bag. When converted into backpack mode, the concealed shoulder straps should be easy to pull out and securely fasten, ensuring a seamless carrying experience in both configurations. Regardless of the style chosen, the ultimate goal of the carrying system is to ensure that players feel comfortable and at ease on their way to and from the court.   3. High-Quality Craftsmanship Craftsmanship details directly determine the service life and overall look and feel of a pickleball bag. Stitching: The stitching must be strong and durable, with consistent stitch spacing and neat, even seams. Key stress points, such as shoulder strap attachment points, handle bases, and zipper ends, should be reinforced with double or even triple stitching, combined with bar-tack reinforcement to improve tear resistance and prevent seams from splitting or breaking under prolonged heavy loads. Hardware: The choice of hardware is crucial. Zippers should be smooth, durable, and offer a certain level of water resistance, preferably from reputable brands such as YKK or SBS. Zipper pulls should be designed for easy gripping and operation, even when wearing sports gloves. Buckles: Buckles should undergo fatigue testing to ensure they resist cracking or deformation even after repeated fastening and release. In addition, fabric edges should be finished neatly, with no loose threads, and the bag should maintain a structured, well-defined shape without easily collapsing, even when empty. These details reflect professional quality and attention to detail.   4. Durable, Water-Resistant Materials Pickleball is often played outdoors, where bags may be exposed to sudden rain showers or morning dew on the court. Therefore, the water resistance of the fabric serves as the first line of defense in protecting the gear inside.   4.1 Main Fabric: Nylon vs. Polyester A high-quality pickleball bag should be made from high-density nylon (such as 600D or higher) or polyester fabric. These materials offer excellent abrasion resistance and tear resistance, along with good water-repellent properties. Nylon: When comparing these two common materials, nylon stands out for its higher strength-to-weight ratio and excellent abrasion resistance, making it a preferred choice for premium pickleball bags. It has a smooth surface and a soft feel, but comes at a relatively higher cost. Polyester: Polyester offers better UV resistance and color retention, making it less prone to fading or degradation after prolonged exposure to direct sunlight. It is also more affordable, making it a cost-effective choice.   4.2 Waterproof Coatings A high-quality fabric base alone is not sufficient to withstand harsh weather conditions. The surface waterproofing treatment is the key factor that determines a bag's water-repellent performance.   Most professional pickleball bags on the market today use one of three main treatments: DWR (Durable Water Repellent) coating, PU coating, or TPU coating. DWR Water Repellency: DWR coating creates a lotus-leaf effect on the surface of the bag, causing water droplets to bead up and roll off quickly rather than penetrate the fabric. This effectively prevents rainwater from soaking the gear inside. PU Waterproof Coating: PU coating is typically applied to the inner side of the fabric, forming a dense waterproof membrane. It not only prevents external moisture from penetrating but also enhances the fabric's overall structure and tear resistance. TPU Waterproof Coating: As a thermoplastic polyurethane elastomer, TPU coating is typically laminated onto the inner side of the fabric as a thin film or incorporated as a separate layer. Compared with PU coating, TPU offers superior hydrolysis resistance and low-temperature flexibility. Even in cold and humid environments, it is less prone to degradation, hardening, or cracking, helping maintain the bag's waterproof performance over long-term use.   5. Customization Recommendations for Brands If you are planning to develop a pickleball bag under your own brand, the following recommendations across three key areas can help you strike the right balance between product performance, cost, and target audience.   5.1 Main Fabric Selection Recommendations Fabric determines a pickleball bag's look and feel, durability, and pricing potential. The following table provides fabric selection recommendations based on product positioning. Fabric Option Common Specifications Strength / Abrasion Resistance UV Resistance Cost Recommended Positioning Polyester 600D / 900D ★★★☆ ★★★★☆ (fade-resistant) Moderate Value-oriented models, entry-level models, and products for prolonged outdoor sun exposure Nylon 600D / 1680D ballistic nylon ★★★★★ (strong and lightweight) ★★★ (UV treatment recommended) Medium to high Mid-to-high-end models and bags for professional players Nylon + Ripstop / Jacquard Checkered nylon, honeycomb texture ★★★★★ ★★★ High Premium models and designer brands Composite Mesh Fabric (PVC/EVA) 500D–1000D ★★★★☆ ★★★☆ Moderate Enhanced waterproof models and bags for beach or multi-purpose use Key Selection Considerations: For high-volume sales models, prioritize 600D polyester. It offers manageable costs and good colorfastness, making it a popular choice for mainstream, entry-level products. For mid-to-high-end models, consider 1000D or 1680D ballistic nylon. Its high strength and good water resistance make it suitable for the mid-to-high-end market. Eco-friendly options: Consider recycled nylon, such as ECONYL®, or recycled polyester (RPET), and support internationally recognized certifications such as GRS to meet the growing demand for sustainable products in European and North American markets.   5.2 Capacity Selection Recommendations Bigger is not always better when it comes to capacity. The ideal size should match the target users' playing scenarios and carrying habits. The following table provides capacity design recommendations for OEM pickleball bag development. Capacity Category Paddle Capacity Typical Configuration Target Audience Reference Dimensions (L × W × H) Lightweight Model 1–2 paddles Main compartment + ball pocket + water bottle holder; usually no shoe compartment Casual players and people who combine walking with playing pickleball Approx. 45 × 20 × 25 cm Standard Model (Recommended) 2–4 paddles Padded paddle compartment + main compartment + separate shoe compartment + ball pocket + small-item compartments Core club members and regular doubles players Approx. 50 × 25 × 32 cm Professional Large-Capacity Model 4–6 paddles Padded paddle compartment + large main compartment + separate shoe compartment + ball pocket + waterproof pouch Professional players and coaches Approx. 55 × 30 × 38 cm Travel / Team Model 6 or more paddles Rolling suitcase-style bag or extra-large backpack with external attachment systems Team bulk purchases and players who travel frequently Approx. 60 × 35 × 45 cm Key Selection Considerations: The standard model is the sweet spot. A bag that holds 2–4 paddles can serve a broad range of players. Brands developing a new pickleball bag product line should consider making this capacity their flagship SKU Lightweight models are ideal for customer acquisition or promotional giveaways. Their simple construction and lower cost make them suitable as companion bags for entry-level sets or as commemorative gifts for club events, lowering the barrier to entry for new players. Professional large-capacity models should prioritize storage efficiency rather than simply adding more space. To address the challenge of organizing extensive equipment carried by coaches and professional players, consider removable dividers or modular inner compartments. These features allow users to accommodate different combinations of paddles and clothing while keeping the interior organized. Travel / team models should prioritize travel-friendly features. In addition to extra-large capacity, they should include a standard luggage strap and abrasion-resistant protective feet. These features help secure the pickleball bag to a suitcase during airport transfers and long-distance travel while reducing wear on the bottom of the bag   6. FAQ: Frequently Asked Questions About Pickleball Bag Customization   Q1: What is the difference between a pickleball bag and a tennis bag? Can they be used interchangeably? They can be used interchangeably on a temporary basis, but it is not recommended. Pickleball paddles (approximately 40 cm long) are shorter than tennis rackets, so tennis racket compartments may leave too much empty space, allowing paddles to shift around and collide with other items. Pickleball bags also typically feature dedicated ball pockets, since hard plastic pickleballs can be damaged by excessive pressure, as well as shoe compartments and more small-item storage sections. If you play only pickleball, a dedicated pickleball bag offers a significantly better user experience.   Q2: How can I tell a bag's waterproof rating? Does water repellency mean it is waterproof? No. Water repellency provided by a DWR coating is generally sufficient for light rain and splashes, but zipper areas can still allow water to seep in. For more comprehensive waterproof protection, the bag needs a combination of PU/TPU-coated fabric or laminated waterproof fabric and waterproof zippers, such as those in YKK's waterproof zipper series. When shopping, check whether the product specifications mention both fabric coating and waterproof zippers.   Q3: Why does a pickleball paddle compartment need thermal insulation? Can summer heat really damage a paddle? Yes. Pickleball paddles made with carbon fiber or fiberglass faces and polypropylene honeycomb cores may experience face softening, delamination, or changes in playing feel after prolonged exposure to high temperatures and direct sunlight. An aluminum foil thermal insulation lining can significantly reduce the temperature inside the bag, making it one of the key features that distinguishes a professional pickleball bag from a budget model.   Q4: What is the typical minimum order quantity (MOQ) and lead time for custom pickleball bags? SYNBERRY's standard MOQ is approximately 500 pieces. The sampling lead time depends on the complexity of the design and is typically 2–3 weeks. Mass production lead time varies according to order quantity and manufacturing complexity. Additional time should be allowed for special processes, such as full-surface printing, reflective strips, and custom-molded buckles.   Q5: Should I choose nylon or polyester for a pickleball bag? Which is more durable? Both materials are durable, but each offers different advantages. Nylon provides greater strength and a better hand feel, making it suitable for mid-to-high-end products. Polyester offers better UV resistance, superior color retention, and a lower price, making it ideal for cost-effective models intended for prolonged outdoor sun exposure. Choose nylon if your budget allows; choose polyester if value for money is the priority.   7. Conclusion Pickleball is experiencing explosive growth in global participation, and pickleball bags are evolving from accessory equipment into a specialized product category. For sports bag brands, this represents not only an opportunity to enter an emerging market but also a critical window to establish professional brand recognition through more refined product development. An excellent pickleball bag should be more than a collection of storage compartments. It should reflect a deep understanding of end-user needs and deliver a thoughtful response to their expectations. From thermal insulation technology that protects expensive paddles, to compartment layouts that improve access efficiency, to weather-resistant materials designed for outdoor conditions, every detail demonstrates respect for the player's sporting experience. This article has been written from the perspective of a pickleball bag manufacturer, with the aim of providing brands developing pickleball bag product lines with a comprehensive reference guide, from understanding customer needs to bringing products into production.   Author        
  • What Type of Fabric Is Commonly Used for Cosmetic Bag Lining?
    What Type of Fabric Is Commonly Used for Cosmetic Bag Lining? Oct 15, 2026
    The most commonly used cosmetic bag lining materials are polyester-based fabrics, especially polyester plain weave, polyester taffeta, pongee, and coated polyester. In addition, nylon, TPU, PEVA, PVC, and EVA are frequently used for products with high waterproof and leak-proof requirements; RPET recycled polyester and recycled nylon are suitable for sustainable brand lines; microfiber, faux suede, velvet, and satin are suitable for high-end tactile feel and gift positioning.    Cotton, canvas, cotton-polyester blends, and cotton-linen blends can also be used for cosmetic bag lining, especially for canvas cosmetic bags, natural style, eco-friendly positioning, or products requiring embroidery texture. However, their waterproof, stain-resistant, and easy-clean performance typically differs from coated synthetic fabrics and needs to be evaluated based on specific use scenarios.   Table of Contents: • Selection by Functional Requirements • Key Technical Parameters for Lining Selection • Lining Customization Processes and LOGO Presentation Methods • How Do We Ensure Full-Process Material Quality Control for Brands? • Frequently Asked Questions • Conclusion   Ⅰ. Selection by Functional Requirements and Analysis of Common Fabrics Cosmetic bag lining selection typically revolves around stain resistance and waterproofing, cosmetic protection, easy cleaning, and shape retention and support. The following section categorizes by functional requirements and explains the characteristics, applicable scenarios, and precautions of commonly used fabrics.   1. Waterproof and Easy-to-Clean Category • PVC/TPU Film: Commonly used for functional cosmetic bags and wet-dry separation compartments, with outstanding waterproof and leak-proof performance. Liquids are easy to wipe clean after splashing. PVC offers outstanding waterproof performance and transparency, but its compliance risks under REACH and Prop 65 must be carefully evaluated for European and American markets; TPU performs better overall in eco-friendliness, UV resistance, and flexibility, making it the preferred direction for high-end waterproof styles. • PEVA: Chlorine-free, it is an eco-friendly alternative direction to PVC, offering good waterproof performance and easy-wipe characteristics, suitable for brands with sustainability requirements. Long-term UV exposure may cause slight yellowing, which needs to be evaluated during the sampling stage. • EVA: Commonly used for rigid inner trays or molded linings, with good waterproof performance and structural support, suitable for cosmetic bag inner cores that require shape retention. • Coated Polyester and Coated Oxford Cloth (e.g., PU coating, TPU coating): After adding a coating to polyester or Oxford cloth, a continuous film forms on the lining surface, effectively blocking liquid splashes such as liquid foundation and skincare water from penetrating. Wear-resistant and tear-resistant, with good cost-effectiveness, suitable for affordable large-capacity cosmetic bags and daily functional styles. Note that coatings and stitching are not absolutely leak-proof. • Polyester Plain Weave, Pongee, Polyester Taffeta: Stable supply, high cutting and sewing efficiency, and stable color fastness, ensuring lining color consistency across different batches in bulk orders. Among them, polyester taffeta is lightweight and high-density, smooth and snag-resistant, with light weight; pongee and plain weave are suitable for mass-market styles. For basic waterproof requirements, light-coated versions can be selected. • Nylon Taffeta: Smooth hand feel, tear strength superior to polyester of the same specification, suitable for mid-to-high-end cosmetic bag products. Nylon itself has certain waterproof properties and is commonly used for waterproof and easy-to-clean linings. If the product emphasizes lightweight, durability, and travel scenarios, nylon is a selection direction worth considering. [Additional Note] Coated fabrics can only resist splashes. Ordinary sewing creates needle holes, and liquids may still seep through the stitching. If complete leak-proofing is required, an additional seam-sealing heat-sealing process is needed.   2. Shape Retention and Cushioning Category • Felt: High stiffness, strong support, helps the cosmetic bag maintain a three-dimensional silhouette, and provides certain cushioning and shock-absorbing effects, suitable for custom inner bags and products that need to protect powder compacts and eyeshadow palettes. Attention should be paid to weight, cleaning methods, and thickness. • Fleece Category (e.g., microfiber fleece, faux suede, velvet): Delicate touch, with slight damping feel, can reduce cosmetic bottle sliding and scratching, suitable for mid-to-high-end cosmetic bags. Microfiber, faux suede, and velvet offer premium tactile feel and anti-slip properties, mostly used for high-end brand matching. 3. High-End Texture Category • Acetate Satin: Smooth and soft touch, warm luster, good drape and wrinkle resistance, smooth for taking out and putting in cosmetics, will not snag makeup brush bristles, suitable for light luxury positioning. • Ordinary Satin/Sateen: Smooth surface, skin-friendly, with soft luster, can enhance refinement, suitable for gifts and products that value visual design. Need to evaluate snagging, abrasion resistance, and color fastness. Polyester satin and nylon satin have excellent printing effects, suitable for high-end linings. 4. Eco-Friendly Recycled and Sustainable Category • RPET: Made from recycled PET bottles through crushing, cleaning, and spinning into yarn. Its hand feel, color fastness, and abrasion resistance are minimally different from virgin polyester, and it can seamlessly replace traditional polyester plain weave or taffeta, suitable for most conventional cosmetic bag linings. It is a commonly used material for brands practicing ESG concepts. • Recycled Nylon: Mainly derived from discarded fishing nets, carpet fibers, and other industrial waste, regenerated through depolymerization and polymerization. Compared with RPET, recycled nylon performs better in strength, elasticity, and chemical resistance, with a more delicate and smooth touch, but market supply is less stable than RPET, and cost is usually higher than RPET. 5. Natural Style and Blended Category • Cotton: Natural hand feel, skin-friendly, moisture-absorbing, suitable for natural style, eco-friendly positioning, and canvas cosmetic bag linings. • Canvas: Higher gram weight, good structural support, wear-resistant, suitable for canvas cosmetic bags, toiletry bags, travel storage bag linings or outer pockets. When used as lining, weight, thickness, and sewing processes need to be comprehensively considered. All-cotton canvas has good breathability and is lightweight, suitable for powder products and makeup brushes and other items that need ventilation. Ordinary cotton and canvas are not waterproof, easily absorb color and stains. If directly exposed to liquid cosmetics, cleaning is difficult. A common approach is to combine with removable washable inner bags, coating finishing, independent waterproof bags, or internal compartment structures.   • Cotton-Polyester Blend: Balances the natural hand feel of cotton with the durability and dimensional stability of polyester, suitable for projects that need to balance texture and bulk production consistency. • Cotton-Linen Blend: Prominent natural texture, suitable for specific style brands, but stain resistance and color fastness need to be confirmed during the sampling stage. 6. Other Practical Categories • PU Lining: Textured, easy to wipe, suitable for daily commuting and mid-range positioning products. Its surface is dense, effectively blocking oil-based stains such as liquid foundation and lipstick from penetrating. A damp cloth can easily wipe it clean, with low maintenance cost. Note to choose PU materials with good hydrolysis resistance to avoid coating peeling or stickiness after long-term use, especially in high-temperature and high-humidity environments where aging tests are required. • Mesh/Three-Layer Mesh: Excellent breathability, light weight, commonly used for internal compartment bags or brush storage layers of cosmetic bags, facilitating quick identification of items and accelerating internal moisture dissipation, reducing mold growth risk. However, due to its uneven surface and large pores, it easily traps dirt and is difficult to thoroughly clean. It is not recommended as the main lining directly contacting liquid cosmetics, and usually needs to be used with a waterproof inner bag. Ⅱ. Key Technical Parameters for Lining Selection When selecting lining fabrics for cosmetic bags, the following parameters directly affect final product quality and user experience. It is recommended to confirm each item during the sampling stage.   1. Gram Weight and Thickness • Low Gram Weight (e.g., 30-50gsm polyester taffeta or pongee): Lightweight and soft, maximizes internal space saving, reduces overall weight, suitable for travel cosmetic bags pursuing ultimate portability and lightweight. • Medium Gram Weight (e.g., 60-100gsm plain weave polyester, nylon, or cotton): Balances hand feel and durability, the mainstream choice for most conventional cosmetic bags. Fabrics in this range have moderate stiffness, can maintain the basic silhouette of the bag, while providing good sewing stability and abrasion resistance, suitable for daily commuting and multi-functional storage scenarios. • High Gram Weight (e.g., 120gsm+ thick canvas, thickened coated fabric, or composite felt): Excellent stiffness and structural support, effectively maintaining the three-dimensional shape of the cosmetic bag, preventing deformation from internal item compression, commonly used for hard-case cosmetic bags or inner designs that need to stand independently.   2. Coating Type and Waterproof Performance Coating Type Waterproof Performance Abrasion Resistance Eco-Friendliness Typical Application PU Coating Good Good Medium Daily cosmetic bags TPU Composite Excellent Excellent Excellent High-end waterproof styles PEVA Good Medium Good Eco-friendly positioning styles PVC Excellent Good Compliance requires careful assessment Transparent styles EVA Good Good  Medium Molded inner trays, rigid linings   3. Color Fastness, Rubbing Resistance, and Color Selection • Linings need to pass dry rubbing and wet rubbing color fastness tests, meeting order target market and brand requirements (refer to ASTM/ISO industry testing standards). • Color selection needs to combine brand vision, target market usage habits, cleaning and maintenance expectations, and overall design. • Dark or medium color systems are generally less likely to show stains in daily use; light color systems look fresh and suit some brand tones, but may show cosmetic residue more easily, so coating, easy-clean finishing, or removable washable inner bags can be combined.   4. Breaking Strength and Tear Strength • Lining fabric breaking strength and tear strength need to comply with industry general testing standards, such as ASTM D5034. • Specific indicators need to match product positioning, usage scenarios, and brand quality requirements.   5. Hand Feel, Noise, Folding Resilience, and Sewing Compatibility • Nylon and coated fabrics may generate friction noise, which needs to be evaluated during the sampling stage. • Microfiber, faux suede, canvas, and other materials need attention to the impact of thickness on sewing efficiency and finished product weight. • Coated and film materials need attention to whether they whiten after folding, whether resilience is stable, and whether stitching leaks.   6. Cleaning Methods and Consumer Usage Scenarios • If the product is oriented toward daily office, travel, fitness, and other scenarios, the lining should prioritize easy-wipe and leak-proof performance. • If the product emphasizes natural style or removable washable design, cotton, canvas, and cotton-polyester blends can be considered, combined with removable inner bags or waterproof storage bags. • If the product is positioned as gifts or high-end brands, satin, microfiber, and faux suede can be considered, and maintenance methods should be clearly stated in the instructions.   Ⅲ. Lining Customization Processes and LOGO Presentation Methods 1. Lining Customization Dimensions • Color Customization: Dyeing according to Pantone color numbers. First orders need to reserve a color confirmation cycle. • Texture Customization: Plain weave, twill, jacquard, satin, pearlescent, and other surface effects. • Print Customization: Full-print brand patterns, LOGO repeat printing, seasonal graphics, etc. • Structure Customization: Brush pockets, transparent inner bags, zippered hidden pockets, elastic band fixing positions, etc. • Material Composite: Coating, lamination, bonding, embossing, and other processes can be combined according to waterproof and hand feel requirements.   2. LOGO Process Selection Process Applicable Lining Types Durability Process Characteristics Silk Screen Printing Polyester, nylon, canvas, and other fabrics Medium Direct color expression Heat Transfer Printing Polyester, nylon, canvas, and other fabrics Good Good pattern detail expression Embroidery Polyester, nylon, canvas, and other fabrics Excellent Strong three-dimensional effect Woven Label All types Excellent Low cost Metal Label All types Excellent High-end feel Hot Stamping/Foil Stamping Satin, faux suede, PU leather Medium High-end feel   3. Added Value of Branded Linings • Custom printed linings or brand woven labels can enhance product unboxing experience and brand recognition. • For DTC brands and gift channels, branded linings are an important means to enhance perceived value. • Lining customization does not affect the flexibility of outer bag design, and can form an overall brand solution with outer bag fabric, zippers, and packaging.   Ⅳ. How Do We Ensure Full-Process Material Quality Control for Brands? 1. Communication Before Cosmetic Bag OEM: • Requirement Confirmation: Understand customer product positioning and target market. • Fabric Selection: Confirm lining material, gram weight, coating, and color.   2. Sampling Stage • Sampling: Produce samples, confirm hand feel, color, and structure. (It is recommended to complete at least one round of physical sample confirmation before formal order placement.) • Sample Confirmation: During the sampling stage, simultaneously confirm lining color, hand feel, thickness, coating, LOGO process, sewing effect, and cleaning performance. • Compliance Requirements: If the product is oriented toward European and American markets, target market compliance documents and testing arrangements can be confirmed simultaneously during the sampling stage.   3. Key Quality Control Checkpoints • Incoming Material Inspection: Verify fabric color difference, gram weight, and width. • Cutting Stage: Check fabric surface defects and coating uniformity. • Sewing Stage: Check whether the lining and zipper junction is flat and whether there are skipped stitches. • Finished Product Stage: Conduct lining cleaning tests and zipper smoothness tests. • Outgoing Inspection: Execute appearance and function inspection according to SYNBERRY AQL 1.5/4.0 sampling standards.   4. Lining Cleaning Test Method Reference • In actual product development, real cosmetics can be used for lining cleaning comparison tests, rather than only testing with water. • Candidate lining samples can be respectively exposed to liquid foundation, lipstick, sunscreen, and other cosmetics, then treated with the same cleaning method and wiping frequency, comparing residue conditions. • This method can effectively screen the practical performance of lining solutions during the sampling stage.   Ⅴ. Frequently Asked Questions (FAQ) Q1: What is the most common choice for cosmetic bag lining? Can cotton and canvas be used? A: Polyester plain weave, polyester taffeta, pongee, and coated polyester are widely used cosmetic bag lining materials, especially suitable for mass-market and conventional functional styles. Cotton, canvas, cotton-polyester blends, and cotton-linen blends can also be used for cosmetic bag lining, especially suitable for canvas cosmetic bags, natural style, eco-friendly positioning, or products requiring embroidery texture. However, cotton and canvas are usually not waterproof and easily absorb stains and color. It is recommended to combine with removable washable inner bags, coating finishing, or independent waterproof bag designs. If emphasizing waterproof and leak-proof, TPU, PEVA, PVC, and EVA are more common; if emphasizing sustainability, RPET recycled polyester and recycled nylon are growing options.   Q2: How long does lining fabric sampling take? A: Conventional polyester or nylon lining sampling is relatively fast, generally 15-20 days. Coated fabrics or custom printed linings require more time. If custom dyeing or Pantone color matching is involved, an additional color confirmation cycle needs to be reserved. It is recommended to complete at least one round of physical sample confirmation before formal order placement. Specific sampling schedules need to be confirmed with the factory.   Q3: How to choose between PVC lining and PEVA lining in European and American markets? A: PVC lining has the strongest waterproof performance and high transparency, but due to chlorine and phthalate issues, it faces high compliance risks under EU REACH and California Prop 65. PEVA is chlorine-free and is a more eco-friendly alternative, suitable for brands with sustainability requirements.   Q4: How are MOQ and lead time for custom printed linings determined? A: The MOQ for custom printed linings is usually negotiated based on pattern complexity, printing method, and fabric customization degree. Silk screen printing is suitable for larger batches, while digital printing can support small batches but with higher unit costs. In terms of lead time, the production cycle for printed linings is usually longer than plain color linings. Conventional printing MOQ starts at 500 pieces. Specific MOQ and lead time are subject to factory evaluation.   Q5: How to judge the quality of lining fabric? A: Factories usually evaluate from the following dimensions: whether gram weight meets specification requirements, whether coating is uniform without peeling, whether color fastness passes industry general tests, whether breaking strength meets standards, and whether wrinkling or thread breakage occurs after sewing. During the sampling stage, real cosmetics can be used for cleaning comparison tests, rather than judging only by visual inspection. During mass production, systematic control can be carried out through incoming material inspection, cutting inspection, sewing inspection, and outgoing sampling inspection.   Q6: Can cosmetic bag lining achieve both waterproofing and custom LOGO? A: Yes. Common solutions include: heat transfer printing LOGO on coated polyester lining, silk screen printing brand logo on TPU fabric, adding woven labels or printed labels on the lining. Note that some coating surfaces may affect ink adhesion. It is recommended to test the adhesion firmness of the LOGO process during the sampling stage.   Q7: Will lining fabric fade and contaminate cosmetics? A: This risk exists, so lining fabrics must complete dry rubbing and wet rubbing color fastness tests, meeting target market standards. Dark fabrics especially need key verification of wet rubbing indicators. During sampling, color fading tests can be conducted simultaneously to avoid after-sales issues of lining dyeing contaminating cosmetics in finished products.   Ⅵ. Conclusion As a professional bag OEM/ODM manufacturing factory, we provide brands and buyers with one-stop services from lining fabric selection, sampling confirmation, LOGO process customization to bulk production and outgoing quality control. Whether you need basic styles for mass markets, functional styles with waterproof and leak-proof features, high-end styles focusing on tactile feel, or sustainable brand lines, we can match suitable lining solutions and supply chain resources according to your target market and product positioning. To obtain lining fabric samples or discuss specific project requirements, please feel free to contact our business team.     Author        
  • Is neoprene a good material for making bags?
    Is neoprene a good material for making bags? Oct 14, 2026
    Yes, it's perfect choice for some categories of bags but not all type. Neoprene (scientific name: chloroprene rubber, CR) is a material that is highly suitable for specific types of bags. It is soft, water-resistant, highly shock-absorbent, and offers excellent formability. It is particularly suitable for beach bags, diving equipment bags, camera insert bags, gym bags, lunch bags, and various types of trendy soft bags.  If your product requires any two of the following features — “softness + water resistance + protection + foldability” — neoprene is almost an ideal choice. However, if you are designing a structured business briefcase, a high-end handbag that aims for a leather-like texture, or a mass-produced product where cost sensitivity is extremely high, neoprene may not be the optimal solution. Whether it is “good” depends on your product positioning, target usage scenarios, and cost structure. In the following sections, we will start from the fundamental properties of the material and go through the production considerations step by step to help you determine whether it is suitable for your product. Table of Contents: What is Neoprene? Advantages of Neoprene Disadvantages of Neoprene What types of bags are suitable for using Neoprene? Practical Recommendations for Neoprene Bag Customization Frequently Asked Questions Conclusion   1. What is Neoprene? Neoprene (Chloroprene Rubber, abbreviated as CR) was invented by the American company DuPont in the 1930s. It was originally developed for wetsuits, which is why many people’s first impression of it comes from the term “diving material.” Its scientific name is polychloroprene rubber, a type of synthetic rubber produced through the polymerization of chloroprene monomers. In the bag manufacturing industry, the material we actually use is usually not pure rubber sheets, but neoprene foam composite material — a layered material made by bonding a neoprene foam layer with nylon fabric or polyester fabric. A common structure consists of: an outer layer made of nylon/polyester fabric, a middle layer of neoprene foam sponge, and an optional inner layer of lining fabric. The foaming ratio (such as thicknesses of 2mm, 3mm, and 5mm, with softness and firmness differentiated by Shore hardness and density) determines the final product’s structure, stiffness, and cushioning performance. Once you understand its “sandwich structure,” you can understand all the advantages and disadvantages of neoprene as a bag material. This is the logical starting point for all the evaluations and decisions that follow.   2. Advantages of Neoprene   2.1 Excellent Water and Moisture Resistance Neoprene itself has a closed-cell foam structure, with an extremely low water absorption rate that allows very little water vapor to penetrate. This characteristic makes it naturally suitable for the following applications: Beach bags / Swimming bags: Wet swimsuits and wet towels can be placed directly inside without water seeping through to the outer layer and wetting other belongings. It is also less prone to mold growth. Lunch bags / Insulated bags: The closed-cell structure itself acts as an insulating layer. When combined with an aluminum foil lining, it can keep contents cool for several hours, making neoprene a mainstream material in the lunch bag market in Europe and North America. Outdoor and Water Sports Bags: Suitable for paddleboard bags, canyoning bags, and sailing equipment bags.   2.2 Natural Cushioning and Protective Properties The foam layer acts like a built-in shock absorber. This is the core advantage that distinguishes neoprene from almost all traditional bag fabrics: Camera Bags / Drone Bags / Instrument Bags: A 3mm–5mm neoprene layer can provide drop and shock protection for precision equipment, eliminating the need for additional pearl cotton or EVA foam lining. Laptop Sleeves: This is one of the most well-established markets for neoprene applications. The material is lightweight and flexible, yet capable of absorbing impact when dropped. Wine Bottle Bags: Single-bottle and double-bottle neoprene wine bags are common product categories in the gift market. To achieve the same level of protection, traditional fabrics require additional padding and cushioning, which comes at the expense of softness and lightweight performance.   2.3 Softness and Foldability Neoprene bags can be folded and stored away when not in use, making them easy to tuck into a drawer or another bag. Once filled, they can also conform to the contours of the body. This makes them particularly suitable for: Gym Bags / Yoga Bags: The soft bag body can be easily tucked into a gym locker. Travel Organizer Bags: They can be folded and stored in a suitcase, yet offer considerable capacity when unfolded. Diaper Bags / Baby Bags: The soft bag body will not press uncomfortably against the baby and is also easier to fit into a stroller's storage basket. In comparison, canvas and leather bags often face a trade-off: “if they are soft, they lack structure; if they are rigid, they become bulky and heavy.” Neoprene achieves a better balance between “softness” and “shape retention.”   2.4 Excellent Printing and Design Versatility The nylon/polyester fabric bonded to the surface of neoprene is an excellent printing medium. Digital printing, screen printing, and heat transfer printing all deliver very good results, with vibrant colors and sharp details. Moreover, the printed patterns are less likely to crack when the material is stretched. In addition, the bag body can be designed with wavy edges, contrasting-color zippers, color-blocked panels, and other distinctive features. In recent years, neoprene has become a popular choice for trendy fashion brands, IP collaboration collections, and customized corporate gift bags. The rising popularity of designer brands such as Jacquemus has also helped bring soft, sculptural-style neoprene fashion bags into the spotlight.   2.5 Easy to Maintain and Stain-Resistant The neoprene foam layer provides a barrier against liquid penetration. When laminated with a lightly water-resistant, easy-to-wipe outer fabric, such as high-density waterproof nylon or polyester fabric, everyday stains (such as coffee spills, mud splashes, and sweat marks) are unlikely to penetrate the interior. In most cases, the surface can be restored to a clean condition simply by gently wiping it with a damp cloth and a small amount of mild, neutral detergent. There is no need for frequent washing as with canvas, and the hassle of regular maintenance associated with leather can also be avoided.   3. Disadvantages of Neoprene Neoprene is a material designed for specific applications rather than a universal bag fabric. When it solves a practical problem, it can perform very well. However, if you choose it simply because a sample feels soft and premium to the touch, we would typically review the complete product specifications carefully before proceeding to the sampling stage. A rational evaluation of a material cannot focus solely on its advantages. The disadvantages of neoprene are also determined by its structure:   3.1 Finished Bags May Be Heavier Than Expected A small piece of neoprene may not feel particularly heavy. However, once the large surface area of the sandwich structure is combined with zippers, webbing, and hardware, the overall weight can increase significantly. Taking commonly used 3mm-thick neoprene laminated fabric as an example, its weight per square meter is considerably higher than that of ordinary 210D nylon or 600D Oxford fabric. This becomes particularly important when the product is intended to be lightweight or designed for extended periods of carrying.   3.2 Limited Breathability Because the core layer of neoprene consists of a closed-cell foam structure, its dense physical properties not only prevent moisture from penetrating but also effectively block air circulation. This means that neoprene bags have virtually no breathability. When air circulation is the primary consideration, we generally do not choose neoprene as the material.   3.3 Sewing Requires Specialized Expertise Due to the unique elasticity of foam materials, neoprene can be prone to fabric feeding issues, skipped stitches, and wrinkling during sewing. It requires careful control of stitch length, needle type, and fabric feeding methods. Thick materials are also prone to seam splitting at corners, so experienced sewing operators are essential. If a small factory has no prior experience sewing foam materials, the initial defect rate may be relatively high. In addition, ultrasonic seamless welding cannot completely replace stitching to achieve waterproofing with neoprene. High-frequency welding is an option, but it requires substantial investment in equipment. Most products still need to be paired with water-resistant zippers to achieve a level of water resistance beyond basic splash protection.   3.4 Prone to Creasing and Compression Marks During long-term folded storage or transportation, the neoprene foam layer is prone to developing compression marks along fold lines, affecting the smoothness and overall appearance of the product. After receiving a folded or compressed product, users typically need to leave it undisturbed and allow the material to recover naturally before it gradually returns to its original shape. For products designed for “ready-to-use” convenience or positioned as premium gifts, additional support structures should be incorporated into the packaging design to prevent excessive compression.   3.5 Higher Cost Than Conventional Fabrics The price of conventional 3mm neoprene laminated polyester fabric is approximately 3–5 times that of ordinary 600D Oxford fabric. In addition, cutting waste is higher (the elasticity of foam materials makes fabric layout less compact than with plain-woven fabrics), and sewing efficiency is lower. As a result, the overall cost is significantly higher than that of polyester- or nylon-based products. This makes neoprene unsuitable for low-priced, high-volume products, but more appropriate for functional or design-oriented products with medium-to-high profit margins.   4. What Types of Bags Are Suitable for Neoprene? By weighing the advantages and disadvantages discussed in the previous two sections, we can establish a clear decision-making framework. Recommended product categories: Camera / Drone / Instrument Sleeves and Organizer Bags: Ideal when cushioning and protection are the primary requirements. Laptop Sleeves: An established product category with a well-defined competitive landscape.  Lunch Bags / Insulated Bags: Ideal for products that require both thermal insulation and leak protection. Wine Bottle Bags / Cup Sleeves: Suitable for products that combine protective functionality with gift appeal. Beach Bags / Swimming Bags / Water Sports Bags: Ideal for applications where water resistance is the primary requirement. Sports Waist Bags: Suitable for products that prioritize softness and ease of cleaning.  Diaper Bags / Cosmetic Bags: Suitable for products that require softness, stain resistance, and water resistance. Not Recommended Product Categories: Briefcases and Structured Commuter Bags High-End Handbags Requiring a Premium Leather-Like Texture Low- to Mid-Range Mass-Produced Bags: The cost structure is not viable. Short-Term Products with Strong Seasonality   5. Practical Recommendations for Neoprene Bag Customization For brands and backpack factories, selecting the material is only the first step. There are five key factors to control during implementation:   5.1 Thickness and Hardness The standard thickness of neoprene used for bags is typically 2mm–5mm. A thickness of 2–3mm is sufficient for inner sleeves. For tote bags that need to stand upright, 4–5mm is recommended, or a lining can be added through lamination. During sampling, be sure to test the material's recovery after folding and the degree of sagging under load. This ensures that the thickness matches your expectations for the bag's structure and shape retention.   5.2 Lamination Quality The lamination quality of the three-layer material structure (outer fabric + foam layer + lining fabric) determines the product's service life. Poor-quality lamination may begin to delaminate or form bubbles after just a few months of use, whereas high-quality laminated layers should be firmly bonded together and difficult to separate by hand. Therefore, choosing a professional bag factory with experience manufacturing similar products is essential.   5.3 Odor Control During the foaming and lamination processes, neoprene may inevitably retain a certain amount of chemical odor, commonly referred to as a “rubber smell” or “glue smell.” Although materials that meet environmental standards will gradually lose their odor after ventilation, unpleasant smells when opening the package can easily lead to negative reviews, especially among odor-sensitive users, such as parents purchasing products for babies and recipients of high-end gifts. Therefore, during the Neoprene Bag OEM process, we pay particular attention to the following factors: Material Source Lamination Process Packaging Conditions Ventilation Time Before Shipment   5.4 Zipper Selection Determines the Level of Water Resistance Ordinary nylon zippers are one of the main points where water can seep into splash-resistant products. For products with higher water-resistance requirements, waterproof or watertight zippers (such as YKK's waterproof zipper series) must be used, or a waterproof zipper flap should be added to the inside of the zipper. It is important to note that waterproof zippers generally feel stiffer than ordinary zippers, offer greater resistance when opening and closing, and cost more. If the product is not intended for professional diving or extreme outdoor environments, there is no need to blindly pursue the highest level of waterproof zipper performance. Doing so may compromise the user experience while unnecessarily increasing costs.   5.5 Rust Resistance of Metal Hardware Considering that neoprene bags are often used in humid environments, the metal hardware must have excellent rust resistance. In practice, salt spray testing can be used to evaluate the corrosion resistance of the hardware. Priority should be given to zinc alloy hardware with a thick electroplated coating or stainless steel hardware. This helps prevent rapid oxidation and rusting caused by exposure to coastal environments or perspiration, which could otherwise compromise the overall appearance and perceived quality of the product.    6. Frequently Asked Questions   Q1: What Is the Difference Between Neoprene and SBR? CR (chloroprene rubber / neoprene) and SBR (styrene-butadiene rubber) are both synthetic rubbers, and both can be made into a “sandwich” structure consisting of outer fabric + foam layer + lining fabric. Their appearance, feel, and thickness can even be made virtually identical. However, based on practical experience in neoprene bag OEM manufacturing, there are two notable differences between the two materials: Resilience and Shape Recovery: CR offers better resilience and recovers more quickly from compression marks after folding, making it less prone to deformation during long-term use. SBR, by contrast, has relatively weaker resilience and is more likely to develop permanent creases or collapse after repeated folding or heavy compression. Durability and Weather Resistance: CR offers better durability and weather resistance, with significantly greater resistance to UV radiation, ozone, and seawater corrosion than SBR. When exposed to sunlight or humid environments for extended periods, SBR is more susceptible to aging, hardening, and surface powdering. The following table compares the inherent performance characteristics and costs of the two materials: The following table compares their inherent performance characteristics and costs: Comparison Factor CR (Genuine Neoprene) SBR (Styrene-Butadiene Rubber) Abrasion Resistance Good, but not as good as SBR Excellent; commonly used in bags requiring higher abrasion resistance Temperature Resistance Approximately -40°C to +120°C Approximately -20°C to +80°C Durability Excellent; less prone to powdering during long-term use Average; prone to cracking and powdering outdoors Elasticity and Feel Flexible with good resilience Relatively weaker resilience than CR Cost High; CR costs approximately twice as much as SBR Lower; the predominant material used in many “diving fabric” products on the market Odor Relatively mild Usually more noticeable Summary: SBR is a “budget-friendly substitute for neoprene.” If your product's selling points are softness, cushioning, water resistance, and stain resistance (such as beach bags, camera bags, and lunch bags), SBR is generally a cost-effective choice. However, if you intend to promote “genuine neoprene quality,” position the product at a premium price point, or meet higher customer requirements for temperature resistance, crease recovery, and weather resistance, CR may be the better option. The cost difference should also be factored into your pricing strategy.   Q2: Can Neoprene Bags Be Machine-Washed? Machine washing is not recommended. Although neoprene itself can withstand washing, the bonding layers (adhesive) and stitching in the “sandwich structure” cannot withstand the vigorous agitation and high centrifugal forces of a washing machine's spin cycle. Machine washing can easily cause fabric delamination, bubbling, and even irreversible deformation or damage to the hardware. The correct cleaning method is to use lukewarm water and a neutral detergent, gently wiping the stained areas with a soft cloth or sponge. Then wipe away any remaining detergent with clean water and allow the bag to air-dry naturally in a cool, well-ventilated area. Avoid direct sunlight and high-temperature tumble drying, as heat can accelerate rubber aging, causing it to harden or even crack. For persistent odors or deep cleaning, consider seeking assistance from a professional dry cleaner. However, inform them of the material's properties in advance to ensure that strong solvents are avoided.   Q3: Can Neoprene Bags Be Customized into Different Shapes? Yes, but the possibilities are limited by the material's properties. Neoprene has a certain degree of flexibility and can be formed into simple textured patterns through mold-based heat pressing. However, unlike EVA or injection-molded plastics, it cannot easily achieve complex geometric structures or sharp right angles. If a highly structured, rigid appearance is required, internal reinforcement (such as PP boards or EVA sheets) or a thicker foam layer (over 5mm) is usually needed. For designs that aim to achieve a “soft sculptural effect,” we recommend discussing the construction with the factory during the design stage and using multi-panel construction and structural segmentation to create the desired shape, rather than relying on the natural structural support of a single material.   Q4: Are Neoprene Bags Heavy? Neoprene bags may be heavier than buyers expect, especially when large areas of neoprene fabric are combined with lining, webbing, zippers, and metal hardware. They can be considerably heavier than ordinary polyester and nylon bags.   Q5: Are Neoprene Bags Environmentally Friendly? This question needs to be addressed from several perspectives. In terms of the materials themselves, both chloroprene rubber (CR) and styrene-butadiene rubber (SBR) are synthetic rubbers that are difficult to biodegrade naturally and are not considered biodegradable materials. However, their environmental performance during actual production and use depends on the specific manufacturing processes and standards employed. The first consideration is the adhesive and lamination process. Traditional solvent-based adhesives may contain volatile organic compounds (VOCs), which not only produce strong odors but are also environmentally unfriendly. Today, many mid- to high-end supply chains have shifted to water-based adhesives or hot-melt adhesive lamination processes, significantly reducing harmful residual substances and helping products meet major environmental regulations such as the EU's REACH and RoHS requirements.   Q6: Is Neoprene Better Than Nylon or Polyester for Making Bags? Not necessarily. If you prioritize extremely low weight, low cost, and high breathability, choose nylon or polyester. If you need water resistance, cushioning, a soft feel, or a distinctive fashion aesthetic, and can accept higher costs and product weight, neoprene may be the better choice. Many high-end brands even adopt a “hybrid strategy,” using neoprene for the main body and incorporating polyester or nylon panels in key areas to combine the advantages of both materials.   7. Conclusion There is no absolute distinction between good and bad materials; what matters is whether the material is the right fit for the application. For bag manufacturers and brands, the best practice is to work backward from the “application scenario–function–material” framework during the product development stage. Use neoprene where it performs best, and address its limitations through manufacturing processes and quality inspections. When applied correctly, neoprene can become a valuable asset in your product line, offering significant potential for both product differentiation and profit margins. SYNBERRY BAG has over 30 years of experience in bag OEM/ODM manufacturing and specializes in advanced material processing and precision manufacturing across a wide range of materials. We understand the specific requirements of neoprene in lamination, sewing, and quality control, and provide professional support throughout the entire process, from material selection to finished product delivery. Whether you are developing functional protective sleeves that prioritize maximum cushioning or designer handbags that showcase contemporary fashion aesthetics, SYNBERRY BAG can help brands translate creative concepts into finished products with precision, balancing performance, cost, and aesthetics to create high-quality products that stand the test of the market.   Author        
  • Custom Cosmetic Bag FAQ
    Custom Cosmetic Bag FAQ Oct 10, 2026
    Planning to customize cosmetic bags but not sure where to start? This article draws on extensive OEM cosmetic bag manufacturing experience from a factory perspective to address frequently asked questions about key aspects such as materials, dimensions, printing techniques, compliance and quality inspection, and minimum order quantities (MOQs). It will help you communicate more efficiently with your supply chain partners and complete your product customization with ease.   Q1: What materials are commonly used for cosmetic bags? What are their advantages and disadvantages? Material Advantages Disadvantages Suitable Applications Nylon (210D/420D) Lightweight and abrasion-resistant Ordinary texture and appearance Promotional giveaways, travel-size product kits Polyester / Oxford Fabric Vibrant colors and easy printing Ordinary texture and appearance Brands targeting younger consumers PU Leather Premium appearance and texture, water-resistant Higher cost Mid- to high-end brands PVC/EVA Fully transparent, waterproof, and easy to clean Less environmentally friendly Airport-compliant transparent bags, storage bags Canvas / Cotton-Linen Fabric Eco-friendly and suitable for printing complex patterns Not waterproof and prone to staining Eco-friendly brands, gift items Mesh Fabric Combinations Breathable and lightweight Limited load-bearing capacity Toiletry bags, sports-related applications Q2: Do makeup bag Fabrics Need to Be Waterproof? We recommend applying at least a water-repellent treatment. Liquid spills from cosmetics are among the most common accidents during use, and fabrics with a water-repellent coating can effectively protect the items inside the bag.   Q3: What Is the Best Material for Cosmetic Bag Linings? Common options include 210D polyester lining fabric or easy-to-clean PVC/PU-coated fabric. If the product is designed to be “leakproof,” we recommend using a TPU waterproof lining throughout the bag, combined with needle-free stitching or high-frequency heat-sealing technology.   Q4: What Are the Common Sizes of Cosmetic Bags? Mini Size: 15 × 10 × 5 cm, suitable for lipstick bags or touch-up makeup pouches. Standard Size: 20 × 12 × 8 cm, suitable for storing everyday skincare products (the most popular size). Large-Capacity Size: 25 × 15 × 10 cm, suitable for carrying a complete set of travel essentials. Foldable / Hanging Style: Can be unfolded and hung in the bathroom, making it ideal for travel. Q5: Can Cosmetic Bag Dimensions Be Customized? Yes. We support sample making based on physical samples or technical drawings provided by customers. Recommendation: For your first order, confirm the capacity and proportions through sample approval before mass production to avoid dimensional deviations in bulk orders.   Q6: What Details Are Often Overlooked When Specifying Cosmetic Bag Dimensions? Thickness (gusset width). Many customers specify only the length and width, resulting in bulk-produced bags that are too flat to accommodate bottles and jars. Since typical bottles and jars have diameters of approximately 5–7 cm, we recommend a gusset width of at least 5 cm.   Q7: What Logo Application Techniques Are Available for Cosmetic Bags? Technique Features Suitable Materials Screen Printing (Silkscreen Printing) Ideal for simple logos, vibrant colors, and low unit costs Polyester, nylon, canvas Heat Transfer Printing Supports gradient colors and photo-quality graphics Polyester, nylon, canvas Embroidery Premium texture and excellent durability Polyester, nylon, canvas PU Embossing / Foil Stamping Creates a high-end appearance PU leather Metal Logo Plates Creates a high-end appearance Most fabrics Woven Labels Relatively low cost Most fabrics PVC Rubber Labels Relatively low cost with a casual style Polyester, nylon, canvas   Q8: Which Logo Application Techniques Are the Most Durable and Least Likely to Peel or Fade? Embroidery and high-frequency embossing on PU materials offer the best durability. Screen printing can last for years under normal use, but vigorous scrubbing and wiping with alcohol should be avoided.   Q9: Are There Any Color Limitations for Cosmetic Bag Printing? With screen printing, each additional color requires an extra production step and an additional screen-making fee. If the design contains more than four colors, we recommend switching to heat transfer printing or digital printing, as the overall cost may actually be lower.   Q10: What Colors Are Most Popular for cosmetic pouch? Neutral colors such as black, white, gray, and beige are the most versatile and tend to generate higher repeat-purchase rates. For younger target audiences, muted shades of pink, blue, and green are also popular choices. We recommend referring to the current season's Pantone trend colors or providing reference images of competing products. The factory can assist with color matching and sample approval.   Q11: Can Cosmetic Bag Packaging Be Customized? Yes. We offer a variety of packaging options, including polybags, color boxes, dust bags, hang tags, and barcodes. All of these can be customized with your brand information.   Q12: What Compliance Requirements Apply to Cosmetic Bags Exported to Europe and the United States? European Union: REACH Regulation (chemical substances). If the products are intended for the children's market, EN 71 requirements should also be considered. United States: California Proposition 65.Common testing items: Azo dyes, formaldehyde, heavy metals, and phthalates (particularly important for PVC materials).   Q13: How Can You Find a Suitable Cosmetic Bag Manufacturer? We recommend evaluating a factory's capabilities in the following four key areas: Industry and product expertise: Check whether its previous projects include similar materials or manufacturing techniques. Response speed and communication efficiency: Determine whether the factory can quickly understand your requirements and provide professional recommendations. Certifications and compliance: Confirm whether it has the factory audit reports or environmental certifications required for export. Quality control procedures: Verify that the factory has a comprehensive quality control process, including incoming material inspection, in-process inspection, finished product sampling inspection, and final pre-shipment inspection, to ensure that every batch of products meets the agreed standards.   Q14: What Quality Inspection Standards Are Used Before Shipment? We follow AQL (Acceptable Quality Limit) sampling inspection standards, typically using AQL levels of 1.5/4.0. Key inspection points include:  Stitching strength Zipper smoothness Logo adhesion and durability Dimensional tolerance (±0.5 cm) Appearance defects   Q15: What Is the Minimum Order Quantity (MOQ) for Custom Cosmetic Bags? Standard fabrics + screen-printed logos: Starting from 500–1,000 pieces. Custom fabrics / special manufacturing techniques: Starting from 1,000 pieces. In-stock fabrics + simple manufacturing techniques: Some styles may be negotiable at 300–500 pieces.   The MOQ mainly depends on fabric procurement requirements and how printing screen costs are allocated across the order.   Q16: How Long Does It Take to Produce a Cosmetic Bag Sample? Is There a Sampling Fee? Standard sampling typically takes 5–7 days. Sample fees depend on the complexity of the manufacturing techniques involved.   Q17: How Long Is the Lead Time for Bulk Production? After sample approval, bulk production typically takes 25–35 days, including fabric procurement, manufacturing, quality inspection, and packaging. During the peak season (September–December), we recommend allowing an additional week.   Q18: What Are the Payment Terms? Standard payment terms are a 30% deposit and the remaining 70% payable before shipment. The balance can be paid after inspection.   Q19: What Information Should You Provide to Get a Fast Quote for Custom Cosmetic Bags? We recommend preparing the following information: Design artwork or reference images: Clearly indicate the desired style and structural design. Specified materials or texture requirements: Identify the preferred fabric or desired hand feel. Logo files and preferred application technique: Provide the logo artwork and specify the preferred logo application method. Estimated order quantity: Indicate the anticipated quantity.   The more detailed the information provided, the more accurate the quotation will be, helping reduce the time and cost associated with repeated communication.   Q20: Will the Sample Be Confirmed Again Before Bulk Production? Yes. Before mass production begins, we provide a pre-production sample (PP sample) for the customer's final approval. This is a crucial step in ensuring that the color, materials, and manufacturing techniques used in bulk production match expectations.   We recommend carefully checking the sample and signing off on it once everything is confirmed. The approved and sealed sample will serve as the reference standard for subsequent product inspections.   Conclusion Customized cosmetic bags are more than just manufactured products; they are an extension of a brand's philosophy and identity. From material selection to manufacturing techniques, every step directly affects the final user experience and brand image.   We hope this FAQ on custom makeup bags helps clarify the key considerations in the customization process and enables you to make more informed decisions.   If you have additional customization requirements or specific questions, please feel free to contact our professional team. As a specialized cosmetic bag factory, we are committed to providing one-on-one consultations and tailored solutions to help you create high-quality products that combine aesthetics with practicality.     Author        
1 2 3 4 5 6 7 8 9 10 11 12
A total of12pages
Contact Us
Address : Unit 905, Block B, Jinri Building, No. 88 Anling Second Road, Huli District, Xiamen, Fujian, China
Get in Touch

Please Read On, Stay Posted, Subscribe, And We Welcome You To Tell Us What You Think.

Linkedin WhatsApp Facebook instagram

Copyright @2024 Synberry Bag & Package Products Co.,Ltd All Rights Reserved. Network Supported

Sitemap / Blog / Xml / Privacy Policy

Contact Us

Contact Us
Hi there, I hope you're having a lovely day! Thank you for reaching out to us at Synberry --- where 30 years of craftsmanship meets everyday style. With three decades of expertise in bag manufacturing, we don't just make bags --- we build trust, stitch by stitch. Whether you're looking for timeless design, durable quality, or a partner who truly understands your needs,feel free to talk to us.
submit

home

products

WhatsApp

Contact Us