china backpack manufacturer
Home

Blog

Blog

  • How Is Antimicrobial Fabric Made?
    How Is Antimicrobial Fabric Made? Sep 23, 2026
    Antimicrobial fabrics are made in three primary ways: antimicrobial agents such as silver ions, copper and zinc are blended into the raw material at the fiber-manufacturing stage, giving the fiber itself antimicrobial properties; an antimicrobial finish is applied after the fabric is woven, through padding or coating processes; or a coating or film containing antimicrobial actives is laminated onto the fabric surface. In addition, natural fibers such as bamboo and hemp exhibit inherent bacteriostatic properties of their own.   If you have ever checked the labels while choosing a gym bag, backpack or travel case, you have likely come across terms like “antimicrobial fabric,” “odor-resistant” or “antibacterial lining.” But what do these claims actually mean?   As an OEM/ODM bag manufacturer, Synberry works with antimicrobial textiles every day. In this article, we break down the principle, pros and cons, compliance requirements and practical applications of each process in custom bag manufacturing.   Contents Ⅰ. Antimicrobial Fabric: Definition and Technical Boundaries Ⅱ. Four Manufacturing Processes for Antimicrobial Fabric Ⅲ. Quality Control and Testing Standards: How to Verify Antimicrobial Fabric Ⅳ. Regulatory Compliance for Antimicrobial Fabric Ⅴ.Practical Applications of Antimicrobial Fabric in Bag Manufacturing Ⅵ. Frequently Asked Questions (FAQ) Ⅶ. Conclusion   Ⅰ. Antimicrobial Fabric: Definition and Technical Boundaries Antimicrobial fabric is a textile that has been treated or specially manufactured to inhibit the growth of microorganisms such as bacteria, fungi and mold. Rather than masking odor, its job is to reduce the microorganisms that cause it at the source.   Two concepts are often confused and need to be clarified first: Antimicrobial ≠ odor-resistant. Odor-resistant fabrics usually mask odor by adsorbing or neutralizing odor molecules, while antimicrobial fabrics inhibit the reproduction of odor-causing bacteria at the source. The two are frequently combined, but antimicrobial treatment delivers a more fundamental effect over long-term use. Antimicrobial ≠ bactericidal. “Bacteriostatic” means inhibiting the reproduction of microorganisms, whereas “bactericidal” means killing them. Most textile antimicrobial functions fall into the bacteriostatic category: the mechanism is to prevent bacteria from colonizing and proliferating on the fabric surface, rather than actively killing them.   Understanding this distinction is essential for choosing the right test standards and interpreting test reports correctly.     Ⅱ. Four Manufacturing Processes for Antimicrobial Fabric 1. Fiber-Level Treatment (Built-in Protection) This is one of the most durable processes: treatment is applied at the fiber or yarn stage — before weaving. Antimicrobial agents (such as silver, copper and zinc compounds) are added directly to the polymer during fiber extrusion. Principle: Silver ions (Ag+) bind to bacterial cell walls and disrupt their function. Mechanistically, silver ions bind to sulfur-containing proteins on the cell membrane, altering the cell wall structure while interfering with DNA replication and metabolic enzyme activity, ultimately leading to bacterial death. Gram-positive bacteria such as Staphylococcus aureus carry a thicker peptidoglycan layer and a negatively charged surface, making them more likely to adsorb positively charged Ag+, which destroys the cell wall and kills the cells. Because the antimicrobial agents reside inside the fiber rather than on its surface, they do not wash out easily. Effect: Long-lasting protection that withstands repeated washing and heavy everyday use — an excellent fit for high-performance bag products.   2. Fabric Finishing (Surface Coating Treatment) Another common approach is to apply an antimicrobial finish after the fabric has been woven. The fabric passes through a padding bath or coating rollers to pick up the finishing agent, and is then dried and cured at high temperature.   Common finishing agents include: Silver-based compounds (e.g., silver chloride, nano-silver) Quaternary ammonium compounds (“quats”) Natural antimicrobials such as chitosan (derived from crustacean shells) or plant essential oils   Note: Finishing is lower in cost, but its laundering durability is weaker than fiber-level treatment — performance gradually declines with each wash cycle.   3. Antimicrobial Coatings and Lamination For the bag industry, this is the most practical and widely used approach. A thin antimicrobial coating or film is laminated onto the bag’s lining or outer fabric — often completed in the same production step as a waterproof coating or PU coating.   Because it can be embedded directly into existing production lines, it is highly cost-effective and scalable for high-volume custom manufacturing.   4. Naturally Antimicrobial Fibers Some fibers are inherently antimicrobial and require no chemical additives: Hemp and bamboo fibers contain naturally occurring bacteriostatic constituents The lanolin in wool provides mild antimicrobial activity   It is worth noting that copper-ion fiber, though commonly used in antimicrobial textiles, is a modified man-made fiber with copper ions embedded inside during spinning — not a natural fiber.   Natural fibers used alone usually fall short of stringent antimicrobial standards, but they can be combined with other processes while appealing to environmentally conscious consumers. In practice, a “natural fiber + physical antimicrobial finish” combination is often adopted.     Ⅲ. Quality Control and Testing Standards: How to Verify Antimicrobial Fabric A fabric must pass standardized testing before it can truly be called “antimicrobial.” The most frequently cited standards include: • AATCC 100 (US textile antibacterial test standard): uses the shake flask method to calculate the 24-hour antibacterial rate. In commercial practice, an antibacterial rate of ≥90% is commonly used as the effectiveness threshold; this figure is not a mandatory pass/fail criterion in the standard text. • ISO 20743 (international standard for evaluating antibacterial activity): uses the quantitative absorption method to determine the antimicrobial activity value. The industry generally agrees on R ≥ 2.0 (a 2-log reduction) as the commercial threshold for effectiveness; this threshold is likewise not a mandatory provision of the standard. • JIS L 1902 (Japanese Industrial Standard): covers both quantitative (bacterial suspension absorption) and qualitative (zone of inhibition) methods. The standard was in fact revised from ISO 20743, and the quantitative test methods of the two are consistent.   Key insight on these standards: the three standards differ in test organisms, inoculation methods, contact times and how results are expressed, so they cannot be compared directly. For example, AATCC 100 expresses results as a percentage reduction, ISO 20743 as an antimicrobial activity value (log reduction), and JIS L 1902 may involve both qualitative zones of inhibition and quantitative activity values. Brands should select a test standard based on their target market and customer requirements.   These tests assess effectiveness by measuring the log reduction of bacteria. For instance, “kills 99.9% of bacteria” corresponds to a 3-log reduction against Staphylococcus aureus or E. coli, with a test contact time of typically 18–24 hours.   Durability testing is carried out with wash cycles per ISO 6330. ISO 6330 only defines the washing procedure and does not set a pass line for antimicrobial performance; however, many brands’ internal specifications and some industry guidance standards require that ≥80% of the antibacterial rate be retained after 50 washes — a technical threshold agreed between customers and the industry.     Ⅳ. Regulatory Compliance for Antimicrobial Fabric This is the most easily overlooked yet most important step in purchasing decisions. Antimicrobial textiles are subject to dedicated regulations in every major market around the world — the days of launching a product on the word “antimicrobial” alone are over.   1. European Union: The Biocidal Products Regulation (BPR) The EU Biocidal Products Regulation (BPR, EU No 528/2012) came into effect on September 1, 2013, formally bringing "articles treated with biocidal products" under regulation.   Under the BPR, antimicrobial-treated textiles sold in the EU market must only be treated with approved active substances. More importantly, if the antimicrobial function is claimed as the product’s primary function, the product may be classified as a “biocidal product” rather than a “treated article,” which triggers a more stringent authorization procedure.   At present, some traditional silver-based active substances are in the review process of ECHA (the European Chemicals Agency) and face the risk of non-approval. Not all silver-ion technologies will be banned; the industry is actively developing BPR-compliant alternative antimicrobial solutions.   2. United States: FIFRA and the EPA In the United States, treated articles with antimicrobial functions are regulated under the Federal Insecticide, Fungicide, and Rodenticide Act (FIFRA). Under FIFRA, products that kill or repel bacteria or germs are pesticides and must be registered with the EPA before they can be sold.   However, FIFRA provides an exemption for “treated articles”: if the antimicrobial agent is used solely to protect the article itself (for example, preventing the fabric from degrading or developing odor due to microbial activity), and no public health claims are made (such as “prevents the spread of bacteria” or “reduces virus exposure”), the article can be exempt from registration. The prerequisites are that the antimicrobial active substance itself must already be EPA-registered for the intended use, and the product must not make claims beyond the scope of the exemption.   3. Other Relevant Regulations Beyond the BPR and FIFRA, the following also deserve attention: • The EU REACH regulation restricts the chemicals used in antimicrobial agents; • California Proposition 65 requires a reproductive toxicity warning when silver exposure from a product exceeds the safe harbor threshold (the relevant requirements took effect in 2025; products meeting the exemption threshold are exempt from the warning); • Under OEKO-TEX® STANDARD 100 certification, biocidal active substances are prohibited in baby-grade and other mucosa-contact sensitive products; for other product classes, compliant biocidal antimicrobial substances are permitted provided their toxicological assessment passes — it is not a blanket ban across all categories.   Ⅴ. Practical Applications of Antimicrobial Fabric in Bag Manufacturing Different bags differ greatly in usage frequency, cleaning methods and exposure environments, which determines the choice of antimicrobial process. As a bag OEM/ODM manufacturer, we typically match processes to the following three scenarios: 1. High-Frequency Washing: Gym Bags, Sports Bags and School Backpacks These bags pick up sweat easily, and consumers expect frequent cleaning. In production, fiber-level antimicrobial fabrics (such as yarns embedded with silver or copper ions) or durable finishes with covalently grafted treatments are the top recommendation. These processes ensure that the antibacterial rate remains above 80% even after dozens or even hundreds of washes (tested to ISO 6330).   2. Damp, Enclosed Environments: Cooler/Ice Bags, Luggage Linings and Shoe Bags These bags have damp interiors with poor air circulation, making them highly susceptible to mold and odor-causing bacteria. In production, the most economical approach is antimicrobial coating and lamination. A coating containing silver-based or quaternary ammonium agents is usually combined with a PU waterproof coating or TPU film in a single lamination step, achieving both water and moisture resistance and microbial control.    3. Light-Duty Use: Promotional Giveaway Bags, Cosmetic Bags and Toiletry Bags These bags are cost-sensitive and are not washed frequently. A low-cost surface padding or spray finish is sufficient to meet basic bacteriostatic needs. By precisely matching the use scenario, antimicrobial fabric delivers maximum value in bag products while balancing cost, durability and compliance.     Ⅵ. Frequently Asked Questions (FAQ) Q1: Does the antimicrobial effect wear off after repeated washing? A: It depends on the process. Fiber-level treatments (built-in antimicrobial agents) can withstand dozens or even hundreds of washes; surface coatings and non-grafted finishes are less durable, typically showing a marked decline after 20–30 washes. Grafted modifications (such as covalently bonded chitosan or silver-based finishes) significantly improve laundering durability.   Q2: Is antimicrobial fabric safe for human health? A: When compliant with regulations and used as intended, approved antimicrobial fabrics are generally safe to use. The key lies in whether the type and dosage of antimicrobial agents meet the regulatory requirements of the target market, such as the EU BPR/REACH, the US EPA/FIFRA or relevant Japanese standards. Reputable bag manufacturers should be able to provide corresponding compliance documents and safety test reports.   Q3: What types of bags are suitable for antimicrobial fabric? A: Almost any bag exposed to moisture, sweat or bacteria-prone environments is suitable, including gym bags, luggage linings, cooler bags, shoe bags, cosmetic bags, diaper bags, medical bags and school backpacks.   Q4: Are natural antimicrobial fibers (such as bamboo fiber) better than chemical antimicrobial treatment? A: Both have their strengths.  Natural fibers are more eco-friendly and skin-friendly, but their antimicrobial strength is limited, and used alone they usually cannot reach the commercial pass thresholds of AATCC 100 or ISO 20743.  Chemical treatments (such as silver ions) deliver stronger antimicrobial performance and can pass standard tests, but some consumers have concerns about their environmental footprint, and regulatory trends such as the BPR’s stance on silver-ion technologies need to be watched.  In practice, a “natural fiber + compliant antimicrobial finish” combination is often adopted.   Q5: How much more does adding antimicrobial function cost for a bag? A: The cost increase depends on the type of antimicrobial agent, process route, fabric weight (GSM) and order quantity.  Generally speaking, antimicrobial coating processes add less cost than fiber-level antimicrobial fabrics (which involve raw-material modification). The actual increase varies significantly from project to project, so we recommend requesting itemized quotations from suppliers on a per-project basis. Large-volume orders can effectively amortize unit costs.   Ⅶ. Conclusion Antimicrobial fabric is not magic; it is built on materials science across three levels: fiber, fabric and coating. Silver-ion antimicrobial linings, coated antimicrobial finishes and natural fiber blends each have their own pros and cons. The best solution is determined by combining the product’s use scenario, the export market’s regulations and the project budget.     Author        
  • What does GRS certified mean?
    What does GRS certified mean? Sep 21, 2026
    GRS (Global Recycled Standard) is an international, voluntary product standard developed by Textile Exchange. The standard is designed to verify the recycled material content of products and ensure the traceability of these materials throughout the entire supply chain.   At the same time, GRS also covers requirements related to social responsibility, environmental management, and chemical restrictions, to ensure that the production process of recycled products complies with environmental and ethical standards. In short, obtaining GRS certification means that the product not only contains a certain percentage of recycled materials, but also that the entire production process has undergone rigorous third-party auditing and meets relevant sustainable development requirements.   For bag OEM purchasers, understanding GRS certification is not only a reflection of choosing environmentally friendly materials, but also a key measure to mitigate supply chain risks and meet brand compliance requirements. By purchasing GRS-certified products, brands can ensure that upstream suppliers meet international standards in areas such as raw material traceability, labor rights protection, and pollutant emissions, thereby effectively addressing increasingly stringent international trade barriers and consumers’ expectations for transparent production.   In addition, GRS-certified bag products can help enhance brand image, strengthen market competitiveness, and provide brands with a more compelling sustainability narrative.   Table of Contents:   What Materials Does GRS Certification Cover? What Are the Steps for Obtaining GRS Certification? The Specific Role of GRS Certification in Bag Manufacturing FAQ Conclusion   1. What Materials Does GRS Certification Cover? The GRS standard applies to any product containing at least 20% recycled materials. Its scope is not limited to the textile industry, but broadly covers the entire supply chain, from raw material recovery, processing, and manufacturing to the distribution of finished products.   According to Textile Exchange, qualified recycled materials are mainly divided into two categories: Post-Consumer Recycled (PCR) materials and Post-Industrial Recycled (PIR) materials.   Post-Consumer Recycled (PCR) Materials: These refer to waste generated by households, commercial facilities, or public facilities. These items are no longer capable of serving their original intended function and are collected and reprocessed into new materials. Examples include discarded plastic bottles (PET) collected from recycling centers, old clothing, or scrapped automotive interiors. Since these materials directly reduce the amount of waste entering landfills or the natural environment, they are generally considered to have greater environmental value and are also a key aspect that brands emphasize in their marketing. Post-Industrial Recycled (PIR) Materials: These refer to waste generated during the manufacturing process. Such waste has never entered the consumer market but is recovered and reused because it does not meet quality standards or is left over from production. Examples include fabric scraps left over from cutting processes in textile factories, runner materials from injection molding, or waste yarn generated during the spinning process.   In the bag industry, GRS-certified materials come in various forms, mainly including: Recycled fibers: Such as recycled polyester (rPET), recycled nylon, recycled cotton, etc. Among these, rPET is currently the most widely used recycled material and is mainly derived from recycled plastic beverage bottles. Recycled metal and plastic accessories: Accessories such as zipper teeth, buckles, hooks, and other components are also within the scope if they are made from recycled metal or recycled plastic and the supplier holds a valid GRS certificate.   The GRS standard places particular emphasis on the integrity of the Chain of Custody, requiring all companies involved in the production process—including recyclers, spinning mills, weaving mills, dyeing and printing factories, accessory suppliers, and final bag assembly factories—to obtain GRS certification. This ensures that recycled materials are not mixed up or replaced during the transfer process, thereby achieving full traceability from the source to the finished product.     2. What Are the Steps for GRS Certification? GRS certification is not a one-time audit, but a complete process covering application, auditing, certification, and ongoing monitoring.   Application Submission: The company must submit an application to a third-party certification body recognized by Textile Exchange and sign the relevant agreements. The certification body will then conduct a preliminary review of the company's management system documents to determine whether they meet the basic requirements of the GRS standard regarding recycled material content claims, Chain of Custody traceability, environmental management, and social responsibility. On-Site Audit: After the document review is approved, the certification body will arrange an on-site audit. Auditors will conduct an in-depth inspection of the production operations and verify key records such as raw material procurement records, production logs, inventory records, and waste disposal records. Particular attention will be paid to verifying the full traceability of recycled materials from warehouse entry to finished product shipment, ensuring the accurate implementation of physical segregation or the mass balance calculation method. At the same time, auditors will also inspect the factory's compliance in areas such as chemical management, wastewater treatment, and employee rights protection. Post-Certification Transaction Management: If any non-conformities are identified during the on-site audit, the company must complete corrective actions within the specified timeframe and provide supporting evidence. Only after all major non-conformities have been closed and minor non-conformities have been properly addressed will the certification body issue a GRS Scope Certificate (SC). It is important to note that certification does not mean that every transaction is automatically compliant. When goods are delivered between buyers and sellers, a Transaction Certificate (TC) usually needs to be applied for in accordance with the relevant rules. The TC verifies details such as the product name, composition, recycled material percentage, quantity, buyer and seller, and transaction date.   In addition, GRS certification has a validity period. Generally, an annual surveillance audit or recertification is required to ensure continued compliance with the standard requirements. For a bag factory, planning the certification schedule in advance and coordinating preparation with upstream and downstream partners are key to successfully passing the certification process.   3. The Specific Role of GRS Certification in Bag Manufacturing In bag manufacturing, the core role of GRS certification is to ensure that every component containing recycled materials is traceable and compliant. Fabric, as a major component of bags, is a key focus of GRS certification. When selecting recycled fibers, brands should prioritize suppliers that hold a valid GRS Scope Certificate (SC) and request the corresponding Transaction Certificate (TC) to verify the authenticity of each batch of materials. In terms of accessories, zippers and buckles are often overlooked, but they are also critical links in supply chain traceability.   Recycled metal zippers or injection-molded buckles containing recycled plastic, if claimed to comply with the GRS standard, must also be produced by certified manufacturers. Since accessories are used in relatively small quantities but come in a wide variety of types, professional bag manufacturers typically establish strict accessory procurement records, clearly distinguishing between recycled and non-recycled accessories to prevent material mixing on the production line.   For filling materials, such as recycled cotton or recycled synthetic fiber filling, it is likewise necessary to verify their recycled content percentage and the qualifications of upstream suppliers.   In the finished product assembly stage, the bag OEM factory must implement strict physical segregation measures or use an approved mass balance system to prevent recycled materials from being mixed with conventional materials. Waste management during the production process must also comply with GRS environmental management requirements to ensure that waste is properly handled.   Ultimately, only when all components have compliant documentation and complete, verifiable production records can the finished bags be recognized as GRS-certified products and the corresponding TC certificate be issued. Therefore, refined management throughout the entire process, from design and material selection to production and manufacturing, is the fundamental guarantee for achieving GRS compliance for bags.   The following are recommendations for brands regarding GRS fabric selection and application: Material Supply Chain Maturity Suitable Bag Types Key Considerations for Procurement Recycled Polyester (rPET) High – Well-established certification system, large supply, and many certified weaving mills Backpacks, laptop bags, travel bags, tote bags, cooler bag linings, promotional gift bags Best cost-effectiveness; good colorfastness and color stability; abundant ready-stock inventory and a wide range of options Recycled Nylon (such as ECONYL®) Medium – Broad certification coverage Outdoor backpacks, travel bags, high-end functional bags, high-end handbags, sports and fitness bags High strength and vibrant dyeing; limited ready-stock options, with higher MOQs and unit prices; suitable for high-wear applications Recycled Cotton Medium – Mature system, but short fibers limit 100% recycled content Canvas tote bags, shopping bags, casual shoulder bags, dust bags Soft hand feel and a strong sustainability story; relatively lower wet strength and limited color options; often blended with rPET or virgin cotton Recycled Polypropylene (PP) Medium – Commonly used in woven fabric form Woven shopping bags, laminated tote bags, supermarket shopping bags Good printing performance and low cost; relatively stiff hand feel; for laminated products, compliance of the adhesive should be verified   In addition to the mainstream materials mentioned above, companies should also pay attention to the balance between physical performance and environmental attributes when sourcing materials. For example, although recycled polyester offers good cost-effectiveness, for high-end bags, brands may prefer recycled fabrics with a special hand feel or functional properties. In such cases, the feasibility and lead time of customized development should be discussed with suppliers in advance. For recycled nylon, although it offers excellent performance, its higher cost and longer lead times require brands to become involved in supply chain planning at the early stage of product development to ensure that the project is delivered on time.   4. FAQ Q1: What is the difference between GRS and RCS? A: GRS is more comprehensive. In addition to recycled content, it also emphasizes chemicals, environmental management, and social responsibility. RCS focuses more specifically on recycled content claims. When customers only require proof of the recycled content percentage, RCS may be sufficient; when customers require stronger supply chain responsibility, GRS is generally more recognized.   Q2: What is the relationship between GRS certification and the percentage of recycled materials? A: GRS certification has clear requirements regarding recycled material content. A product must contain at least 20% recycled materials to obtain GRS certification. The labeling claims also differ depending on the recycled content: When the recycled material content is between 20% and 94%, the product may be labeled “GRS Blended.” When the recycled material content reaches 95%–100%, the product may be labeled “GRS 100.” It should be noted that this percentage refers to the proportion by weight and only counts the certified recycled raw material portion, excluding non-fiber components such as dyes and auxiliaries. For bag brands, clearly defining this percentage helps ensure accurate marketing claims and avoid compliance risks caused by overstating environmental benefits.   Q3: Does GRS certification cover organic cotton or bio-based materials? A: No. The GRS standard specifically applies to “recycled” materials, meaning materials recovered and processed from post-consumer or post-industrial waste Organic cotton is a naturally grown crop. While it aligns with environmental principles, the relevant sustainability certification is GOTS certification. Bio-based materials (such as PLA) are derived from renewable resources rather than recycled waste and are generally covered by other specific standards, such as ISCC PLUS.   Q4: Are GRS products more expensive? Why? A: Generally, yes. Certified recycled materials, dedicated batch management, documentation and TC costs, testing, and batch-to-batch variations can all increase costs. However, reasonable quotations should transparently reflect these factors. An unusually low “GRS quotation” may instead raise concerns about whether traceability and quality control have been compromised.   Q5: If a company has a GRS certificate, can the GRS logo be used on every order? A: Not necessarily. It depends on whether the scope of the certificate covers the relevant materials and processes, whether the recycled content meets the requirements, whether the transaction chain is complete, and whether a Transaction Certificate can be issued for the order. The certificate establishes eligibility, while compliance for each individual batch also requires a complete documentation trail.   Q6: If the final finished-product factory does not have GRS certification, can the brand still use the GRS logo? A: No. GRS certification follows the principle of supply chain Chain of Custody, and the final finished-product assembly factory must hold a valid GRS Scope Certificate (SC) in order to be recognized as a compliant GRS production unit. If the bag factory is not certified, even if the fabrics and accessories it uses all have compliant Transaction Certificates (TCs), the finished product cannot obtain official GRS recognition, and the brand cannot attach a GRS hangtag to the product or use the GRS mark for promotional purposes. In addition, an uncertified factory cannot issue valid Transaction Certificates to downstream customers, resulting in a break in supply chain traceability.   5. Conclusion GRS certification is not only a “passport” for the bag industry to enter green markets, but also a core foundation for companies to build sustainable supply chain competitiveness. For backpack OEM or handbag OEM purchasers, gaining an in-depth understanding of the GRS standard means moving from passive compliance to proactive management. It requires purchasers to look beyond the price and lead time of a single finished product and extend their focus to every link of the upstream supply chain, establishing long-term partnerships based on data transparency and trust.  
  • What Does LWG-Certified Mean?
    What Does LWG-Certified Mean? Sep 17, 2026
    LWG certification (Leather Working Group) means a tannery has passed one of the leather industry's most-recognized independent audits, verifying it meets international standards for environmental protection, chemical management, supply-chain traceability and more.    For B2B buyers sourcing leather bags, it signals compliant, reliable suppliers qualified for access to global markets and effectively mitigates supply-chain risks. Simply put, LWG certification serves as a "responsible production" credential for leather manufacturing.   This is not merely a marketing buzzword; it is a core supplier screening requirement set by international brands and for European and American markets. Brands need to focus not only on product quality but also supply-chain compliance and sustainable development. When evaluating leather-product manufacturers, material compliance should be treated as a key assessment metric.    This article offers a full breakdown of LWG certification from a B2B procurement perspective.   I. What Is LWG?   Founded in 2005, the Leather Working Group (LWG) is a non-profit industry coalition jointly launched by international brands and tanneries including Nike, Adidas, IKEA, Timberland, Clarks, and Marks & Spencer. Its core mission is to develop and implement globally unified environmental audit standards for tanneries.   Important note: LWG applies exclusively to genuine animal leather. PU and synthetic leathers fall outside LWG's audit scope; alternative sustainable standards should be referenced for man-made materials. Furthermore, LWG audits factories — not finished goods or individual batches of material. Certification covers upstream players such as tanneries and leather traders, but does not certify finished handbags.   II. Certification Levels: Gold, Silver, Bronze and Their Business Value   The current Protocol 7.2 uses a 100-point scoring system with four distinct levels, each carrying different implications for procurement strategies:   Level Score Range Meaning for Buyers Gold ≥85 Top-tier environmental performance. Suited for luxury brands and high-end retailers; excellent supporting material for corporate ESG reporting Silver 75-84 Meets requirements for most global brands. Acts as the baseline threshold for entry into mainstream supply chains Bronze 65-74 Basic-level compliance. Increasingly insufficient to satisfy requirements from leading brand clients Audited 50-64 Audit completed but no medal awarded. Most brands do not recognize this as compliant status; buyers must conduct careful due diligence   Notes: Tannery certificates are generally valid for 24 months, and trader certificates for 12 months, subject to dates printed on the certificate. Re-audits are mandatory upon expiry. Partnering with Gold- or Silver-rated suppliers indicates you are working with vendors capable of stable long-term performance and continuous improvement, rather than those achieving compliance for one-off audits.   Beyond total score thresholds, every key audit chapter must hit level-specific benchmarks for Gold/Silver/Bronze accreditation. Poor performance in any single critical section cannot be offset by high scores in others and will directly lower the final medal level.     III. What Does an LWG Audit Actually Assess?   LWG is far more than a routine environmental inspection: it delivers a holistic evaluation of factory operations across roughly 17 audit modules under the current protocol. Every component below impacts supply-chain stability:   1. Environmental management  Wastewater treatment, air emissions, solid-waste disposal, energy efficiency and carbon emissions. This helps confirm factories can withstand regulatory environmental inspections and avoid production shutdowns that cause supply disruptions.   2. Chemical management Verification that factory chemical usage aligns with the ZDHC (Zero Discharge of Hazardous Chemicals) MRSL list, and testing for restricted substances such as hexavalent chromium and formaldehyde. LWG's chemical module cross-references the ZDHC framework. Compliance here directly supports export requirements and mitigates risks of cargo rejection and fines.   Supplementary note: Protocol 7.1 mandates factories implement the ZDHC Level 3 chemical-management system. Holding a standalone ZDHC Level 3 certificate is not sufficient; full process implementation on-site is required.   3. Supply-chain traceability Traceable origin, type and source location for raw hides and skins. This forms the foundational requirement for complying with the EU Deforestation-free Products Regulation (EUDR) and proving legal raw-material sourcing.   4. Social accountability Working hours, wages, occupational health and fire safety. LWG Protocol 7 includes a dedicated Social Audit chapter, though it carries relatively low weighting. LWG accepts pre-existing third-party social-audit outcomes such as BSCI and SMETA to prevent redundant factory audits.   5. Governance systems Existence of continuous-improvement mechanisms and regular monitoring. These criteria help buyers gauge supplier operational maturity and assess long-term collaboration potential.   Important caveat: Although often described as a "comprehensive health check" for factories, LWG does not cover all sustainability topics. Animal welfare, deforestation at farm level, and full labour-rights requirements (e.g. freedom of association, collective bargaining) are outside LWG's direct audit scope. Buyers should supplement LWG findings with other standards and due-diligence tools.   For purchasers, an LWG audit report acts as a full operational health check for factories. It enables quick identification of high-risk and poorly managed suppliers and reduces trial-and-error costs.   IV. Standard Updates: Protocol 7 Remains in Transition; New Sustainability System Timeline Adjusted   LWG is rolling out its largest-ever standard overhaul. The new LWG Sustainability System was scheduled for phased roll-out, including modules for the Leather Production Standard, Chain-of-Custody (CoC), deforestation due diligence, and decarbonisation frameworks with factory-level carbon metrics. Carbon emissions and raw-material traceability will shift from bonus criteria to mandatory core audit requirements.   Based on latest public announcements, LWG has postponed the official launch of the full LWG Sustainability System to early 2027. As of September 2026, Protocol 7 remains the active audit protocol, while the new system stays in pilot, consultation and preparation phases. Protocol 7 will not be fully superseded immediately in 2027; the full transition timeline will follow official LWG announcements.   Timeline (updated September 2026): • 2023-2025: Multiple rounds of public consultation on new standards; pilot audits completed at 15-20 global factories between 2024-2025. • 2026: Further refinement of the new framework and modules; expanded pilot scope. Official launch delayed; Protocol 7 continues as the valid audit reference. • Early 2027: Official release of the LWG Sustainability System, followed by a transition period for migration audits. • Full replacement: To be confirmed via official LWG communications; complete replacement is not expected to occur in 2027.   Implications for Buyers • Audit requirements for certified factories will keep evolving; certification does not grant permanent validity. When collaborating, always verify certificate expiry dates, re-audit status, and pro-actively enquire about suppliers' migration-audit roadmaps. • The extended transition window still brings pressure for carbon-data management and raw-material traceability. Suppliers lacking robust data capabilities may face extensive remediation work, which could temporarily affect supply reliability. • Brand-level requirements for chain-of-custody and deforestation due diligence will cascade down the supply chain. • Include suppliers' LWG level, certificate validity, audit protocol version, progress toward adopting new standards, and carbon-data management foundations within annual supplier reviews. Prioritise partners proactively preparing for the upcoming new system.   V. Tangible Business Benefits of LWG-Certified Tannery Partnerships for B2B   Collaborating with LWG-certified tanneries delivers these practical advantages: • Market-access security: Many premium international brands make LWG certification a supplier entry requirement. For instance, Coach has publicly targeted sourcing at least 90% of its leather from Silver-level or higher tanneries by 2025; Hugo Boss aims for 100% of leather procurement to meet at least Silver standard by 2027. These represent publicly disclosed corporate targets subject to internal brand policy updates. Confirm clients' latest procurement rules prior to contracting. • Reduced repetitive factory audits: LWG audits are widely recognised across global brands. One audit can be accepted by multiple stakeholders, cutting audit-related time and expenses. • Regulatory-risk mitigation: Supports compliance with European and American environmental and chemical regulations including REACH and EUDR, lowering legal exposure and brand-reputation risk. • Strengthened ESG performance: Integrate LWG into sustainable-procurement programmes to demonstrate supply-chain transparency to clients and investors.   VI. Frequently Asked Questions (FAQ)   Q1: Is LWG certification awarded to finished-goods leather factories or tanneries? A:LWG certification is issued to tanneries. Finished-goods leather manufacturers cannot obtain tannery-focused LWG certification. Finished-product factories achieve supply-chain compliance by purchasing leather originating from LWG-certified tanneries.   Q2: How long is an LWG certificate valid? A:Tannery certificates are typically valid for 24 months; trader certificates for 12 months. Re-audit is required upon expiry. Always confirm a certificate is in force before entering procurement partnerships.   Q3: What is the relationship between LWG and ZDHC? A:LWG audits incorporate ZDHC hazardous-chemical-control requirements. Protocol 7.1 mandates factories establish a ZDHC Level 3 chemical-management system.   Q4: Does holding an LWG certificate automatically guarantee compliance with the EU Deforestation-free Products Regulation (EUDR)? A:Not exactly. LWG traceability modules deliver foundational prerequisites for EUDR compliance, yet an LWG certificate is not equivalent to formal EUDR compliance proof. Companies must retain full batch-level traceability documentation and complete supply-chain due-diligence procedures to satisfy regulatory obligations.   Q5: What direct impacts will the new-standard transition have on buyers? A:The full new system launch has been pushed to early 2027, extending the transition period while uncertainties persist. Some established tanneries risk downgrade or certificate withdrawal during migration audits if they fail carbon-disclosure and ZDHC Level 3 system requirements, shrinking the pool of available qualified suppliers.  In parallel, customers will request upstream tannery carbon-emission and chemical-management documentation, requiring proactive document collection from suppliers. Track official LWG timelines and request migration-readiness plans from vendors.   Q6: Are counterfeit LWG certificates possible? How can I verify authenticity? A:Fake certificates exist. Do not rely solely on PDF files provided by suppliers. Use the official LWG public database to input factory names and validate certification level, expiry date and audit-protocol version.   Q7: Can a tannery's rating drop from Gold to Silver? A:Yes. Re-audits take place every two years. Non-compliance with updated carbon metrics under new rules may also trigger downgrades. Ratings are not permanent; conduct periodic re-verification for active partnerships.   Q8: Do PU or synthetic leathers require LWG certification? A:LWG covers only genuine animal-based leather. PU and synthetic alternatives sit outside LWG's audit scope; other sustainability standards apply for man-made materials.   Q9: If a supplier holds LWG certification, is REACH testing still required? A:Yes. LWG constitutes a factory-system audit; REACH covers substance-level testing of finished products. The two are not interchangeable. While LWG reduces chemical-risk exposure, it does not waive finished-goods testing obligations.   Q10: Are LWG audits performed by third-party on-site assessors? A:Yes. LWG authorises qualified independent third-party bodies to conduct on-site audits. Audits are neither run directly by internal LWG staff nor self-declared by factories.   Q11: Are LWG certificates differentiated for tanneries versus traders? A:Yes. Distinct certificate types exist for tanneries and leather traders. When sourcing genuine leather raw materials, confirm you are reviewing a tannery certificate: trader certificates are not equivalent to tannery accreditation. Notably, leather trader standards do not issue Gold/Silver/Bronze medals — only pass/fail outcomes. Beware of industry misrepresentation where vendors falsely claim "Silver-level LWG trader status".   A fourth certificate category exists for Commissioning Manufacturers, which are eligible for Gold/Silver/Bronze medals with a 24-month validity; these differ from standard trader certificates. Distinguish medal-bearing certification from separate Chain-of-Custody (CoC) certificates, which serve different purposes. Subcontractor-specific LWG certificates carry only an "Audited" status with no medal awards.   VII. Conclusion   Revisiting our opening question: what exactly is LWG certification?   It serves as a benchmark to evaluate the comprehensive capabilities of leather-goods manufacturers, acts as a passport for brands accessing international markets, and represents a vital tool for procurement teams managing risk and aligning with industry sustainability trends.   As an OEM leather-goods manufacturer, our facility cannot obtain tannery-specific LWG certification since LWG audits target tanneries rather than finished-goods production sites. Even so, we source leather exclusively from LWG-certified tanneries and preserve full batch-level traceability documentation, enabling our clients to meet EUDR, REACH and other compliance requirements. If you are seeking a leather-goods supplier capable of delivering design execution alongside global compliance, please feel free to contact us.     Author        
  • How to customize a mommy handbag?
    How to customize a mommy handbag? Sep 16, 2026
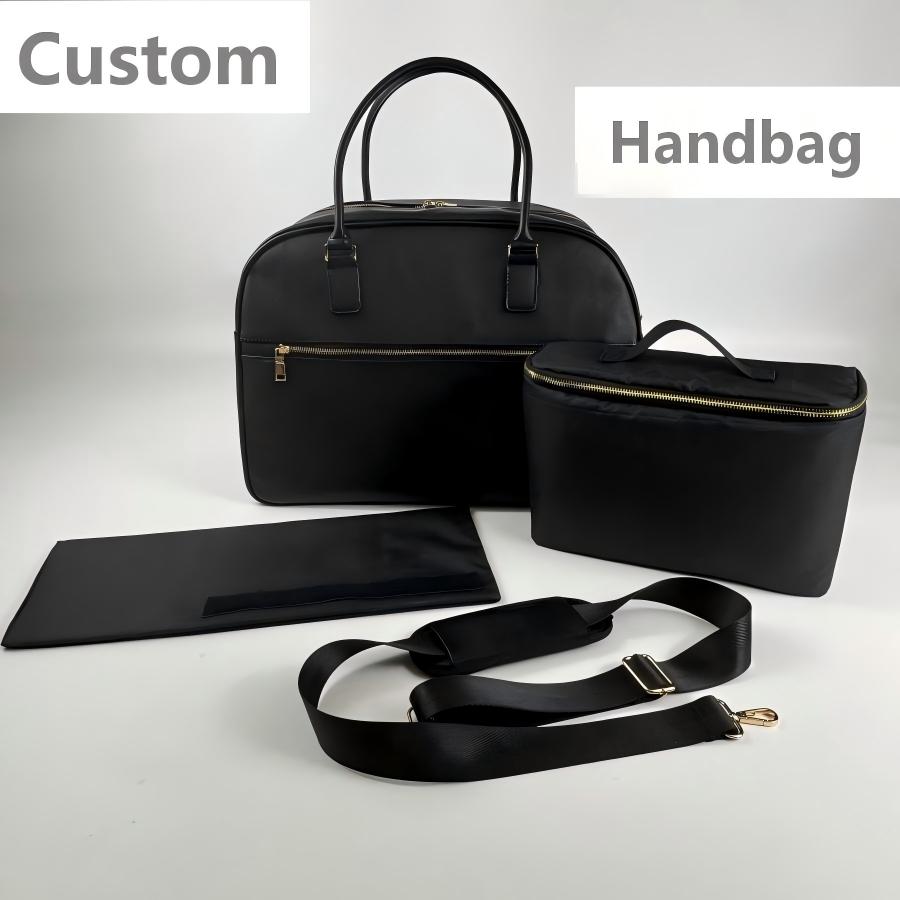
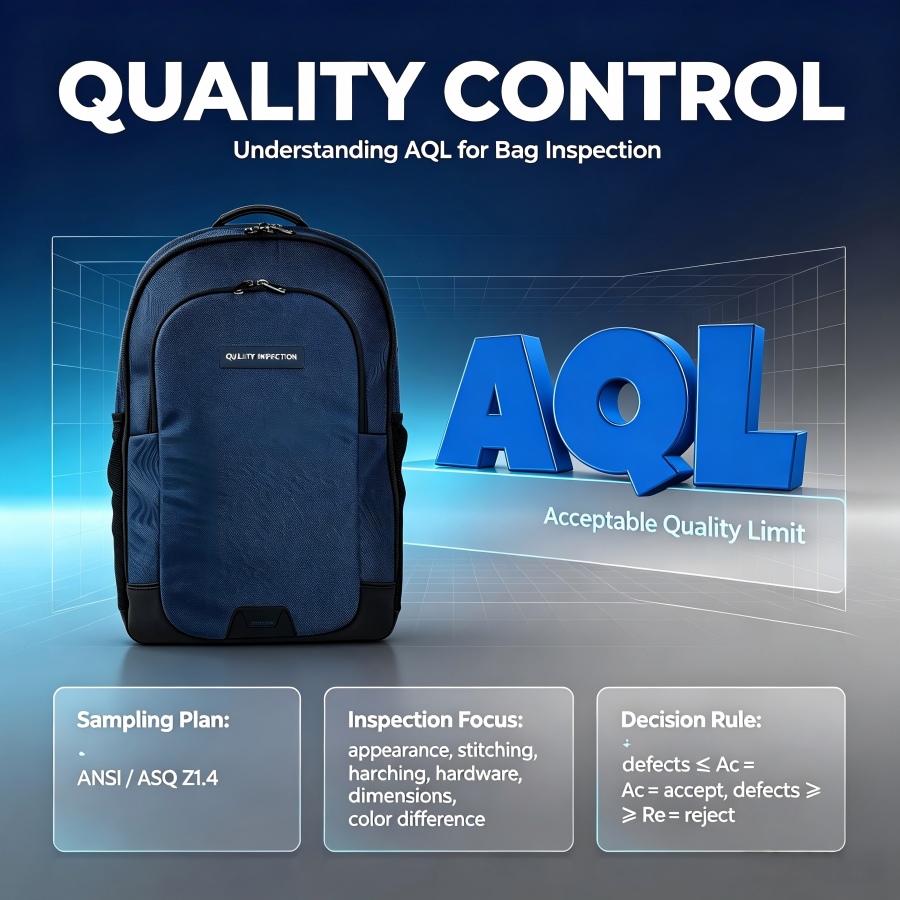
    Today, we're continuing to share the custom bag stories that take place every day at Synberry Bag.   In this article, we’ll take you behind the scenes of the customization process for a high-end mommy handbag, covering every stage from material selection and custom hardware development to pattern making and the final finished product. For your brand, the systematic customization process demonstrated in this case provides a practical reference for developing your own custom bags.   Whether you’re developing a leather duffel bag, a leather tote bag, or a lady handbag , our comprehensive customization process can help turn your design concepts into high-quality finished products.   Table of Contents: Step 1: Organize the Customer’s Technical Specification Sheet and Analyze Customer Requirements Step 2: Fabric Selection Step 3: Hardware and Accessories Selection Step 4: Structural Pattern Making and Internal Storage Planning Step 5: Pre-Production Sample Confirmation and Mass Production Step 6: Frequently Asked Questions (FAQ) About Mommy Handbag Customization   Step 1: Organize the Customer’s Technical Specification Sheet and Analyze Customer Requirements   This is not simply a matter of listing data, but rather a key transformation stage for turning vague market concepts into precise manufacturing processes. We need to communicate in depth with the customer to clearly identify the core pain points and aesthetic preferences of the target user group, thereby determining the bag’s dimensions and specifications, capacity threshold, and load-bearing standards. On this basis, each parameter in the technical specification sheet is subjected to a feasibility assessment, including the fabric’s weight and grain direction, the waterproof rating of the lining, and the salt spray testing grade of the hardware components.   Through the detailed review and organization during this stage, we can not only avoid potential risks in the handbag OEM production process, but also ensure that the final finished product precisely meets the brand’s expectations in terms of functionality and aesthetics, laying a solid data foundation for the subsequent pattern-making process.     Step 2: Fabric Selection   2.1 Fabric The customer wanted a textured black leather-like material that could meet the wear-resistance requirements of daily commuting while also presenting a subtle yet luxurious visual appeal. After multiple rounds of screening and hand-feel comparisons, we ultimately selected three high-quality PU leather materials. These materials retain natural, subtle textures on the surface, with a warm and delicate hand feel. They have also been treated with a special waterproof and stain-resistant coating, so even when exposed to milk stains or rainwater, they can be easily wiped clean, greatly reducing the daily maintenance burden for mothers.   In terms of texture selection, we provided the customer with two refined cross-grain options and one classic unembossed leather material for selection.   Cross-grain texture: The orderly, three-dimensional texture creates rich layers across the black leather surface as light and shadow shift, avoiding the monotony and dullness that can result from large areas of solid color. It perfectly matches the sophisticated yet fashionable character required of a high-end mommy bag. In addition, this texture also offers good scratch resistance and shape-retention properties, helping the bag maintain its structured silhouette. Therefore, it was included as our first choice.  Unembossed leather material: The unembossed leather material interprets another form of sophistication through a simpler visual language. The leather surface presents a smooth and delicate original texture, similar to the soft and fine skin of a baby, with an even softer and more skin-friendly hand feel. Visually, it creates a relaxed and elegant atmosphere, making it particularly suitable for urban mothers who pursue a subtle and understated style.   Although the unembossed leather material is slightly inferior to the cross-grain texture in terms of scratch resistance, its firmness and durability have been effectively enhanced through a thicker base fabric and reinforced coating process. This ensures that it is less likely to develop creases or deformation during daily use, perfectly balancing aesthetics and practicality. It provides an ideal alternative solution for users who prefer a minimalist style, and was therefore included as our alternative option. 2.2 Lining In addition to the main material, the selection of the lining is equally important. It is necessary to consider not only the waterproof performance and hygiene safety of the interior environment, but also the stability of stored items and the convenience of access. For this reason, we also provided three materials for the customer to choose from: high-density waterproof lining fabric, plain-weave fabric with a thick coating treatment, and pure cotton fabric.   High-density waterproof lining fabric: While maintaining a soft hand feel, it is treated with a PU waterproof coating, which can effectively prevent the penetration of liquids such as milk stains and urine. Its smooth surface also makes it easy to wipe and clean on a daily basis. It is the preferred option for balancing comfort and practicality and was therefore our first recommendation to the customer. Plain-weave fabric with a thick coating treatment: With excellent abrasion resistance and a structured feel, it can provide strong structural support for the inside of the bag and prevent the bag from collapsing due to the accumulation of heavy items. However, its disadvantage is that it increases the overall weight of the handbag. Therefore, it was offered as an alternative option, mainly targeting usage scenarios involving users who have extremely high requirements for the bag’s structured shape and who carry a relatively large number of items on a daily basis. Pure cotton fabric: It has a gentle hand feel and excellent skin-friendliness, making it suitable for direct contact with baby clothing. However, its disadvantages are its strong water absorption and lack of structural support. Once it becomes contaminated with liquid, it is difficult to dry quickly and can easily become a breeding ground for bacteria. Therefore, it was also offered as an alternative option, mainly targeting users who have an extreme preference for natural materials and whose usage scenarios are relatively clean. Considering that the exterior surface of the mommy bag needs to be waterproof and abrasion-resistant, while the interior frequently comes into contact with items such as baby bottles and wet wipes, it also needs to have a certain level of waterproof performance. Therefore, based on our recommendation and in combination with its own brand positioning, the customer ultimately selected ① the cross-grain fabric and ① the high-density waterproof lining fabric. This scientifically designed combination of interior and exterior materials not only ensures that the bag maintains a structured and well-defined shape, but also fundamentally addresses the pain points of traditional leather bags being “heavy and difficult to maintain,” providing ideal material support for the subsequent structural pattern-making process.     Step 3: Hardware and Accessories Selection   Metal Zipper Hardware components are a key detail in determining the overall quality and durability of a bag. Considering the high-frequency opening and closing characteristics of a high-end mommy bag, we established three core standards for hardware selection: durability, corrosion resistance, and smooth operation.   First, in terms of material, zinc alloy was selected as the primary material. Its high-density characteristics ensure the structural stability of the hardware components and feet under long-term load-bearing conditions, making them less prone to deformation or breakage. To address the challenge of frequent exposure to moisture and cleaning agents in mother-and-baby usage scenarios, all hardware surfaces undergo a three-layer electroplating process and have passed a 48-hour salt spray test, effectively preventing oxidation and rusting and ensuring that the hardware remains bright and new-looking over time.   In terms of functional experience, we placed particular emphasis on optimizing for “quiet” and “smooth” operation. The zipper system uses customized, high-quality metal teeth paired with precisely polished zipper sliders. This not only provides a silky and smooth opening and closing experience, but also significantly reduces friction noise, preventing harsh sounds when retrieving items while the baby is sleeping and demonstrating thoughtful attention to the details of the usage scenario. In addition, the magnetic fasteners feature a strong magnetic-force design, ensuring both convenient one-handed operation and secure closure, preventing items inside the bag from accidentally slipping out.   In terms of visual presentation, the color and finish of the hardware need to create a harmonious complement to the black cross-grain leather material. We provided three color options for the customer to choose from: light gold, champagne gold, and rose gold. The final selection, champagne gold, uses its soft and warm luster to balance the coolness of the black leather material, adding a touch of elegance and understated luxury to the overall design, perfectly matching the aesthetic preferences of urban mothers.     Custom Metal Logo The customer wanted to customize an exclusive brand logo. We provided the artwork design, and the design team carried out the corresponding process matching based on the brand positioning as well as the color and material of the metal zipper. Considering the understated luxury quality of the champagne gold hardware, we recommended using a 3D die-casting process for the logo to enhance its relief-like layering and substantial feel, avoiding the inexpensive appearance that flat printing may potentially create.   After repeatedly fine-tuning the thickness of the font lines, the roundness of the corners, and the visual center of gravity of the logo on the front of the bag, we ultimately finalized an exclusive metal nameplate solution with a moderate size and smooth, flowing lines.     Through the customization of the hardware components, we not only enhanced the overall durability and user experience of the bag, but also transformed them into refined highlights that complement the overall design, achieving a balance between practical value and artistic aesthetics. This perfectly matches the bag’s sophisticated yet fashionable character, while further enhancing the overall sense of luxury and visual consistency.   Metal Feet To protect the bottom of the bag from friction with the ground and the erosion caused by stains, we installed champagne gold metal feet in the same color family as the zipper at the four corners of the bottom of the bag. These feet not only provide support, making the bag more stable when placed down and preventing the bottom leather material from coming into direct contact with rough surfaces, but also create a visual connection with the front logo nameplate and zipper slider through their refined metallic luster, further strengthening the overall integrity and luxurious feel of the design.     Step 4: Structural Pattern Making and Internal Storage Planning   Pattern making is the core stage of transforming two-dimensional drawings into a three-dimensional physical product, and it is also a key step in determining whether a mommy bag is truly “functional and easy to use.” Based on the material characteristics and hardware specifications determined in the previous two steps, we began the pattern development process, focusing primarily on solving the logic of internal space organization and carrying comfort.   4.1 Functional Compartments In response to the pain point of mothers carrying a wide variety of items when going out, we adopted a modular compartmentalization concept for the internal structure.   The main compartment provides ample space and can easily accommodate larger items such as diapers and changes of clothing; One side features one zippered pocket and two deepened and widened slip pockets; The other side is designed with a thickened, shock-resistant laptop compartment for mothers who need to commute. It can store digital devices and important documents, while the thickened padding effectively cushions external impacts. This design cleverly accommodates the dual identities of a “mother” and a “working woman,” allowing mothers to handle temporary work needs with ease while caring for their babies, achieving a seamless transition between childcare and work.     Additional Functional Design:  A fixed, independent insulated baby bottle pocket was added inside the main compartment and sewn onto one side of the handbag, without affecting the utilization of the main compartment space. The inner layer is made with thickened thermal insulation padding, while the lining uses PEVA insulating material to ensure that the temperature remains stable during feeding.     In addition, we also designed an independent insulated bottle bag that can accommodate 3–4 baby bottles at the same time. It also uses thickened pearl cotton and PEVA insulating materials, providing excellent temperature-retention performance. Whether storing refrigerated breast milk or keeping complementary food warm, it can maintain a suitable temperature for an extended period of time.   It can be removed and used independently, making it convenient for short trips or temporary emergency situations, while it can also be securely fitted inside the bag to prevent shaking and collisions, achieving a flexible “one bag, multiple uses” solution.     4.2 Carrying Comfort In terms of carrying comfort, considering that the weight of a fully loaded mommy bag often exceeds that of an ordinary handbag, we added a 1 mm thick removable PP support board to the bottom of the mommy bag to enhance the bottom’s support and resistance to deformation, while also reducing the load pressure on the hands.   A high-resilience sponge core is embedded inside the handles, with the outer layer wrapped in cross-grain leather material in the same color as the bag body. This not only ensures visual consistency, but also significantly improves the softness and comfort of the grip, helping to relieve hand fatigue caused by carrying the bag for extended periods.     During the pattern adjustment stage, we produced the initial pattern according to the original proportions provided by the customer and conducted three-dimensional draping and real-person simulation testing.   We focused on verifying the smoothness of the bag opening and closing, the convenience of accessing items from the side pockets, and the balance of the overall center of gravity. In response to the insufficient corner radius at the bag corners found during the initial testing, which resulted in the zipper not opening and closing smoothly enough, we fine-tuned the pattern by modifying the curvature of the two top corners of the handbag and optimizing the force distribution along the zipper track. This ensures that the zipper can maintain smooth and effortless opening and closing even when the bag is fully loaded, without jamming or the risk of the zipper bursting open, while also improving the overall aesthetics.     Step 5: Pre-Production Sample Confirmation and Mass Production   Next, the sample was sent to the customer for a comprehensive functional review and detailed inspection to ensure that it remained highly consistent with the expectations established during the earlier stages. After several rounds of usage testing in different scenarios, all indicators of the final sample met the expected standards. The customer gave high praise to this high-end mommy bag, which combines a clean and attractive appearance with practical functionality, and officially signed off on the sample for confirmation.   The successful completion of this stage marked the perfect closed loop from conceptual design to physical realization, while also establishing an uncompromising quality benchmark for the subsequent bulk production.   With the final confirmation of the pre-production sample, the project officially enters the mass production preparation stage. As a leather handbag manufacturer, we have extensive practical experience and understand how to control details and transform them into standardized production processes. We strictly follow the process standards and quality specifications of the confirmed sample, initiate bulk procurement of raw materials and production line scheduling, and ensure that every production process precisely replicates the excellent quality of the confirmed sample.   From incoming material inspection, precise cutting on the cutting table, and detailed stitching on sewing machines, to the strict quality control process (AQL 1.5/4.0), we will monitor production progress and finished-product quality throughout the entire process. We strive to transform this meticulous care for mothers and babies into tens of thousands of high-quality mommy bags through standardized industrial processes, and ultimately deliver them safely and on time to the buyers.   Step 6: Frequently Asked Questions (FAQ) About Mommy Handbag Customization   Q1: How long does it usually take to customize a mommy bag from consultation to shipment? A: It is usually divided into three stages: approximately 2–5 days for technical specification sheet communication and material selection, approximately 7–15 days for pattern making and pre-production sample confirmation (depending on the number of modification rounds and whether molds need to be made for the hardware), and approximately 25–35 days for bulk production. In the case described in this article, because it involved fabric selection, hardware customization, and two rounds of structural pattern-making adjustments, we recommend that brands allow approximately 2 months for the complete cycle.   Q2: What is the minimum order quantity (MOQ) for a customized mommy bag? Is there a sample fee? A: The MOQ will vary depending on whether the fabric and hardware are existing materials. If existing cross-grain PU leather, standard zippers, and feet are used, the MOQ will be relatively low. If a custom metal logo or special hardware requires mold development, the mold cost will need to be shared, and the MOQ will increase accordingly. A sample fee is usually charged for the pre-production sample, and the specific fee depends on the complexity of the product and the difficulty of the manufacturing process.   Q3: Is a leather mommy bag waterproof? What should I do if milk stains or urine stains get on it? A: The cross-grain PU leather material we selected is treated with a special waterproof and stain-resistant coating. Its surface features a fine three-dimensional texture, making it difficult for liquids to penetrate. After milk stains or rainwater splash onto the surface, they can be cleaned simply by gently wiping with a damp cloth. The lining is paired with high-density waterproof lining fabric, which can prevent liquids from penetrating into the inner layers of the bag body, addressing the pain point of being “difficult to maintain” from both the exterior and interior.   Q4: Are the hardware components prone to rusting or fading? A: No. The zippers, magnetic fasteners, and feet used in this case are all made of zinc alloy. Their surfaces undergo a three-layer electroplating process and have passed a 48-hour salt spray test, effectively resisting the corrosion caused by moisture, sweat, and daily cleaning agents, while maintaining smooth opening and closing and a bright finish over the long term. Q5: Can the bag really keep items warm? How long does the insulation effect last? A: Yes. We designed a fixed, independent insulated baby bottle bag inside the main compartment, using thickened thermal insulation padding + PEVA insulating material. In addition, we provide a removable insulated handbag with a thickened pearl cotton structure that can accommodate 3–4 baby bottles at the same time. Refrigerated breast milk or warm complementary food can maintain a suitable temperature for several hours under normal room-temperature conditions, so there is no need to carry additional insulation equipment for short trips.   Q6: What size laptop can fit in the laptop compartment? A: The shock-resistant laptop compartment in this case uses a thickened padded design and can generally accommodate 13–14-inch laptops and important documents. The actual dimensions can be adjusted according to the commuting habits of your target users. During the pattern-making stage, we will provide physical simulation testing for confirmation.   Q7: What processes can be used for the logo on a leather handbag? A: Common processes include metal die-cast nameplates, hot stamping, leather embossing, embroidery, and others. To match the understated luxury quality of the champagne gold hardware, the customer in this case selected a three-dimensional die-cast metal logo. Our design team provides artwork design and size adjustments free of charge, while the mold fee is quoted separately according to the actual manufacturing process.   Q8: Will the bag deform when fully loaded? Will the handles feel uncomfortable or dig into the hands? A: We address this issue through a three-part structural solution: ① A 1 mm removable PP support board is built into the bottom to enhance bottom support and resistance to deformation; ② A high-resilience sponge core is embedded inside the handles and wrapped with leather material to improve grip softness; ③ The cross-grain leather material itself provides good shape-retention properties. During the pattern-making stage, we will also conduct a fully loaded real-person simulation test to verify the balance of the overall center of gravity.   Q9: How is the quality of bulk production guaranteed? A: Bulk production strictly follows the process standards of the pre-production confirmed sample. The entire process is monitored, from incoming material inspection, cutting-table operations, and sewing to finished-product packaging. Finished products are inspected by sampling according to the AQL 1.5/4.0 standard, meaning an acceptable quality level of 1.5 for critical defects and 4.0 for minor defects, ensuring that the delivered quality is consistent with the confirmed sample.   Q10: We do not have a design team and only have a product idea. Can we still cooperate? A: Absolutely. You only need to provide the target user profile, core functional requirements (such as whether an insulated bag, laptop compartment, two-way carrying options, etc. are needed), and your budget range. Our technical team will assist in organizing the technical specification sheet, recommending fabric and hardware solutions, and completing the entire development process from drawings to finished products—as demonstrated in this case, the customer provides the concept, and we are responsible for bringing it to life.   Q11: Will the zipper jam or burst open when the bag is fully loaded? A: We specifically verified this point during the pattern adjustment stage. The initial sample had insufficient corner radius at the bag corners, which caused the opening and closing to be less smooth. After modifying the curvature of the pattern and optimizing the force distribution along the zipper track, the zipper remained smooth and free of jamming even when the bag was fully loaded. The pre-production sample has also passed simulated testing under multiple usage scenarios.   Conclusion   Customizing a high-end mommy bag is not simply a matter of combining different materials. Instead, it requires in-depth customization based on user profiles and actual usage scenarios. From the careful selection of cross-grain leather for its abrasion resistance, to waterproof testing of the lining, and then to the thoughtful integration of insulated compartments and a laptop compartment, every stage embodies a deep understanding of the real-life usage scenarios of mothers.   As a leather goods manufacturer with more than 30 years of manufacturing experience, we have always firmly believed that excellent product design can provide brands with market competitiveness that exceeds expectations. It is not merely a carrier of functionality, but also an extension of the brand philosophy and a bridge for emotional connection.   We are committed to transforming every subtle requirement into a tangible, high-quality experience through excellent craftsmanship and rigorous quality control, helping brands stand out in the fierce market competition. We look forward to working with you to uphold craftsmanship and remain true to the original vision, and together create outstanding products that not only understand what customers want but also deliver commercial value.     Author        
  • What does AQL mean?
    What does AQL mean? Sep 07, 2026
    1. What is AQL?   AQL stands for Acceptable Quality Limit (Acceptable Quality Level). It is a statistical sampling method widely used in the global manufacturing industry to determine whether a batch of manufactured goods meets predetermined quality standards. For large-volume shipments, inspecting every single item is not only extremely costly but also very time-consuming. AQL allows quality inspectors to inspect a representative sample and make a statistically valid conclusion about the entire batch of goods.   This concept was formally established by the International Organization for Standardization (ISO) in the ISO 2859-1 standard and has been widely adopted in the military, medical, consumer electronics, and textile industries. In the bag manufacturing industry, AQL serves as a common language between brands and bag factories. It eliminates ambiguity and provides both buyers and sellers with a quantitative reference standard—specifically, the number of defective items that can be accepted in a single inspection according to the AQL sampling guidelines.   2. Understanding What a Defect Is   Before discussing AQL, it is important to first understand defects, meaning defective products. In large-scale production, defects of varying degrees are unavoidable, and they can directly affect the buyer's financial interests.   Inspection is primarily conducted through final random sampling inspection, with the purpose of providing an objective and measurable quality assessment of the batch of products that the buyer is about to receive. Based on the inspection results, the buyer can understand what types of defects may exist in the batch and then make decisions regarding the disposition of the goods.   Different buyers may have different understandings of what constitutes a defect. Defects can be further classified into critical defects, major defects, and minor defects. Generally, buyers will clearly specify the definitions of these defects in their inspection procedures or inspector operation manuals.   In general, these three types of defects can be explained as follows: Critical Defects: Problems that may endanger user safety or violate regulatory requirements, such as harmful chemical substances or sharp metal protrusions. The acceptance number for critical defects is almost always zero. Major Defects: Functional problems or significant appearance defects that are very likely to result in customer returns, such as a damaged zipper, misaligned handles, an incorrectly positioned logo, or obvious color differences. Minor Defects: Small imperfections that do not affect functionality or the overall appearance, such as loose threads, slight surface wear on the lining, or asymmetry that is barely noticeable.   3. Familiarizing Yourself with the AQL Table The “AQL Table” is a statistical tool that purchasing inspectors can use for product inspections, and it is also an industry standard. The standard basically consists of two tables. The first table tells you which “code letter” should be used. Then, based on the code letter, you can determine the corresponding sample size and the maximum number of defects that can be accepted.   First Table: Sample Size Code Letter Table   The table above is based on the ANSI/ASQ Z1.4-2008 standard of the United States (which is generally consistent with the ISO 2859-1 standard).   To understand the first table, you must first understand what “General Inspection Levels” and “Special Inspection Levels” mean.   General Inspection Levels Level Sample Size Discriminating Power Standard Definition and Selection Reference I Smaller Lower Used when a relatively small amount of inspection is sufficient to meet requirements, or when product quality has been stable over a long period and inspection costs are a concern. II Medium Medium Default standard level. Unless otherwise specified, Level II should be used. It is applicable to the inspection of the vast majority of conventional consumer products. III Larger Higher Used when greater discriminating power is required. Applicable to new products, products with significant quality fluctuations, high unit-price products, critical components, products with special customer quality requirements, situations where the consequences of a rejected lot are serious, and other similar scenarios.   Special Inspection Levels The core definition of S1–S4 is: “Used when relatively small sample sizes are necessary and a larger sampling risk can be tolerated.”   Level Sample Size Typical Application Scenarios Reference for Coordination with AQL S-1 Extremely small Used only for very simple checks and very low-risk scenarios AQL ≥ 1.5 (recommended by some industries) S-2 Very small Good processing conditions, highly uniform quality within the lot, simple verification AQL ≥ 1.0 S-3 Small Quality characteristics are determined by design/structure; products that are not manually assembled AQL ≥ 0.25 S-4 Relatively small Inspection costs are extremely high, inspection cycles are long, or the test is destructive AQL ≥ 0.10 Note: Special Inspection Levels are generally not used for comprehensive inspection of an entire lot of products. Instead, they are intended for certain specific testing items on an inspection checklist, such as destructive testing, functional testing, safety testing, and other similar tests. Therefore, for most conventional orders, General Inspection Level II is typically used.   After understanding the inspection levels, you can use the “II” standard to refer to Table A and select the corresponding sample size. For example, if your order quantity is between 3,201 and 10,000 units, the corresponding sample size code letter is “L.”     Table 2:  Normal Inspection Sampling Plan Table   Using the “L” from Table A as a reference, the corresponding sample size for row “L” in Table B is 200. Next, refer to the respective AQL standard values established by the brand or bag manufacturer to determine the corresponding Acceptance Number (Ac) and Rejection Number (Re).   Taking the AQL 2.5/4.0, which is currently widely adopted for mass-market products, as an example: AQL 2.5 means that the Acceptance Number (Ac) for major defects is 10, while the Rejection Number (Re) is 11; AQL 4.0 means that the Acceptance Number (Ac) for minor defects is 14, while the Rejection Number (Re) is 15.   This means that among the 200 samples inspected, if the number of major defects is no more than 10 and the number of minor defects is no more than 14, the lot will be determined to be acceptable. Conversely, if the number of either type of defect reaches or exceeds its corresponding rejection number, the entire lot will be determined to be unacceptable.   By combining the total order quantity, inspection level, and AQL value in this way, brands can scientifically determine the sampling size and acceptance thresholds, ensuring that quality control is both consistent with statistical principles and aligned with actual business requirements.   4. SYNBERRY BAG's Standard: A Detailed Explanation of AQL 1.5/4.0 At SYNBERRY BAG, our quality assurance system is built on the high standards of 0% for critical defects, AQL 1.5 for major defects, and AQL 4.0 for minor defects. This combination strategy is designed to ensure that our products not only meet the bottom-line requirements for safety and regulatory compliance, but also satisfy consumers’ core expectations for functionality and appearance quality.   4.1 “Critical Defects AQL 0”: A critical defect level of zero means that once any fatal issue that could potentially endanger user safety or violate laws and regulations is discovered in the sampled units, regardless of the quantity, the entire lot will be directly determined to be unacceptable and subjected to 100% rework. This is a non-negotiable red line and reflects the brand’s high level of responsibility toward consumer safety.   4.2 “Major Defects 1.5”: These types of defects involve the product’s core functionality or significant appearance issues, such as a zipper getting stuck, handles that are not securely stitched, incorrectly printed logos, or obvious color differences. Such defects are highly likely to result in returns or complaints from end consumers, directly damaging the brand’s reputation.   For these types of defects, we have established a higher inspection standard than the normal commercial standard (AQL 2.5)—AQL 1.5. Taking a sample size of 200 as an example, the Acceptance Number (Ac) for major defects under AQL 1.5 is 7, and the Rejection Number (Re) is 8.   This means that under statistical sampling, the allowable rate of major defects is extremely low. It requires the factory to implement strict controls over critical processes during production to ensure that product functionality and appearance consistency meet high standards.   4.3 “Minor Defects AQL 4.0”: For minor imperfections that do not affect usability or functionality and may only be detected through careful inspection at close range, such as slight loose threads or small stains on non-load-bearing areas of the lining, we apply the AQL 4.0 standard for minor defects. Although these issues do not make the product unusable, an excessively high occurrence rate can still affect consumers’ perception of the brand’s level of refinement.   Setting AQL 4.0 does not mean allowing quality issues to go unchecked. Rather, it represents a rational balance with perfectionism while ensuring that overall shipment efficiency is maintained and costs remain controllable. It ensures that the vast majority of products delivered to consumers continue to maintain a clean, standardized, and presentable appearance.   Through this tiered quality control system, SYNBERRY BAG is able to safeguard core quality and safety while optimizing the allocation of production resources, providing brands with a quality delivery solution that is both reliable and cost-effective.     5. How Do We Implement This Standard? Our implementation follows a strict multi-stage process:   5.1 Incoming Material Inspection Raw materials—including leather, fabrics, hardware, and zippers—are inspected according to AQL 1.5 immediately upon arrival. Non-conforming materials are never allowed to enter the production process.   5.2 In-Process Quality Control (IPQC) Production line inspectors conduct inspections of semi-finished components at critical workstations. Major defects identified at this stage are immediately reworked to prevent them from becoming permanent defects in the finished products.   5.3 Final Random Inspection Finished products are inspected according to the AQL 1.5/4.0 standard, using the sampling tables specified in ANSI/ASQ Z1.4-2008 or ISO 2859-1. The inspection is carried out by trained quality inspectors who are independent of the production team.   5.4 Pre-Shipment Inspection The final verification is conducted before the cartons are sealed. It not only checks product quality, but also verifies packaging integrity, label accuracy, and carton weight.   This layered approach means that by the time a batch of goods reaches the final inspection stage, the defect rate has already been significantly reduced through prevention rather than detection. The AQL standard serves as the final gatekeeper, rather than the primary quality control tool.   6. Frequently Asked Questions About AQL Understanding the theory behind AQL is only the first step. In actual cooperation with a bag factory or handbag manufacturer, brands may also encounter a series of questions and uncertainties regarding practical implementation. Based on our many years of experience serving customers worldwide, we have compiled the following frequently asked questions and detailed answers.   Q1: How exactly is the sample size determined during AQL sampling? Can a brand request an increased sample size? A: The AQL sample size is not arbitrarily determined by the factory or the brand. Instead, it strictly follows the corresponding relationships specified in the sampling tables. The standard uses General Inspection Level II as the default basis. According to the total quantity of the entire lot (Lot Size), a Sample Size Code Letter is determined, and the corresponding code is then matched to the specific number of units to be inspected.   Of course, a brand has the right to request a higher level of inspection strictness, such as switching to General Inspection Level III (with the sample size increasing by approximately 1.5 times), or requiring Tightened Inspection. However, two points should be clearly understood: first, increasing the sample size will extend the inspection period and result in additional labor costs; second, an increase in sample size does not proportionally increase the defect detection rate, because the core of AQL is a probability model, rather than simply increasing the number of units inspected.   Q2: During AQL sampling, should a brand hire a third-party inspection company or rely on the factory’s self-inspection? A: Each approach has its own advantages and disadvantages, depending on how the brand balances objectivity and cost control. Factory Self-Inspection: The advantages of factory self-inspection include fast response, low cost, and the ability to provide immediate feedback on production problems so that rapid rework can be carried out. However, its limitation is the lack of independence. There may be a conflict of interest in which the factory is effectively “both the player and the judge,” resulting in inspection results that may lean toward being more lenient. However, if a supplier with its own strict quality control system is selected, the risk can be significantly reduced.   Third-Party Inspection Companies: The advantages of third-party inspection companies, such as SGS, Bureau Veritas, or inspection agencies designated by the brand, include independence and extensive OFFICE networks. For some large retailers with suppliers distributed across multiple regions all over the world, third-party inspection provides convenience and consistency. Conversely, smaller brands may not have a complete internal QA/QC quality control system and may sometimes rely on the professional judgment of third-party inspection agencies to compensate for their internal capabilities.   The main limitations of third-party inspection are that the cost is relatively high, and such inspections are generally responsible only for the condition of the goods on the day of inspection. It is difficult for third-party inspectors to participate as deeply in the entire production process and quality prevention activities as an internal team can.   Q3:  If a batch of goods is determined to be “Rejected” (Failed) during an AQL inspection, what should be done next? A: Rejection does not mean that the entire batch of goods must be scrapped. The usual handling process includes:   100% Sorting: The factory must inspect all products in inventory one by one and remove all defective items. Repair and Re-Inspection: Repairable defects, such as loose stitching or minor stains, should be corrected, after which the goods are resubmitted for inspection. Concession Acceptance: If the defects do not affect core functionality and the brand agrees, the parties may negotiate a reduced-price acceptance or treat the goods as seconds. However, this must be agreed upon by both parties in advance of the order. Order Reproduction: In cases involving serious defects or defects that cannot be repaired, the brand has the right to request a return or require the factory to assume responsibility for reproducing the order.   In the SYNBERRY BAG Quality Agreement, we clearly commit that if a final inspection is rejected due to reasons attributable to our side, we will bear the resulting rework costs and liability for delayed delivery, ensuring that the brand’s commercial interests are not adversely affected.   Q4: Does the AQL standard apply to all types of bag products? A: AQL is a general statistical sampling method and, in principle, can be applied to products across all manufacturing industries. However, in specific applications, it should be adjusted flexibly according to the characteristics of the product. For structurally complex products with extremely high craftsmanship requirements, such as LUXURY HANDBAGS or PREMIUM BUSINESS BACKPACKS, relying solely on AQL sampling may not be sufficient to cover all potential risk points. Such products often require stricter testing and a higher inspection level, such as Level III.   Q5: Why do different brands set different AQL values, such as 1.5/4.0 versus 2.5/4.0? A: This reflects differences in brand positioning, target customer groups, and risk tolerance. Mass-market fast-fashion brands may tend to adopt AQL 2.5/4.0 to balance costs and shipment speed, while well-known or premium bag brands may choose AQL 1.5/4.0, or even establish customized inspection standards with their factories, in order to maintain their brand image and ability to command a high premium.   SYNBERRY BAG chooses AQL 1.5/4.0 precisely to help brand customers establish a differentiated competitive advantage through superior quality details in a highly competitive market, with very few after-sales complaints, thereby increasing long-term customer lifetime value.   7. Conclusion   Product inspection is essential for understanding the quality of goods before shipment. Effective use of the AQL standard can provide in-depth insight into quality and an objective means of measurement, thereby helping bag OEM purchasing parties make relevant procurement decisions.   If a brand needs assistance in developing an inspection plan and inspection requirements, we are very happy to provide support by leveraging our professional knowledge and experience in the industry.     Author        
  • What Makes a Good Gym Bag?
    What Makes a Good Gym Bag? Sep 01, 2026
    A truly functional gym bag is built around three core elements: intelligent compartment organization, effective ventilation design, and reliable material craftsmanship.   These three elements are equally essential. The compartment layout determines whether users can access their belongings efficiently; ventilation directly affects the internal environment of the bag and odor control; and material selection determines the product’s overall durability and service life. Only by optimizing these three dimensions can a gym bag genuinely solve the practical challenges users encounter during workouts.   As a bag OEM/ODM manufacturer with more than 30 years of industry experience, we have been providing full-service solutions — from design development to mass production — for sports brands across North America, Europe, Australia, and other global markets.   From technical drawings to final production, our extensive manufacturing experience has taught us one key principle: the success of a best-selling product depends on precise control over critical details. Designs that are disconnected from real user scenarios often create unnecessary manufacturing costs without generating long-term customer loyalty or repeat purchases.   In this article, from the perspective of a professional gym bag manufacturer, we will break down how to develop a gym bag that truly appeals to both channel partners and end users, focusing on three essential dimensions: compartment structure, ventilation performance, and material selection. We will also provide practical customization solutions for brands seeking OEM partnerships.   Table of Contents 1. Compartment Planning 2. Ventilation Design 3. Material Selection 4. Gym Bag OEM Purchasing Recommendations 5. What Can We Provide as a Manufacturer? 6. Frequently Asked Questions (FAQ) 7. Conclusion   1. Compartment Planning A well-designed compartment system must satisfy real user needs while maintaining production efficiency. Excessively complicated structures increase sewing processes and defect rates. A smart design approach is based on modularity — allowing flexible customization while maintaining a strong structural foundation.   1.1 Wet/Dry Separation — More Than Just “Two Pockets,” It Is Two Independent Systems During market research conducted for our brand partners, we found that many gym users have experienced problems such as odor transfer between items, mold growth, and moisture damage to electronic devices. Therefore, wet/dry separation is not a marketing gimmick — it is an essential functional requirement.   Our manufacturing solutions include: • Independent Wet Compartment We use TPU-laminated nylon fabrics combined with waterproof zippers and seam sealing processes to achieve effective moisture protection.A drainage structure can also be added to the bottom of the wet compartment. Even if a small amount of condensation occurs, moisture naturally collects in the waterproof base layer instead of leaking into the main compartment. • Ventilated Wet Compartment Design Breathable mesh panels and antibacterial lining fabrics can be integrated into the inner side of the wet compartment cover to improve moisture release and odor control. • Dry Compartment Protection The main compartment can feature a suspended mesh pocket structure that keeps clean clothing and electronic devices elevated, preventing direct contact with the outer wall of the wet compartment and reducing moisture exposure.   Customization Options: Wet compartment size, placement (bottom / side / independent insert), and waterproof zipper specifications can all be adjusted according to brand requirements.   1.2 Dedicated Shoe Compartment — The Key Solution to Odor Control The shoe compartment is one of the areas where gym bag design most often fails. Many brands reduce costs by using only a thin mesh divider, which allows shoe odors to spread throughout the bag and contaminate other belongings.   Our standard configuration includes: • The shoe compartment is separated from the main compartment and is typically positioned at the bottom or side of the bag. A rigid support panel is added to prevent collapse and protect the main storage area. • The shoe compartment lining uses easy-clean coated fabrics that can be wiped clean and prevent dirt accumulation. • Ventilation openings with metal or plastic eyelets can be added to the shoe compartment cover or side panel to improve airflow. • The shoe compartment can be designed to fold away when not in use through hook-and-loop or zipper systems, preserving main compartment capacity.   Customization Options: Shoe compartment location (bottom / side access / top access), detachable structure, ventilation hole design, and lining colors.   1.3 Functional Zoning — Keeping Every Item Organized A gym bag typically carries more than ten different items, including keys, earphones, smartphones, power banks, wrist wraps, resistance bands, water bottles, shaker cups, and other workout accessories.   A properly planned internal organization system keeps belongings neat and allows users to access items quickly and conveniently.   Our modular organization solutions include:   Functional Area Storage Purpose Manufacturing Solution Quick-access front pocket Access cards, keys, earphones Independent zipper pocket with key clip (custom LOGO application available) Side bottle pocket Water bottles, shaker cups Stretch mesh fabric with reinforced bottom stitching for reliable load support Electronic device compartment Tablets, laptops Thickened pearl cotton padding with soft fleece lining for shock and scratch protection Small-item organizer Gloves, wrist wraps, resistance bands Internal elastic webbing with mesh dividers for clear organization Main compartment Clothing, towels, protective gear Spacious open structure with optional corner fastening loops   Customization Options: Number and position of compartments, opening methods (zipper / hook-and-loop / magnetic closure), lining materials, and colors.   1.4 Detail Craftsmanship — The Key to Durability and Brand Reputation • Zipper System Depending on brand positioning, we can provide branded zipper solutions such as YKK or SBS. Reinforcement patches are added at zipper ends to prevent zipper separation caused by excessive pulling force. • Stress Point Reinforcement All high-stress areas, including handles, shoulder strap anchors, and attachment points, are reinforced with multi-layer nylon fabric and bartack stitching to ensure reliable load-bearing performance in daily use. • Stitching Standards High-strength polyester thread is used with consistent stitch density and uniform sewing quality to meet international brand inspection standards. 2. Ventilation Design Even the highest-quality materials cannot deliver an excellent user experience if ventilation is poorly designed. Through years of testing and optimization, we have found that moisture and heat dissipation performance depends on the balance between three key factors: fabric breathability, airflow pathways, and internal compartment architecture.   2.1 Moisture-Controlled Ventilation — Releasing Humidity Without Water Penetration For premium gym bags, we have developed a "breathable wet compartment"system featuring a dual-layer construction: • Outer layer: High-density nylon fabric with water-repellent performance. • Inner layer: A microporous moisture-permeable membrane that blocks liquid water while allowing water vapor to escape freely. • Airflow channels: Ventilation pathways are incorporated at both the top and bottom of the compartment. By utilizing temperature and pressure differences generated after exercise, moisture can be actively released from inside the compartment.The exact implementation depends on the bag structure and design requirements. Common solutions include integrated mesh panels and side ventilation openings.   This construction delivers outstanding moisture transmission performance, achieving the ideal balance of "allowing moisture vapor to escape while preventing water penetration.” 2.2 Shoe Compartment Ventilation — Giving Odors an Exit Path For shoe compartments, we follow a multi-directional ventilation principle.   Rather than simply adding ventilation holes to one surface, we create airflow channels through multiple areas, including the front, back, and bottom panels. The interior of the shoe compartment can also feature an elevated base structure, preventing shoes from directly contacting the bottom of the bag while allowing air circulation underneath.   This continuous airflow helps reduce moisture accumulation and prevents odor buildup after repeated use. 2.3 Back Panel and Shoulder Strap Ventilation — Improving Carrying Comfort Many brands focus only on internal ventilation while overlooking the areas directly contacting the user's body.   For all of our gym bags, the back panel and shoulder strap padding are designed with 3D honeycomb mesh fabric. The thickness, elasticity, and rebound performance are repeatedly tested to provide both cushioning support and efficient sweat evaporation.   This design is particularly suitable for short-distance carrying scenarios, such as walking from the gym entrance to the parking area.   Customization Options: Ventilation hole design, moisture-permeable membrane grade, mesh fabric color, thickness, and density. 3. Material Selection Purchasing Consideration: Material selection represents one of the largest cost factors in gym bag manufacturing and also plays a critical role in brand positioning and perceived value.   We recommend that brands select the most suitable material combination based on target retail price, sales channels, and product positioning, rather than simply pursuing the most expensive or cheapest option.   3.1 Main Fabric — Nylon vs. Polyester For mid-to-high-end gym bag collections, nylon is the material we recommend most frequently due to its superior overall performance.   Performance Nylon (PA) Polyester (PET) Abrasion Resistance ★★★★★ (Excellent abrasion resistance with approximately 90% elasticity recovery, suitable for high-friction applications) ★★★ (Good) Tear Resistance ★★★★★ ★★★☆ Lightweight Performance ★★★★ (Lighter than polyester under the same denier specification) ★★★ Weather Resistance ★★★ (Requires UV additives for enhanced protection) ★★★★★ (Naturally UV resistant) Hand Feel Soft, smooth, and premium tactile experience Firmer texture, more prone to pilling Cost Higher Lower   Our recommendations: • Mid-to-high-end gym bags: Use 600D or higher-grade nylon to achieve a balance between durability and lightweight performance. • Military-grade / extreme-use products: Use 1000D Cordura® nylon or ballistic nylon for exceptional abrasion resistance and durability. • Eco-conscious collections: Use recycled nylon such as ECONYL® or recycled polyester (RPET) with certifications such as GRS to meet the growing sustainability requirements of European and North American markets.   3.2 Waterproof Coating — Why TPU Is a Better Choice For wet compartments, shoe compartments, and bag bases, we prioritize TPU coating instead of traditional PU coating.   The key differences are: TPU (Thermoplastic Polyurethane): • Excellent hydrolysis resistance • Better low-temperature performance • More environmentally friendly and recyclable • Longer service life   PU (Polyurethane): • More vulnerable to hydrolysis over long-term use or in humid environments • More likely to experience coating breakdown, peeling, or delamination   For brands seeking long-term durability and premium user experience, TPU provides a more reliable solution.   All of our lamination processes are completed under strict production controls, with peel strength exceeding industry standards.If you would like to gain a comprehensive understanding of the differences between TPU and PU, please feel free to read our in-depth comparison blog.   3.3 Linings and Hardware — The Often-Overlooked Quality Factors Although lining materials and hardware components are not always visible to consumers, they have a significant impact on product durability and user experience.   Lining Fabric We commonly use tear-resistant nylon oxford fabric and can apply antibacterial and odor-control finishes, including silver-ion or chitosan-based treatments.   Zippers Wet/dry separation compartments should use waterproof zippers, with zipper tape sealed through waterproof coating processes to improve moisture protection.   Hardware Components Load-bearing hardware components use POM (polyoxymethylene / acetal resin) or aluminum alloy. • POM hardware provides high hardness, excellent wear resistance, and stable dimensional performance. • For products designed for extremely cold environments, PA (nylon) hardware is recommended due to its superior low-temperature toughness.   3.4 Sustainable Material Trends In recent years, sustainability has become an increasingly important requirement for European and North American brands.   The eco-friendly materials we currently work with include: • RPET fabric (made from recycled plastic bottles) • Recycled nylon • Bio-based TPU • Solvent-free water-based PU coatings   It is important to note that recycled nylon currently has more limited supply availability due to the complexity of recycling processes. Many recycled nylon specifications require minimum order quantities of approximately 1,000 yards or more.   Therefore, gym bag OEM buyers should communicate with suppliers early to plan material sourcing, production schedules, and order quantities.   Compared with recycled nylon, RPET fabrics have a more mature supply chain and a wider range of readily available specifications.   4. Gym Bag OEM Purchasing Recommendations   Category Our Recommended Standard Our Manufacturing Capability Suitable Brand Positioning Compartment Design Independent wet compartment + shoe compartment + quick-access pockets + small-item organization zones Flexible customization of compartment quantity, location, and opening methods Mid-to-high-end sports brands Ventilation System Microporous moisture-permeable membrane + 3D mesh fabric + ventilation eyelets Customizable ventilation hole density, placement, and structure Recommended standard configuration for premium models Materials 600D+ nylon + TPU coating + branded zipper systems Multiple material solutions and sustainable certification options available Entry-level: 600D nylon; Mid-to-high-end: 840D nylon and above Craftsmanship Reinforced stitching + seam sealing + high stitch density Supports BSCI, ISO, and other factory audit requirements Applicable across the entire product range   A successful gym bag is not created by adding unnecessary features. Instead, it comes from selecting the right combination of structure, materials, and manufacturing techniques based on the actual needs of the target market.   5. What Can We Provide as a Manufacturer? If you are a brand owner, distributor, or designer, you should now have a clearer understanding of our manufacturing expertise. We are not simply a production supplier accepting orders. We are a full-service development partner covering the entire process — from design optimization, material selection, and mold development to prototype creation and mass production.   Our Core Advantages: • 30 Years of Industry Experience With three decades of expertise in bag manufacturing, we have continuously served sports brands across North America, Europe, Australia, and other international markets. This experience gives us deep knowledge of global quality standards, consumer expectations, and market trends.   • Fast Prototyping and Development Support We respond quickly during the sampling stage and work closely with brands through design verification and product refinement, helping transform concepts into tangible products efficiently.   • Flexible Production Capability Our production system supports both small-batch trial production for emerging brands and large-scale manufacturing for established companies. We help customers successfully progress from initial concept development to commercial production.   • Strict Quality Control System From incoming material inspection to final shipment inspection, every production stage is monitored by dedicated quality control personnel to ensure that every bag meets demanding customer expectations.   • One-Stop Customization Service We provide complete customization solutions, including LOGO applications (embroidery, screen printing, heat transfer labels, etc.), color customization, packaging and hangtags, structural modifications, and other personalized requirements — ensuring that brand identity is reflected throughout every detail.   We believe that a successful gym bag is the result of continuous refinement and collaboration between the brand and the manufacturer.   6. Frequently Asked Questions (FAQ) Q1: What are the advantages and disadvantages of placing the wet compartment at the bottom versus the side of a gym bag? A:A bottom wet compartment provides stronger separation from the main compartment and creates a lower center of gravity, improving carrying stability. However, the disadvantage is that access is less convenient, as users usually need to bend down or place the bag horizontally to retrieve items. A side wet compartment offers easier access and visually communicates the wet/dry separation function more clearly to consumers. However, it takes up side space and usually has a more limited storage capacity. From a manufacturing perspective, bottom wet compartments require higher technical requirements for waterproof zippers and base reinforcement, while side wet compartments are relatively easier to manufacture. Currently, many premium gym bags on the market use a combination of a bottom wet compartment and a side shoe compartment.   Q2: What is the difference between waterproof zippers and standard zippers? A:Waterproof zippers use waterproof films or TPU coating processes between zipper teeth. After closing, the zipper teeth create a tighter seal, reducing the possibility of water penetration. Even when the fabric itself is waterproof, standard zippers can still allow water to enter through gaps between the zipper teeth. However, waterproof zippers usually create slightly higher sliding resistance compared with standard zippers, meaning users may need to apply slightly more force during operation. This is a normal characteristic. For brands seeking a smoother user experience, low-resistance waterproof zipper options are available, although they come with higher material costs.   Q3: How many ventilation holes should a gym bag shoe compartment have, and where should they be placed? A:The key principle of ventilation hole design is not simply increasing the number of holes, but creating effective airflow circulation through the shoe compartment. We recommend placing ventilation openings on two opposite surfaces of the shoe compartment, such as: • Front and back panels • Side panel and bottom panel Typically, 2–3 ventilation holes are placed on each side, with a recommended diameter of approximately 8–12 mm. This allows air to enter from one side and exit from another, creating natural airflow circulation when the bag is moved. If all ventilation holes are placed on the same surface, airflow remains limited to the outer area and cannot effectively remove moisture and odors from deeper areas of the compartment.   Q4: How does a microporous moisture-permeable membrane work? Does it really prevent water leakage? A:A microporous moisture-permeable membrane contains extremely small pores, usually ranging from approximately 0.01–0.1 μm in diameter. These pores are much smaller than liquid water droplets (typically hundreds of micrometers to several millimeters), but larger than water vapor molecules (approximately 0.0004 μm). As a result: • Liquid water is blocked due to surface tension and pore-size filtering. • Water vapor can pass through and escape. In simple terms: liquid water cannot enter, but water vapor can exit. However, this membrane structure is delicate. During sewing or production, punctures from needles or excessive heat exposure can damage the membrane and reduce local moisture-permeability performance. Therefore, fabrics containing moisture-permeable membranes require specialized manufacturing processes, such as high-frequency welding or low-stitch-density sewing combined with seam sealing, to protect the membrane integrity.   Q5: What is the practical difference between 600D nylon, 840D nylon, and 1000D Cordura® nylon? A:For everyday gym use — such as exercising 3–5 times per week while carrying clothing, water bottles, shoes, and other personal items — 600D nylon is already sufficient. It provides a good balance of lightweight performance and abrasion resistance. 840D nylon offers a thicker, more substantial hand feel with significantly improved tear resistance. It is suitable for users and brands requiring higher durability performance. 1000D Cordura® nylon represents the benchmark for extreme abrasion resistance. Its durability far exceeds the requirements of normal gym bag applications. Unless the brand positioning focuses on rugged outdoor use, tactical styling, or extreme environments, this specification may be considered excessive for most gym bags. Our recommendation is that brands select materials based on target retail price, product positioning, and brand identity rather than simply choosing the highest specification available for marketing purposes.   Q6: Can consumers actually feel the difference between TPU coating and PU coating? A:Yes. The difference is highly noticeable during actual use. A gym bag using TPU coating can maintain a smooth and intact interior surface even after one or two years of use. By comparison, traditional PU coating — especially polyester-based PU — may begin showing signs of deterioration after six months to one year in humid environments. The inner coating may become sticky, peel, or flake off. In severe cases, coating particles may stick to wet towels, creating a poor user experience. The reason lies in the chemical structure of the materials. Traditional PU coatings are more vulnerable to hydrolysis in hot and humid environments. The ester bonds within the molecular chain can break down when exposed to moisture, while salts and water from sweat accelerate this degradation process. TPU, especially polyether-based TPU, provides significantly better hydrolysis resistance than conventional PU. Although the material cost is higher, the additional investment is worthwhile from the perspective of long-term user satisfaction and brand reputation.   Q7: Why do some gym bags develop a sour odor after long-term use that cannot be removed even after washing? A:The unpleasant odor that develops over time is usually not caused simply by residual sweat. Instead, it is primarily caused by microorganisms and their metabolic by-products inside the fabric structure. Standard polyester fabrics can contain microscopic spaces within their fiber structure where bacteria and fungi accumulate. Meanwhile, proteins and oils contained in sweat provide nutrients that support microbial growth. Even when the surface appears clean after washing, microorganisms trapped deep inside the fibers may remain. When exposed to moisture again, they can reproduce and release unpleasant odors. There are two effective solutions: 1. Apply antibacterial and odor-control treatments during fabric finishing, such as silver-ion or chitosan-based additives. 2. Develop removable and machine-washable inner lining structures, allowing users to thoroughly clean areas that are more likely to accumulate moisture and odor.   Q8: Do sustainable recycled fabrics such as RPET perform worse than virgin materials? A:High-quality recycled polyester (RPET) and recycled nylon can now achieve performance levels very close to virgin materials in terms of abrasion resistance and tear strength. The performance difference is generally within approximately 5%, depending on recycling processes and testing standards. For normal daily use, most consumers will not notice a significant difference. The main difference is usually found in the hand feel. Recycled fabrics may initially feel slightly less soft compared with virgin materials, but this difference becomes much smaller after the first washing cycle. Color fastness should also be carefully evaluated, especially for darker colors. During the sampling stage, brands should conduct sufficient color fastness testing. For brands with sustainability goals, recycled materials are a reliable choice, provided that they are sourced from qualified suppliers with certifications such as GRS (Global Recycled Standard).   Q9: How should a gym bag be cleaned and maintained? Will cleaning affect the materials? A:Cleaning methods depend on the material construction of the bag. For gym bags made with nylon fabric and TPU coating, daily maintenance can usually be handled by wiping the surface with a damp cloth. If odors develop inside the bag, open the wet compartment and shoe compartment and allow them to air dry in a well-ventilated area. Avoid direct sunlight exposure, as excessive UV exposure may affect material performance. If machine washing is necessary: • Use a mild detergent. • Wash with cold water using a gentle cycle. • Remove all rigid support panels or inserts before washing. • Allow the bag to air dry naturally. • Do not tumble dry or iron. It should be noted that frequent machine washing — more than twice per month — may accelerate aging of waterproof coatings and seam-sealed areas. Therefore, we generally recommend spot cleaning whenever possible to extend product lifespan.   7. Conclusion A truly successful gym bag is essentially the result of finding the perfect balance between an exceptional user experience and controlled manufacturing costs.   As discussed throughout this article, whether it is intelligent compartment planning, efficient ventilation systems, or durable material construction, every technical detail ultimately serves one commercial objective:Reducing consumer decision barriers and increasing long-term repurchase potential.   This philosophy represents the value of SYNBERRY’s more than 30 years of expertise in the sports bag manufacturing industry.   From material selection and sewing craftsmanship to prototype development and mass production delivery, we understand not only how to manufacture bags, but also how to help brands transform concepts into commercially competitive products through precise attention to detail.   Whether you are developing a new gym bag collection or looking to optimize an existing product line, even if you only have an initial sketch or concept, we look forward to exploring the possibilities of bringing your ideas to life.     Author        
  • Latest tariff on bags from China and Cambodia
    Latest tariff on bags from China and Cambodia Aug 28, 2026
    Over the past two years, due to frequent changes in U.S. tariff policies, our customers often ask us about the latest tariff rates.  So, what are the current U.S. tariffs on China, Cambodia, and other countries?  The answer is 12.5% on China and 10% on Cambodia since this July.24.2026. Important note that, for China origin, if the HTS code within The Section 301 scope, the tariff 25% imposed since 2018 still remains in effect. The U.S. Supreme Court ruled that the Trump administration's tariff measures implemented under the International Emergency Economic Powers Act (IEEPA) exceeded presidential authority. Subsequently, the Trump administration shifted to citing relevant provisions of the Trade Act of 1974 as the new legal basis to continue advancing its tariff policies. However, there are no more reciprocal tariffs for all countries. Effective July 24, 2026, new import tariff measures have been implemented for 60 countries and regions. Among them, Cambodia has been included in the list subject to a 10% tariff rate, while the previous 19% reciprocal tariff is no longer in effect. According to the plan announced by the Office of the United States Trade Representative (USTR), the countries and regions subject to the 10% rate mainly include those that have committed to prohibiting the import of products made with forced labor, have established relevant regulatory systems, or have enacted related laws but still require strengthened enforcement. The list includes Cambodia, Bangladesh, Malaysia, Indonesia, El Salvador, Argentina, Guatemala, the United Kingdom, and 14 other countries. For the remaining 46 countries and regions, the U.S. will impose a 12.5% import tariff, including major trading partners such as China, Vietnam, Japan, and South Korea.  The following table illustrates the current specific tariff rates using the HTS codes for HANDBAG and BACKPACK as examples: Origin HTS Code Product Commodity Duty Section 301 Tariff New Tariff (from 7/24) Total Rate China 4202.19.00.00 Handbag 20% 25% 12.5% 57.5% China 4202.92.31.20 Backpack 17.6% 25% 12.5% 55.1% Cambodia 4202.19.00.00 Handbag 20% N/A 10% 30% Cambodia 4202.92.31.20 Backpack 17.6% N/A 10% 27.6% Again the new tariffs above had taken effect at midnight Eastern Time on July 24, 2026.   Author        
  • What is salt spray testing?
    What is salt spray testing? Aug 28, 2026
    Table of Contents: The essence of salt spray testing Electroplating layer thickness Substrate selection Interpretation of test results From standards to practice — recommended testing standards for different handbag categories Industry evolution — environmental regulations and new technologies FAQ Conclusion   1. The Essence of Salt Spray Testing 1.1  What is salt spray testing? Salt spray testing (Salt Spray Test / Salt Fog Test) is an accelerated aging method that simulates corrosive environments under laboratory conditions. Its core principle is that, under controlled temperature, humidity, and salt concentration conditions, corrosion phenomena that would originally take months or even years to appear can be compressed and observed within several hours to several days. It is important to first clarify one point: the results of salt spray testing cannot be directly converted into the actual service life of a product. Corrosion in natural environments is affected by multiple factors, including ultraviolet radiation exposure, temperature cycling, alternating wet and dry conditions, air pollutants (such as SO₂), and mechanical wear. However, the laboratory salt spray environment represents a single condition of continuous moisture and high concentrations of chloride ions. Therefore, the true value of salt spray testing lies in: Process stability verification: Whether hardware components from the same production batch demonstrate consistent corrosion resistance performance; Supplier capability benchmarking: Comparing the protective performance levels of different electroplating factories or different process routes; Defect screening: Quickly identifying manufacturing defects such as coating porosity, poor adhesion, and incomplete pretreatment. 1.2 The Standard System of Salt Spray Testing Neutral Salt Spray (NSS) testing is currently the most widely used testing method in the handbag hardware industry. It mainly follows the following three standard systems: Standard Number Applicable Scope Core Parameters ISO 9227 International standard 5% NaCl, pH 6.5–7.2, 35°C ± 2°C ASTM B117 North American market 5% NaCl, pH 6.5–7.2, 35°C ± 2°C QB/T 3826-1999 China light industry sector 5% NaCl, pH 6–7, 35°C ± 2°C, deposition rate 1–2 mL/80 cm²·h These three standard systems are highly consistent in terms of test environment parameters. The main differences lie in equipment calibration and result recording formats. In handbag OEM/ODM manufacturing, we usually adopt the ISO 9227 testing standard. 1.3 Differentiation of the Three Salt Spray Tests Under the ISO 9227 System ISO 9227 actually specifies three testing methods, with increasing levels of severity: NSS (Neutral Salt Spray): The most basic accelerated corrosion test, suitable for routine quality control of the majority of handbag hardware components. AASS (Acetic Acid Salt Spray): Glacial acetic acid is added to a 5% NaCl solution to reduce the pH to approximately 3.1–3.3. The corrosion rate is about three times that of NSS and is commonly used to evaluate the performance of zinc coatings in mildly acidic environments. CASS (Copper Accelerated Acetic Acid Salt Spray): Copper chloride is added on the basis of AASS, and the test temperature is increased to 50°C. The corrosion rate is approximately eight times that of NSS. It is mainly used for rapid verification of high-end decorative chrome-plated and nickel-plated components. In the daily quality control of handbag hardware, NSS testing remains the absolute mainstream method. AASS and CASS are more commonly used for rapid screening during the introduction of new materials or process changes, rather than for batch shipment inspections.   2. Electroplating Layer Thickness 2.1 Materials and Thickness Classification of Electroplating Layers Electroplating layer thickness is measured in micrometers (μm, 1 μm = 0.001 mm). In the field of handbag hardware, this value directly determines the passing duration of salt spray testing. The industry’s empirical rule is that electroplating thickness has an approximately linear relationship with corrosion resistance time — when the thickness is doubled, the protective lifespan is roughly doubled. Layer Level Material Typical Thickness Function Strike Layer Copper or Nickel 0.5–2 μm Improves substrate adhesion and fills microscopic surface defects Barrier Layer Nickel 1–3 μm Blocks migration of substrate metal ions and provides the primary corrosion protection capability Decorative Layer (Color) Gold / Palladium / Chromium / Imitation Gold 0.1–3 μm Provides surface color and gloss Top Coat Clear coating / Nano ceramic coating 5–15 μm Seals the entire system and protects against sweat, scratches, and oxidation 2.2 Different Thickness Levels Corresponding to Different Testing Standards According to industry practices, the electroplating quality of handbag hardware can be divided into four grades. The differences in coating thickness and salt spray performance are significant: Quality Grade Total Coating Thickness Typical Salt Spray Passing Time Application Scenario Economy Grade <1 μm 16–24 hours Fast fashion, promotional products, internal accessories Mid-range Grade 1–2 μm 24–48 hours Regular product lines of mainstream brands High-end Grade 2.5–5 μm More than 48 hours Designer brands, premium product lines Luxury Grade 5–10+ μm More than 96 hours Top luxury brands such as Hermès and LV Most standard handbags only need to meet a 24–48 hour requirement. However, the specific testing threshold should be dynamically adjusted according to the product’s actual usage environment and application scenario. 2.3 Key Misunderstandings Misunderstanding 1: Focusing only on the thickness of the decorative layer while ignoring the barrier layer Many buyers, when evaluating suppliers, only focus on “how many micrometers thick the surface decorative layer is,” while overlooking the thickness of the nickel barrier layer. In fact, the nickel layer is the core protective barrier against corrosion. If the nickel layer is too thin (<1 μm), even if the decorative layer reaches 1 μm, white rust may still appear within 24 hours during salt spray testing — because the decorative layer itself contains microscopic pores, allowing corrosive media to penetrate through the decorative layer and directly reach the substrate. Misunderstanding 2: Ignoring the protective layer (Top Coat) Clear coating or nano ceramic protective coating acts as the “raincoat” of hardware components. Electroplated parts without a protective layer may still discolor quickly after long-term contact with human sweat (which contains salt and mild acids), even if they pass a 24-hour NSS test. A high-quality protective layer can extend the service life of hardware components by 2 to 5 times. Misunderstanding 3: Confusing “rack plating” and “barrel plating” processes Rack plating suspends individual hardware components on electroplating racks for processing. It provides uniform coating, controllable thickness (typically 0.1–0.5 μm or above), and high surface finish quality, making it the standard process for mid-to-high-end handbags. Barrel plating places large quantities of small components into rotating barrels for batch processing. Collisions between parts can cause microscopic scratches and uneven coating thickness (typically only 0.01–0.05 μm), making it suitable only for concealed components such as rivets and magnetic snaps.   3. Substrate Selection 3.1 Corrosion Characteristics of Three Mainstream Substrates The performance ceiling of an electroplated coating is largely determined by the substrate material. The three commonly used substrates for handbag hardware each have their own advantages and disadvantages: Zinc Alloy (Zamak) Approximately 80%–90% of fashion handbag hardware is manufactured through zinc alloy die casting. Its advantages include good fluidity, ease of achieving complex designs, and moderate cost. However, zinc alloy itself has a porous structure. If the pretreatment process before electroplating (polishing, degreasing, acid cleaning) is not thorough, residual gases and impurities inside the pores may form “plating blisters” after electroplating, becoming the starting points of corrosion during salt spray testing. Brass A preferred substrate material for high-end handbags. Brass has a dense structure, high mechanical strength, and a smaller electrochemical potential difference with plated metals such as nickel and gold, resulting in a lower tendency toward electrochemical corrosion. Classic hardware components from top luxury brands such as Hermès and Chanel often use brass substrates. The disadvantages of brass are its higher density (approximately 15% heavier than zinc alloy at the same volume), higher cost, and the possibility of dezincification if the alloy composition is not properly controlled. After long-term exposure, this may cause pink-colored spots to appear on the surface. Stainless Steel (304/316) The most corrosion-resistant substrate material, especially 316 stainless steel, which performs exceptionally well in marine and high-humidity environments due to its molybdenum content. Stainless steel hardware can usually be used directly without electroplating (such as brushed or mirror-polished finishes), or used as a substrate for PVD (Physical Vapor Deposition) coatings. Its disadvantages include high processing difficulty, limited design flexibility, and higher cost. It is mainly used for functional load-bearing components in luggage and outdoor backpacks.    3.2 Pretreatment: A More Critical Process Than Electroplating Regardless of how high-quality the substrate material is, the electroplating layer will fail if the pretreatment process is inadequate. A standard pretreatment process includes: Mechanical polishing: Removes die-casting burrs and surface oxide layers. The surface roughness must be controlled below 0.4 μm; Ultrasonic degreasing: Removes polishing wax and fingerprint oils; Acid cleaning and activation: Removes microscopic oxide films and increases surface activity; Water rinsing and drying: Prevents cross-contamination. A frequently overlooked detail is that zinc alloy die-cast components require a “cold flow mark” inspection before electroplating. Cold flow marks are surface defects formed when the leading edge of molten metal cools during the die-casting process. They are difficult to detect with the naked eye, but they become obvious dents after electroplating and serve as potential entry points for corrosion.   4. Interpretation of Test Results 4.1 Identification of Failure Modes After salt spray testing, hardware components commonly show three types of corrosion phenomena: White Rust White rust is a corrosion product of the coating itself. It usually appears on the surface of zinc or nickel coatings and presents as white powdery or mist-like deposits. The appearance of white rust indicates that the coating has been penetrated, but the substrate has not yet corroded. During testing, the time point at which white rust appears reflects the density and thickness of the coating. For multi-layer electroplating systems, white rust may appear on the nickel layer surface, indicating that the nickel layer has pores or insufficient thickness. Red Rust Red rust is a corrosion product of the substrate (iron or steel), appearing reddish-brown in color. The appearance of red rust indicates that the entire coating system has completely failed and is considered a serious quality failure. In handbag hardware, if red rust appears on zinc alloy substrates, it is usually accompanied by large-scale coating blistering or peeling. Blistering / Peeling This is a typical manifestation of poor adhesion. Blistering is usually caused by incomplete degreasing during pretreatment or hydrogen embrittlement during the electroplating process. Peeling may be related to excessive internal stress within the coating or insufficient bonding strength between the base layer and the substrate. Components with blistering often develop red rust within a short peri   4.2 ISO 10289 Rating Standard After the test is completed, the corrosion area must be evaluated according to ISO 10289: Rating Corrosion Area Percentage Quality Assessment 10 No defects Perfect 9 ≤0.1% Excellent 8 ≤0.25% Good 7 ≤0.5% Acceptable 6 ≤1% Critical ≤5 >2.5% Unqualified In the actual quality control of handbag hardware, the rating is usually required to be no lower than Grade 7 (corrosion area ≤0.5%), and red rust is not allowed. Some high-end brands’ internal standards require a rating of Grade 9 or above.   5.  From Standards to Practice — Recommended Testing Standards for Different Handbag Categories Product Category Differences Determine Testing Thresholds Different types of handbags face significantly different corrosion risks for their hardware components, and testing requirements should therefore be adjusted accordingly: Backpack Backpack hardware typically includes zippers, buckles, D-rings, and adjustment buckles. Since backpacks are often used in outdoor environments and exposed to rainwater and sweat, it is recommended that the NSS testing baseline should be no less than 24 hours with no red rust and no blistering. For orders targeting tropical markets or marine climate markets, it is recommended to increase the requirement to more than 48 hours. For backpack OEM purchasers with special requirements for hardware corrosion resistance, the testing duration and failure criteria can be clearly defined with the backpack manufacturer during the sampling stage in advance, avoiding disputes caused by unclear standards during mass production. Handbag Handbag hardware is primarily decorative, with functionality as a secondary consideration. It includes components such as locks, chains, bag feet, and magnetic snaps.The usage environment of handbags is relatively mild (mainly indoors), but consumers have extremely low tolerance for visible appearance defects. It is recommended that NSS testing should achieve 24 hours with no visible corrosion spots. For handbag OEM purchasers, chains and locks are key control components for verifying changes during long-term use and wearing conditions, and they should be included as mandatory inspection items for every production batch. Cosmetic Bags & Toiletry Bags The hardware components of cosmetic bags are usually smaller (such as zipper pulls and small fasteners), but the usage environment is relatively harsh — high humidity in bathrooms, chemical ingredients in cosmetics (such as alcohol, oils, and fragrances), as well as mechanical wear caused by frequent opening and closing. For cosmetic bag OEM purchasers, conducting a 24-hour NSS test for cosmetic bags and toiletry bags is a mandatory requirement.   Luggage & Business Bags Hardware components such as telescopic handles, wheel bases, and locks are subject to both mechanical loads and corrosion challenges. Standards such as ISO 9227 provide clear salt spray testing requirements for luggage hardware. In general, a 24-hour NSS test is conducted according to the standard. However, high-end business bag brands often have internal requirements of more than 48 hours.   6 . Industry Evolution — Environmental Regulations and New Technologies 6.1  From Hexavalent Chromium to Trivalent Chromium In traditional electroplating processes, hexavalent chromium (Cr⁶⁺) passivation layers were widely used due to their excellent corrosion resistance. However, hexavalent chromium is classified as a Substance of Very High Concern (SVHC) under the EU REACH regulation and is carcinogenic. Its use in handbag hardware has therefore been strictly restricted. The current industry trend has shifted toward trivalent chromium (Cr³⁺) passivation. Although its corrosion resistance is slightly inferior to hexavalent chromium under certain extreme conditions, equivalent NSS testing performance can be fully achieved by increasing coating thickness and optimizing sealing processes. For bag OEM orders exported to the EU, we recommend that products provide REACH compliance certification. 6.2 PVD: A High-End Alternative to Electroplating Physical Vapor Deposition (PVD) is a process that deposits metallic or ceramic materials onto substrate surfaces in a vacuum environment. Compared with electroplating, PVD coatings have hardness approximately 10 times higher than traditional electroplated coatings, are almost impossible to scratch or fade, and do not require the use of harmful chemical solutions. In the field of handbag hardware, PVD is currently mainly applied to: High-end brand black/gunmetal hardware (such as Hermès “So Black” series); Functional components made from stainless steel substrates; Zippers and fasteners requiring extremely high wear resistance. The limitations of PVD include high equipment investment costs, extremely high requirements for substrate surface smoothness (usually requiring a nickel electroplating base layer and mirror polishing beforehand), and less flexibility in color selection compared with electroplating. Therefore, in the next 5 to 10 years, electroplating will likely remain the mainstream process for handbag hardware, but the penetration rate of PVD will continue to increase.   7.  FAQ Q1. Why must handbag hardware undergo salt spray testing? A:For handbag hardware, salt spray testing is a core method for verifying electroplating quality and predicting long-term product performance in humid climates (such as Southeast Asia and coastal regions). Q2. What are the commonly used salt spray testing standards in the handbag hardware industry? Standard Applicable Scope Notes ASTM B117 North America and international markets The most commonly used neutral salt spray (NSS) reference method ISO 9227 International export certification Covers three methods: NSS, AASS, and CASS GB/T 10125 Chinese national standard Commonly used by domestic and export factories QB/T 3826 Light industrial products (luggage and handbag hardware) Historical standard used in China’s luggage industry EN 1670 European architectural/furniture hardware Classifies corrosion resistance into Grades 1–5 (24h–480h) Q3. What salt spray testing duration is typically required for different handbag hardware positioning levels? The following are common industry references (based on Neutral Salt Spray NSS): Market Positioning Typical Salt Spray Requirement Application Scenario Fast fashion / Entry-level 24 hours or above Indoor dry environments, short-term use Mid-range brands 48 hours or above General urban daily commuting High-end brands 48–72 hours High-humidity climates (such as Florida, Singapore, and Hong Kong) Luxury brands More than 96 hours Long-term durability, coastal markets, heirloom-level quality Q4. Why do different batches show large variations in salt spray test results despite using the same electroplating process? Common reasons include: Inconsistent pretreatment: Differences in polishing quality and incomplete oil/wax removal result in variations in coating adhesion. Coating thickness fluctuations: Copper layer, nickel layer, and decorative layer thicknesses may not meet requirements or may lack uniformity. Substrate differences: Zinc alloy die-cast components may contain sand holes or pores, which become corrosion pathways. Missing post-treatment: Failure to apply sealing agents (Top Coat) or passivation layers increases coating porosity. Testing operation differences: Sample placement angles, chamber loading density, and spray deposition rates are not standardized. Q5. What are the fundamental differences in salt spray performance among zinc alloy, brass, and stainless steel substrates? Substrate Salt Spray Characteristics Zinc Alloy (Zamak) Most cost-effective, but the substrate is highly reactive and relies heavily on the electroplating layer; coating defects easily lead to white rust/red rust Brass The substrate itself has better corrosion resistance than zinc alloy and can maintain longer durability even without plating; suitable for high-end unplated or lightly plated designs Stainless Steel (304/316) The strongest substrate corrosion resistance; can be used directly or only coated with PVD; 316 can achieve 500h+ performance Q6. What are the differences between PVD coatings and traditional electroplating in salt spray testing performance? Traditional electroplating: Relies on a “barrier + sacrificial protection” mechanism through multiple metal coating layers. It has lower cost and more color options, but coatings contain microscopic pores, making salt spray performance highly dependent on process control. PVD coating: Forms a dense ceramic/metal film through vacuum deposition, with extremely low porosity. It generally provides better salt spray resistance and wear resistance; however, color options are more limited, costs are higher, and substrate surface flatness requirements are also very strict. The two processes are not mutually exclusive — high-end hardware often adopts a combined process of “electroplating base layer + PVD top layer.” Q7. Can salt spray testing be directly equated with the actual service life of a product? Answer: No. Salt spray testing is an accelerated comparative test. A 48-hour laboratory test does not equal 48 days of actual use. It is mainly used to: Cmpare corrosion resistance levels of different electroplating systems or suppliers; Verify whether mass production remains consistent with the approved Golden Sample; Screen out obviously defective processes. In actual usage, the effects of wear, sweat, ultraviolet exposure, and temperature cycling on hardware differ from salt spray conditions. Therefore, high-end projects often require additional artificial sweat testing, wear testing, and adhesion testing. Q8. Besides salt spray testing, what other supporting tests are usually required for handbag hardware? Test Type Purpose Common Standards Artificial Sweat Testing Simulates corrosion and discoloration caused by hand contact ISO 3160-2, customer-defined formulas Adhesion Testing Verifies whether coatings are prone to peeling Cross-cut test, tape test, bending test Wear / Friction Testing Evaluates durability during daily contact Reciprocating friction test, RCA tape test Hardness Testing Confirms surface scratch resistance Pencil hardness test, Vickers hardness test Tensile / Torque Testing Verifies mechanical strength of load-bearing hardware (D-rings, lobster clasps) Customer-defined (typically 30–80 kg) Cycle Testing Evaluates repeated opening and closing lifespan of locks and spring clasps 5,000–10,000 cycles   Conclusion The corrosion resistance performance of handbag hardware can never be judged simply by whether it looks shiny or feels heavy. NSS salt spray testing provides a unified comparison benchmark, electroplating thickness provides measurable physical indicators, and the design of multi-layer electroplating systems reflects the depth of a supplier’s manufacturing capabilities. For bag factories and various bag OEM service providers, establishing internal testing capabilities based on ISO 9227 is a necessary investment for improving supply chain competitiveness. For brands and purchasers, when developing technical specifications (Tech Pack), the actual product usage environment should be clearly defined. Based on this, reasonable salt spray testing durations and acceptance criteria should be established to avoid cost waste or quality control failures caused by a “one-size-fits-all” approach.   Author        
  • How to comply with PPWR?
    How to comply with PPWR? Aug 25, 2026
    The EU Packaging and Packaging Waste Regulation (PPWR, Regulation (EU) 2025/40) officially entered into force in February 2025 and has been fully enforced from August 12, 2026, replacing the previous Packaging and Packaging Waste Directive (94/62/EC).   Given that these are brand new regulatory requirements, numerous importers and brand owners are unsure about their specific obligations under PPWR. This article will clarify the key compliance items you need to address.   The regulation introduces stricter full life-cycle compliance requirements for packaging products placed on the EU market, covering material restrictions, packaging design, recyclability, recycled content, labeling, and producer responsibility obligations.   The key requirements include:   I. Restrictions on Materials and Chemical Substances (Mandatory from August 12, 2026)   1. Heavy Metal Limits The total content of four heavy metals — lead (Pb), cadmium (Cd), mercury (Hg), and hexavalent chromium (Cr VI) — contained in packaging materials must not exceed 100 mg/kg.   This requirement applies to all packaging components, including inks, adhesives, coatings, and surface treatments.   2. PFAS Restrictions For food-contact packaging, the use of per- and polyfluoroalkyl substances (PFAS) is strictly restricted.   The requirements include: • Total fluorine content: ≤ 50 ppm  • Non-polymeric PFAS substances: ≤ 25 ppb  • Total PFAS content: ≤ 250 ppb    II. Packaging Design and Waste Reduction Requirements (Phased Implementation)   1. Packaging Minimization and Waste Reduction Packaging must be designed to achieve the minimum volume and weight necessary to ensure its intended function, while avoiding excessive packaging.   Starting from January 1, 2030, the empty space ratio of e-commerce packaging and transport packaging must not exceed 50%.   2. Recyclability Requirements From January 1, 2030, packaging placed on the EU market must meet defined recyclability standards.   Packaging will be classified into different recyclability grades: • Grade A: ≥ 95% recyclable  • Grade B: ≥ 80% recyclable  • Grade C: ≥ 70% recyclable    Packaging below Grade C will gradually be prohibited: • Grade C packaging will be banned from 2030  • Grade B packaging will be banned from 2038    3. Minimum Recycled Content Requirements From January 1, 2030, plastic packaging must contain a minimum percentage of post-consumer recycled material (PCR).   Examples: • Food-contact PET packaging: minimum 30% PCR content (increasing to 50% by 2040)  • Other plastic packaging: minimum 35% PCR content (increasing to 65% by 2040)    4. Restrictions on Specific Packaging Types Starting from January 1, 2030, certain single-use plastic packaging formats will be prohibited, including: • Lightweight plastic bags  • Single-use plastic packaging components  • Single-use miniature packaging used in hotels and catering industries  • Small single-use fruit and vegetable packaging  • Other unnecessary disposable plastic packaging formats    III. Labeling and Information Disclosure Requirements (Phased Implementation)   1. Standardized Packaging Labels From August 12, 2028, packaging must display standardized labeling requirements.   Labels must clearly indicate: • Material composition  • Recyclability level  • Waste sorting instructions    The EU will gradually introduce unified digital labeling systems, including QR-code-based information disclosure.   2. Compostability Identification Packaging labeled as “industrially compostable” must clearly indicate this information to prevent consumers from incorrectly disposing of packaging waste and contaminating recycling streams.   IV. Compliance and Registration Requirements (Mandatory from August 12, 2026)   1. Extended Producer Responsibility (EPR) Registration All entities placing packaging products on the EU market, including: • Manufacturers  • Importers  • E-commerce sellers  Must complete EPR registration in each applicable EU member state and pay corresponding waste collection and recycling fees based on packaging volume and weight.   Non-EU companies must appoint an authorized representative within the EU to fulfill relevant compliance obligations.   2. Declaration of Conformity (DoC) Companies must prepare an EU Declaration of Conformity (DoC) and maintain supporting technical documentation, including: • Test reports  • Compliance assessment records  • Packaging evaluation documents    These documents must be retained for inspection by customs authorities and market surveillance agencies.   Note: EPR registration systems, fee structures, and enforcement procedures may vary between EU member states. Companies must complete compliance procedures separately according to the specific requirements of each destination country.     Author        
  • Why Ripstop Fabric is More Tear Resistant for Bags?
    Why Ripstop Fabric is More Tear Resistant for Bags? Aug 23, 2026
    Because of its crosshatch grid weaving, Warp & Weft Reinforcement Threads of Ripstop Fabric Enhance Tear Resistance for Bags.   "Why do some bag fabrics tear apart at the slightest pull, with the rip spreading like a zipper, while others contain damage to a minimal area even when scraped by sharp rocks?"   This is a question we frequently hear from our global B2B clients. Often, the answer lies not in how thick the fabric is, but in its weaving structure.   In ordinary plain-weave fabrics, once a yarn breaks, stress instantly transfers to adjacent yarns, triggering a chain reaction—the rip spreads like a zipper. Ripstop fabric, on the other hand, has built-in tear resistance. It does not rely on 'added thickness' for strength, but rather on a warp-and-weft bidirectional reinforcement thread weaving structure that prevents tear propagation.   Today, we will explore the weaving principles behind ripstop fabric and analyze how warp and weft reinforcement threads give bags exceptional tear resistance.   I What Is Ripstop Fabric? 1.1 Definition & Structural Characteristics Ripstop fabric is a functional textile in which high-strength reinforcement threads are interwoven at regular intervals over a base weave.   1.2 Fundamental Differences from Ordinary Oxford Fabric What sets ripstop Oxford apart from standard Oxford? The core difference lies in structure. Here is a detailed comparison:   Feature Standard Oxford Ripstop Fabric Tear-Resistance Mechanism Relies on yarn strength alone Structural reinforcement threads intercept rips Rip Propagation Spreads rapidly Contained within the grid Weight Similar at equivalent denier Almost no additional weight Visual Feature Smooth surface Visible grid texture     II How this Weaving works: Warp & Weft Reinforcement Threads Work The tear resistance of ripstop fabric stems from its precision-engineered weaving structure. Here is the technical breakdown:   2.1 Base Weave: Plain or Basket Weave Ripstop fabric uses plain weave (1×1) or 2×2 basket weave as its foundation. At regular intervals in both the warp (longitudinal) and weft (transverse) directions, thicker, stronger high-denier filaments are inserted. These reinforcement threads create a clearly visible texture on the fabric surface. Plain weave is the most basic interlacing method—warp and weft yarns cross one-over, one-under, creating a stable, uniform fabric structure. Some high-end specifications use 2×2 basket weave, where two warp yarns interlace with two weft yarns simultaneously, producing a tighter, more abrasion-resistant surface while maintaining good hand feel.   2.2 Reinforcement Thread Insertion: Bidirectional Locking This is the core of ripstop technology. During weaving, reinforcement threads are inserted at fixed intervals in both directions: • Warp Ripstop Thread: Along the fabric length (longitudinal direction), a higher-denier high-strength filament is inserted at intervals of every 5 mm, 7 mm, or 10 mm. • Weft Ripstop Thread: Along the fabric width (transverse direction), reinforcement threads are also inserted at fixed intervals. These reinforcement threads are woven simultaneously with the base yarns, forming a bidirectional grid structure. When a tear occurs, the rip edge first encounters these 'high-strength barriers.'   2.3 Grid Spacing Selection There are three mainstream grid specifications on the market:   Grid Spacing Tear Resistance Hand Feel / Stiffness Recommended Bag Types 5 mm ★★★★★ Stiffer Tactical packs, tool bags, industrial bags 7 mm ★★★★☆ Balanced Outdoor hiking packs, travel bags 10 mm ★★★☆☆ Softer Daily commuter backpacks, storage pouches   Selection Tip: The smaller the grid spacing, the stronger the tear resistance, but the hand feel and softness will decrease slightly. We can recommend the optimal solution based on the end-use scenario and tactile requirements.   2.4 Denier & Material of Reinforcement Threads • Polyester Reinforcement: Lower cost. Standard polyester suits medium-strength applications; high-tenacity polyester achieves higher strength grades. • 210D Nylon Reinforcement: Commonly used in 210D–420D ripstop fabrics. It balances tear performance, fabric appearance, and cost—an industry-standard, high-value specification. It can also be used for lower-denier base fabrics depending on performance needs. • 420D Nylon Reinforcement: Used in 420D and above mid-to-high-denier ripstop fabrics to significantly improve tear strength. For 600D+ heavy-duty fabrics, 420D or higher-denier reinforcement threads can be selected. For extreme strength, high-performance fibers such as high-tenacity polyamide, aramid, or UHMWPE are available.   III Tear-Resistance Mechanics: Why Rips Don't Spread To understand how ripstop fabric works, we must compare its failure mode with that of ordinary fabric.   3.1 "Zipper Tear" in Ordinary Fabric In standard plain-weave fabric, all yarns have uniform strength. When external force causes one yarn to break, stress instantly transfers to adjacent yarns. Because neighboring yarns have the same strength, they cannot withstand the sudden load increase, leading to a chain fracture—the rip spreads like a zipper, causing large-scale damage.   3.2 "Grid Interception" Mechanism in Ripstop Fabric Ripstop fabric solves this problem through mechanical discontinuity design: Rip Initiation: External force causes base yarns to break, and the rip begins to spread. Encountering Reinforcement Threads: When the rip reaches the grid line where reinforcement threads lie, the thicker, tougher threads absorb and redistribute the stress. Stress Dispersion: The reinforcement threads disperse the concentrated tearing stress over a larger area of the fabric, preventing single-point overload. Rip Arrest: Because the reinforcement threads are far stronger than the base yarns, the rip is 'intercepted' within a single grid cell and cannot cross the grid boundary to continue spreading.   3.3 How Much Does Tear Strength Improve When Switching from Standard Oxford to Ripstop at Equivalent Density? Based on ASTM D2261 tear strength testing standard (Elmendorf Tear Test), laboratory measurements compared standard Oxford and ripstop Oxford of the same denier:   Fabric Spec Standard Oxford Tear Strength Ripstop Tear Strength Improvement 210D Nylon ~25 N ~35–42 N +40%–68% 420D Nylon ~35 N ~50–60 N +43%–71% 600D Polyester ~30 N ~42–50 N +40%–67%   Note: Actual data varies depending on weaving density, finishing processes, and test conditions. The above figures are for reference only.    IV Ripstop Fabric Specification Guide for Bag Manufacturing If you are looking to customize bags, how do you choose the most suitable ripstop fabric specification? Here is a summary based on our 30 years of manufacturing experience:   4.1 Recommendations by Bag Type   Bag Type Recommended Spec Grid Spacing Key Considerations Ultra-Light Foldable Pouch 20D–70D Nylon Ripstop 10 mm Weight priority; adequate tear strength Daily Commuter Backpack 210D Ripstop Oxford 7–10 mm Best value; balances durability and hand feel Outdoor / Hiking Backpack 210D–420D Ripstop Nylon 5–7 mm High load-bearing, high abrasion resistance Tactical / Military Pack 420D–600D Ripstop Nylon 5 mm Extreme durability; compatible with MOLLE systems Tool Bag / Industrial Bag 600D–1000D Ripstop + PU Coating 5 mm Maximum durability + waterproof + UV resistance Travel Case / Luggage Outer 420D–840D Ripstop Nylon 5–7 mm Impact and scratch resistance   4.2 Material Selection: Polyester vs. Nylon   Property Polyester (PET) Nylon (PA) Strength Good; slightly lower than nylon Higher; excellent abrasion resistance Moisture Absorption Lower; quick-drying Higher; softer touch Weather Resistance Naturally better UV resistance Requires additional UV treatment Cost Lower Higher Typical Applications Daily backpacks, promo bags, linings Premium outdoor bags, tactical bags   Our Recommendation: If your end product targets the mid-to-high-end outdoor or professional market, prioritize nylon ripstop. If you are aiming for cost efficiency and quick-dry performance, polyester ripstop is the ideal choice.   V What Additional Finishing Processes Can Be Applied to Ripstop Fabric? Ripstop weaving solves structural strength, while finishing processes add further functionality.   5.1 PU / PVC Coating & TPU Lamination for Waterproofing Applying polyurethane (PU) coating or thermoplastic polyurethane (TPU) film lamination on the fabric backside significantly improves waterproof performance: • PU Coating: Lower overall cost. Polyester-based PU has poor hydrolysis resistance; polyether-based PU offers relatively better hydrolysis resistance. • TPU Film Lamination: TPU also comes in polyester and polyether types—selection must be differentiated. Compared to standard PU, polyether-based TPU offers superior hydrolysis resistance, and solvent-free systems are more environmentally friendly. It is commonly used in premium product lines. • PVC Coating: Excellent waterproofing, puncture resistance, and weather durability. However, the coating adds noticeable weight and gives the fabric a stiffer hand feel. Additionally, environmental regulations restrict its use in certain applications.   5.2 DWR (Durable Water Repellent) Treatment A fluorocarbon-based surface treatment causes water droplets to bead up and roll off rather than penetrate. Suitable for outdoor bags requiring 'water repellency' rather than 'full waterproofing.'   5.3 UV Resistance Treatment Nylon fibers degrade and become brittle under prolonged UV exposure. UV-resistant finishing agents delay fiber aging and extend fabric lifespan—especially important for camping storage bags and outdoor backpacks exposed to sunlight for extended periods.   5.4 Flame-Retardant Treatment Compliant with NFPA 701, CPAI-84, and other flame-retardant standards. Suitable for industrial safety bags, firefighter equipment bags, and other specialized industry requirements.   Through post-processing, ripstop fabric can achieve not only structural tear resistance but also synchronized functional goals—better meeting clients' needs for product differentiation.   VI Frequently Asked Questions (FAQ) Q1: Is smaller grid spacing always better for ripstop fabric? A: Not necessarily. When base yarn and reinforcement thread denier remain constant, smaller grid spacing means higher reinforcement thread density and better tear resistance. However, smaller grids increase weaving complexity and cost. Selection should balance performance, hand feel, and cost. Industry reference: daily backpacks typically use 7–10 mm grids; professional outdoor and tactical products commonly use 5 mm grids.   Q2: How do I choose between nylon and polyester ripstop? A: Nylon offers higher strength, better abrasion resistance, and a softer hand feel—ideal for mid-to-high-end outdoor and tactical bags. Polyester is lower in cost, dries faster, and has naturally superior UV resistance—ideal for daily backpacks and promotional products. We can recommend the optimal solution based on your budget and target market.   Q3: Is ripstop fabric fully waterproof? A: Ripstop weaving itself does not provide waterproofing. For waterproof performance, PU coating or TPU lamination must be added. For example, 210D ripstop nylon with PU coating typically achieves 5,000 mm hydrostatic pressure, allowing the fabric itself to withstand moderate to heavy rain. However, for a fully rainproof finished product, seam taping is also required to prevent water ingress through needle holes.   Q4: Which B2B industries are suitable for ripstop bags? A: The applicable B2B client range is broad, including: outdoor gear brands, tactical equipment suppliers, travel goods companies, tool bag brands, industrial safety equipment manufacturers, pet product brands, and any other clients requiring high-abrasion, tear-resistant storage bags. Different industries have varying requirements for tear resistance, fabric denier, waterproof coating, and grid specifications. One important note: ripstop structure can only delay rip propagation; it does not equal bite resistance. Pet product applications require targeted evaluation.   Q5: Are reinforcement threads placed in the warp or weft direction? One side or both? A: Standard ripstop fabric embeds reinforcement threads in both warp and weft directions, forming a grid structure for balanced tear resistance. Low-cost unidirectional ripstop fabrics exist with reinforcement in only one direction, offering limited tear resistance suitable only for lightweight storage pouches. For backpacks, tool bags, and outdoor bags, bidirectional reinforcement is strongly recommended.   Q6: Are thicker reinforcement threads always better? Does higher denier mean better tear resistance? A: Not necessarily. Overly thick reinforcement threads cause fabric bulging, stiff hand feel, increased weight, and excessive bag rigidity. A balanced rule of thumb: reinforcement thread denier ≥ base fabric denier, typically 1–2× the base fabric denier for optimal balance. Tear resistance depends not only on denier but also on grid spacing, material (nylon/polyester), and weave density.   Q7: Why does ripstop fabric feel soft in some cases and stiff in others? A: Hand feel differences come from three main factors: (1) Reinforcement thread thickness—thicker threads create stiffer fabric; (2) Grid size—smaller grids with more intersection nodes feel stiffer; (3) Finishing / coating—PU/TPU coatings significantly increase stiffness. Lightweight bags suit fine reinforcement threads with small grids; heavy-duty tool bags and tactical bags suit thick reinforcement threads with medium grids.   Q8: How can I quickly tell if a fabric is genuine ripstop? A: Three simple on-site checks: (1) Look at the fabric surface—does it have a uniform grid pattern? (2) Feel the intersection nodes—are there thicker reinforcement thread bumps at the grid crossings? (3) Make a small tear—does the rip get stopped by the grid and fail to spread?   VII Conclusion The core value of ripstop fabric lies in its use of structural design rather than simply 'adding bulk and weight' to solve bag tearing issues. The grid formed by warp and weft reinforcement threads acts like a 'safety line' within the fabric—intercepting rips when they appear and containing damage to the smallest possible area.   If you are looking for a reliable ripstop bag manufacturing partner, we welcome you to contact us: • Request free fabric swatch cards and technical parameter sheets • Consult on customized fabric solutions and quotations • Schedule factory visits and sample confirmations     Author        
  • What Is Bar Tack Stitching and Why Is It Important for Backpack OEM?
    What Is Bar Tack Stitching and Why Is It Important for Backpack OEM? Aug 19, 2026
    Bar tack stitching, also known as tack stitching or bartacking, is a reinforcement technique that uses dense back-and-forth stitching at stress points to create a highly secure locking stitch structure. It acts as a reinforced locking point for every major load-bearing area of a backpack.   Standard lockstitch seams mainly provide basic assembly. When a backpack carries weight, pulling forces concentrate along individual stitch lines, eventually causing seam failure, delamination, or tearing. Bar tack reinforcement distributes these forces through dense stitch patterns and firmly secures the joining areas, providing 3–5 times higher tensile strength than standard stitching.   Many customers wonder why backpacks made with the same materials and thickness can have completely different service lives. Some lose shoulder straps or develop torn corners after only six months, while others remain durable for years.   The difference is not only the fabric — it lies in the bar tack reinforcement process.   For backpack OEM projects, understanding bar tack reinforcement is not only essential for quality control but also a fundamental factor in product durability and brand reputation. This guide explains the load distribution logic, critical reinforcement locations, and proper bartacking methods for different backpack components.   Contents Ⅰ. Why Do Backpacks Require Bar Tack Reinforcement? Ⅱ. Three Main Sources of Backpack Stress Ⅲ. Common Backpack Bar Tack Reinforcement Areas Ⅳ. Four Key Principles of Proper Bar Tack Execution Ⅴ. Bar Tack Configurations for Different Backpack Applications Ⅵ. FAQ Ⅶ. Conclusion   Ⅰ. Why Do Backpacks Require Bar Tack Reinforcement? Standard lockstitch seams create a straight stitching line. Once a backpack is loaded, gravity, movement, and twisting forces are concentrated on this single line, causing repeated stress that eventually leads to loose threads, broken seams, and fabric separation.   The purpose of bar tack stitching is simple: distribute concentrated tension across a larger stitched area and lock the connection point securely through dense repeated stitching.   Standard stitching = basic joining.   Bar tack reinforcement = structural locking.   Properly applied bartacking can achieve 3–5 times the tensile strength of standard stitching based on ASTM D5034 breaking strength comparison testing, greatly reducing the risk of tearing, cracking, and seam failure.   Ⅱ. Three Main Sources of Backpack Stress Backpack damage usually comes from three types of forces:   1. Static Load Stress When carrying heavy items, gravity pulls downward vertically. The stress concentrates around shoulder strap anchors and hip belt attachment points, which are the main causes of shoulder strap failure.   2. Dynamic Pulling Forces During walking, running, or climbing, backpacks experience vertical bouncing, lateral pulling, and twisting movements. Instant dynamic forces can reach 2–3 times the static load. Areas such as corners, handle bases, attachment points, and zipper ends are repeatedly stressed and may fail without proper reinforcement.   3. Long-Term Wear and Fatigue Corners, webbing edges, and seams constantly rub against clothing, walls, and surfaces. Over time, stitches loosen and wear down, eventually causing fraying, thread separation, and small tears. Preventive bartacking helps reduce these hidden risks.   Ⅲ. Common Backpack Bar Tack Reinforcement Areas Bar tack stitching is a critical reinforcement process in bag manufacturing. By creating dense repeated stitches at high-stress locations, it forms reinforced zones that prevent tearing.   As a backpack factory with 30 years of manufacturing experience, we classify common bartacking locations according to functional areas:   1. Shoulder Straps (Primary Load-Bearing Area)   Location Bar Tack Position Functional Purpose Shoulder strap root Junction where shoulder straps attach to upper back panel of backpack body Bears total pack weight; mandatory bar tack zone Lower shoulder strap end Connection between bottom/side gusset and shoulder strap base Prevent strap pull out from lower attachment Strap adjuster anchorage Sewing joints for slide buckles and ladder lock buckles to webbing Resist frequent cyclic pulling; prevent buckle detachment   2. Handles (Hand-Carrying Stress Points)   Location Bar Tack Position Functional Purpose Top carry handle root Sewing joints between handle webbing and top lid/rear panel  Absorb concentrated force during manual lifting Side / vertical carry handles  Connection points of side mounted handles to main body Resist vertical tension; avoid side panel tearing   3. Suspension System (Supporting Load Transfer)   Location Bar   Tack Position Functional Purpose Hip belt anchor points Sewing joints between hip belt buckles and hip belt webbing High stress zones during load weight transfer Chest stabilizer strap Attachment joints of chest strap buckles to shoulder straps Withstand frequent dynamic pulling during movement Back panel mounting points Sewing interfaces between back panel frame and main backpack body Structural joint reinforcement   4. Zippers (Opening Reinforcement)   Location Tack  Tack Position Functional Purpose Zipper head end Origin end of zipper track (slider rest position) Prevent zipper slider from pulling out of track channels Zipper tail end  Terminal stop end of zipper assembly Avoid zipper track separation and blow out at tail stop   5. External Attachments and Hardware   Location Bar Tack Position Functional Purpose Buckle attachment joints Sew in anchor points for buckles onto pack body Primary load bearing points for externally hung accessories Webbing loops / daisy chains External daisy chain webbing mounted on shoulder straps Individual bar tack for each loop to guarantee independent load bearing capacity Side compression strap anchorages Sewing joints for side compression straps to main body Counteract transverse tension generated during strap tightening   6. Special Functional Areas   Location Bar Tack Position Functional Purpose Hydration tube port / earphone cable port Perimeter reinforced stitching around cut out openings Prevent progressive tearing and enlargement of apertures in service Reflective strips / brand logo patches End anchorage stitching for decorative trims onto pack body Resist pull off forces acting on decorative components Internal hanging points / key leash anchorages Sew in joints for key hook webbing Avoid detachment caused by weight of carried keys Ⅳ. Four Key Principles of Proper Bar Tack Execution Standard compliant bar tack stitching must follow four key principles:   1. Precise Placement Bar tacks must accurately cover the joining area between webbing and fabric. Misalignment reduces reinforcement effectiveness and wastes production effort.   2. Strength Grading High-load areas require denser and larger reinforcement, while low-stress areas need lighter reinforcement. This balances durability, weight, and production efficiency.   3. Correct Thread Selection Heavy fabrics and load-bearing backpacks usually require high-strength polyester thread (minimum No. 40 recommended). Lightweight products should use suitable medium-weight threads. Threads that are too thin may break easily, while overly thick threads can damage fabric or create wrinkles.   4. Symmetrical Balance Corresponding left and right reinforcement points must maintain consistent construction. Uneven reinforcement can cause unbalanced loading, deformation, and premature wear.   Ⅴ. Bar Tack Configurations for Different Backpack Applications 1. Lightweight Commuter Backpacks Focus reinforcement on shoulder strap anchors, attachment points, and bottom areas. Secondary areas can use simplified construction to balance lightweight design, durability, and cost.   2. Outdoor Hiking Heavy-Duty Backpacks All major load-bearing points should use premium double bartacking. Bottom panels and external attachment areas require reinforced density to withstand long-term heavy loads, rough terrain, and impact.   3. Tactical Functional Backpacks All external webbing, loops, and attachment points require enhanced reinforcement. Frequently used functional areas should receive additional bartacking for accessory mounting and high-intensity applications.   Ⅵ. Frequently Asked Questions Q1: Does more bar tack stitching always mean a stronger backpack? No. Excessive bartacking can make fabric areas unnecessarily thick and stiff while increasing weight and cost. The correct approach is graded reinforcement: dense reinforcement for high-stress areas and lighter reinforcement for low-stress areas.   Q2: What is the difference between polyester thread and nylon thread? Which one is preferred for bar tack work? Polyester thread offers UV resistance and excellent aging performance, making it the mainstream choice for outdoor and commuter backpacks. Nylon thread provides greater elasticity and impact resistance but costs more, making it suitable for tactical and extreme-load applications.   Q3: How can you quickly judge whether a backpack has good bartacking quality? Check three points: 1. Whether shoulder strap connections use box-X or double reinforcement bartacking. 2. Whether webbing is embedded into the fabric layers before bartacking instead of simply stitched onto the surface. 3. Whether symmetrical reinforcement points are consistent and free from cost-cutting practices.   Q4: Can bartacking repair an already damaged backpack? It can provide partial repair, but it cannot fully restore original factory strength if the webbing or fabric has already been damaged. The most reliable solution is proper reinforcement during initial production.   Q5: Do lightweight backpacks also need bartacking? Yes, but with a different approach. Ultralight backpacks should use smaller, lightweight bartacks at critical stress points to maintain tear resistance without compromising fabric flexibility or weight control.   Ⅶ. Conclusion The principle of bar tack reinforcement is simple: reinforce where stress is highest, and lock edges precisely where wear occurs.   As an OEM/ODM manufacturer specializing in customized bag solutions, Synberry develops reinforcement structures based on real-world load conditions. We avoid unnecessary process complexity while maintaining essential reinforcement standards.   For commuter, outdoor, and tactical backpacks, we provide customized bartacking solutions covering reinforcement placement, stitch specifications, and quality control standards, meeting global premium manufacturing requirements.   If you require backpack customization, manufacturing upgrades, pattern optimization, or sampling and mass production services, contact Synberry. We provide tailored reinforcement solutions based on product positioning, application scenarios, and budget, controlling every stress point to improve durability, reduce after-sales issues, and strengthen product competitiveness in global markets.     Author        
  • DWR Coating vs PU Lamination vs TPU Composite: What Is the Best Fabric for Waterproofing?
    DWR Coating vs PU Lamination vs TPU Composite: What Is the Best Fabric for Waterproofing? Aug 13, 2026
    In bag procurement and product development, “waterproofing” is one of the most frequently mentioned yet most easily misunderstood performance indicators. End consumers often use “whether it is waterproof” as the key criterion for judgment, but professional bag manufacturers understand that waterproof performance is actually a graded spectrum — ranging from surface treatments that can only resist minor splashes to composite barriers capable of withstanding water immersion. Different processes correspond to completely different technical approaches, cost structures, and application scenarios.   Currently, the three most widely used waterproof finishing technologies in the bag industry are: DWR Durable Water Repellent Coating, PU Polyurethane Coating/Lamination, and TPU Thermoplastic Polyurethane Lamination.   They are not simply a linear hierarchy of “good” and “better.” Instead, each technology represents a different solution with its own trade-offs among waterproof rating, breathability, hand feel, durability, and cost. For backpack OEM buyers, understanding the fundamental differences between these three technologies is essential for developing reasonable product specifications, controlling costs, and meeting end-user expectations.   This article will provide a systematic comparison of these three waterproof finishing technologies from three perspectives: process principles, performance data, and manufacturing practices, offering an objective reference for material selection decisions in the bag industry. Table of Contents: Process Principles  Performance Data Comparison  Selection Recommendations for Bag Manufacturing  Waterproof Performance Testing Standards and Interpretation  Frequently Asked Questions  Conclusion    Ⅰ.  Process Principles 1.1  DWR Coating 1.1.1 Technical Principle: Making Water Droplets “Stand” on the Fabric DWR (Durable Water Repellent) is a chemical finishing process applied to the surface of fabric, rather than a structural waterproof layer. It works by changing the surface tension characteristics of the fibers, causing water molecules to form droplets on the surface of the fabric and roll off, rather than wetting and penetrating into the gaps between the yarns.   It is important to clarify that DWR does not make the fabric waterproof. It cannot prevent water penetration under continuous water pressure, nor can it seal the pores of the textile itself. A canvas or nylon fabric treated only with DWR typically achieves a hydrostatic head value of just 300–600 mm in the Hydrostatic Head Test, which means it can only cope with light splashes or brief periods of drizzle. 1.1.2 Core Advantages: Lightweight, Breathability, and Quick Drying The core advantage of DWR lies in the fact that it has almost no impact on the original properties of the fabric. Since the coating is extremely thin (typically at the micron level), the fabric’s hand feel, softness, breathability, and weight are barely affected. For foldable bags, lining materials, or summer commuter backpacks that pursue an “ultralight” design, DWR is an ideal choice. It can also significantly reduce the amount of moisture absorbed by the fabric, allowing the bag to dry faster in humid environments and reducing the burden caused by increased weight as the fabric absorbs water.   In the production practice of Outdoor Waterproof Backpack OEM, DWR is often used as the “first layer of protection.” It reduces the amount of water reaching the underlying waterproof barrier, thereby indirectly extending the service life of the PU or TPU waterproof layer. For example, in an outdoor backpack featuring a three-layer construction of “ripstop nylon + DWR surface + PU backing,” the presence of DWR means that the PU coating does not have to bear the full impact of surface moisture on its own.   1.1.3 Limitations: Durability Bottlenecks and Maintenance Costs The biggest drawback of DWR is its durability. As time goes by, dirt, oils, detergent residues, and repeated bending and abrasion on the fabric surface can all damage the hydrophobic molecular layer of DWR. Consumers often have this experience: when a backpack is new, water droplets roll off it like water on a lotus leaf in the rain, but after six months of use, the fabric begins to become wet and absorb water. This does not mean that the fabric is “leaking”; rather, the failure of the DWR treatment allows water to directly wet and penetrate the interior of the textile.   Maintaining DWR requires end users to periodically reapply a DWR restoration treatment, which increases the product’s overall cost of use to some extent. For brands, this means that the limitations of DWR need to be clearly explained in the product instructions to avoid a gap between “waterproof” claims and actual performance.   1.1.4 Environmental Transition: The Shift from C8 to C0 and Fluorine-Free Formulations The DWR industry is undergoing a profound environmental transformation. Traditional DWR formulations were often based on fluorinated compounds (PFAS), such as C8 or C6 fluorocarbon chains. These substances are extremely chemically stable and are known as “Forever Chemicals.” They can accumulate in the environment and living organisms, raising serious ecological and health concerns.   EU REACH regulations, restrictions imposed by the U.S. EPA, and the sustainability commitments of major outdoor brands are driving the transition from fluorinated DWR formulations to fluorine-free formulations (C0 or PFAS-free). Fluorine-free DWR treatments are based on hydrocarbons or siloxanes. Although they are somewhat inferior to traditional fluorinated products in terms of oil and grease resistance and long-term durability, they are now capable of meeting the requirements of most bag applications. 1.2  PU Lamination 1.2.1 Technical Principle: Sealing Fabric Pores by Converting Liquid into a Solid PU (Polyurethane) lamination is the most widely used waterproof finishing process in the bag industry. Unlike the surface treatment provided by DWR, PU waterproofing involves directly applying a liquid PU coating to the back side (reverse side) of the fabric. After the coating cures, it forms a strong yet flexible polymer film that adheres to the textile substrate. This PU film fills the gaps between the interlaced points of the fabric, thereby preventing liquid water from penetrating through.   The thickness of a PU coating is typically measured by “coating weight” or “wet film thickness.” The greater the coating weight, the stronger the waterproof performance; however, the fabric will also become correspondingly stiffer and heavier. A piece of 210D nylon combined with a standard PU coating (approximately 30 g/m²) can typically achieve a hydrostatic head value of 1,000–2,000 mm, which is sufficient to handle moderate rain in everyday commuting environments. 1.2.2 Core Advantages: The Balanced Choice in Terms of Performance The reason PU lamination has become the mainstream choice in the industry is that it achieves an “acceptable balance” across multiple key performance indicators: Waterproofing: PU coating provides a substantial waterproof barrier, far exceeding the water-repellent effect of DWR. For travel backpacks, everyday commuter bags, and general outdoor bags, PU-coated fabric offers an optimal balance between cost and performance. Hand Feel and Processability: Fabric with a PU coating still retains a certain degree of softness and offers good sewability and processing performance. Cost: The additional cost of PU coating is relatively moderate and is significantly lower than that of TPU lamination. Supply Chain Maturity: At the same time, PU lamination is supported by mature production processes, low supply-chain barriers, readily available stock, and more controllable lead times, making it highly suitable for production planning for large-volume orders. 1.2.3 Limitations: Insufficient Durability and Breathability However, PU coating also has several significant drawbacks that cannot be overlooked: Hydrolysis Risk: The ester bonds in the PU molecular chains are susceptible to moisture attack in hot and humid environments, resulting in a hydrolysis reaction. This can cause the coating to powder, peel off, or become sticky. The severity of this issue is closely related to the PU formulation (polyether-based vs. polyester-based), the temperature and humidity of the operating environment, and storage conditions. Reduced Breathability: While PU coating seals the pores of the fabric, it also significantly reduces the fabric’s water vapor transmission rate. Low-Temperature Embrittlement: Traditional PU gradually becomes harder in low-temperature environments and, in extreme cases, the coating may crack. This represents a potential risk for backpacks intended for outdoor use during winter.   1.3  TPU Composite 1.3.1 Technical Principle: A Seamless Barrier Made from Thermoplastic Elastomer TPU (Thermoplastic Polyurethane) composite technology represents a higher level of waterproofing technology for bag fabrics. Unlike the “coating and film-forming” process used for PU coating, TPU lamination involves firmly bonding a pre-formed TPU film to the fabric substrate through hot-melt adhesive or heat-pressing, creating an independent, continuous, and uniformly thick waterproof barrier.   TPU itself is a block copolymer that combines the high elasticity of rubber with the processability of plastic. The hard segments in its molecular chains (composed of diisocyanates and chain extenders) provide strength and temperature resistance, while the soft segments (composed of long-chain polyols) provide flexibility and elasticity. This unique structure allows TPU film to remain flexible across a very wide temperature range (-40°C to +80°C), without becoming brittle at low temperatures or softening and becoming sticky at high temperatures like PU coatings can. 1.3.2 Performance Advantages: Comprehensive Protection at a Higher Level Superior Waterproofing: TPU composite fabrics typically achieve a hydrostatic head value of 3,000–5,000 mm, or even higher, making them capable of withstanding extreme conditions such as heavy rain and water immersion. For diving bags, canyoning bags, water sports equipment, and high-end outdoor backpacks, TPU lamination provides the technical foundation for achieving “true waterproofing” rather than simply “rain resistance.” Excellent Durability: TPU offers significantly better resistance to hydrolysis, UV exposure, oils, and chemicals than PU. Weldability: The thermoplastic properties of TPU allow seamless connections to be achieved through High-Frequency (HF) Welding or Hot Air Welding. This means that a bag factory can manufacture completely needle-hole-free waterproof bags, elevating waterproof performance from the “fabric level” to the “structural level.” Elasticity and Hand Feel: TPU film has a lower elastic modulus than PU coatings. Therefore, even after lamination, the fabric can maintain high strength while retaining good flexibility and resilience. 1.3.3  Limitations: Cost and Processing Challenges The main drawbacks of TPU lamination are concentrated in its cost and manufacturing complexity. Material Cost: TPU film itself is more expensive than PU resin. Combined with the equipment investment and energy consumption required for the lamination process, TPU laminated fabric typically costs 1.5 times or more than PU-coated fabric of the same specification. For bags targeting price-sensitive mass markets, this cost increase may directly determine the product’s market positioning. Higher MOQ: There are very few standard TPU specifications available from stock, and most require customization. Except for standard black and white colors, which can be customized with a relatively low MOQ, other colors generally have a minimum order quantity of around 1,000 yards. Processing Requirements: TPU laminated fabrics have more demanding sewing requirements. When pierced by a needle, TPU film is prone to the “needle-hole effect.” Although the needle holes themselves are very small, they can become pathways for water penetration under high water pressure. Therefore, Backpack OEM orders using TPU fabric usually need to incorporate seam tape or welding processes to seal the needle holes. Breathability Limitations: Although TPU can be manufactured into microporous breathable films (using a principle similar to Gore-Tex), most TPU laminated fabrics used for bags employ dense, non-microporous films in order to maximize waterproof performance. This means their breathability is generally lower than that of PU-coated fabrics, resulting in a higher risk of condensation forming inside the bag.   II. Performance Data Comparison of the Three Waterproofing Processes To provide a more intuitive understanding of the differences among the three processes, the following table presents a quantitative comparison across multiple key dimensions: Comparison Dimension DWR Coating PU Lamination TPU Composite Waterproofing Level Water Repellent (IPX2) Rain Resistant (IPX3–IPX4) Waterproof (IPX5 and above) Hydrostatic Head 300–600 mm H₂O 1,000–3,000 mm H₂O 3,000–20,000+ mm H₂O Breathability (MVTR) Extremely high (close to that of the original fabric) Moderate (1,000–1,200 g/m²/24h) Relatively low (200–500 g/m²/24h) Impact on Hand Feel Almost none Slightly stiffer Moderately stiffer, while retaining elasticity Weight Increase Extremely light (+1–3 g/m²) Light (+20–60 g/m²) Moderate (+30–80 g/m²) Durability Prone to wear; requires regular maintenance 3–5 years, with hydrolysis risk 5–8+ years, with excellent hydrolysis resistance Processing Difficulty Low Low Medium to high (requires seam taping or welding) Environmental Attributes Transitioning toward fluorine-free formulations Transitioning from solvent-based to water-based formulations Recyclable thermoplastic material Typical Applications Casual backpacks, linings, foldable bags Commuter backpacks, travel bags, school bags Outdoor bags, diving bags, professional equipment   In summary, the three processes show a clear stepwise difference in waterproofing performance: DWR-treated fabrics will eventually allow water to penetrate the textile structure during prolonged rainfall;  PU-coated fabrics can block liquid water, but may leak under high water pressure or where the coating has been damaged;  TPU laminated fabrics can provide a reliable waterproof barrier in the vast majority of non-immersion applications.    For Rucksack OEM manufacturers, this means that waterproof specifications must be established according to the product’s actual usage scenarios, rather than blindly pursuing the highest possible numerical rating.   III.  Selection Recommendations for Bag Manufacturing 3.1 Backpack Backpacks are one of the product categories where all three waterproofing processes are most widely applied, because backpacks with different market positions have vastly different waterproofing requirements. Urban Commuter Backpacks (20L–30L) typically use a combination of “PU coating + DWR surface treatment.” Rainfall in urban environments is generally short-duration and moderate, making PU coating sufficient for most situations; DWR helps maintain a dry, clean, and attractive appearance on the fabric surface. This combination achieves an optimal balance among cost, performance, and hand feel, making it a standard configuration for backpack suppliers producing mid-range commuter backpacks. Outdoor Hiking Backpacks (40L–65L) face more demanding environmental challenges. The outer fabric may use ripstop nylon + DWR, while high-wear areas such as the bottom and side pockets may use TPU laminated fabric or a thickened PU coating. Some high-end technical backpacks add a TPU laminated waterproof liner inside the main compartment (similar to a dry-bag construction), creating a dual layer of protection: “rain protection on the outside, waterproofing on the inside.” Water Sports Bags / Diving Bags must meet genuine waterproofing standards. These products typically use fully TPU-laminated fabric, combined with welded seams, water-resistant zippers (such as YKK Aquaguard), and a Roll-Top Closure design. For these types of products, the production line at a bag factory needs to be equipped with high-frequency welding equipment rather than relying on traditional sewing machines.   3.2 Handbags and Purses The waterproofing requirements of handbags and purses are often less apparent, but they are equally important. Business Handbags focus on appearance and texture. They typically use leather-textured fabrics with PU coating or high-density polyester, combined with a DWR surface treatment. Since business scenarios rarely involve heavy rain or immersion, the waterproofing capability provided by PU coating is more than sufficient. Fashion Handbags for Women can use a lighter DWR treatment, or even rely solely on the fabric’s high-density weave to slow down moisture penetration. This is because the waterproofing requirements of fashion handbags are typically limited to “accidental splashes,” while overly heavy coatings can compromise the fabric’s delicate hand feel. Travel Bags and Sports Bags tend to favor PU or TPU solutions because they need to cope with unpredictable liquid exposure in a variety of environments, including airports, train stations, and gyms. In particular, the bottom area can be reinforced with TPU laminated fabric, which not only improves abrasion resistance but also effectively prevents water stains and moisture from the ground from penetrating into the bag, thereby extending the service life of the bag. Beach Bags are primarily used for short-term outdoor leisure activities and often come into contact with wet sand on the beach and splashes of seawater from swimming pools. Therefore, they typically use a TPU laminated waterproofing solution, which can effectively prevent water and moisture from penetrating and soaking personal belongings. At the same time, the TPU laminated layer also makes it easier to quickly clean off sand particles and salt residue afterward.  3.3 Cosmetic Bags and Toiletry Bags Cosmetic bags and toiletry bags are among the smallest bag categories, but their waterproofing requirements are particularly unique. Unlike backpacks and handbags, which primarily need to deal with “external rainwater,” the main threat for cosmetic bags comes from internal leakage. A bottle of foundation that tips over, a tube of sunscreen that bursts under pressure, or a leaking bottle of perfume can ruin all the items inside the bag and may even damage other belongings packed in the same suitcase. Therefore, the waterproofing logic of cosmetic bags and organizer bags is “from the inside out.”   Cosmetic Bags: For Cosmetic Bag OEM manufacturers, the fabric selection for cosmetic bags needs to meet three requirements simultaneously: refined appearance, leak protection on the inside, and easy cleaning.   The outer fabric typically uses a DWR surface waterproof treatment, which preserves the fabric’s glossy appearance and delicate hand feel while also providing protection against splashes from bathroom sinks.   The layer that truly takes on the primary waterproofing responsibility is the lining layer. Mid-range cosmetic bags commonly use a “PU-coated lining” construction. This approach keeps costs under control and effectively prevents liquid penetration, but after prolonged use, the lining may swell or undergo surface degradation due to exposure to oils, essential oils, and alcohol-based ingredients found in cosmetics.   Some high-end products instead use a TPU laminated lining, which offers significantly better chemical resistance than PU. It provides stronger resistance to essential oils and alcohol-based cosmetics and can also be made into a seamless inner liner through high-frequency welding, completely eliminating the risk of leakage through needle holes. Toiletry Bags Compared with cosmetic bags, toiletry bags are closer to the positioning of a “soft waterproof case.” Since they directly carry liquid personal-care products, TPU laminated fabric + water-resistant zipper + roll-top closure has become a standard configuration for high-end products.   TPU’s hydrolysis resistance is particularly important in this application. Toiletry bags are often used in high-humidity environments such as bathrooms, where the aging rate of PU coatings can accelerate significantly. For Toiletry Bag OEM buyers targeting European and American markets, toiletry bags made with TPU laminated fabric can not only pass more stringent waterproof tests (such as IPX4 splash-water testing) more easily, but also have a greater chance of receiving positive “leak-proof” feedback from customers based on their actual user experience.     IV.  Waterproof Performance Testing Standards and Interpretation In custom communication within the bag industry, “waterproof” is an overused and often ambiguous term. After understanding the conventional waterproofing processes, let us now look at the standardized tests used in the industry to define and verify waterproof performance.   4.1  Hydrostatic Head Test The Hydrostatic Head Test is the most basic and widely used method for measuring a fabric’s resistance to liquid water penetration. The test principle involves securing a fabric specimen onto a fixture with a standardized test area, then applying water pressure to one side of the fabric at a constant rate and recording the pressure height at which water penetrates through to the opposite side of the fabric (measured in millimeters of water column, mm H₂O).   The major standards include: l AATCC 127 (American Association of Textile Chemists and Colorists): The test pressure increases at a rate of 60 mbar/min, and the method is suitable for routine evaluation of most bag fabrics. l ISO 811 (International Organization for Standardization): Similar in principle to AATCC 127, but with slightly different pressurization rates and specimen dimensions. European customers typically require test reports based on this standard. l JIS L 1092 (Japanese Industrial Standard): Widely used throughout Asian supply chains. Method A is the low-pressure method, while Method B is the high-pressure method. High-end outdoor bags often require Method B data.   4.2  Spray Test The Hydrostatic Head Test measures a fabric’s resistance under static pressure, but in actual use, rainwater comes into contact with the surface of a bag through dynamic impact. The Spray Test is designed to simulate this scenario.   l AATCC 22 and ISO 4920 are the most commonly used spray test standards. During testing, 250 mL of water is sprayed from a fixed height (typically 150 mm) onto a fabric specimen positioned at a 45° angle. The specimen is then evaluated by comparing the wetted area on its surface with a standard wetting rating scale from 1 to 5, with 5 being the best rating.   l The core value of DWR coating is most clearly demonstrated in the Spray Test. A nylon fabric treated with a high-quality DWR finish will cause water droplets to roll off after spraying, leaving almost no wetting on the specimen surface and potentially achieving a 4–5 rating. By contrast, the same fabric after DWR failure will allow water to spread rapidly across the surface and penetrate into the textile structure, potentially resulting in a rating as low as 1–2.   4.3  Rain Test Both of the tests above use fabric as the test subject, but the ultimate waterproof performance of a bag depends on the systematic performance of “fabric + construction.” The Rain Test (AATCC 35) places the entire bag or sewn fabric assembly in a simulated rainfall environment, spraying water at a specified angle and flow rate to evaluate leakage at structurally vulnerable areas such as seams, zippers, and corners.   A TPU laminated fabric may have a hydrostatic head value as high as 5,000 mm, but if the seams are not sealed with seam tape after sewing, water may first penetrate through the seams during the rain test. Therefore, the Rain Test serves as a bridge connecting “material performance” with “finished-product performance.”   4.4  Moisture Vapor Transmission Rate In the outdoor backpack sector, consumers often discuss “waterproofing” and “breathability” as opposing characteristics. However, these two properties need to be quantified through different tests. Moisture Vapor Transmission Rate (MVTR) measures a fabric’s ability to allow water vapor to pass through, typically expressed in g/m²/24h. l ASTM E96 (Cup Method) and JIS L 1099 (Calcium Chloride Method / Moisture Permeability Cup Method) are the major testing standards. l DWR-treated fabrics have the highest MVTR, generally close to that of the original untreated fabric; PU coatings significantly reduce moisture vapor transmission; and TPU laminated fabrics using dense, non-microporous films typically have the lowest MVTR.   4.5  Reading Test Reports and Applying Them to Quality Control A qualified waterproof fabric test report should contain at least the following information: Test standard and method number (e.g., AATCC 127-2017)  Test conditions (temperature, humidity, and pressurization rate)  Specimen description (fabric specifications, coating/lamination type)  Test results (raw data and ratings)  Testing laboratory qualifications (CNAS, CMA, or an internationally recognized third-party laboratory)    In actual production, manufacturers should implement an incoming material inspection system. When fabric enters the warehouse, hydrostatic head should be sampled and tested according to AATCC 127. This pre-production material verification can identify waterproofing failure risks at an early stage of manufacturing and prevent large-scale rework.   In this regard, Synberry Bag, a source factory specializing in bag manufacturing for 30 years, conducts standardized waterproof testing to confirm performance parameters before each new product is launched, ensuring that the waterproof performance of the final delivered products remains stable and meets customer order requirements, while avoiding customer complaints caused by missing testing procedures. Image showing SYNBERRY BAG conducting hydrostatic pressure tests on each batch of waterproof materials before launching new products.   V. FAQ Q1: What is the difference between PVC waterproofing and PU waterproofing? A: PVC (Polyvinyl Chloride) and PU (Polyurethane) are two completely different polymer systems, and they differ significantly in waterproofing applications for bags. Chemical Structure and Environmental Performance: PVC contains chlorine in its molecular chain and requires the addition of plasticizers (such as phthalates) and stabilizers (which may contain heavy metals) during production. When incinerated, it may release harmful substances such as dioxins. EU REACH regulations impose strict restrictions on phthalates and heavy metals in PVC products, and some countries have already restricted the use of PVC in food-contact products and children’s products. PU does not contain chlorine and offers greater formulation flexibility. Water-based PU has significantly better environmental performance than solvent-based PVC. Hand Feel and Low-Temperature Performance: PVC film tends to have a relatively stiff hand feel and a strong plastic-like feel. In low-temperature environments (below 0°C), it becomes noticeably harder and may even become brittle, making it prone to creasing or cracking when bent. PU coatings and TPU films remain flexible at low temperatures, making them more suitable for bags that require frequent bending or are intended for use in cold regions. Waterproofing and Durability: PVC offers excellent waterproofing, with hydrostatic head values easily exceeding 10,000 mm. However, PVC’s hydrolysis resistance is actually inferior to that of TPU. Long-term exposure to oils or high temperatures may cause plasticizer migration and surface stickiness. PU offers a moderate level of waterproofing (1,000–3,000 mm) but carries a risk of hydrolysis; TPU, meanwhile, offers overall superior performance to both PVC and traditional PU in terms of waterproofing, hydrolysis resistance, and low-temperature toughness.   Q2: Can consumers restore DWR after it fails? A: Yes, but the effectiveness is limited. DWR is a surface treatment, and once it loses effectiveness, it can be restored using commercially available DWR sprays (such as Nikwax TX.Direct or Grangers). The restoration process typically involves: cleaning the fabric → low-temperature tumble drying or ironing to activate the fibers → evenly applying a DWR restoration treatment → applying low-temperature heat again to cure the treatment. However, self-restoration is generally less effective than factory-level pad application or spraying processes, and frequent restoration may alter the fabric’s hand feel.   Q3: Is there any way to remedy PU coating that has undergone hydrolysis and become sticky? A: Once PU coating has undergone obvious hydrolysis (surface stickiness, powdering, or peeling), it constitutes irreversible chemical degradation and cannot be repaired through simple cleaning or recoating. For brands, prevention is better than remediation. During the procurement stage, bag factories should be required to use hydrolysis-resistant PU, with polyether-based formulations preferred over polyester-based formulations. During storage, warehouse temperature and humidity should also be controlled, with a recommended relative humidity below 60% and temperature below 25°C. For inventory products showing early signs of hydrolysis, isolation and evaluation of the scrap rate are the only appropriate quality-control measures.   Q4: Can the three waterproofing processes be used together? A: Yes, and this is very common in actual production. A typical “sandwich” construction consists of: DWR water repellency on the face of the fabric → PU coating or TPU lamination on the back of the fabric → seam tape sealing at the seams. This combination is not simply an addition of performance; rather, the functions are complementary: DWR reduces the amount of water reaching the waterproof barrier and extends the service life of the PU/TPU layer; PU/TPU provides the actual waterproof barrier; and seam tape eliminates structural leakage. For brands, however, combining multiple solutions significantly increases both cost and process complexity, so whether it is worthwhile should be determined according to the product’s market positioning.   Q5: Is TPU laminated fabric really more environmentally friendly than PU-coated fabric? A: From a material-property perspective, TPU is a thermoplastic material and can theoretically be recycled and reprocessed, whereas PU coating is a thermosetting/reactive system that becomes difficult to separate and recycle once cured. However, “more environmentally friendly” is a full-life-cycle question. TPU laminated fabric requires more energy during production, and the composite structure of TPU and fabric also makes actual recycling more difficult. For brands, rather than focusing excessively on “which one is more environmentally friendly,” it is more practical to clearly restrict harmful substances (such as PFAS, phthalates, and heavy metals) in procurement contracts and prioritize suppliers that have obtained relevant environmental certifications.   Q6: Are waterproof zippers necessary? Can ordinary zippers with storm flaps replace them? A: This depends on the product’s target waterproofing level. Ordinary zippers have gaps between their teeth, which may allow water to penetrate once hydrostatic pressure exceeds 300–500 mm. Waterproof zippers (such as YKK Aquaguard and Vislon waterproof series) use PU-coated zipper teeth or TPU-laminated zipper tapes to raise the waterproof performance of the zipper area to a level comparable to that of the fabric. An external Storm Flap can provide a certain degree of protection against rainwater, but it cannot adequately handle strong wind-driven rain or liquid contact when the bag is turned upside down. For commuter bags positioned at the “rain-resistant” level, a storm flap + ordinary zipper is a cost-effective solution. For diving bags or canyoning bags positioned at the “waterproof” level, a waterproof zipper or Roll-Top Closure is a structural element that cannot be compromised.   Conclusion DWR coating, PU lamination, and TPU composite technology together form a complete technical spectrum in the bag industry, ranging from “water repellency” to “waterproofing.” There is no absolute hierarchy of advantages and disadvantages among them; rather, the key lies in how well each technology matches the product’s positioning, usage scenario, cost budget, and environmental requirements.   As waterproofing technology continues to evolve, DWR is becoming more environmentally friendly, PU is becoming more durable, and TPU is becoming lighter and thinner. As a key link in the bag manufacturing chain, we have always maintained close attention to these technological developments, helping brands transform advances in materials science into greater competitiveness for their end products.     Author        
1 2 3 4 5 6 7 8 9 10 11
A total of11pages
Contact Us
Address : Unit 905, Block B, Jinri Building, No. 88 Anling Second Road, Huli District, Xiamen, Fujian, China
Get in Touch

Please Read On, Stay Posted, Subscribe, And We Welcome You To Tell Us What You Think.

Linkedin WhatsApp Facebook instagram

Copyright @2024 Synberry Bag & Package Products Co.,Ltd All Rights Reserved. Network Supported

Sitemap / Blog / Xml / Privacy Policy

Contact Us

Contact Us
Hi there, I hope you're having a lovely day! Thank you for reaching out to us at Synberry --- where 30 years of craftsmanship meets everyday style. With three decades of expertise in bag manufacturing, we don't just make bags --- we build trust, stitch by stitch. Whether you're looking for timeless design, durable quality, or a partner who truly understands your needs,feel free to talk to us.
submit

home

products

WhatsApp

Contact Us