china backpack manufacturer
Home

Synberry

Synberry

  • Why Are Brands Choosing PU Leather for Cosmetic Bags?
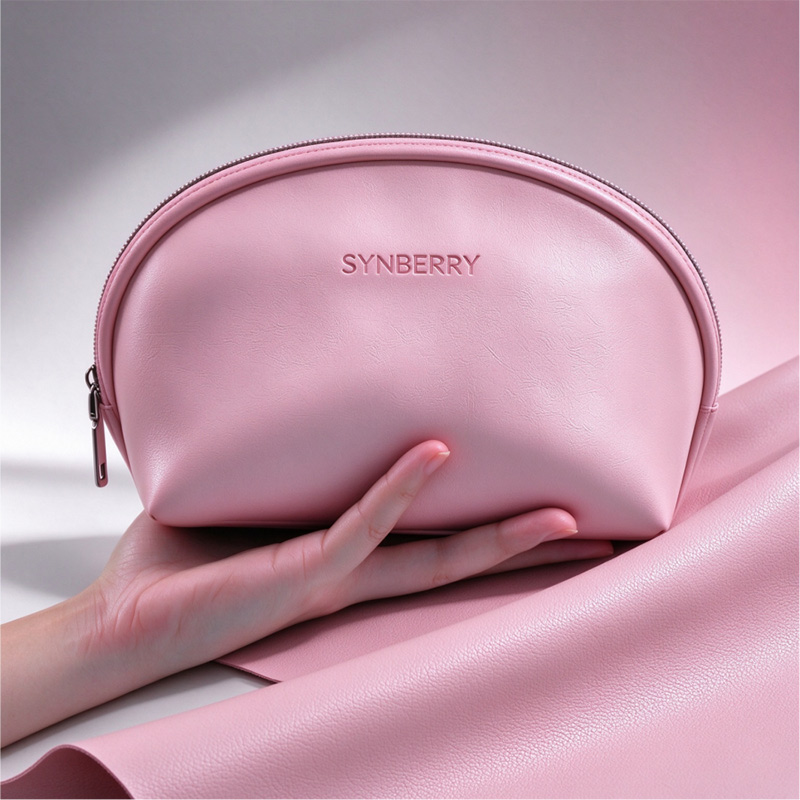
    Why Are Brands Choosing PU Leather for Cosmetic Bags? Oct 30, 2026
    Why are more and more brands choosing PU leather for cosmetic bags? The answer is simple — PU leather offers a good balance of practicality, appearance, and cost: Water-Repellent and Easy to Clean: Its surface does not easily absorb water. When exposed to small amounts of toner, lotion, or foundation, stains can usually be wiped away with a damp cloth, reducing the risk of liquids penetrating the material. Good Abrasion Resistance: When placed in a handbag or suitcase for everyday use, PU leather can withstand a certain degree of friction and compression. It is less likely to develop pilling as quickly as ordinary fabric. Rich Textures and Colors: PU leather can be made in various finishes, including glossy, matte, and pebbled textures. It is also available in a wide range of colors, combining the look of leather with fashionable design possibilities. Soft and Easy to Process: It is convenient for sewing, embossing, hot stamping, and creating different bag shapes. It is also suitable for designs featuring zippers, compartments, and linings. Lightweight and Cost-Effective: Compared with genuine leather, PU leather is generally lighter and more cost-effective. It also does not require complicated leather care and maintenance. Higher Material Utilization: Its relatively consistent width and performance help reduce cutting waste, making it suitable for mass production.     Table of Contents • What Is PU Leather? • What Are the Different Surface Finishes of PU Leather? • What Factors Affect the Quality of PU Leather? • How Do We Help Beauty Brands Find the Right PU Leather? • Frequently Asked Questions About Custom Leather Bags / PU Cosmetic Bags • Conclusion   1. What Is PU Leather? PU leather generally refers to artificial leather or synthetic leather products that use polyurethane (commonly abbreviated as PU) as the primary coating or film-forming material. It typically uses woven fabric, knitted fabric, non-woven fabric, or microfiber fabric as its base material. Through processes such as coating, impregnation, lamination, embossing, and surface finishing, it is transformed into a sheet material with the appearance and feel of genuine leather. By applying embossed patterns such as pebbled grain, crosshatch grain, or Nappa grain, PU leather can achieve different leather styles and appearances.   Therefore, PU leather is not natural leather processed from animal hides, nor should it simply be regarded as equivalent to all types of "faux leather." For example, PVC artificial leather also has a leather-like appearance, but its primary coating material, hand feel, flexibility at low temperatures, and processing methods differ from those of PU leather.   Key Advantages: For OEM cosmetic bag manufacturing, the value of PU leather lies in its material structure: the base fabric provides basic dimensional stability and tensile strength, while the polyurethane surface layer is responsible for the hand feel, abrasion resistance, water repellency, and overall appearance. This material structure is highly compatible with the usage environment of cosmetic pouches.   Cosmetic pouches frequently come into contact with foundation, lipstick, toner, and other skincare products. In addition, they must withstand frequent opening and closing, everyday carrying, and compression inside luggage. Therefore, they need to be easy to clean while maintaining a certain degree of flexibility and abrasion resistance.   Compared with ordinary uncoated fabrics, PU leather surfaces are generally less likely to absorb moisture and stains. Minor water stains or cosmetic residue can usually be wiped away with a slightly damp, soft cloth. Compared with genuine leather, PU leather is generally lighter, and its colors, textures, and batch-to-batch consistency are easier to control. It also does not require complicated leather care and maintenance.   2. What Are the Different Surface Finishes of PU Leather? Surface finishing of PU leather can be understood as a series of processes applied after the polyurethane coating has been formed. Through techniques such as embossing, printing, coating, film lamination, and functional finishing, these processes modify the texture, color, gloss, hand feel, and durability of the material. In actual production, multiple finishing techniques are often combined.   2.1 Texture Finishes 2.1.1 Embossing Embossing creates surface textures using embossing rollers or release paper. It is one of the most common surface treatment methods. This process enhances the leather-like appearance and can, to some extent, minimize the visual impact of minor scratches and creases. Common textures: Pebbled grain, crosshatch grain, and crocodile grain.     Special Embossed Patterns: Such as woven patterns, fabric-like textures, wheat-ear patterns, V-shaped patterns, geometric patterns, and wave patterns.   2.1.2 Plain Grain Finish This finish retains a delicate, smooth, and even surface, although it may also feature very subtle natural textures (such as Nappa grain). It is suitable for minimalist cosmetic bags and provides an ideal surface for screen printing, hot stamping, and logo embossing. However, scratches may be more noticeable on this type of surface.   2.1.3 Suede and Matte Velvet Finish This finish creates a soft, matte appearance with a delicate hand feel, producing an effect similar to suede leather. It is suitable for products with a natural, understated style.   2.2 Coating and Surface Finishes 2.2.1 High-Gloss and Mirror Finishes Through surface coating or film lamination, this treatment creates a high-gloss, patent-leather-like appearance. It delivers a strong visual impact and is suitable for gift cosmetic bags, limited-edition fashion collections, and small beauty pouches.   2.2.2 Matte Finish This finish reduces surface reflection, giving the leather a softer and more understated appearance. It is suitable for products positioned around minimalist, natural, or understated luxury styles.   2.2.3 Skin-Like and Soft-Touch Finish By adjusting the surface-layer formulation and coating process, this treatment gives the material a finer, smoother, and more pleasant hand feel. It is suitable for small makeup pouches that emphasize tactile quality.   2.2.4 Oil-Waxed and Vintage Finish This treatment gives the leather a natural sheen, variations in color depth, or a vintage leather appearance. It is suitable for travel toiletry bags and vintage-inspired collections.     2.3 Color and Decorative Finishes 2.3.1 Pearl and Metallic Finishes Pearlescent or metallic effects are incorporated into the surface finish to create appearances such as pearl white, champagne gold, and rose gold. These finishes are commonly used for makeup gift cosmetic bags, holiday gift sets, and loyalty program gift products.   2.3.2 Two-Tone and Multi-Tone Finishes By using differences between the base color and surface color, this treatment creates varying shades in the recessed and raised areas of the texture, enhancing the three-dimensional and vintage effects. The resulting color layers are richer and more dimensional, making this finish suitable for highlighting brand color schemes or coordinating with seasonal theme colors.     2.3.3 Printed Finishes Through screen printing, roller printing, or other suitable printing techniques, brand graphics, animal patterns, or geometric designs can be applied to the surface. This finish is suitable for themed collections and collaboration products.     2.3.4 Laser and Iridescent Finishes Special coatings or films are used to create reflective effects that change depending on the viewing angle. These finishes are suitable for products targeting younger consumers and trend-conscious markets.     2.4 Film Lamination Finishes Transparent, colored, or specially designed optical films are laminated onto the surface of PU leather. This process can create mirror, laser, and iridescent effects while also providing additional protection for printed designs or the leather surface     2.5 Functional Finishes In addition to decorative effects, the following post-processing treatments can also be applied according to the product positioning:  Stain-Resistant and Easy-to-Clean Treatment: Reduces the adhesion of water stains and certain types of dirt to the surface, making everyday cleaning easier.  Scratch-Resistant and Abrasion-Resistant Treatment: Improves the surface's resistance to minor friction and scratches. However, this does not mean the material is completely immune to scratches from sharp objects.  Anti-Yellowing and UV-Resistant Treatment: Slows down color changes caused by light exposure. This is particularly important for light-colored, white, and transparent-looking materials.  Hydrolysis-Resistant and Anti-Aging Treatment: Improves the material's stability in hot and humid environments, reducing the risk of coating powdering, cracking, or becoming sticky after long-term use.  Low-Temperature Flexibility Treatment: Reduces the possibility of the leather surface becoming stiff or cracking when bent in low-temperature environments. It is suitable for products intended for sale or transportation in cold regions.   Some of these performance characteristics come from surface finishing, while others are jointly determined by the base fabric, polyurethane formulation, and overall manufacturing process.   Before customizing a PU leather cosmetic bag, beauty brands can communicate their product usage scenarios and specific requirements to the factory in advance to determine which additional post-processing treatments are necessary.   However, it is important to note that additional post-processing treatments generally require a relatively high minimum order quantity (MOQ). Standard in-stock materials already provide basic stain resistance, water resistance, and abrasion resistance.   3. What Factors Affect the Quality of PU Leather? The quality of PU leather is not determined simply by whether it is "thick enough" or "soft to the touch." The durability of a PU leather material depends on the combined effects of its polyurethane formulation, base fabric, coating structure, and manufacturing processes.   3.1 Polyurethane Resin Formulation Polyurethane resin is the core raw material used to form the PU leather film. Its type, molecular structure, and formulation directly affect the material's softness, resilience, abrasion resistance, hydrolysis resistance, and aging resistance. Polyurethane can be divided into two main systems. Different types of polyurethane have different levels of stability in hot and humid environments: Polyester-Based Polyurethane: This is one of the more commonly used types in the market. It generally offers good abrasion resistance, mechanical strength, and a substantial, full hand feel. However, the ester bonds in its molecular structure are relatively sensitive to hot and humid environments. Prolonged exposure to high temperatures and humidity, or repeated contact with water-based skincare products, may cause hydrolysis. This can lead to a sticky surface, coating powdering, or peeling. Polyether-Based Polyurethane: Due to the relatively greater stability of the ether bonds in its molecular structure under hot and humid conditions, this type generally offers better hydrolysis resistance and low-temperature flexibility. Under the same usage conditions, polyether-based PU leather is less likely to experience coating powdering, stickiness, or significant reductions in strength caused by prolonged moisture exposure. Therefore, for toiletry bags that frequently come into contact with water-based skincare products such as toners and lotions, or are used in high-humidity regions or near bathrooms for extended periods, polyether-based polyurethane is a more reliable resin choice.   3.2 Base Fabric Quality The base fabric serves as the "skeleton" of PU leather. Common types include woven fabric, knitted fabric, non-woven fabric, and microfiber fabric. The main effects of base fabric quality on PU leather can be seen in the following aspects: Influencing Factor Impact on PU Leather Quality Potential Problems if Not Properly Controlled Fiber and Weaving Structure Affects the material's tensile strength, tear strength, and bursting strength, as well as its softness, flexibility, and resistance to deformation. The material may easily deform or tear under stress, or become damaged prematurely in high-stress areas such as handles and bag corners. Weight and Density Affect the material's thickness and fullness, resilience, structural support, and dimensional stability. The material may be too soft or thin, causing the bag to lose its shape or collapse. Uneven density may also result in inconsistent performance across different areas. Base Fabric Uniformity Affects coating distribution, finished material thickness, and hand-feel consistency throughout the entire roll. Uneven surface thickness, horizontal lines or streaks, and inconsistent softness or stiffness may occur, affecting cutting and sewing stability. Bonding with the Coating Determines the adhesion strength between the base fabric and polyurethane coating, affecting folding resistance and peel resistance. Blistering, delamination, peeling, or coating detachment in folded areas may occur during use.     Therefore, even if two types of PU leather use similar surface coatings, differences in their base fabrics can result in significantly different softness, deformation resistance, and durability in the finished materials.   3.3 Coating Structure and Uniformity PU leather is generally not made of just a single layer of coating. Instead, it typically consists of multiple layers, including the base fabric, impregnation layer, foam layer, surface layer, and decorative finish layer. The specific structure varies depending on the manufacturing process and product type.   The following aspects require particular attention:  Is the coating thickness uniform? Areas with coatings that are too thin are more susceptible to wear, while coatings that are too thick may negatively affect flexibility and hand feel.  Are the different layers firmly bonded? Insufficient adhesion can easily lead to peeling, blistering, and delamination.  Is the foaming process uniform? The foam cell structure affects softness, resilience, and folding performance.  Are there any pinholes, bubbles, or impurities? These defects not only affect the appearance but may also become starting points for subsequent cracking or wear.   3.4 Manufacturing Processes Even when using the same raw materials, different manufacturing conditions can result in different product quality. Key parameters include coating application weight, oven temperature, drying time, production speed, tension control, impregnation level, and curing conditions.  Insufficient drying or curing may result in residual odors, a sticky surface, or unstable coating performance.  Improper temperature or production speed control may cause abnormal foam cell structures, surface defects, shrinkage, or color differences.  Excessive production tension may also lead to inconsistencies in material width, thickness, and texture.   Therefore, PU leather quality cannot be evaluated based on hand feel and thickness alone. It is also closely related to polyurethane composition, coating structure, and post-processing techniques.   For a wash bag, what truly affects the user experience is whether the material can maintain its appearance and structural stability after repeated opening and closing, contact with cosmetics, and everyday carrying.   5. How Do We Help Beauty Brands Find the Right PU Leather? 5.1 Thickness Recommendations The common thickness range of PU leather used for bags is approximately 0.6–1.2 mm. Some travel bags and backpacks that require greater structural support use thicker specifications. For makeup bags, the following thickness ranges can serve as a reference:   Finished PU Leather Thickness Material Characteristics Typical Applications Approx. 0.5–0.7 mm Lightweight and soft, easy to fold and sew. Lipstick pouches, flat zipper bags, lightweight promotional gift bags. Approx. 0.6–0.8 mm Offers a relatively balanced combination of softness and durability. Everyday handheld cosmetic bags, small Boston-style bags, standard travel storage bags. Approx. 0.8–1.0 mm Provides enhanced structural support and a fuller bag shape. Semi-structured box bags, wide-opening toiletry pouches, cosmetic bags with compartments. Approx. 1.0–1.2 mm and above Provides stronger structural support and a more rigid, structured appearance. Box-shaped cosmetic bags, cosmetic cases, display-oriented products, and premium gift collections.   The thickness mentioned here generally refers to the finished material thickness, including both the base fabric and the coating. Even two materials with the same thickness may have completely different hand feels due to differences in base fabric density and coating softness or stiffness.   When customizing leather cosmetic bags, thicker material is not necessarily better. The appropriate specifications should be selected according to the product positioning.   For example, soft, small-sized pouches can prioritize lightweight materials and good folding performance. Larger, three-dimensional bags, on the other hand, may require a combination of thicker outer materials, padding, reinforcement materials, or internal support boards to achieve the desired shape.   Using excessively thick materials for small bags may actually result in bulky corners, difficult zipper operation, and challenges when turning the bag inside out during manufacturing.       5.2 Appearance and Texture Recommendations After confirming the bag structure, we can further match the appropriate leather surface finish:  Plain Grain and Fine Nappa Grain: Suitable for minimalist designs and ideal for screen printing, hot stamping, and logo embossing.  Pebbled Grain and Fine-Grain Textures: Offer a stronger leather-like appearance and are suitable for everyday retail products and travel storage bags.  Crosshatch Grain: Creates a clean and refined visual effect, making it suitable for structured and sophisticated cosmetic bags.  Pearlescent, Metallic, Mirror, and Iridescent Finishes: Suitable for holiday limited editions, collaborative collections, and themed gift boxes.  Decorative Textures Such as Crocodile Grain and Woven Patterns: Help strengthen collection recognition and visual identity. However, the proportion and scale of the texture on small cut panels should be carefully evaluated.   Colors can be developed based on brand color cards, Pantone color codes, or physical samples. At the same time, gloss level, embossing depth, and logo application techniques should also be confirmed.   For dark-colored embossed materials, mirror-finish materials, or specially laminated materials, the adhesion performance of hot stamping and printing should be evaluated in advance. This helps avoid situations where the material looks attractive but cannot consistently reproduce the brand logo.   5.3 Verifying Actual Performance Through Sample Testing Material swatches can only be used for preliminary selection. Actual product sampling is necessary to identify potential problems during manufacturing and use.   We pay particular attention to the forming results around sewing lines, edge binding, bag turning, corners, and zipper areas, checking for wrinkles, whitening, corner bursting, or coating cracks.   Considering the actual usage environment of leather cosmetic bags, we can also evaluate the following aspects according to the product positioning:  Color transfer after dry and wet rubbing tests.  Surface and printed-layer conditions after repeated folding and bending.  Surface abrasion resistance, scratch resistance, and coating adhesion performance.  Anti-yellowing and stain-resistance performance of light-colored materials.  Risks of stickiness, powdering, or delamination after exposure to hot and humid aging conditions.  Whether water stains and common cosmetic residues can be easily cleaned.   5.4 Supporting Compliance Testing Based on the Target Market We assist brands in identifying the testing items required according to their target markets and intended consumer groups. Compliance requirements for cosmetic bags and their materials are not entirely the same across different markets.  For products entering the European Union market: Attention should generally be paid to the restricted substance requirements under the REACH Regulation, including restrictions on certain phthalates, heavy metals, and specific azo dyes.  For products entering the United States market: Attention should generally be paid to the chemical substances listed under California Proposition 65, particularly phthalates and lead content. Although Proposition 65 does not directly prohibit the sale of products, it requires warning labels when exposure to listed chemicals exceeds applicable safe-harbor levels. Brands should therefore reserve sufficient space for relevant warnings on product packaging and product pages in advance.  For Asia-Pacific and Southeast Asian markets: Compliance requirements are relatively diverse and vary by country. Some countries refer to the EU REACH Regulation or International Organization for Standardization (ISO) testing methods, but enforcement levels and the scope of random inspections may differ.   For brands exporting products to multiple regions, we recommend prioritizing a relatively comprehensive testing plan, using EU standards as the foundation and supplementing them with specific testing items required by individual destination markets.   This approach can help reduce duplicated testing costs while lowering the risk of products failing random inspections in specific markets.   5.5 Maintaining Consistent Mass Production Quality Through a Standardized Quality Control System SYNBERRY BAG has established in-depth partnerships with dozens of beauty brands worldwide and has consistently followed a strict quality control system, which includes the following procedures:  Incoming Material Inspection: All PU leather raw materials entering our factory are inspected by batch before being stored in the warehouse. We check color, thickness, texture, and hand feel, and compare them with customer-approved samples and standard reference samples. Only after confirming that the materials meet the approved sample specifications can they proceed to the cutting stage.  Cutting and Sewing In-Process Inspection: During the cutting stage, we inspect cut panels for color differences, texture misalignment, surface scratches, and coating peeling. We also verify the cutting layout and material orientation to avoid mixing cut panels from different batches within the same bag.   During the sewing stage, we follow a three-step inspection process: First Article Approval – In-Process Inspection – Finished Product Sampling Inspection.   The first article must be checked to ensure that the bag shape, stitching, zipper position, edge binding, and logo application meet the required specifications. During  in-process inspections, we pay particular attention to sewing tension consistency and whether any stress-bearing areas show signs of pulling or deformation.    Pre-Packaging Inspection: Before packaging, each cosmetic bag is inspected for surface defects, loose threads, dirt, glue overflow, zipper smoothness, lining condition, and hardware durability. We also verify product quantities and label information to prevent mixed colors, incorrect styles, or discrepancies between labels and actual products.  Pre-Shipment Sampling Inspection: Before shipment, a final random inspection is conducted according to AQL standards or an inspection plan mutually agreed upon by both parties to ensure that the appearance and functionality of the entire batch meet the required specifications.   Relevant inspection records, retained samples, and test reports are archived according to each order, making it easier to manage repeat orders, trace customer complaints, and compare different production batches in the future.   Through this closed-loop management system, covering everything from raw materials to finished products, we can minimize the impact of batch variations on material performance to the greatest extent possible.   For beauty brands, choosing a professional cosmetic pouch factory like this not only helps reduce the risk of rework and quality issues at later stages but also contributes to maintaining consistent brand presentation and delivering a stable consumer experience in the market.     6. Frequently Asked Questions About Custom Leather Bags / PU Cosmetic Bags Q1: Is PU leather genuine leather? No. PU leather is generally made using woven fabric, knitted fabric, non-woven fabric, or microfiber fabric as its base material, combined with polyurethane coating, impregnation, and surface finishing processes. It can replicate the textures and hand feel of natural leather, but it is not genuine leather made from processed animal hides.   Q2: Are PU leather and microfiber leather the same material? No. Microfiber leather, also known as microfiber synthetic leather, uses ultra-fine fibers woven through specialized textile processes as its base material. It is then combined with polyurethane resin impregnation and surface coating treatments. Its overall structure and performance are closer to those of natural leather.   PU leather, on the other hand, can use a much wider range of base fabrics, including not only microfiber fabrics but also ordinary woven fabrics, knitted fabrics, and non-woven fabrics. The most noticeable differences between the two are their prices and performance:  Microfiber Leather: Its tear strength, abrasion resistance, folding resistance, and dimensional stability are generally better than those of ordinary PU leather. Its hand feel is also closer to genuine leather, but its cost is correspondingly higher.  PU Leather: Its advantages lie in the wide variety of available textures, colors, and surface finishes, as well as a broader price range. It can accommodate various product positioning requirements, from lightweight promotional items to mid-to-high-end everyday products.  Appearance and Hand Feel: It can be difficult for ordinary consumers to distinguish PU leather from microfiber leather just by looking at or touching them, because both materials can achieve similar surface finishes, such as pebbled grain, plain grain, and Nappa grain. Microfiber leather is also frequently used to develop highly realistic synthetic leather products.   However, differences gradually become apparent after a period of actual use. Microfiber leather generally demonstrates better stability under repeated bending, long-term friction, and humid conditions, with a lower likelihood of delamination, peeling, or coating powdering.   Q3: What Is the Difference Between PU Leather and PVC Artificial Leather? One of the main differences between the two materials lies in their surface composition. PU leather uses polyurethane as its primary film-forming material, while PVC artificial leather is primarily based on a polyvinyl chloride system.   They have different characteristics in terms of hand feel, weight, low-temperature flexibility, processing methods, and application scenarios. Their actual performance still depends on the specific formulation and manufacturing processes, so it is not accurate to simply assume that one material is superior to the other in every aspect.   Q4: What Are Water-Based PU and Solvent-Based PU? The key difference between water-based PU and solvent-based PU lies primarily in the medium used to disperse or dissolve polyurethane during production and processing. Water-based PU uses water as its dispersion medium, while solvent-based PU uses organic solvents as its medium. Both can be used to manufacture PU leather.   However, being "water-based" or "solvent-based" does not directly determine whether the final product is of better or inferior quality. Their main characteristics are as follows: Main Characteristics of Water-Based PU:  Uses water as its dispersion medium, which generally helps reduce the use of organic solvents and related odors.  With an appropriate formulation and manufacturing process, it can achieve a soft and delicate hand feel.  Has relatively high requirements for temperature and humidity conditions in the production environment, drying conditions, and equipment stability.  Water evaporation generally requires a sufficiently thorough drying process, which may increase drying time and energy consumption.   Main Characteristics of Solvent-Based PU:  Has relatively mature film-forming and processing adaptability, making it suitable for a wide variety of textures and surface finishes.  Requires strict control over coating, drying, solvent recovery, and production safety management.  If production control or post-processing is insufficient, it may result in odors, volatile substances, or specific residual solvents. • Its compliance and environmental performance depend on the specific formulation, residual solvent control, exhaust gas treatment, and testing results. It cannot be judged solely by whether it is solvent-based.   Q5: Are PU Leather Makeup Bags Waterproof? PU leather surfaces generally offer a certain degree of water repellency and resistance to liquid penetration. Small amounts of water can usually be wiped away promptly.   However, this does not mean that PU leather is completely waterproof. Moisture may still enter the inside of the cosmetic bag through needle holes, edge binding, seams, or zippers. Therefore, prolonged immersion in water is not recommended.   Q6: Why Does a PU Leather Bag Peel or Crack? Common causes include insufficient adhesion between the coating and base fabric, long-term wear, repeated bending, hydrolysis and aging caused by hot and humid environments, as well as high temperatures, light exposure, or improper storage.   Surface wear does not necessarily mean that the base fabric has already been damaged. However, once the coating begins to powder or peel over a large area, it is generally difficult to restore through simple cleaning.   Q7: How Long Does a PU Leather Makeup Bag Generally Last? There is no fixed lifespan that applies to all types of PU leather.   The service life is affected by factors such as resin formulation, base fabric, coating structure, surface finishing, frequency of use, and storage conditions.   Standard PU leather products on the market generally last around 2–3 years under normal use, while hydrolysis-resistant PU leather can extend this period to approximately 3–5 years without deterioration or peeling.   Q8: What Is the Typical MOQ for Custom PU Cosmetic Bags? The minimum order quantity (MOQ) is generally affected by whether the material is available in stock, whether custom colors or additional surface treatments are required, as well as the bag structure and manufacturing complexity.  Using In-Stock PU Leather and Standard Bag Designs: The MOQ is relatively low, generally starting at around 500 pieces.  Custom Development Requirements: If the order involves new embossing plates, custom embossing patterns, special color dyeing, or specialized finishing treatments, the production line usually needs to be arranged separately. In such cases, the MOQ often increases to more than 1,000 pieces.   Q9: How Long Does Sampling and Mass Production Usually Take for PU Leather Cosmetic Pouches? The sampling lead time for standard designs is generally around 7–15 working days. The exact timeframe depends on the complexity of the bag design, material availability, and logo application requirements.   If new cutting dies, customized hardware, or multiple pattern adjustments are required, the lead time will increase accordingly.   The mass production lead time is generally around 30–40 days. However, production schedules may be further extended during public holidays, peak seasons, or when special post-processing treatments are required.   When planning a product launch, we recommend that brands reserve at least 4–6 weeks of additional buffer time for sample approval and potential revisions. This helps prevent minor design adjustments from affecting the overall product launch schedule.   7. Conclusion For beauty brands, customizing a PU leather cosmetic bag is not simply about choosing a reliable cosmetic bag supplier. It is also a form of proactive management of the overall brand experience.   Every detail of a cosmetic bag, from its appearance and hand feel to zipper smoothness and lining neatness, contributes to the consumer's overall impression of the brand.   Only when the right materials are selected and manufacturing processes are consistently controlled can a product deliver a consistent appearance on retail shelves and a consistent user experience in consumers' hands.   This is also an important foundation for improving repeat purchases and strengthening consumer trust in the brand.       Author        
  • What Is the CPSIA Standard? A Guide to Customizing Children's Bags
    What Is the CPSIA Standard? A Guide to Customizing Children's Bags Sep 29, 2026
    CPSIA, short for the Consumer Product Safety Improvement Act, is a consumer product safety law enacted by the U.S. Congress in 2008 and enforced by the U.S. Consumer Product Safety Commission (CPSC). Its core regulatory scope covers products primarily designed for or intended to be used by children 12 years of age or younger. For children's bag manufacturers and exporters, the CPSIA establishes strict mandatory standards. The key requirements include restrictions on lead content, a prohibition on the use of certain phthalates, and ensuring that products comply with applicable physical and mechanical performance testing requirements. Any bag product sold in the U.S. market that is primarily intended for use by children 12 years of age or younger must undergo testing and certification by a third-party laboratory and be accompanied by a Children's Product Certificate (CPC) to ensure compliance. Table of Contents CPSIA Testing Requirements for Children's Bags Compliance Guidelines Throughout the Children's Bag Customization Process How We Integrate Compliance into Every Production Run Common Compliance Misconceptions and Risk Mitigation Frequently Asked Questions About Children's Bag OEM Conclusion   I.  CPSIA Testing Requirements for Children's Bags CPSIA applies to all bags that are “primarily designed for children 12 years of age or younger,” such as children's backpacks, school bags, lunch bags, pencil cases, and other similar products. The specific core testing requirements are as follows:   1. 1 Chemical Testing (Core Requirements) For textiles and hardware products, the truly important measurable limits are lead and phthalates. Lead is regulated in two ways: first, the total content in the substrate; and second, the lead content in any surface coating or paint. The eight restricted phthalates apply to plasticized components, such as PVC zipper pulls, printed labels, and soft rubber trim. 1.1 1 Lead Content (Section 101) Test Item Limit Coatings/Paint (surface coating) ≤ 90 ppm Substrate (fabrics, plastics, metal zippers, buttons, webbing, prints, and all other accessible components) ≤ 100 ppm Scope of Application and Exemptions: These limits apply to all accessible components of bags, including outer fabric, lining, zipper pulls, fasteners, decorative elements, sewing thread, and printing inks. If the product contains electronic components or certain special metal alloys, special attention must be paid to whether their lead content complies with the standard. It is worth noting that the CPSIA has a clear definition of “accessibility”: If a component is completely covered by a layer of protective material, and the protective layer does not become damaged or detached after undergoing the reasonable use and abuse tests specified by the CPSC, such as tension, torque, drop, and other tests, the internal component may be exempt from lead content testing. Conversely, if the protective layer fails and causes the internal material to become exposed, it must meet the requirement of ≤ 100 ppm (that is, the content of the substance must not exceed 1 gram per kilogram of material). In addition, for internal components that cannot avoid contact through physical isolation, strict compliance is required regardless of whether they are easily accessible to children. Test Methods: CPSC-CH-E1001/E1002/E1003 series (XRF screening + wet chemical confirmation). Zipper pulls, buttons, hardware, inks, and printed materials are high-risk areas. 1.1.2  Phthalates (Section 108) The 8 restricted phthalates (DEHP, DBP, BBP, DINP, DIBP, DPENP, DHEXP, DCHP) are each limited to ≤ 0.1% (1000 ppm), meaning that the content of each substance must not exceed 1 gram per kilogram of material. Scope of Application and Exemptions: Not all children's bag components are subject to this restriction. Section 108 primarily regulates children's toys that can be “put into the mouth” and certain child care articles. For ordinary children's bags, such as school bags and backpacks, phthalate testing is generally not mandatory if their intended use does not include chewing or sucking by children. However, if a bag contains soft plastic components, such as transparent windows made of PVC, soft rubber handles, decorative soft plastic pendants, etc., and these components may be placed in the mouths of children under 3 years of age, they must comply with the requirements. In addition, the CPSC in recent years. Note: If the products are also sold in California, laboratories typically additionally test for DIDP (Prop 65), resulting in a total of 9P.   1.2 Mechanical and Physical Safety (Relevant Regulatory Requirements) Small Parts Testing: Products intended for use by children under 3 years of age must not contain detachable small parts (16 CFR 1501) and must be evaluated after undergoing use and abuse testing. Sharp Edges/Points: (FHSA / 16 CFR 1500.48/49) Choking Hazard: If plastic packaging bags are included, a choking hazard warning must be provided (additional requirements apply to bags with an opening circumference ≥ 380 mm)   1.3  Flammability Performance Textile fabrics must comply with the requirements of 16 CFR 1610 (flammability of clothing textiles), Class 1 or Class 2. Most backpack fabrics generally fall into exempt categories, but the specific determination must be made based on the fabric composition.   1.4  Certification and Labeling Requirements (Not Testing Items, but Equally Mandatory) Third-Party Testing: Testing must be conducted by a CPSC-accepted laboratory. CPC Certificate (Children's Product Certificate): Issued based on the test report and required for each shipment. Permanent Tracking Label (Tracking Label): Must indicate the manufacturer's/private labeler's name, production date, and batch information. eFiling: Starting July 8, 2026, importers must electronically declare CPC/GCC data through the Customs ACE system   II.  Compliance Guidelines Throughout the Children's Bag Customization Process   Step 1: Clearly Define the Product Classification This is the stage where problems are most likely to occur. The compliance costs of an “adult bag” and a “children's bag” can differ significantly. Children's cartoon patterns, children's sizes, and marketing materials featuring school-related scenarios → are very likely to be classified as children's products; If marketing materials (Amazon listings, packaging designs) are targeted at children under 12 years of age, platforms may also require CPSIA compliance. It is recommended to confirm the product positioning for the target market before creating samples, in order to avoid being required to complete a full set of additional tests only at the shipping stage.   Step 2: Lock in Compliant Materials During the Material Selection Stage Key Risk Materials Compliant Alternatives PVC-coated fabric Eco-friendly PU coating Soft rubber raised-print designs Silicone printing (food-grade), embroidery Metal zippers/snap buttons without test reports Hardware from well-known brands (YKK, SBS, etc.) Unknown-source inks/dyes Require suppliers to provide SDS or test reports   Step 3: Arrange Third-Party Testing Select a CPSC-recognized laboratory, such as SGS, Intertek, TÜV, or BV; Testing process: XRF preliminary screening for lead → wet chemical confirmation if the level exceeds the limit; phthalates are tested using GC-MS; One SKU for one bag design and one report; changes to fabrics/hardware require re-evaluation.   Step 4: Prepare the CPC Certificate and Tracking Label CPC Certificate: Issued based on the test report, must accompany each shipment, and must be retained by the importer/seller for recordkeeping; Permanent Tracking Label: The manufacturer's name, production date, production batch/origin information must be sewn or molded onto the inside of the bag; Pay attention to timing: Starting in 2026, U.S. Customs has implemented an electronic filing system (eFiling). Importers of children's products are required to submit CPC data through the ACE system, and a paper certificate alone is no longer sufficient.   III.  How Do We Integrate Compliance into Every Production Run?   SYNBERRY BAG adopts a four-stage quality control system—IQC (Incoming Quality Control), IPQC (In-Process Quality Control), FQC (Final Quality Control), and OQC (Outgoing Quality Control)—to move compliance checkpoints forward into the production process, ensuring that non-compliant materials are identified before they are sewn into thousands of finished products. During the Incoming Quality Control (IQC) stage, fabrics, hardware, zippers, and accessories are inspected upon arrival: factory and laboratory certificates are verified, and samples are taken for preliminary screening so that non-compliant batches can be rejected before the materials reach the cutting table. During the In-Process Quality Control (IPQC) stage, the cutting, printing, and sewing processes are monitored throughout production to ensure that only approved inks and hardware are used and to promptly identify any unauthorized substitutions made during production. During the Final Quality Control (FQC) stage, finished bags are inspected for workmanship, dimensions, and functionality against the approved and signed golden sample. Finally, during the Outgoing Quality Control (OQC) stage, packed cartons are inspected before shipment to confirm that the test reports, tracking labels, and carton markings are fully consistent with the goods. Compliance measures are incorporated into every stage, rather than being merely a superficial formality. This is the key to transforming a quality control system into a compliance system. Throughout the entire bag production process, SYNBERRY BAG consistently follows the AQL 1.5/4.0 sampling standard under ISO 2859, ensuring consistency and stable compliance across mass-produced products.   IV.  Common Compliance Misconceptions and Risk Mitigation During the actual school bag OEM production process, many brand owners have misunderstandings about CPSIA compliance and often encounter a series of problems due to overlooking important details. Below are several common misconceptions and practical response recommendations from a school bag manufacturer:   4.1  Misconception One: A “Smaller Version of an Adult Product” Does Not Need to Comply Many companies believe that as long as the packaging does not state “for children only,” the product can be exported as an adult product. However, the CPSC applies a “primary use” determination principle. If the product's size is clearly suitable for children under 12 years of age, such as mini backpacks or cartoon-style crossbody bags, or if children are shown using the product in marketing images, the product may still be classified as a children's product even without an explicit statement. Response Strategy: Clearly define the target audience during the product design stage. If the product is indeed intended for adults, avoid using juvenile cartoon imagery, bright color combinations, and children's size specifications. Marketing materials should also strictly avoid using child models or suggestive wording that implies the product is intended for children.   4.2  Misconception Two: A Voluntary Test Report Provided by the Supplier Is Sufficient for Customs Clearance Some suppliers provide a voluntary test report (Test Report) rather than compliance documentation based on the mandatory requirements of the CPSIA. Although well-known laboratories may have CPSC-recognized accreditation, if the report does not explicitly reference the relevant CPSIA sections, such as Section 101 and Section 108, or does not cover all accessible components, the report cannot serve as a valid basis for issuing a CPC certificate. In addition, products from different batches and products with different fabric colors need to be tested separately; an old report cannot simply be reused. Response Strategy: When commissioning testing, explicitly require a test report that complies with CPSIA standards, and ensure that the test samples cover all color and material variations. After receiving the report, carefully verify the test standard numbers and applicable limits, and then prepare the CPC certificate accordingly.   4.3 Misconception Three: Tracking Labels Can Be Added Later or Ignored A permanent tracking label (Tracking Label) is a mandatory CPSIA requirement. It must be directly printed or sewn onto the product, and the information must be clear, legible, and resistant to washing and abrasion. The CPSC explicitly requires tracking labels to be “permanent,” meaning that they cannot be removed without damaging the product and must withstand normal use and washing without becoming illegible or falling off. Simple stickers, hangtags, or easily erasable printing do not meet the requirements. Response Strategy: Integrate the tracking information into the care label, interior lining print, or molded/embossed marking at the early stage of bag production. Ensure that the label is positioned discreetly but remains easy to locate, that the text is clear and legible, and that abrasion-resistant and wash-resistant materials and processes are used.   V. Frequently Asked Questions About CPSIA Compliance During Children's Bag OEM   Q1: If my bags are primarily sold to adults but are occasionally used by children, do they need to comply with CPSIA? A: The key factor is the determination of the product's “primary use.” The CPSC will comprehensively consider the product's design, packaging, marketing and promotional materials, and consumer perception. If the product is clearly geared toward children under 12 in terms of size, patterns (such as cartoon characters), or functional design, or if children are shown in e-commerce listings or advertisements or the marketing materials imply scenarios involving children's use, the product is very likely to be classified as a children's product even if it is not explicitly labeled “for children only,” and will therefore be required to comply with CPSIA. If the target group is indeed adults, the product design and marketing should be strictly de-child-oriented to avoid misclassification.   Q2: Does the same bag need to be tested separately in different colors? A: Yes. CPSIA compliance follows the “one product, one test” principle, but more accurately, it is “one material formulation, one test.” If bags in different colors use fabrics and accessories from the same batch and with the same formulation (with only the color masterbatch being different), and the supplier can provide evidence proving that the pigment composition is consistent, some laboratories may allow combined testing or differentiated assessment. However, to minimize risks, especially when colors involve different suppliers or different materials (such as glossy versus matte finishes), it is recommended to sample and test each significantly different color/material combination separately to ensure that all variants comply with the limits for lead and phthalates.   Q3: Can the CPC certificate be issued by the manufacturer itself? A: The CPC certificate must be issued by the U.S. importer or the domestic manufacturer, but its contents must be based on qualified test results issued by a CPSC-accepted third-party laboratory. A manufacturer cannot issue a CPC solely on the basis of its internal quality inspection reports. The certificate must include product information, a list of applicable safety regulations, a summary of test results, testing laboratory information, and the contact information of the person issuing the certificate. Although the certificate is signed by the brand owner or importer, its legal validity depends entirely on the supporting third-party test data.   Q4: If my bag has detachable accessories, do these accessories need to be tested separately? A: Yes. CPSIA requires testing of all “accessible components.” If an accessory is sold as part of the bag and may detach after normal use or abuse testing and become accessible to a child, both the accessory itself and its attachment components must comply with the limits for lead and phthalates. If the accessory is determined to have an independent toy function, it may also be subject to more stringent ASTM F963 toy standard testing. It is recommended to treat the accessory as an integral part of the bag during the design and testing stages for comprehensive evaluation, or separately confirm its compliance.   Q5: What are the costs and timelines for CPSIA compliance testing? A: Testing costs are not fixed and depend on the complexity of the product, the number and types of materials involved, and the fee structure of the selected laboratory. Generally speaking, basic chemical testing (lead and phthalates) costs anywhere from several hundred to several thousand U.S. dollars. If the bag has a complex structure and contains multiple types of hardware, printed materials, or soft plastic/rubber components, separate sampling and testing may be required, resulting in higher costs. Regarding the testing timeline, routine testing usually takes 5–7 business days. During peak seasons or when complex wet-chemical confirmation testing is required, the process may be extended to 10–15 business days. Therefore, sufficient testing time must be reserved at the beginning of the project to avoid shipment delays caused by waiting for test reports. Expedited services are usually available, but they will incur additional fees.   VI. Conclusion CPSIA compliance is not only a legal threshold for entering the U.S. market, but also a core competitive advantage for brands seeking to build consumer trust and mitigate recall risks. For children's bag manufacturers and exporters, compliance should not be regarded as a temporary remedial measure before shipment; instead, it should run throughout the entire product lifecycle, including product design, material selection, production, and certification. Controlling material safety at the source, clearly defining product positioning during the design stage, implementing permanent tracking labels during production, and completing rigorous third-party testing and CPC certification before customs clearance are key steps to ensuring a smooth supply chain. With the full implementation of the eFiling electronic filing system in 2026, requirements for data transparency and compliance traceability will become even stricter. Only by integrating compliance awareness into daily operations can companies navigate intense international competition steadily and achieve sustainable business growth. Synberry Bag has been specializing in various bag OEM/ODM services for more than 30 years. We are familiar with international standards and regulations such as CPSIA and have established mature compliance management systems and supply chain management capabilities. We are committed to providing global customers with one-stop solutions covering everything from design and development to production and manufacturing.   Author        
  • Is Vegetable-Tanned Leather good for handbag manufacturing?
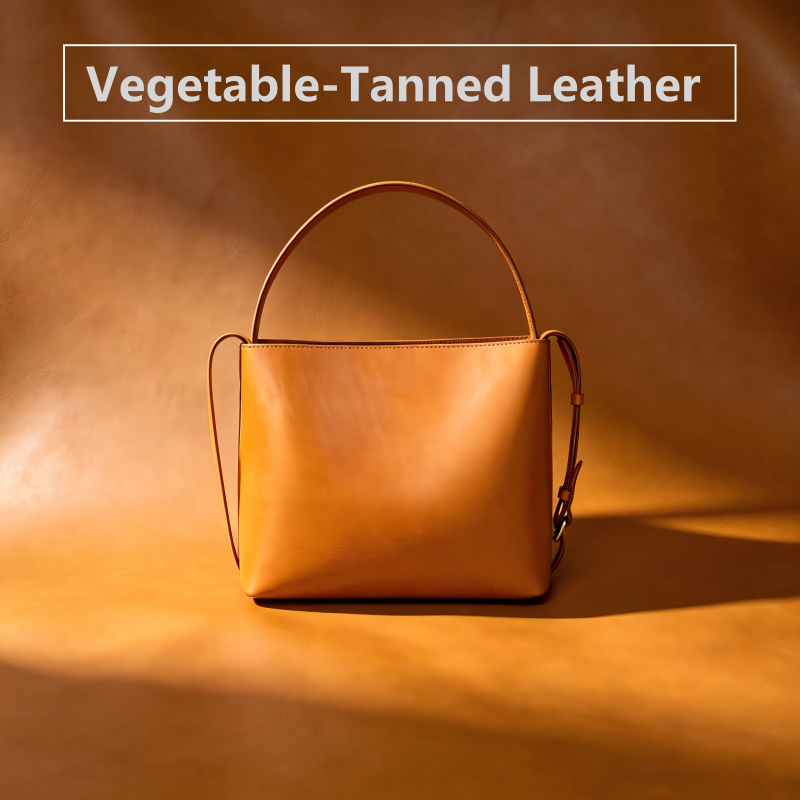
    Is Vegetable-Tanned Leather good for handbag manufacturing? Jul 28, 2026
    Vegetable-tanned leather is often chosen because it can do something that many coated or synthetic materials cannot: it records the marks of use. Sunlight gradually deepens its color. Frequent use makes the surface become smoother over time. Natural oils from the hands create darker tones on the corners, handles, folds, and around buckles. This visual characteristic has made vegetable-tanned leather a favorite among many leather brands, gift companies, and vintage-style product developers. They value the unique “aging journey” of vegetable-tanned leather—every finished product gradually develops a one-of-a-kind patina through everyday use, creating a distinctive imprint that belongs solely to its owner. This evolving character is also the most unique feature that sets it apart from other types of tanned leather. Table of Contents: What Is Vegetable-Tanned Leather?  Vegetable-Tanned Leather vs. Chrome-Tanned Leather  Advantages and Limitations of Vegetable-Tanned Leather  What Is Vegetable-Tanned Leather Suitable for in the Bag Industry?  Logo Techniques Suitable for Vegetable-Tanned Leather  FAQ    I. What Is Vegetable-Tanned Leather? Vegetable-tanned leather is leather that has been transformed from prepared animal hides into stable leather through a controlled tanning process using plant-derived tanning agents (tannins). When an animal hide is first removed, it is essentially a piece of protein that will naturally decompose. To transform it into durable leather, tanning agents must create cross-links with the collagen fibers in the hide. Tannins bond with the collagen structure, improving the leather's resistance to decay while giving it its characteristic firmness, natural grain, excellent workability, superior edge quality, and distinctive aging properties. In modern leather manufacturing, the dominant chrome tanning process uses trivalent chromium salts, offering fast production, lower costs, and a softer finished leather. Vegetable tanning, by contrast, returns to a method that has been used by humans for thousands of years. Natural tannins are extracted from plant materials such as bark, wood, leaves, fruits, and seed pods, allowing the leather fibers to gradually "set" over the course of several weeks or even months. This slow process is the foundation of every defining characteristic of vegetable-tanned leather. Because of the extended tanning period and the deep penetration of tannins, the fiber structure of vegetable-tanned leather is thoroughly transformed. The finished leather is firm, dense, and capable of being burnished to achieve a smooth, mirror-like edge—something that is difficult for chrome-tanned leather to accomplish. At the same time, because the process does not rely on heavy synthetic resin finishes, the surface of vegetable-tanned leather retains its most natural, uncoated appearance: pores remain clearly visible, while natural scars, growth marks, and vein patterns are all openly displayed.   II. Vegetable-Tanned Leather vs. Chrome-Tanned Leather For many buyers encountering vegetable-tanned leather for the first time, the biggest question is: How is it different from ordinary full-grain cowhide? In reality, the difference is determined the moment the tanning process is completed. Comparison Vegetable-Tanned Leather Chrome-Tanned Leather (Mainstream) Tanning Agent Plant-derived tannins (natural) Trivalent chromium salts (chemical) Tanning Time Several weeks to several months 1–3 days Finished Feel Firm and structured, initially quite stiff Soft, supple, and flexible straight out of production Surface Appearance Minimal or no finish, leaving a natural, "bare-faced" look Usually coated with a finish that can conceal imperfections Color Stability Darkens and changes with sunlight and use, developing a patina Color is fixed after production and remains relatively stable Edge Finishing Can be burnished and polished to a smooth, mirror-like finish Typically requires edge paint to cover the edges Water Resistance Poor; exposure to water may cause discoloration and stiffening Better; water tends to bead up and roll off naturally Suitability for Mass Production Lower Higher One common misconception should be clarified: vegetable-tanned leather and full-grain leather are not opposing concepts. Full-grain describes which part of the hide is used—the topmost layer that has not been sanded or buffed. Vegetable tanning, on the other hand, describes the tanning method. A piece of full-grain cowhide can be either vegetable-tanned or chrome-tanned. That said, high-quality vegetable-tanned leather on the market is typically made from premium full-grain hides. Since vegetable-tanned leather does not rely on heavy surface coatings to conceal imperfections, the inherent quality of the hide is fully visible on the finished surface.   III.  Advantages and Limitations of Vegetable-Tanned Leather Vegetable-tanned leather is not a miracle material. It is much like a piece of jade that requires careful nurturing—its strengths and weaknesses are equally distinctive. Advantages 1. A Unique Character Shaped by Time The greatest appeal of vegetable-tanned leather lies in its ability to develop over time. Natural vegetable-tanned leather begins with a light beige tone and gradually darkens through exposure to sunlight, body heat, and the absorption of natural oils from the hands. Over time, it evolves into caramel or honey tones, eventually developing a patina that is unique to its owner. This "the more you use it, the better it looks" characteristic is something no heavily finished leather can truly replicate. 2. A Naturally Sustainable Story The tannins used in vegetable tanning are derived from renewable plant sources. Compared with wastewater from chrome tanning, the waste liquor generated during vegetable tanning is far more biodegradable. For brands that emphasize sustainability, vegetable-tanned leather is a naturally eco-friendly material that requires little explanation. 3. Burnishable, Mirror-Like Edges Under the influence of high-density tannins, the fibers of vegetable-tanned leather become compact enough that the edges can be burnished and polished to a mirror-like finish, much like wood. This allows premium handcrafted bags to achieve clean, refined edges without the need for edge paint—one of the primary reasons why many artisan leatherworkers favor vegetable-tanned leather. 4. Proven Long-Term Durability Although it feels firm when new, vegetable-tanned leather gradually softens with use while retaining exceptional fiber strength. A well-maintained vegetable-tanned leather bag can often last more than a decade. Limitations 1. Highly Sensitive to Water and Oils Because vegetable-tanned leather has no waterproof surface coating, even a single drop of water can leave a dark watermark. Natural skin oils, sunscreen, and even the indigo dye from denim can penetrate the leather and cannot be wiped away. To enthusiasts, these marks are badges of time and character; to many everyday consumers, they may simply be viewed as unacceptable stains. 2. Difficult to Maintain Consistent Color Between Batches The color of vegetable-tanned leather continues to evolve even after production. Two hides from the same batch, stored on opposite sides of a warehouse, may develop noticeably different shades after just three months. 3. Less Suitable for High-Speed Mass Production Its firm structure increases resistance during sewing, while edge finishing requires multiple rounds of sanding, waxing, and polishing. As a result, the labor time required is typically much longer than that for chrome-tanned leather.   IV.  What Is Vegetable-Tanned Leather Best Suited for in the Bag Industry? Based on the characteristics discussed above, vegetable-tanned leather has a well-defined comfort zone when it comes to bag manufacturing. Ideal Applications Small Leather Goods: Card holders, key cases, pen sleeves, and leather charms. Their compact size makes natural imperfections easier to manage while showcasing the beautifully burnished edges that vegetable-tanned leather is known for.  Structured Bag Designs: Satchels, briefcases, and vintage messenger bags. These styles take full advantage of vegetable-tanned leather's natural rigidity, allowing the bags to maintain their shape without collapsing.  Limited Editions and Commemorative Collections: The leather's natural grain and its ability to develop a unique patina over time create a sense of exclusivity and rarity, making it an excellent choice for special collections.        Less Suitable Applications Soft, Large Bags: Tote bags and shopping bags. Vegetable-tanned leather is relatively stiff when new, and repeated bending across large panels can create permanent creases that cannot be reversed.  High-Frequency Everyday Commuter Bags: Bags that are exposed daily to crowded public transportation, rain, and frequent contact with different surfaces. Under these conditions, vegetable-tanned leather's delicate nature becomes much more noticeable.  Fast Fashion, High-Volume Products: Because of its evolving color, lower production efficiency, and higher cost compared with chrome-tanned leather, vegetable-tanned leather is not well suited to the rapid production cycles and aggressive pricing strategies required by fast-fashion brands.  Many handbag brands that prioritize customer experience intentionally introduce natural vegetable-tanned leather as part of their core product line, encouraging customers to "grow" their bags through everyday use. This unique interaction between the owner and the leather creates a highly personal ownership experience, significantly enhancing product appeal, encouraging word-of-mouth discussions, and strengthening customer loyalty. It is also one of the reasons why vegetable-tanned leather has become an outstanding choice for boutique brands seeking meaningful differentiation.   V.  Logo Techniques Suitable for Vegetable-Tanned Leather Vegetable-tanned leather has little to no chemical surface finish. Its firm fiber structure, ability to absorb moisture and oils, and tendency to change color when exposed to heat give it both distinct advantages and clear limitations when it comes to logo application. Below are several methods that have been proven effective in our production experience, as well as techniques that should be avoided. Recommended Methods 1. Blind Embossing / Debossing This is the logo technique that best complements the character of vegetable-tanned leather. A heated brass die is used to apply pressure, creating either a recessed or raised impression on the leather surface. Since no additional material is applied, the logo becomes an integral part of the leather itself. As the leather develops its patina over time, the embossed edges gradually become smoother and develop a subtle natural sheen. Practical Considerations: Because vegetable-tanned leather is relatively firm, embossed edges appear sharper and more defined than on chrome-tanned leather, making this technique ideal for fine lettering and geometric linework.  Temperature must be carefully controlled (typically 80°C–120°C). Exceeding 150°C can leave dark brown scorch marks around the edges of the impression, which are especially noticeable on natural, undyed leather.  Deep embossing (greater than 1 mm) may affect the flatness of the reverse side. If the logo is placed on a large front panel of the bag, the visibility of the impression on the back should be evaluated.  2. Hot Foil Stamping (Gold or Silver) Hot foil stamping adds a refined metallic accent to vegetable-tanned leather. However, the leather's unfinished surface is a double-edged sword: because the foil comes into direct contact with the leather fibers, its adhesion is often less reliable than on chrome-tanned leather with a finished coating. Practical Considerations: Use premium foil specifically designed for leather, with fine pigments and strong adhesion. Standard foil intended for paper is prone to peeling on vegetable-tanned leather.  Avoid stamping over natural scars, vein marks, or other areas where the fiber structure is loose, as the foil may lift or peel away together with these imperfections.  Hot foil stamping generally produces better visual contrast on dark-colored vegetable-tanned leather (such as tea-core or brown leather) than on natural undyed leather. 3. Leather Carving / Tooling If there is one technique that was practically made for vegetable-tanned leather, it is leather carving (tooling). Vegetable-tanned leather is firm, has a dense fiber structure, and becomes highly moldable when dampened. As carving tools pass over the surface, they produce crisp, well-defined patterns that retain their shape. The carved design can then be further enhanced with dyeing, gilding, antique finishing, or other decorative treatments. Practical Considerations: Leather carving demands exceptionally high-quality hides. Only Grade A full-grain vegetable-tanned leather can produce clean, sharp cuts. Areas with scars or loose grain are prone to becoming fuzzy after carving.  The process is entirely handcrafted, making mass production extremely inefficient. A single panel with a complex carved pattern may require several hours to complete, making this technique unsuitable for high-volume production.  After carving, the leather should be properly shaped and treated for moisture resistance. Otherwise, the recessed carved areas may be susceptible to mold growth in humid environments. 4. Laser Engraving Laser engraving can reproduce intricate vector artwork and even grayscale effects without the need for custom tooling. However, vegetable-tanned leather reacts very differently to laser engraving than synthetic leather or chrome-tanned leather. Practical Considerations: The laser burns the tannins within the leather, causing the engraved area to turn dark brown or black. This creates strong visual contrast on natural, undyed vegetable-tanned leather, so the final appearance should always be evaluated through sampling before production.  Since no custom die is required, laser engraving eliminates tooling costs. For small-batch custom orders, it is often more cost-effective than embossing, making it an excellent option for boutique brands and bespoke products. 5. Metal Badges / Nameplates Metal badges or nameplates are attached to vegetable-tanned leather using rivets, screws, or stitching. This approach overcomes some of the limitations of the leather itself, making it possible to achieve multicolor finishes, three-dimensional effects, and even illuminated designs. Practical Considerations: Because vegetable-tanned leather is relatively firm, pilot holes should always be punched before installing rivets. Driving rivets directly into the leather may cause the fibers to crack.  Metal and leather have different coefficients of thermal expansion. In environments with significant temperature fluctuations, rivet holes may gradually enlarge over time, causing the hardware to loosen. Using washers is recommended to improve long-term stability.  The edges of the metal badge should be chamfered or rounded to prevent them from cutting into or wearing through the leather surface during prolonged use.  For stitched metal badges, stitch spacing must be planned with great precision. Needle holes in vegetable-tanned leather are permanent and cannot recover, so the stitching must be positioned correctly on the first attempt.  Not Recommended: Screen Printing and Pad Printing We do not recommend applying screen printing or pad printing directly onto the surface of vegetable-tanned leather. The reasons are straightforward: Vegetable-tanned leather has little to no surface coating, making ink absorption difficult to control. As a result, the printed graphics are prone to bleeding and feathering.  Vegetable-tanned leather continues to darken and absorb oils over time. As the leather naturally ages, the printed design ages with it, often leading to noticeable color inconsistencies after just a few months.  While applying a surface sealing coating before printing can improve ink adhesion, it also defeats the very qualities that make vegetable-tanned leather desirable in the first place. The coating compromises its signature natural, uncoated appearance, as well as its breathability.   FAQ Q1: Which is better: vegetable-tanned leather or top-grain leather? A: These are not comparable concepts, as they describe different aspects of leather. Top-grain leather refers to the layer of the hide used, while vegetable tanning refers to the tanning process. A piece of top-grain leather can be either vegetable-tanned or chrome-tanned. Although premium vegetable-tanned leather is typically made from high-quality full-grain hides, "vegetable-tanned" does not automatically mean "top-grain." Q2: Is vegetable-tanned leather always more environmentally friendly than chrome-tanned leather? A: In terms of tanning agents, plant-derived tannins are indeed more natural and biodegradable than chromium salts. However, environmental sustainability should be evaluated across the entire product lifecycle. Factors such as wastewater treatment at the tannery, whether the dyes contain heavy metals, and the composition of conditioning oils used during maintenance all play important roles. Whenever possible, it is advisable to source leather from tanneries certified by the Leather Working Group (LWG). Q3: Are vegetable-tanned leather bags waterproof? A: Natural vegetable-tanned leather offers little to no water resistance. Improving its waterproof performance requires applying waterproofing agents or waxes after tanning, but doing so alters the leather's breathability and natural feel while compromising its signature uncoated appearance. If the product is intended for frequent use in rainy conditions, chrome-tanned leather with a protective finish is generally a more suitable choice. Q4: Why does the price of vegetable-tanned leather vary so much? A: The price of vegetable-tanned leather mainly depends on three factors: Hide quality, including the grade of the hide, the presence of scars, and the area of the hide used.  Tanning method and duration, such as traditional pit tanning versus accelerated drum tanning.  Country or region of origin.  Vegetable-tanned leather made from premium hides using traditional long-cycle pit tanning is significantly more expensive than leather produced through faster tanning methods, resulting in noticeable price differences in the final products. Q5: How can you tell if leather is genuinely vegetable-tanned? A: You can identify genuine vegetable-tanned leather using the following four methods: Smell: Authentic vegetable-tanned leather has a distinctive earthy aroma with a subtle natural sweetness. Chrome-tanned leather often has a chemical smell or almost no noticeable scent.  Cut Edge: Examine an unfinished edge. Vegetable-tanned leather typically displays a warm cream or tan color throughout its cross-section. Chrome-tanned leather usually has a bluish-gray cross-section—the characteristic color left by chromium sulfate.  Water Reaction: A small drop of water will immediately darken the surface of vegetable-tanned leather before gradually lightening again as it dries. On chrome-tanned leather, water generally beads up and rolls off the surface.  Feel: Genuine vegetable-tanned leather has a firm, structured feel and is relatively stiff when new, requiring a break-in period. If a product advertised as "vegetable-tanned leather" feels excessively soft and floppy right out of the box, it is worth examining more carefully.  Q6: How should vegetable-tanned leather be cared for? A: Here are some practical care tips to help keep vegetable-tanned leather products in their best condition. Brands are encouraged to include these recommendations in their product care instructions. Avoid getting the leather wet, especially during the first month of use.  Keep the leather away from heat sources and never use a hair dryer to speed up drying.  Do not clean it with synthetic brushes—use only natural-bristle brushes.  If the leather product is used frequently, apply a leather-specific conditioning oil or leather care product once a week.  Wax the leather regularly to maintain its condition and appearance.  Conclusion Vegetable-tanned leather is not an industrial material that can simply be used without consideration. Instead, it is more like a long-term project involving the brand, the manufacturer, and the end user. Its firmness, color changes, visible marks, and evolving patina are both its limitations and its greatest sources of appeal. As an OEM bag manufacturer with more than 30 years of experience, we have always believed that there is no universally "good" or "bad" material—only the material that is best suited for a particular purpose. If your brand is built around speed, novelty, and standardization, vegetable-tanned leather may not be the ideal choice. But if your brand tells a story of time, craftsmanship, texture, and companionship, vegetable-tanned leather may be the most authentic storyteller of all.   Author        
  • How to Choose Leather Materials for Handbags & Proper Care Guide
    How to Choose Leather Materials for Handbags & Proper Care Guide Jul 24, 2026
    Sourcing leather for custom leather handbags is far more than a simple aesthetic choice. It directly determines your production costs, retail pricing strategy and overall brand positioning.   SYNBERRY has accumulated over 30 years of experience in OEM custom leather bag manufacturing, serving clients ranging from emerging startup brands to mature premium and luxury lines.    Most purchasing partners repeatedly raise two core questions: which leather grade fits their product lineup, and how end consumers can properly maintain leather bags.    Drawing on our decades of on-site manufacturing experience, this guide systematically explains leather selection logic and post-sale maintenance knowledge, helping OEM buyers pick matching leather and avoid common care mistakes.   Table of Contents: Ⅰ. Two Core Perspectives to Understand Leather  Ⅱ. Match Leather Types to Different Handbag Styles  Ⅲ. Daily Care Guidelines for Leather Handbags  Ⅳ. Four Core Details to Confirm When Requesting Factory Quotations  Ⅴ. Frequently Asked Questions (FAQ)  Ⅵ. Conclusion   Ⅰ. Two Core Perspectives to Understand Leather We divide leather into two major classification systems: categorization by natural hide layers and categorization by post-tanning processing techniques. The combination of these two dimensions jointly decides leather quality and the final presentation of finished handbags.   1.Classification by Hide Layer Top-grain leather:Top-grain leather is made from the outermost grain layer of animal hide plus part of the underlying fibrous corium layer. Its compact fiber structure delivers outstanding tensile strength, durability, flexibility and stable shape retention, making it the core raw material for all high-end leather goods. Split leather :Split leather refers to the residual fibrous layer separated after removing the top grain layer during splitting. Its loose fiber structure leads to weaker strength, poor durability and faint natural texture, so manufacturers usually add PU coating, PVC coating or suede sanding to improve its appearance and practicality.   2.Classification by Processing Craft Full-grain leather:Full-grain leather ranks as the highest-grade leather material. It fully retains the natural grain surface of raw hide with almost no sanding or surface correction, featuring obvious natural grain, excellent wear resistance, superior breathability and the ability to form unique patina with long-term wear. Every hide carries exclusive natural marks, making each finished bag one-of-a-kind. Corrected-grain leather:Corrected-grain leather is processed by lightly sanding top-grain leather to remove surface blemishes, then embossing uniform artificial grain patterns. It boasts consistent surface appearance, reliable durability and balanced cost performance, which is why most mid-to-high-end leather goods such as business briefcases adopt this material. Coated split leather :Coated split leather is produced by attaching a thin PU or PVC synthetic film to split leather and embossing artificial grain on the surface. Its basic composition is split leather substrate plus synthetic coating, serving as an affordable option with uniform visual effects.   3.Comparison Between Top-Grain Leather and Full-Grain Leather Many buyers confuse the logical relationship between top-grain and full-grain leather; the table below sorts out all core differences clearly:   Comparison Item Top-Grain Leather Full-Grain Leather Definition Leather cut from the outermost grain layer of animal hide Premium subdivision of top-grain leather that fully retains natural grain surfaces Belongs to top-layer hide ✅ Yes ✅ Yes Retain original natural grain Not guaranteed ✅ Fully retains natural pores and grain patterns Surface finishing May include sanding, correction, embossing or heavy coating Minimal processing; only dyeing and light protective finishing Visual appearance Uniform texture, customizable artificial embossed patterns Natural grain variations; every hide panel is unique Durability Good Excellent, featuring the most intact natural fiber structure Breathability Fairly good Superior Softness Fluctuates based on finishing craft Gradually softens and develops natural patina with wear Longevity Lasts multiple years with routine care Remains functional for decades under consistent maintenance Price bracket Mid to high-end Premium tier with higher unit pricing   SYNBERRY Manufacturing Insight: We always recommend full-grain leather for clients developing structured luxury handbags. Natural surface variations are not flaws, but distinctive features that endow each bag with irreplaceable unique value.   Ⅱ.  Match Leather Types to Different Handbag Styles Leather selection cannot rely solely on material cost. Different bag silhouettes and usage scenarios put forward distinct performance requirements for leather, so we summarize a targeted matching rule for buyers’ reference:   Handbag Category Recommended Leather Grade Core Matching Advantages Luxury handbags / Premium women’s designer bags Full-grain leather Develops layered patina and elevates product value over time Business briefcases / Daily commuter totes Top-grain leather Maintains rigid silhouette, durable and cost-efficient Casual crossbody bags / Fashion-forward silhouettes Top-grain leather or split suede Supple touch, diverse styling and flexible design potential Fast-fashion bags / Promotional giveaway handbags Split leather Low production cost with consistent surface finish Travel duffels / Large luggage totes Full-grain or thick top-grain leather Highly abrasion-resistant and builds vintage character with wear   Ⅲ. Daily Care Guidelines for Leather Handbags Standardized consumer care can greatly extend a leather bag’s service life. Well-maintained leather goods effectively boost customer satisfaction and build long-term brand loyalty, and you can print all the practical guidance below on product hang tags or custom care booklets.   1. Regular Daily Care Habits Wipe surface dust and light dirt with a soft dry cloth on a regular basis.  When the bag is not in use, stuff its interior with acid-free tissue paper to fix the original shape and cover the whole bag with a dedicated dust bag for storage. Keep leather goods away from direct sunlight, heat sources and humid environments all the time.   2. Targeted Stain Removal Solutions For water stains, use a dry cloth to blot excess moisture immediately and place the bag in cool ventilated space for natural air-drying; never speed up drying with hair dryers or high-temperature heat sources. For oil stains, spread absorbent cornstarch evenly over stained areas, leave it overnight to absorb grease, then gently brush off residual starch the next morning.  For split suede products, only use professional suede brushes for grooming and avoid direct water scrubbing at all costs.   3. Forbidden Improper Operations Do not rinse or submerge the entire leather bag in water.  Do not accelerate drying through hair dryers, radiators or other heating equipment.  Do not fill bags with newspaper, as printing ink will transfer onto leather under humid conditions and cause permanent stains.     Ⅳ. Four Core Details to Confirm When Requesting Factory Quotations Many buyers only write "leather handbags" in quotation requests, which causes repeated sample revisions and wastes plenty of sampling time. Clearly confirming the following four key information can greatly improve OEM communication efficiency.   1. Clear Leather Grade State the exact leather material without vague general descriptions, including full-grain leather, top-grain leather or split leather.   2. Defined Leather Thickness Mark specific thickness data such as 0.8mm or 1.0mm, as this parameter directly affects the bag’s firmness, structural stability and hand touch.   3. Standard Color Reference Provide official Pantone color codes or physical color swatches for color matching. Physical swatches are far more accurate than digital pictures, since screen display deviation is the top cause of sample rework.    SYNBERRY Insight: Our sample department can customize exclusive color swatches for clients within 5 to 7 working days.   4. Confirmed Surface Finishing Specify the surface finishing: Which embossed grain pattern is required (e.g., pebble grain, cross grain)? Matte or glossy finish?   Ⅴ. Frequently Asked Questions (FAQ) Q1: How do I verify leather sample quality before mass production launches?  A: You need to manually test the leather’s softness and hand feel, observe the density of internal fiber layers, and check the adhesion strength of surface coating. We suggest signing and archiving a complete reference sample set containing leather swatches, color panels and matching metal hardware, which will serve as the unified inspection standard for bulk production.   Q2: Why do minor color discrepancies exist between pre-production samples and bulk goods? A: Leather is a natural raw material, so different hide batches absorb dye unevenly; fluctuations in ambient temperature and humidity will also change dye absorption effects. SYNBERRY archives standard color boards for every production batch and strictly controls color differences within commercially acceptable standards.   Q3: As a brand owner, what supplier qualifications should I prioritize?  A: Apart from factory scale and production capacity, focus on ISO 9001 quality management system certification and BSCI social compliance audit. These two credentials prove the factory meets international standards in quality control, labor protection and environmental compliance.    Q4: How long does OEM leather handbag sampling normally take?  A: Sample development takes 7 to 14 working days after design confirmation; customized embossing or complex structural designs will extend the cycle slightly. International sample shipping requires an extra 3 to 5 working days, and the exact timeline depends on product customization complexity.   Q5: Besides traditional animal leather, are there eco-friendly innovative alternatives?  A: Yes. Numerous mainstream brands adopt bio-based leather materials made from corn fiber, cork and pineapple leaf fiber. These sustainable materials have a lower carbon footprint, cater to the sustainable consumption trends of European and American markets, and create unique differentiated selling points for brands.   Q6: How to handle a leather handbag soaked by rainwater?  A: Immediately blot surface moisture with a clean white cotton cloth instead of hard rubbing, which will push water stains deep into leather fibers. Hang or lay the bag flat in cool ventilated space for full natural air-drying, and never use hot air blowers or direct sunlight to speed up the process. After complete drying, apply a thin layer of leather conditioning cream to nourish the hide.   Q7: Can minor scratches on leather surfaces be repaired?  A: Light scratches can be faded by gentle fingertip massage; friction heat activates natural leather oil to blur superficial abrasions. Deep scratches need professional leather recoloring cream for local touch-up. Remember to test the repair paste on the inconspicuous bag bottom to confirm color matching before processing front surfaces.   Q8: Light-colored leather bags easily get stained. How to prevent and fix color transfer?  A: Prevention is more effective than remediation. Avoid long-term contact between pale leather (white, beige, pink) and dark fabrics especially denim to prevent friction color bleeding, and spray dedicated anti-transfer protective spray for daily use. If color transfer occurs, wipe stained areas in gentle circular motions with leather cleaner and soft cloth right away; consult professional leather care stores if stains cannot be fully removed.   Q9: How frequently should consumers maintain leather handbags?  A: Care cycles depend on usage frequency. Daily commuter bags need full conditioning every 2 to 3 months, while occasionally used bags only require maintenance once every six months. A simple judgment standard: if light finger marks do not fade within several seconds after scratching, the leather lacks natural oil and needs immediate nourishing treatment. Regular maintenance can permanently preserve leather’s soft texture and subtle gloss.   Ⅵ. Conclusion Choosing the right leather is a strategic business decision. The most expensive material is not always suitable for your brand, nor can the cheapest option guarantee market competitiveness. The core selection standard lies in matching leather with your brand positioning, target consumer groups and product usage scenarios.   Picking proper leather only completes half of brand success, and the other critical part is guiding end customers to master standardized leather care methods. Even premium leather will turn dull, dry and cracked after years of neglect, while entry-grade leather can accompany customers for decades with consistent proper maintenance. This is why we elaborate on systematic care guidance above — brand reputation is often built through these small but vital customer experience details.   With over 30 years of OEM handbag manufacturing experience, SYNBERRY provides full-cycle leather solutions for brand partners, covering professional material matching, custom sample development and stable mass production with balanced cost and quality control. We also design exclusive leather care cards, printed hang tags and simplified maintenance instructions tailored to each bag model, so customers can grasp correct protection methods at the moment of purchase.   If you have finished product concepts or design sketches, send them to our technical team. We will provide free leather matching evaluation and cost estimation within 1 to 2 working days.    Contact SYNBERRY today to discuss your leather handbag project, and we will help you source ideal leather materials and deliver reliable long-term care guidance for your bag collection.      Author        
Contact Us
Address : Unit 905, Block B, Jinri Building, No. 88 Anling Second Road, Huli District, Xiamen, Fujian, China
Get in Touch

Please Read On, Stay Posted, Subscribe, And We Welcome You To Tell Us What You Think.

Linkedin WhatsApp Facebook instagram

Copyright @2024 Synberry Bag & Package Products Co.,Ltd All Rights Reserved. Network Supported

Sitemap / Blog / Xml / Privacy Policy

Contact Us

Contact Us
Hi there, I hope you're having a lovely day! Thank you for reaching out to us at Synberry --- where 30 years of craftsmanship meets everyday style. With three decades of expertise in bag manufacturing, we don't just make bags --- we build trust, stitch by stitch. Whether you're looking for timeless design, durable quality, or a partner who truly understands your needs,feel free to talk to us.
submit

home

products

WhatsApp

Contact Us